
Individuelle Pulverbeschichtungsdienstleistungen für Blechteile
SR MFG bietet industrielle Pulverbeschichtungsdienstleistungen für Blechteile, Gehäuse, Paneele, Halterungen, Rahmen und individuelle Metallkomponenten. Von der Musterfreigabe bis zur Serienproduktion kontrollieren wir Schichtdicke, Farbkonsistenz, Abdeckung, Prüfprotokolle und Lieferplanung, um eine stabile OEM-Produktion zu unterstützen.
Unser Pulverbeschichtungsverfahren eignet sich für Kohlenstoffstahl, Edelstahl, verzinkten Stahl und Aluminiumteile. Für Projekte, die optische Konsistenz, Korrosionsbeständigkeit, Montagepassung oder Exportdokumentation erfordern, können wir Ihre Zeichnungen, Oberflächenanforderungen, Farbstandards, Beschichtungsdicken und Prüfkriterien vor der Produktion prüfen.
Schichtdickenkontrolle
Typisch 60 ±10 μm, mit Abdeckung für kritische Bereiche.
Farbkonsistenz
RAL-/Pantone-Abgleich basierend auf freigegebenen Mustern.
Korrosionsvalidierung
Salzsprühtest je nach Projektanforderung verfügbar.
Erhalten Sie ein individuelles Angebot in 24 Stunden
Laden Sie Ihre Zeichnungen zur technischen Prüfung hoch.
Warum Blech pulverbeschichten?
Pulverbeschichtung ist eine praktische Oberflächenlösung für Blechteile, die sowohl Oberflächenschutz als auch konsistentes Erscheinungsbild erfordern. Sie bildet eine dauerhafte Beschichtungsschicht auf Kohlenstoffstahl, verzinktem Stahl, Edelstahl und Aluminiumkomponenten und hilft, Rost, Handhabungsverschleiß, Abplatzungen und langfristige optische Probleme zu reduzieren.
Für OEM-Blechprodukte wird Pulverbeschichtung häufig bei elektrischen Gehäusen, Außengerätegehäusen, industriellen Halterungen, Rahmen, Paneelen und Strukturkomponenten eingesetzt, bei denen Haltbarkeit, Chargenkonsistenz und sauberes Erscheinungsbild wichtig sind.
Korrosionsschutz
Schützt Metalloberflächen vor Rost und Umwelteinflüssen.
Bessere Haltbarkeit
Verbessert die Verschleißfestigkeit und reduziert Abplatzungen und Lackablösung.
Längere Lebensdauer
Hilft, die Produktlebensdauer zu verlängern und Nacharbeit sowie Garantierisiken zu reduzieren.
Ideale Anwendungen
Geeignet für Außengerätegehäuse, Schaltschränke/Gehäuse, industrielle Halterungen und Strukturkomponenten.
Was ist Pulverbeschichtung?
Pulverbeschichtung ist ein trockenes Veredelungsverfahren, das eine dauerhafte Schutzschicht auf Metallteilen erzeugt. Anstelle von Flüssiglack wird ein feines Pulver aus Harzen, Pigmenten, Füllstoffen und Härtungsmitteln verwendet.
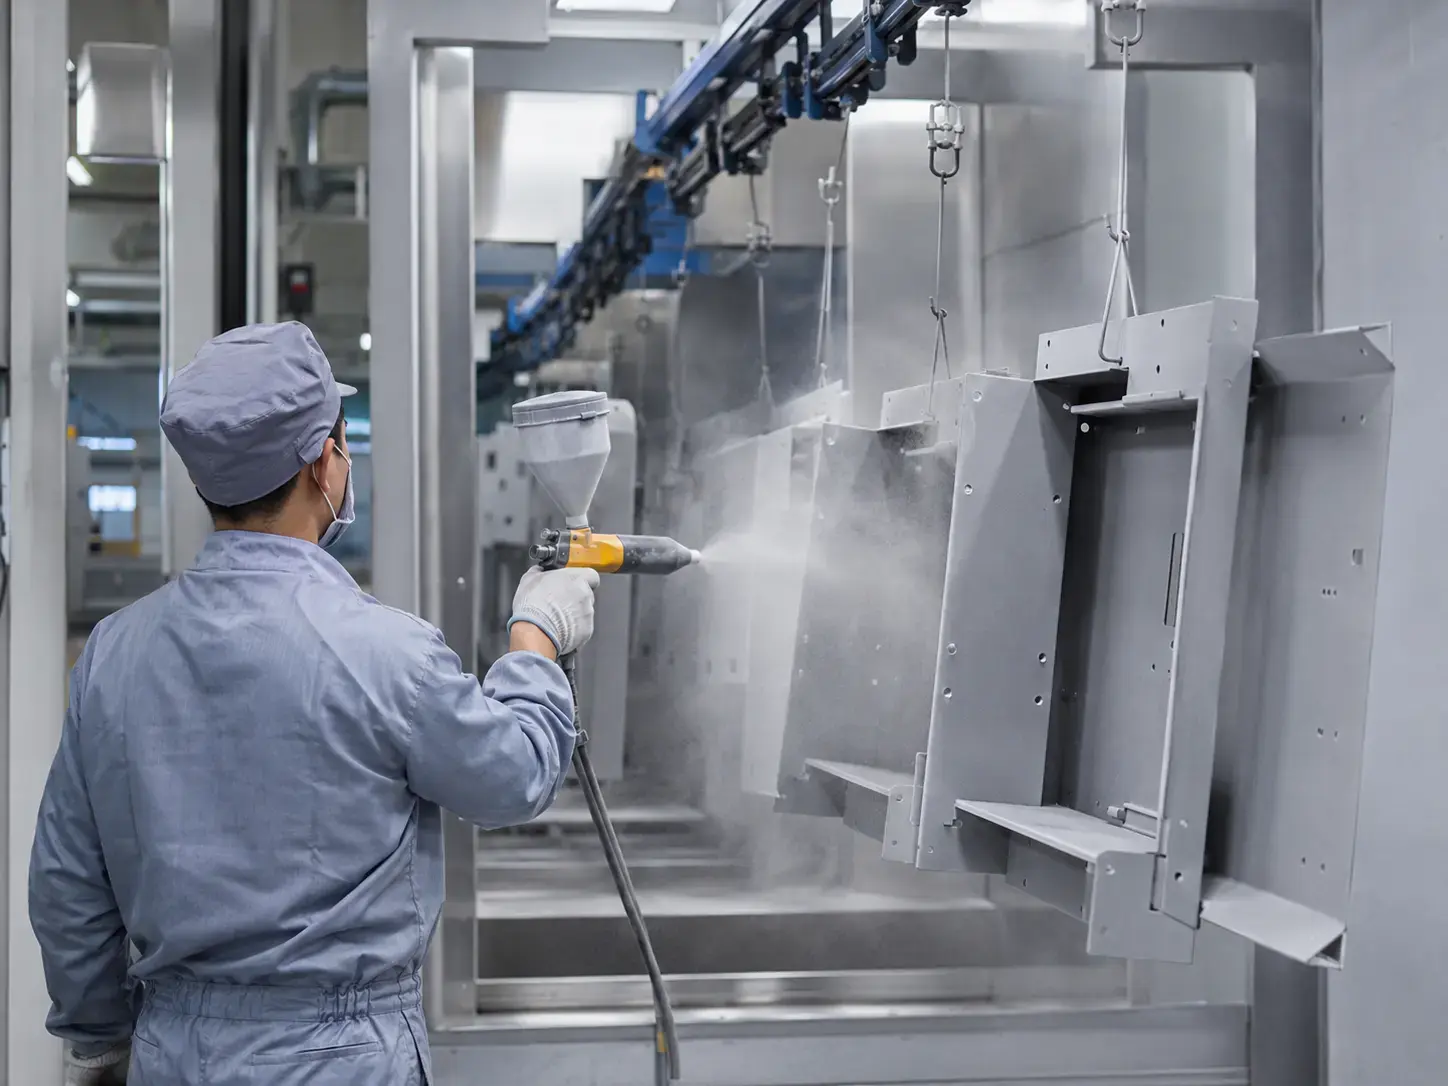
Vor der Beschichtung werden Blechteile gereinigt und vorbehandelt, um die Haftung zu verbessern. Das Pulver wird dann durch elektrostatisches Sprühen, aufgetragen, wobei geladene Pulverpartikel von der geerdeten Metalloberfläche angezogen werden.
Nach dem Sprühen werden die Teile in einem Ofen gehärtet. Während der Härtung schmilzt das Pulver, fließt und vernetzt, um einen durchgehenden Beschichtungsfilm auf der Metalloberfläche zu bilden.
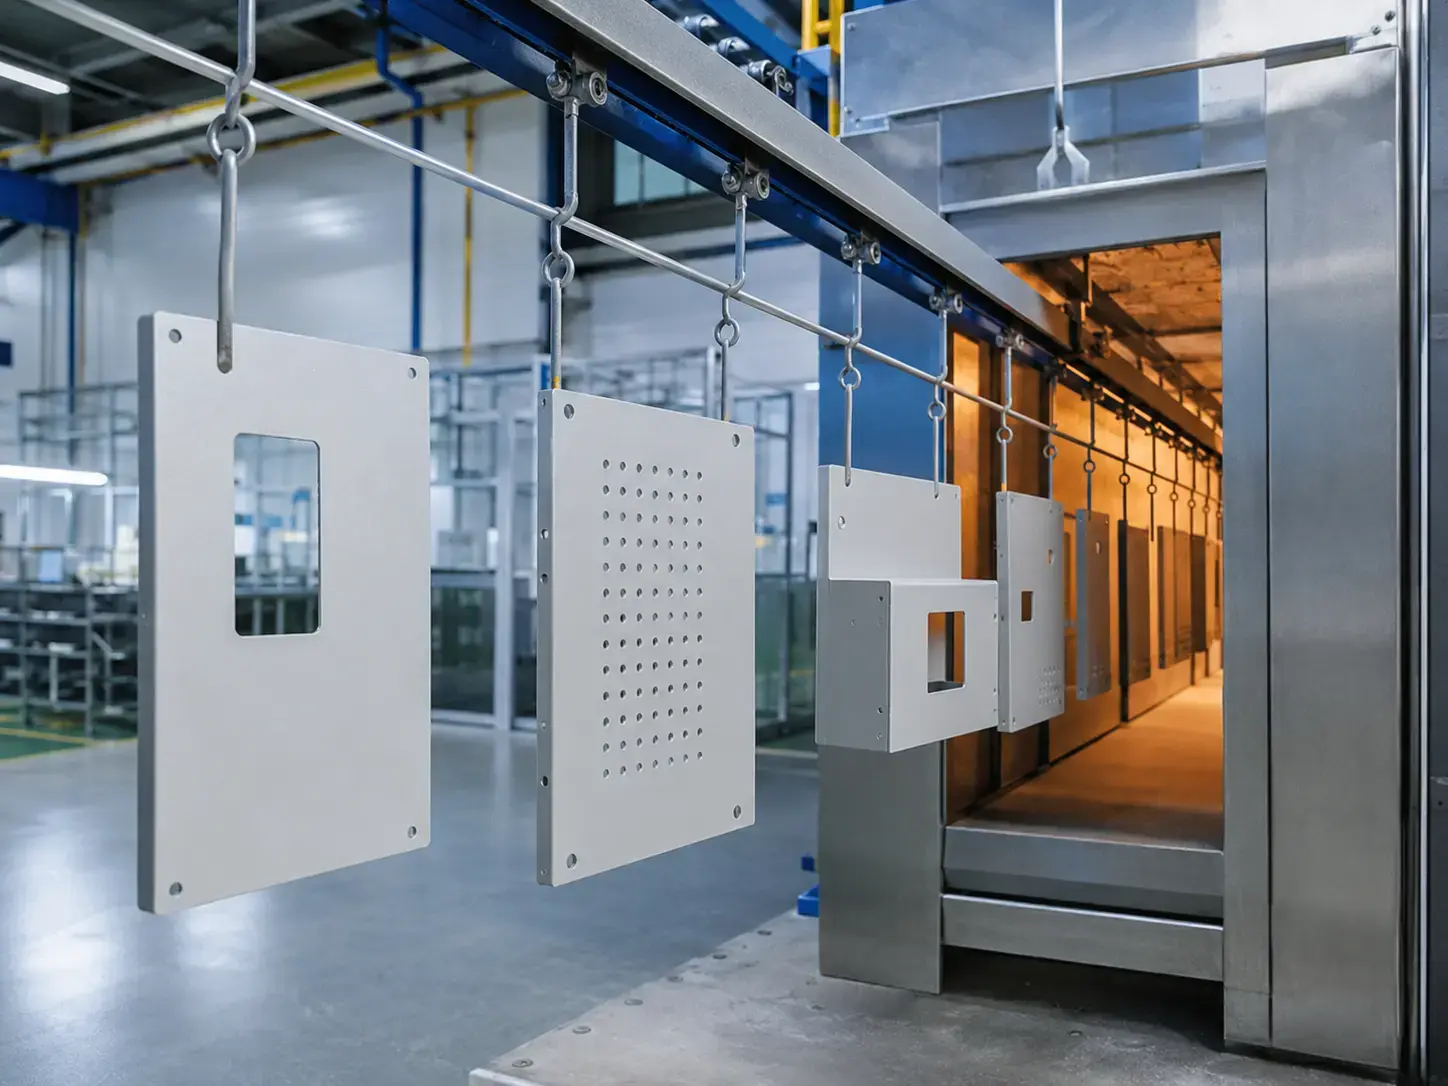
Highlights des Pulverbeschichtungsprozesses
Vorbehandlung
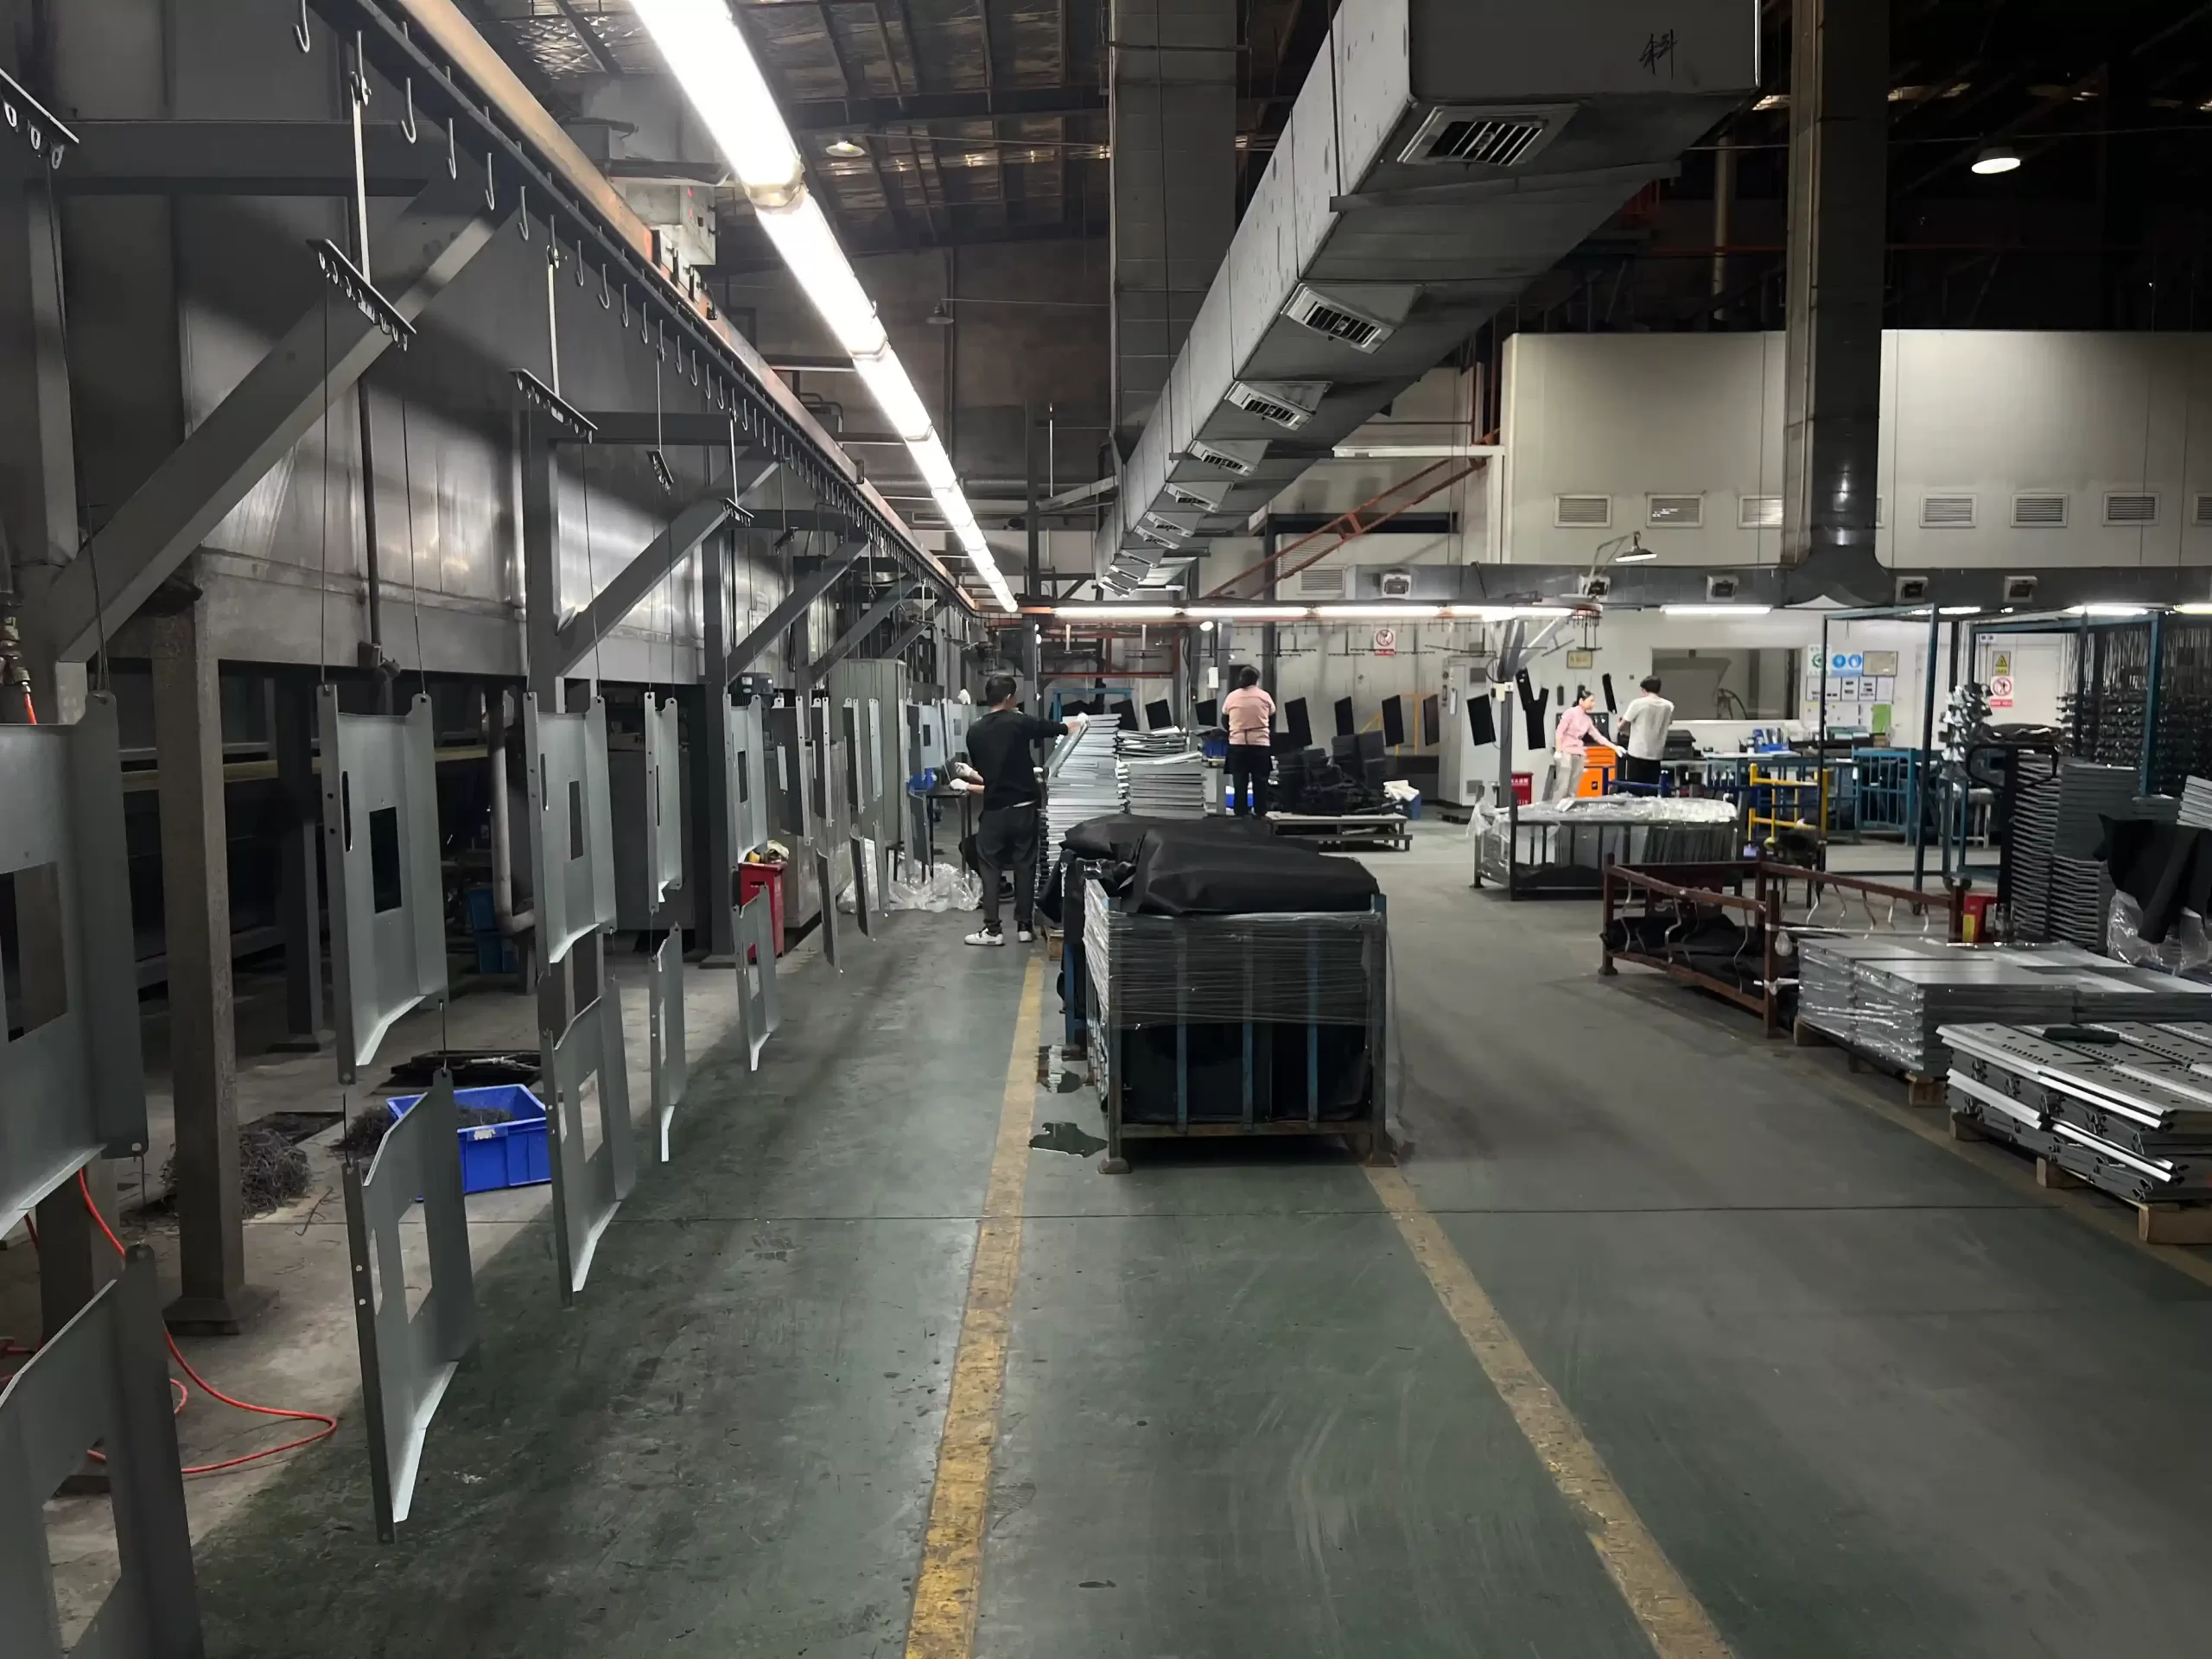
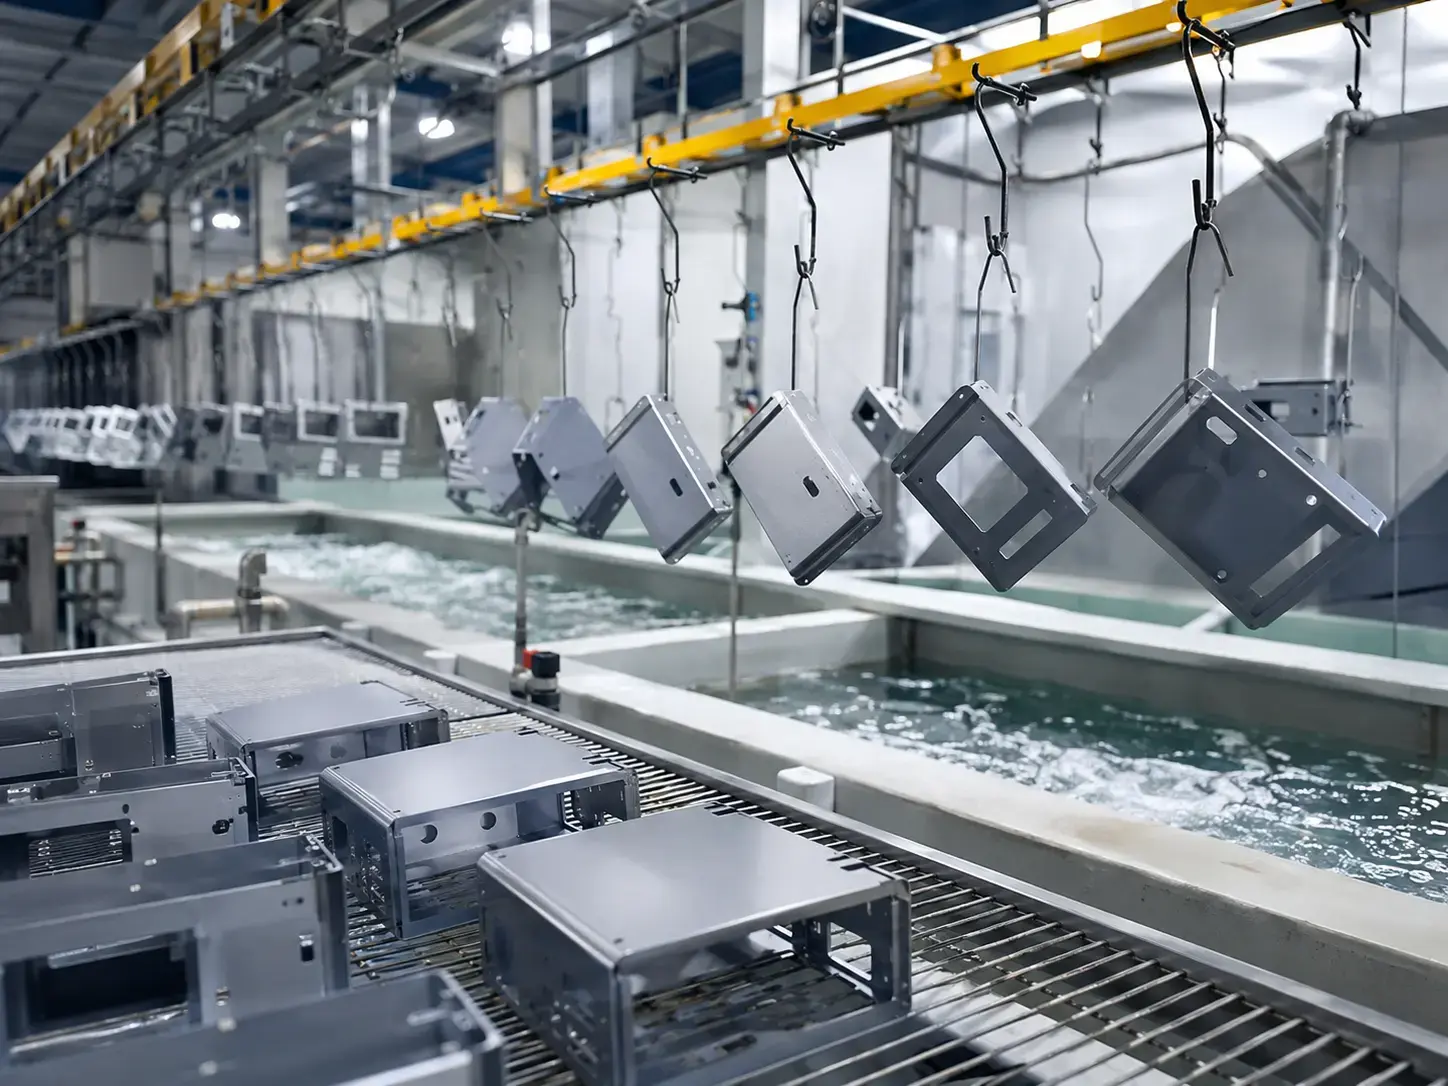
Reinigung, Entfettung und Oberflächenvorbereitung helfen, die.
Elektrostatisches Sprühen
Geladene Pulverpartikel werden gleichmäßig auf das geerdete.
Ofenhärtung
Die beschichteten Teile werden erhitzt, sodass das Pulver schmilzt, fließt und.
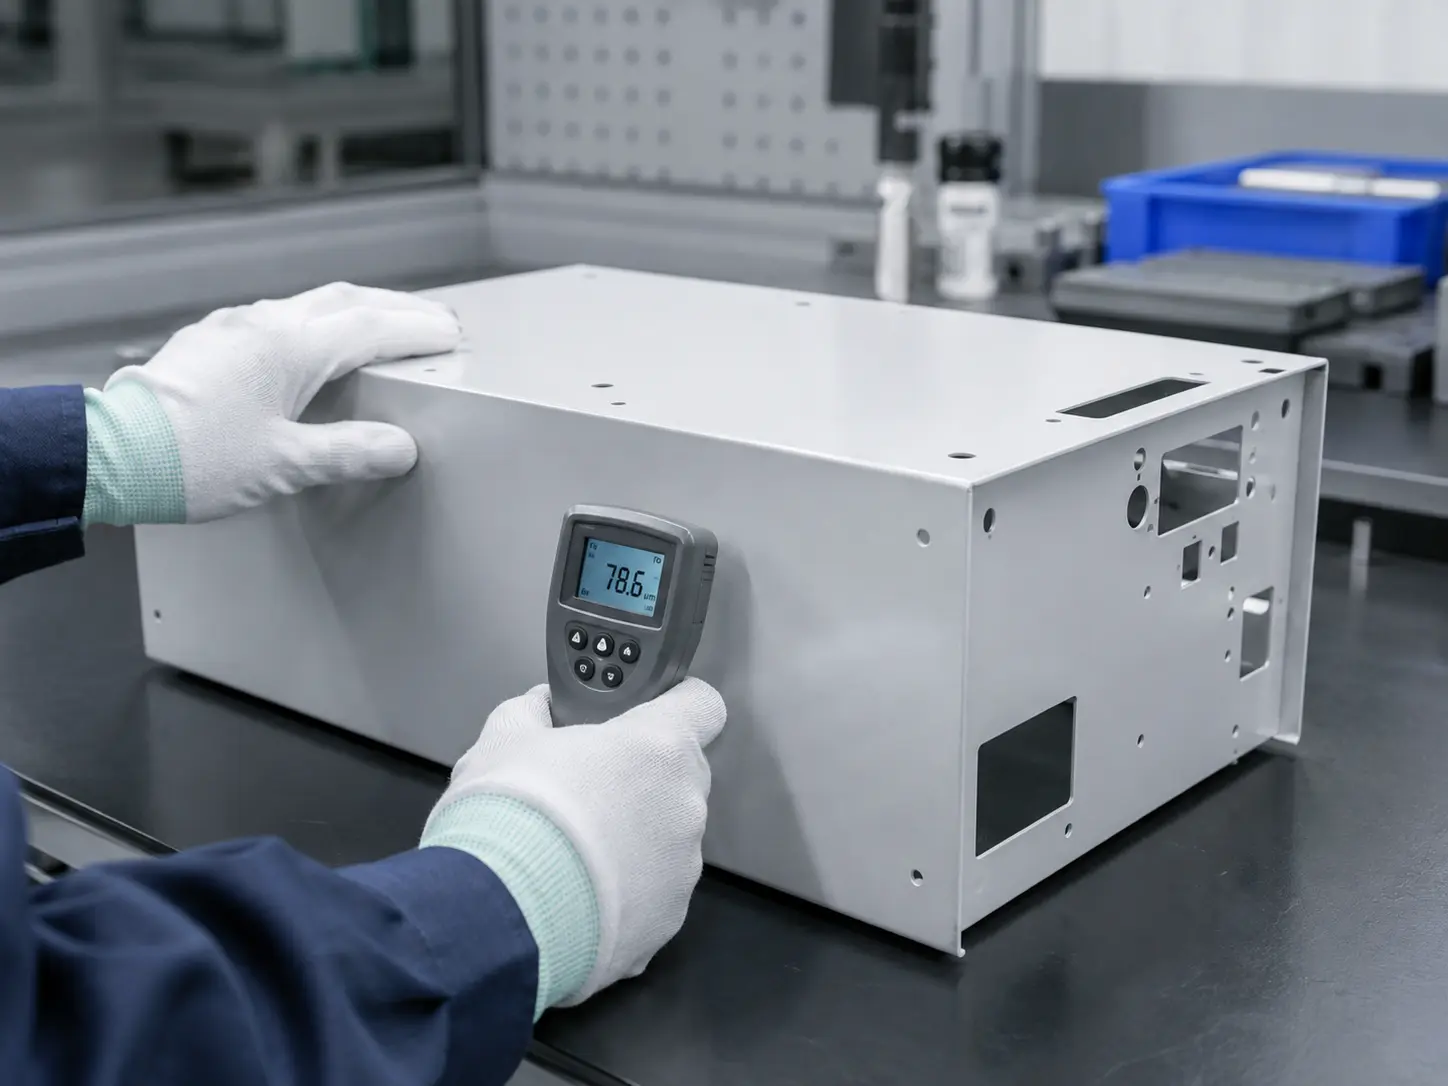
Endkontrolle
Erscheinungsbild, Beschichtungsdicke, Haftung, Abdeckbereiche und.
Überblick über die Pulverbeschichtungskapazität
SR MFG unterstützt die Pulverbeschichtung für individuelle Blechteile, Gehäuse, Paneele, Halterungen, Rahmen und Strukturkomponenten. Unsere Beschichtungskapazität wird anhand von Teilegröße, Gewicht, Oberfläche, Beschichtungsdicke, Farbanforderungen, Abdeckbereichen und Prüfstandards bewertet.
Für jedes Projekt können wir Ihre Zeichnungen und Oberflächenanforderungen auswerten, um den geeigneten Pulvertyp, die Zielbeschichtungsdicke, die Abdeckmethode, den Prüfplan und die Machbarkeit der Serienproduktion zu bestätigen.
Max. Teilegröße
Bis zu
L 6000 × H 2400 × B 700 mm
Max. Teilegewicht
Bis zu
200 kg
pro Stück
Typische Dicke
50–100 μm Empfohlenes Ziel: 60–80 μm
MOQ-Referenz
Typische MOQ:
100 pcs / batch
Small runs reviewed case by case
Powder System Options
Epoxy
Best for indoor corrosion and chemical resistance.
Polyester
General-purpose outdoor weather resistance.
Epoxy /
Polyester Hybrid
Balanced appearance, value, and protection.
Super-Durable /
High-Performance
For stronger weathering resistance and longer service life.
Appearance Options
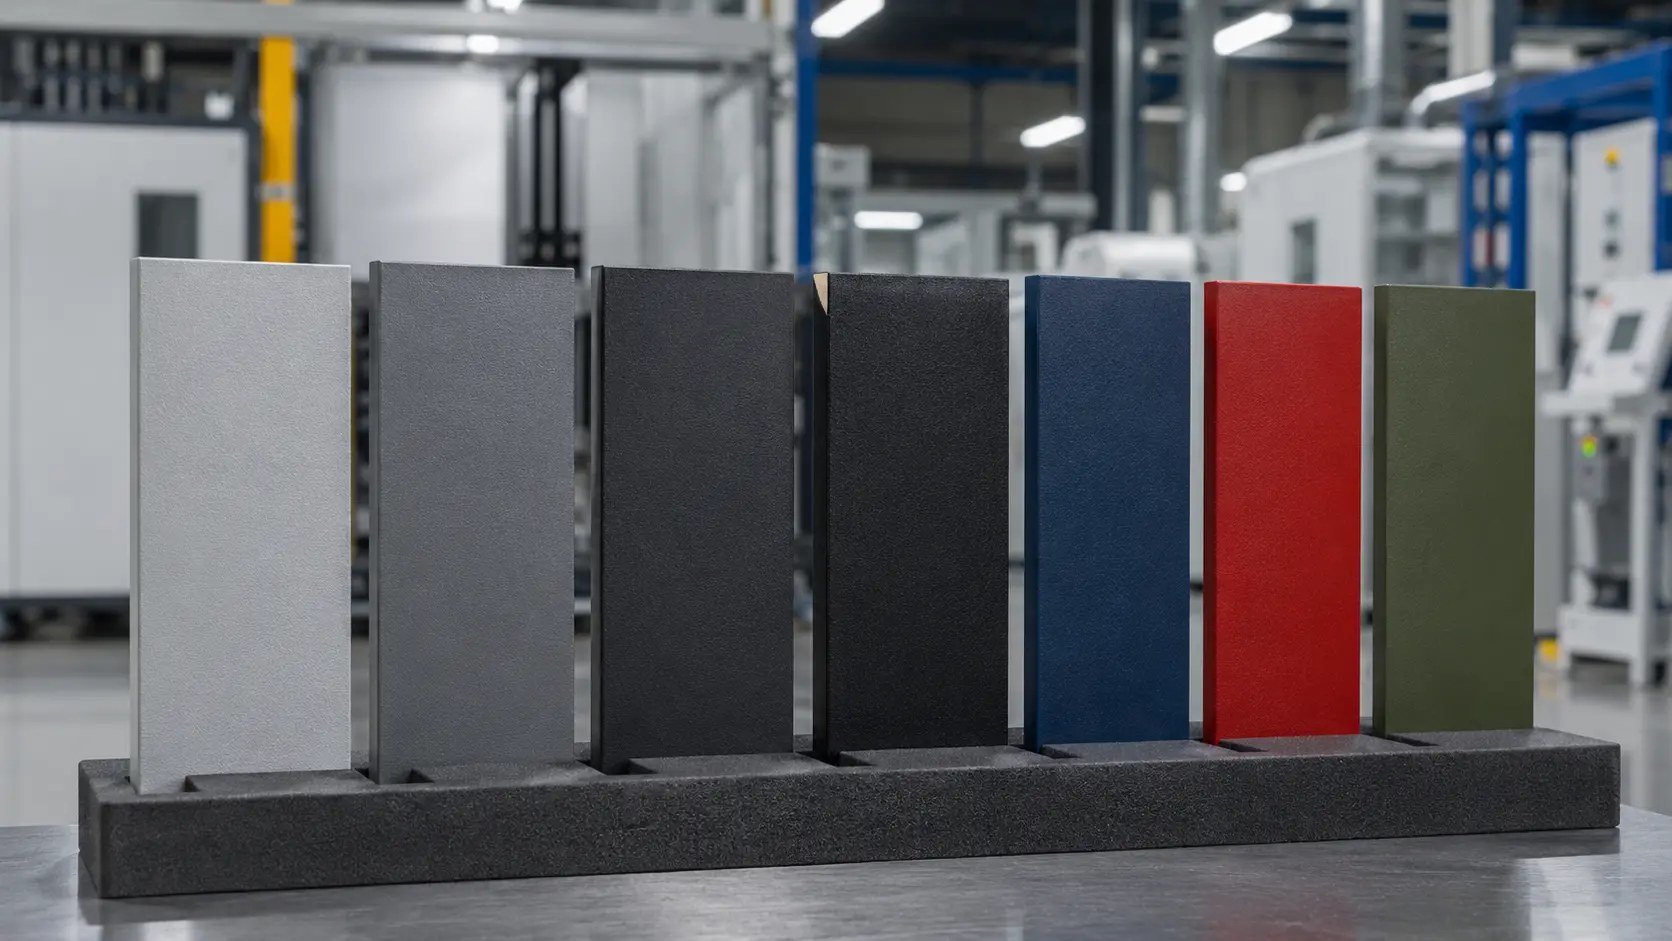
- Matte, gloss, sand texture, metallic, hammer tone
- RAL / Pantone matching available
- Approved sample control for consistent appearance
Masking & Protection
- Threaded holes: Kept clean and free of coating build-up.
- Grounding points: Protected to maintain electrical conductivity.
- Mating surfaces: Masked to ensure fit and function accuracy.
Quality & Validation
- Thickness control: Monitored to target range with records.
- Adhesion testing: Cross-cut and other methods as required.
- Corrosion resistance: Salt spray testing available when required.
Project Review Details for Powder Coating
+
Project Review Details for Powder Coating
| Review Area | What We Check | Warum es wichtig ist |
|---|---|---|
| Part Size & Hanging Method | Part dimensions, hanging direction, hole position, and rack density. | Confirms whether the part can pass through the spray booth and curing oven efficiently. |
| Part Weight & Handling | Single-part weight, lifting method, fixture needs, and deformation risk. | Helps determine safe handling, hanging stability, and whether split coating is required. |
| Coating Thickness Target | Target thickness, tolerance range, coating build-up, and critical fit areas. | Prevents coating thickness from affecting assembly, threaded holes, grounding points, or mating surfaces. |
| Color & Appearance Approval | RAL / Pantone code, gloss level, texture, surface effect, and approved physical sample. | Keeps color, gloss, and texture consistent before batch production release. |
| Powder Type Selection | Indoor or outdoor use, UV exposure, chemical resistance, corrosion target, and service life requirement. | Helps select epoxy, polyester, hybrid, or high-performance powder based on real application conditions. |
| Masking Requirements | Threaded holes, grounding points, mating surfaces, contact areas, and no-coat zones. | Protects assembly function, electrical conductivity, and dimensional fit after coating. |
| Inspektionsaufzeichnungen | Coating thickness, adhesion, appearance, masking results, and final inspection records. | Supports customer receiving inspection, quality tracking, and project traceability. |
| Korrosionsvalidierung | Salt spray requirement, test standard, exposure time, and acceptance criteria. | Confirms whether the coating system meets the intended service environment and performance target. |
How to Choose the Right Powder Coating System
Choosing the right powder coating system depends on where the part will be used, how long it needs to perform, and what appearance or corrosion resistance requirements must be met. SR MFG reviews the service environment, material, coating thickness, color requirements, masking areas, and validation standards before recommending a suitable powder coating solution.
Indoor Use
Epoxy or epoxy-polyester hybrid. Best for indoor cabinets, brackets, equipment frames, and structural parts with no long-term UV exposure.
General Outdoor Use
Polyester powder. Suitable for outdoor covers, brackets, fences, hardware, cabinet shells, and enclosure panels.
Coastal / Heavy Corrosion
Anti-corrosion primer + weatherable topcoat. Recommended for coastal cabinets, industrial frames, and parts exposed to salt spray or high humidity.
Architectural Exterior
Super-durable polyester. Used for façade components, exterior panels, and decorative parts requiring better weathering resistance.
Premium Exterior / Ultra-Long-Life
High-performance coating system. Suitable for demanding exterior applications with strict long-term appearance and weathering requirements.
Detailed Coating System Selection Guide
| Service Environment | Recommended Powder System | Recommended Build | Recommended DFT | Example Parts | Suggested Validation |
|---|---|---|---|---|---|
|
no UV exposure |
Epoxy or epoxy-polyester hybrid | Single coat | 60–80 μm (adjustable within 50–100 μm) |
Indoor cabinets, enclosures, brackets, equipment frames | DFT, adhesion, appearance; chemical or abrasion resistance if required |
|
UV exposure |
Polyester powder | Single coat; primer/base coat optional for higher corrosion target | 70–100 μm | Outdoor covers, fences, hardware, outdoor brackets | DFT, adhesion, salt spray or cyclic corrosion testing if required |
|
heavy corrosion |
Polyester or super-durable polyester topcoat with anti-corrosion primer | Two-coat system preferred | Total 120–200 μm | Coastal cabinets, industrial frames, parts exposed to salt spray or high humidity | Cyclic corrosion testing recommended; define acceptance criteria |
|
exterior |
Super-durable polyester for architectural aluminum applications, aligned with AAMA 2604 when specified. | Per specification, often single coat | Typically ≥30 μm depending on system | Façade accessories, decorative panels | Test to AAMA 2604 when required |
|
ultra-long-life exterior |
High-performance coating system for architectural aluminum applications, aligned with AAMA 2605 when specified. | Per specification, may be multi-coat | Per specification | Landmark projects and demanding exterior parts | Test to AAMA 2605 when required |
Design Considerations for Powder Coated Sheet Metal Parts
Powder coating quality is not determined only by the coating process. Part geometry, edge condition, drainage, masking areas, material porosity, and heat sensitivity can all affect coating coverage, adhesion, corrosion resistance, and final appearance.
Deep Recesses & Inside Corners
Risk: Faraday effect can leave inner corners with light coverage or bare spots.
Design Recommendation: Add inside radii, avoid narrow deep channels, and allow spray access.
Sharp Edges & Burrs
Risk: Sharp edges often receive thinner film build and become corrosion weak points.
Design Recommendation: Deburr, break corners, and add small radii where possible.
Enclosed Cavities & Tubes
Risk: Trapped pretreatment liquid or moisture can cause blistering, corrosion, or drying defects.
Design Recommendation: Add drain and vent holes, especially near the lowest point or closed end.
Outgassing & Pinholes
Risk: Castings, galvanized parts, or weld porosity may release gas during curing and create pinholes.
Design Recommendation: Use pre-bake / outgas bake; add primer or sealer when needed.
Large or Thin Panels
Risk: Heat and hanging conditions can increase warping, oil-canning, or uneven film build.
Design Recommendation: Review hanging direction, support points, stiffness, and visible surfaces.
Critical Functional Surfaces
Risk: Coating build-up can affect threads, grounding points, mating surfaces, and fit.
Design Recommendation: Clearly define no-coat, masking, and thickness-limited areas on the drawing.
Ready to Review Your Powder Coating Requirements?
Not sure which powder coating system is suitable for your project? Contact us with your drawings, material, color, coating thickness, service environment, and masking requirements. Our engineering team will review your specifications and recommend a suitable coating solution.
Industries & Powder Coating Applications
SR MFG provides professional powder coating services for OEM metal parts used in industrial equipment, cabinets, brackets, frames, enclosures, and structural assemblies. From single prototypes to high-volume production runs, we deliver durable, uniform finishes with consistent color and texture across every order.
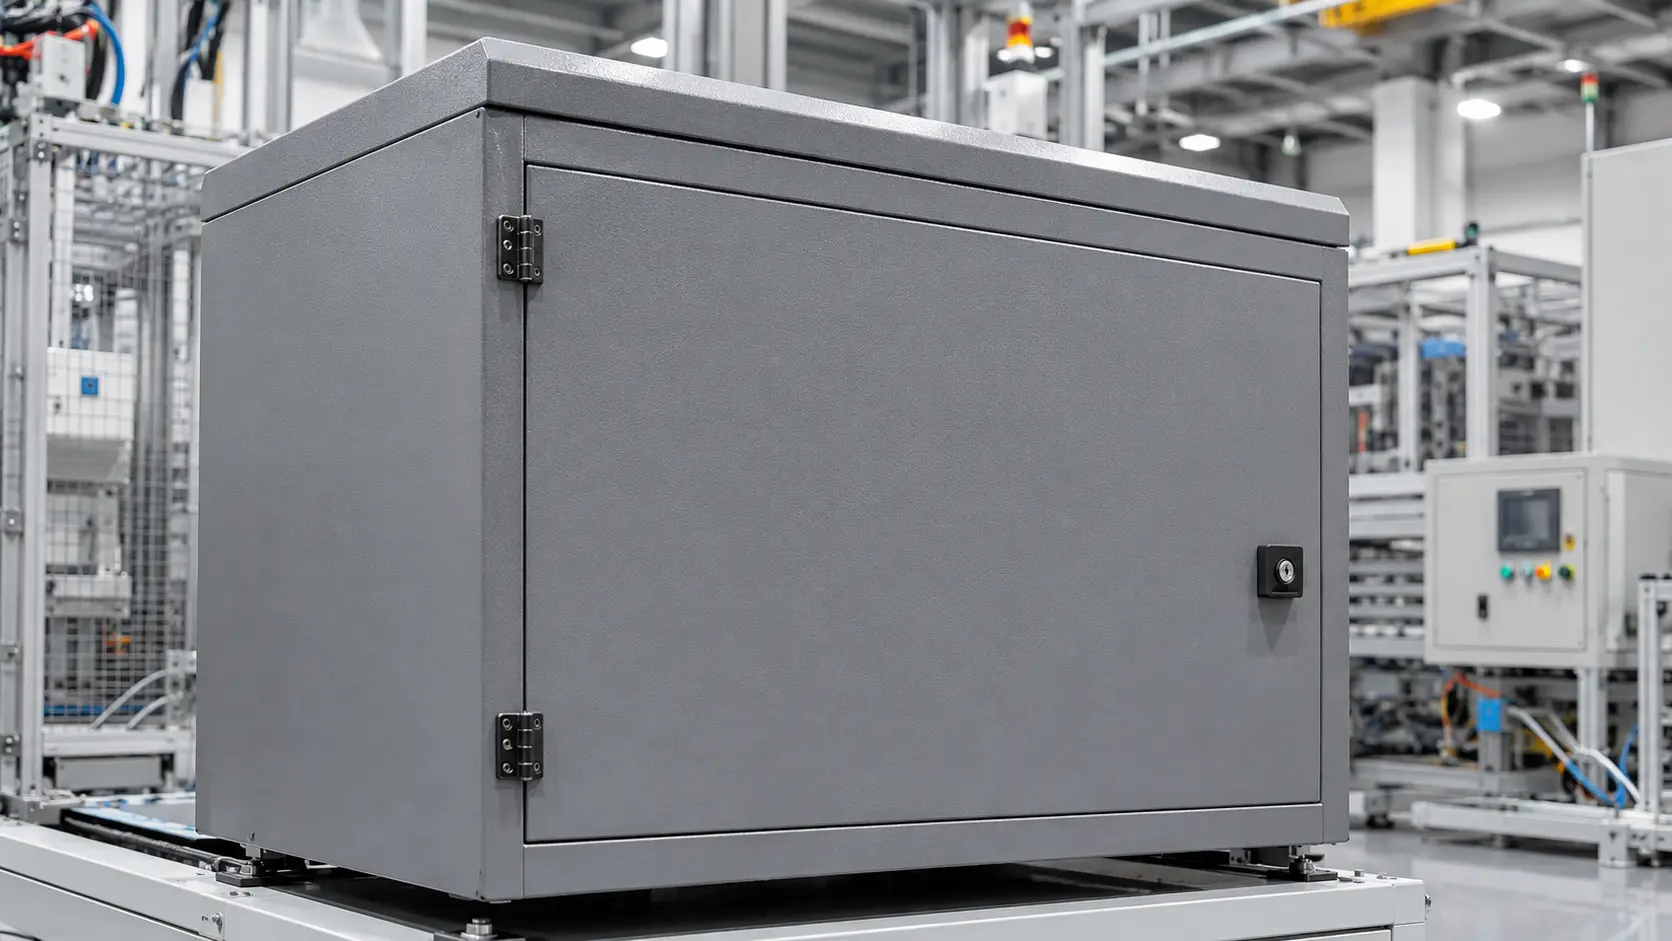
Data Centers & IT Equipment
Powder coated components for data centers, network infrastructure, and IT hardware, delivering corrosion-resistant, professional-grade finishes that withstand continuous indoor operation.
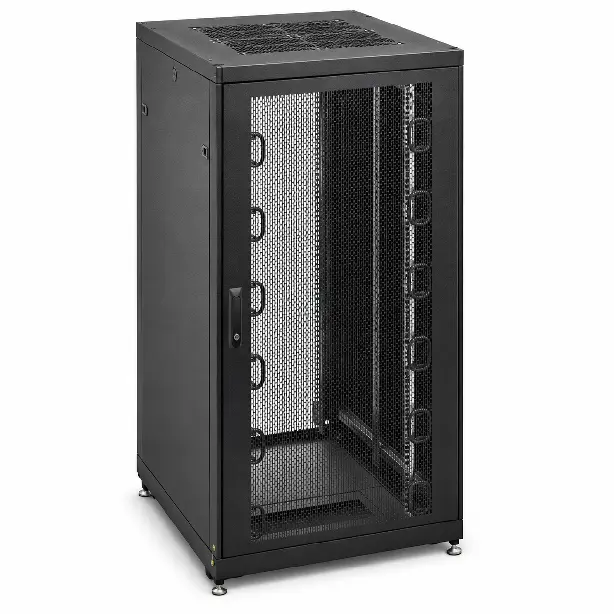
- Server rack frames & rails
- Cable management trays
- Cabinet panels & doors
- Mounting brackets & plates
Unterhaltungselektronik
Powder coating for consumer electronics housings, internal brackets, display structures, and precision metal parts, offering smooth, consistent color with excellent scratch and fingerprint resistance.
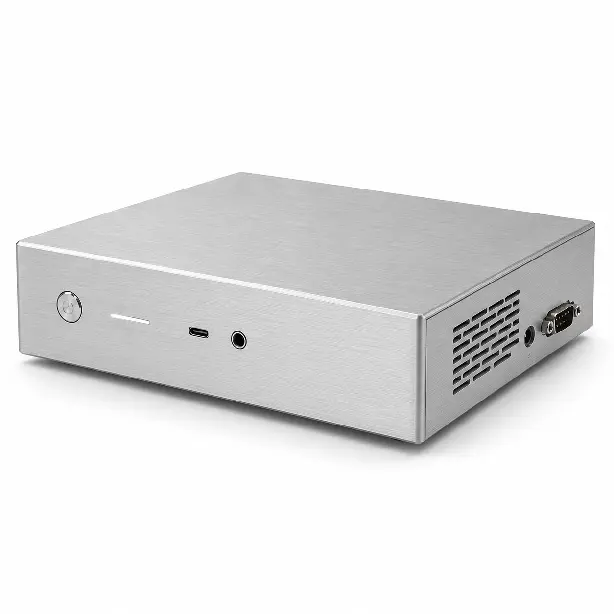
- Device housings & covers
- Internal support brackets
- Display mounting structures
- Speaker & audio metal parts
- Small precision formed parts
Elektrische Geräte
Powder coated components for electrical enclosures, control cabinets, power distribution units, and industrial electrical systems, providing durable surface protection with strong corrosion and chemical resistance.
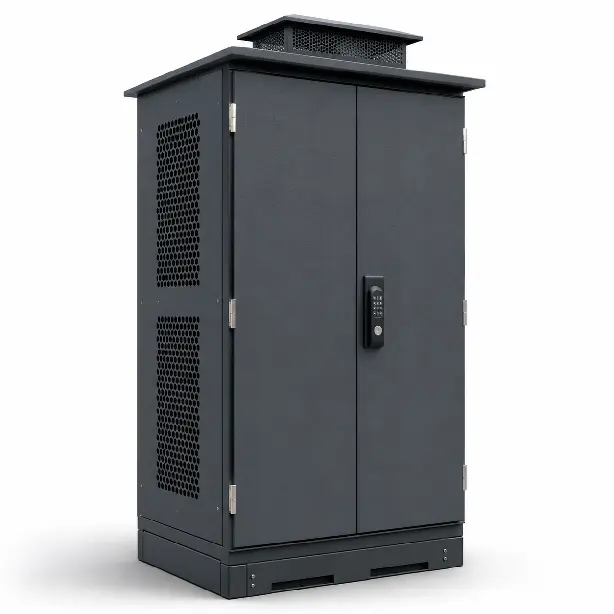
- Electrical cabinet enclosures
- Control box panels
- Terminal mounting plates
- DIN rail brackets
- Ventilation and access panels
Industrieausrüstung
Durable powder coated finishes for machinery, automation systems, production equipment, and structural machine assemblies, built to resist chipping, abrasion, and shop-floor wear.
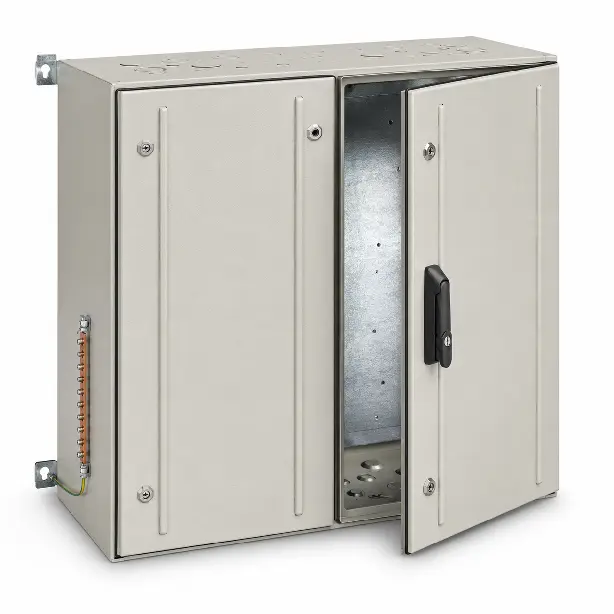
- Machine covers & guards
- Equipment frames
- Conveyor brackets
- Sensor mounting plates
- Protective panels & shields
New Energy Systems
Powder coating solutions for EV charging equipment, battery systems, energy storage cabinets, and power conversion units, delivering long-lasting UV-stable finishes rated for demanding indoor and outdoor environments.
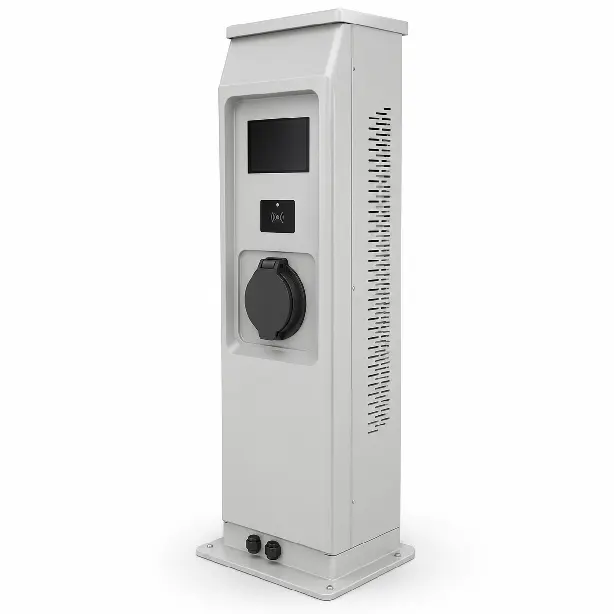
- Battery enclosure parts
- Charging station cabinets
- Energy storage cabinet panels
- Busbar support brackets
- Power module housings
Outdoor Equipment
Weather-resistant powder coated finishes for outdoor enclosures, equipment covers, BBQ grills, lighting systems, and structural fixtures, engineered for UV stability, moisture protection, and years of fade-resistant color retention.
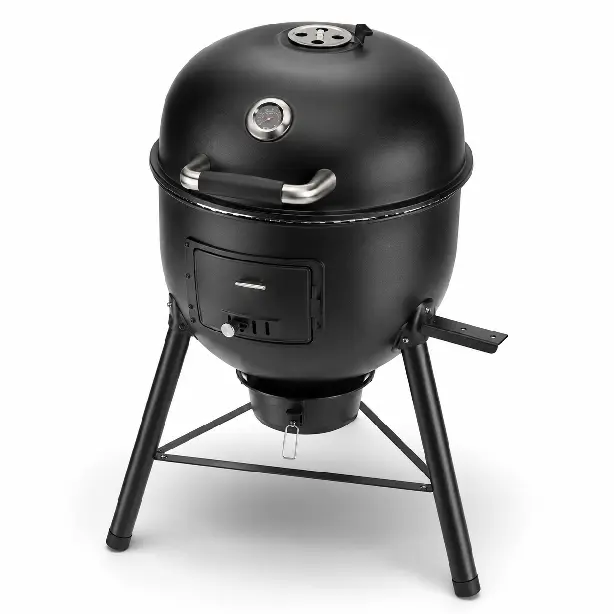
- Outdoor equipment housings
- BBQ grill sheet metal bodies
- Protective covers & panels
- Mounting brackets
- Weather-resistant structural parts
Built for Your Application
Whether you need a single sample or full production volumes, SR MFG ensures consistent coating thickness, uniform color matching, and reliable delivery for every powder coating project. We offer a wide selection of RAL colors, gloss levels, and texture finishes to match your specifications.
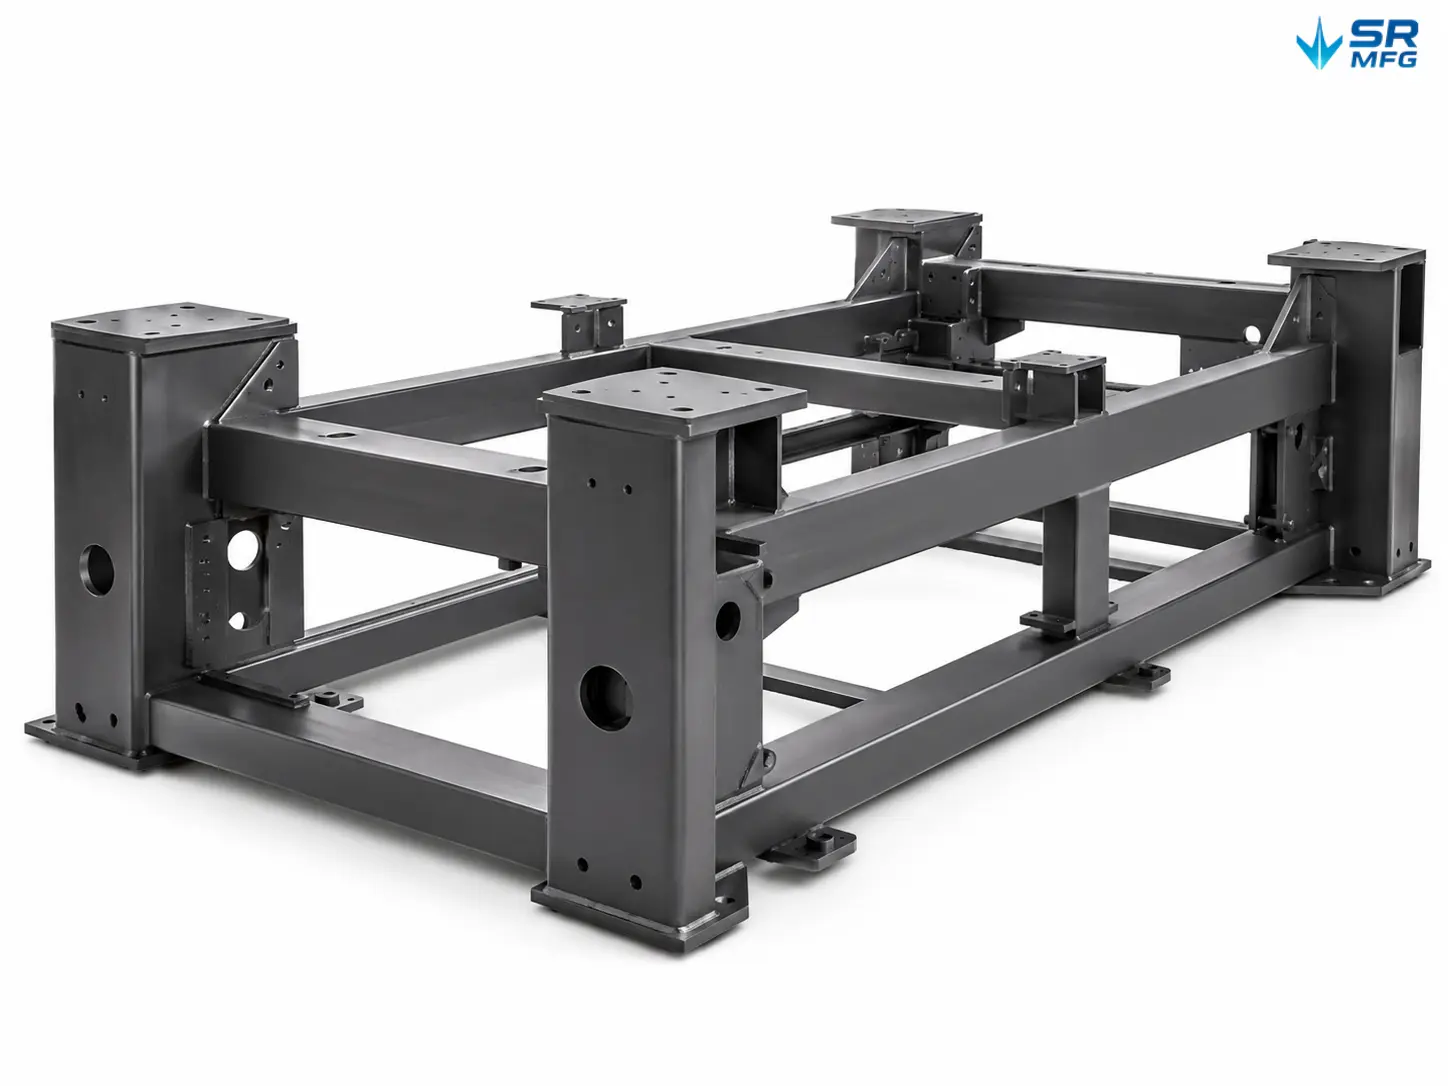
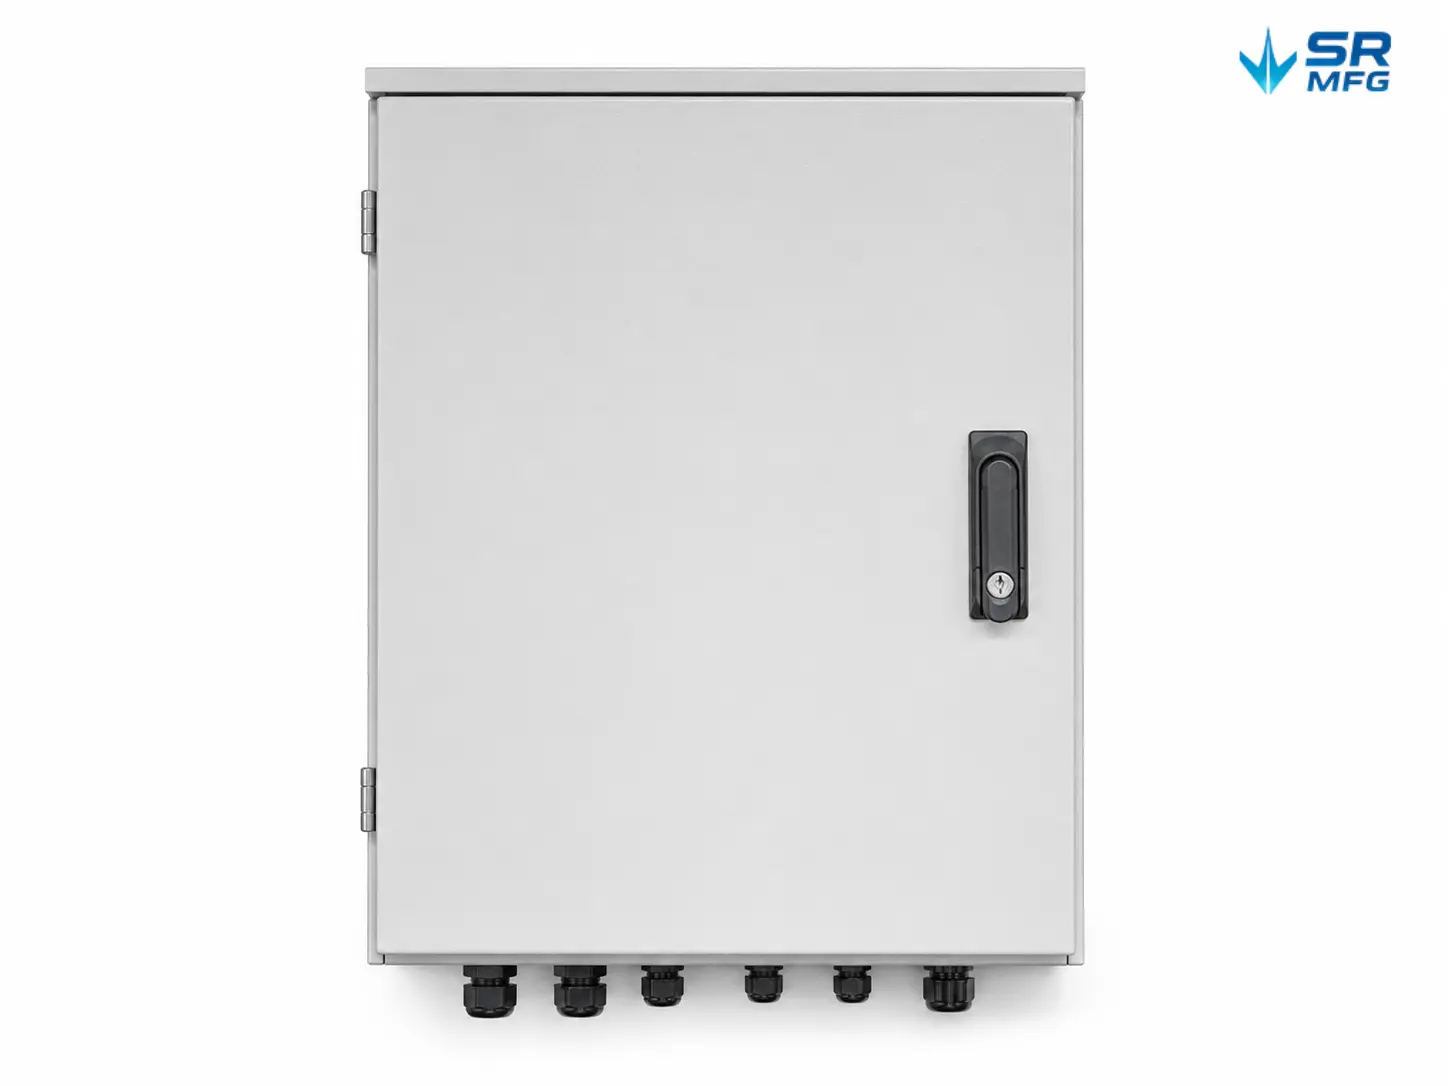
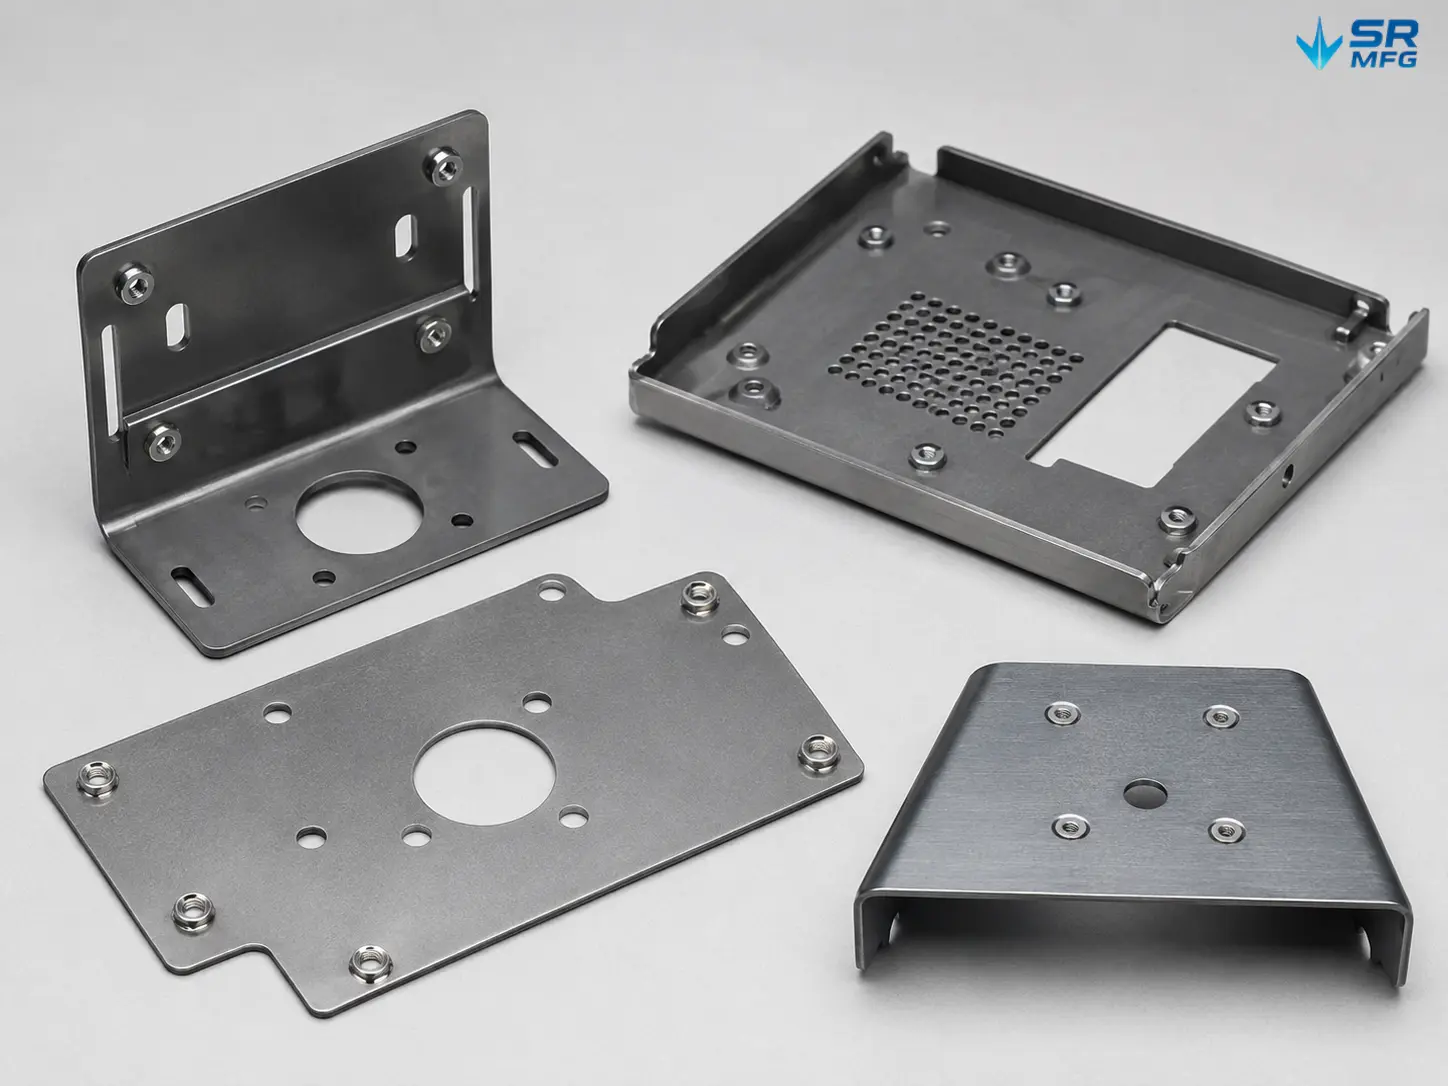
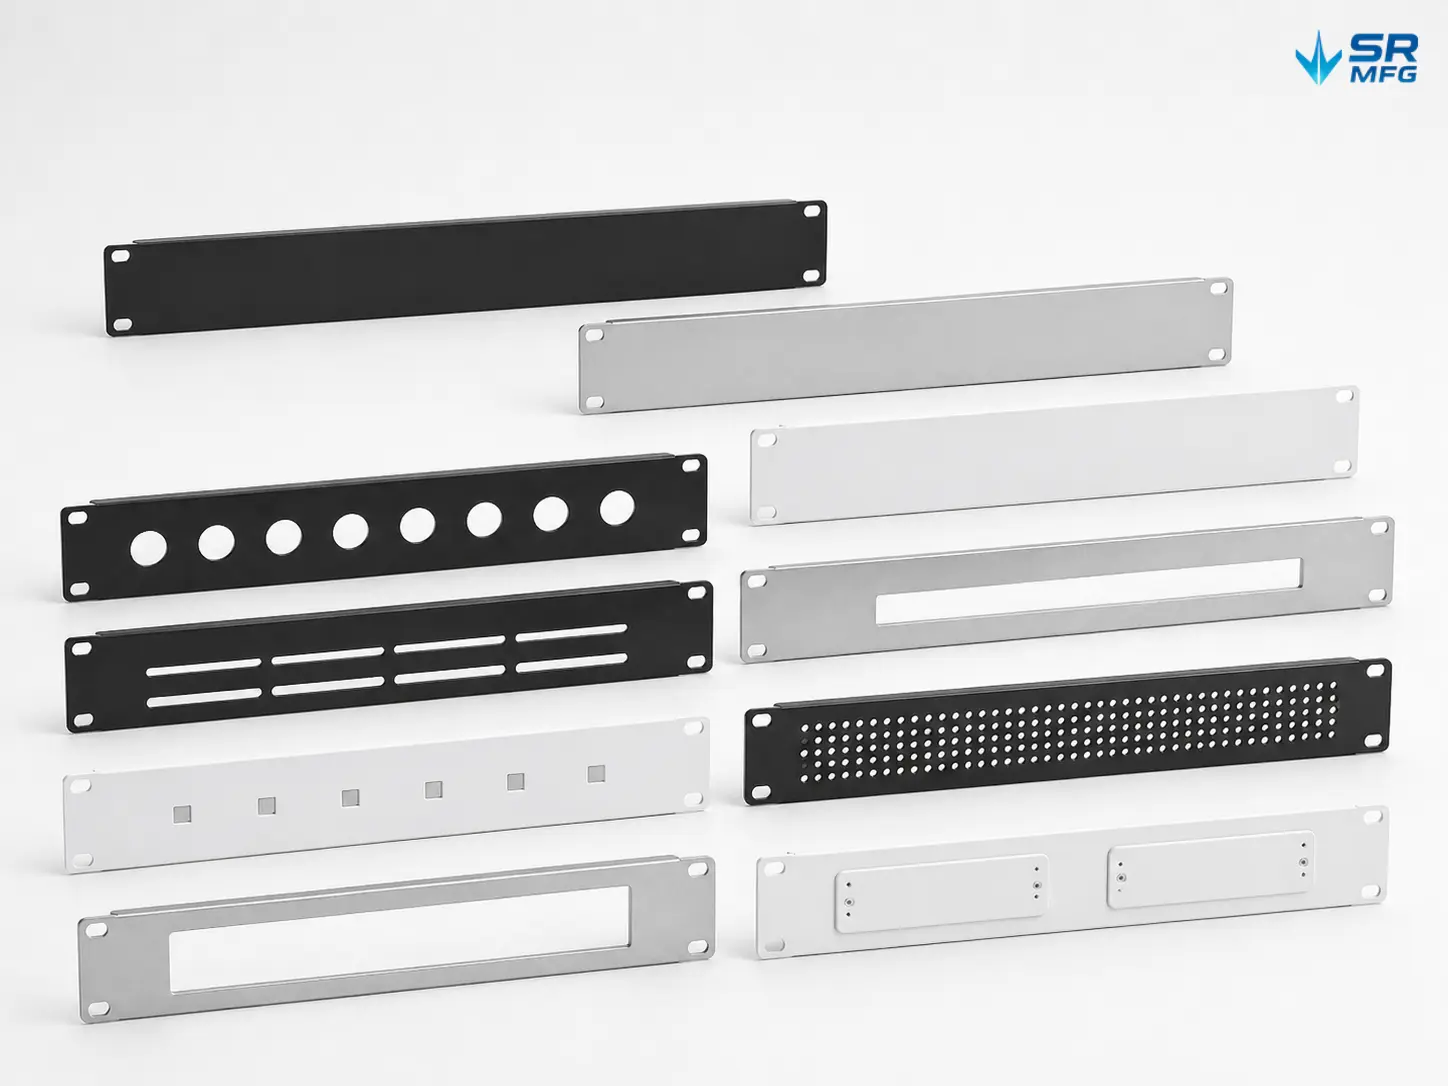
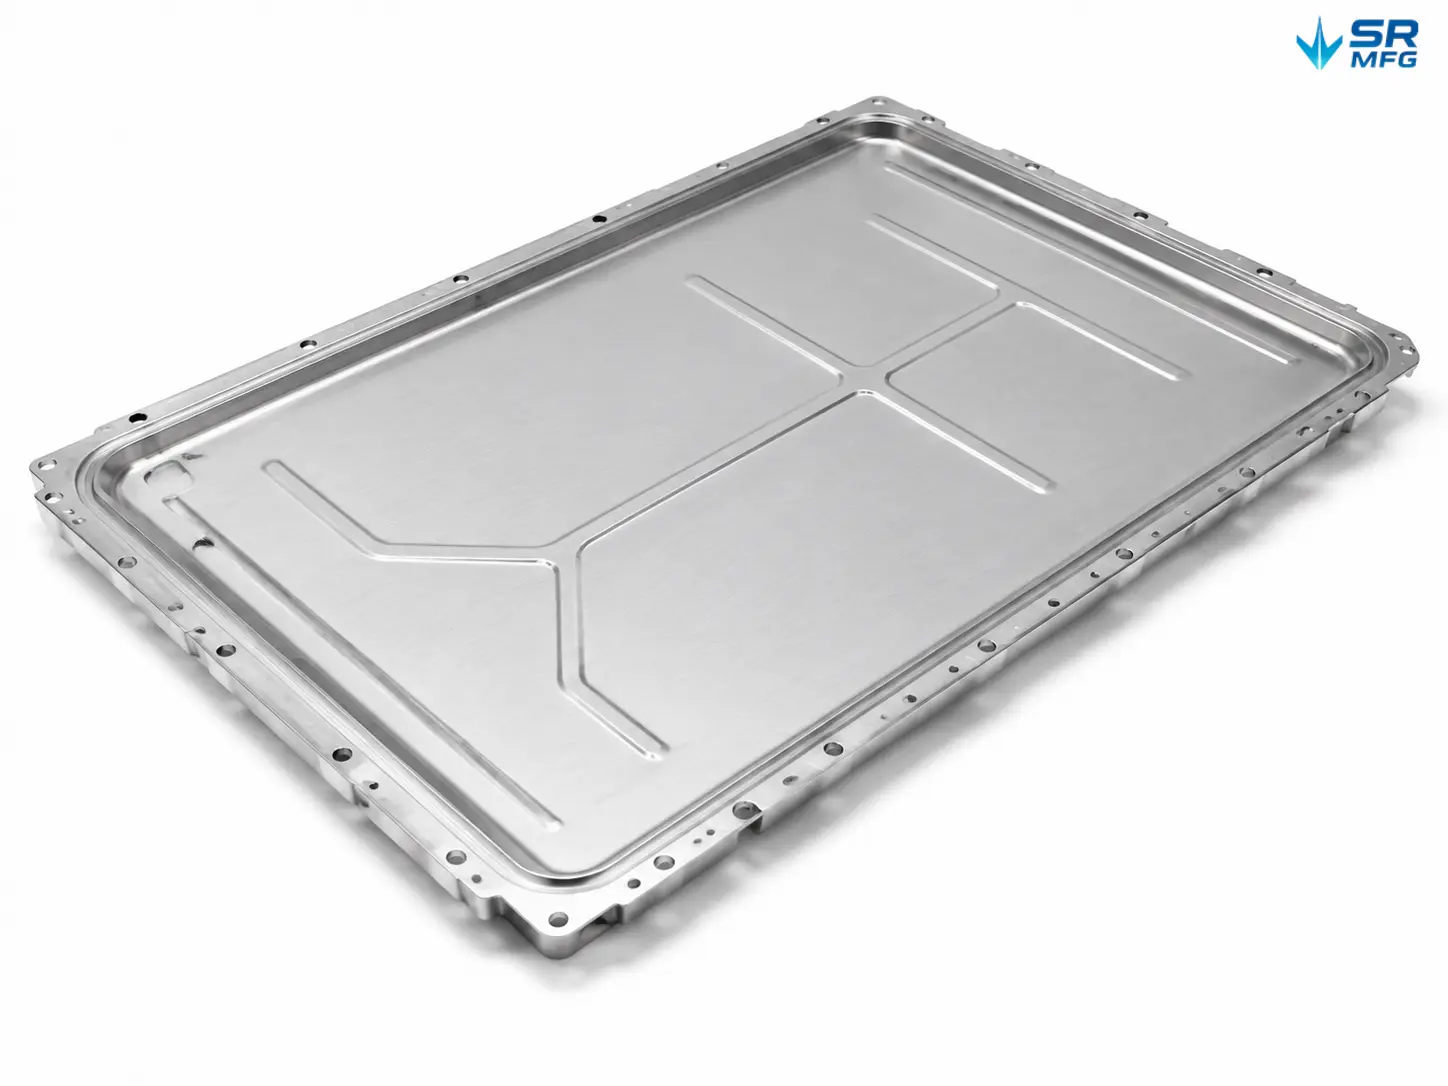
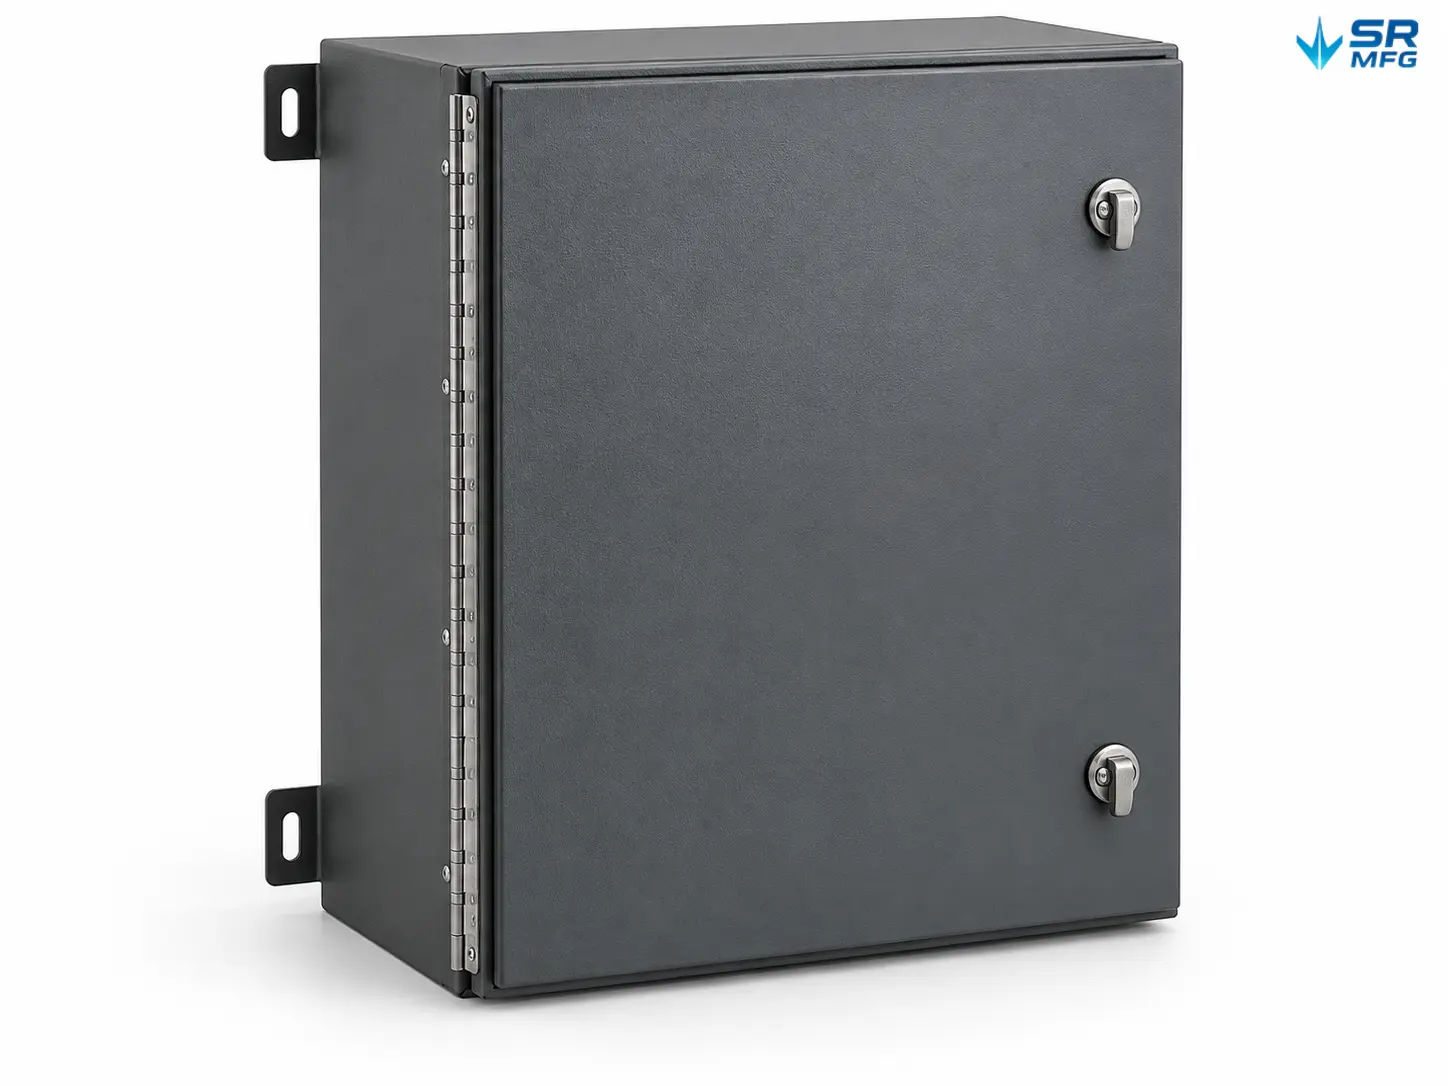
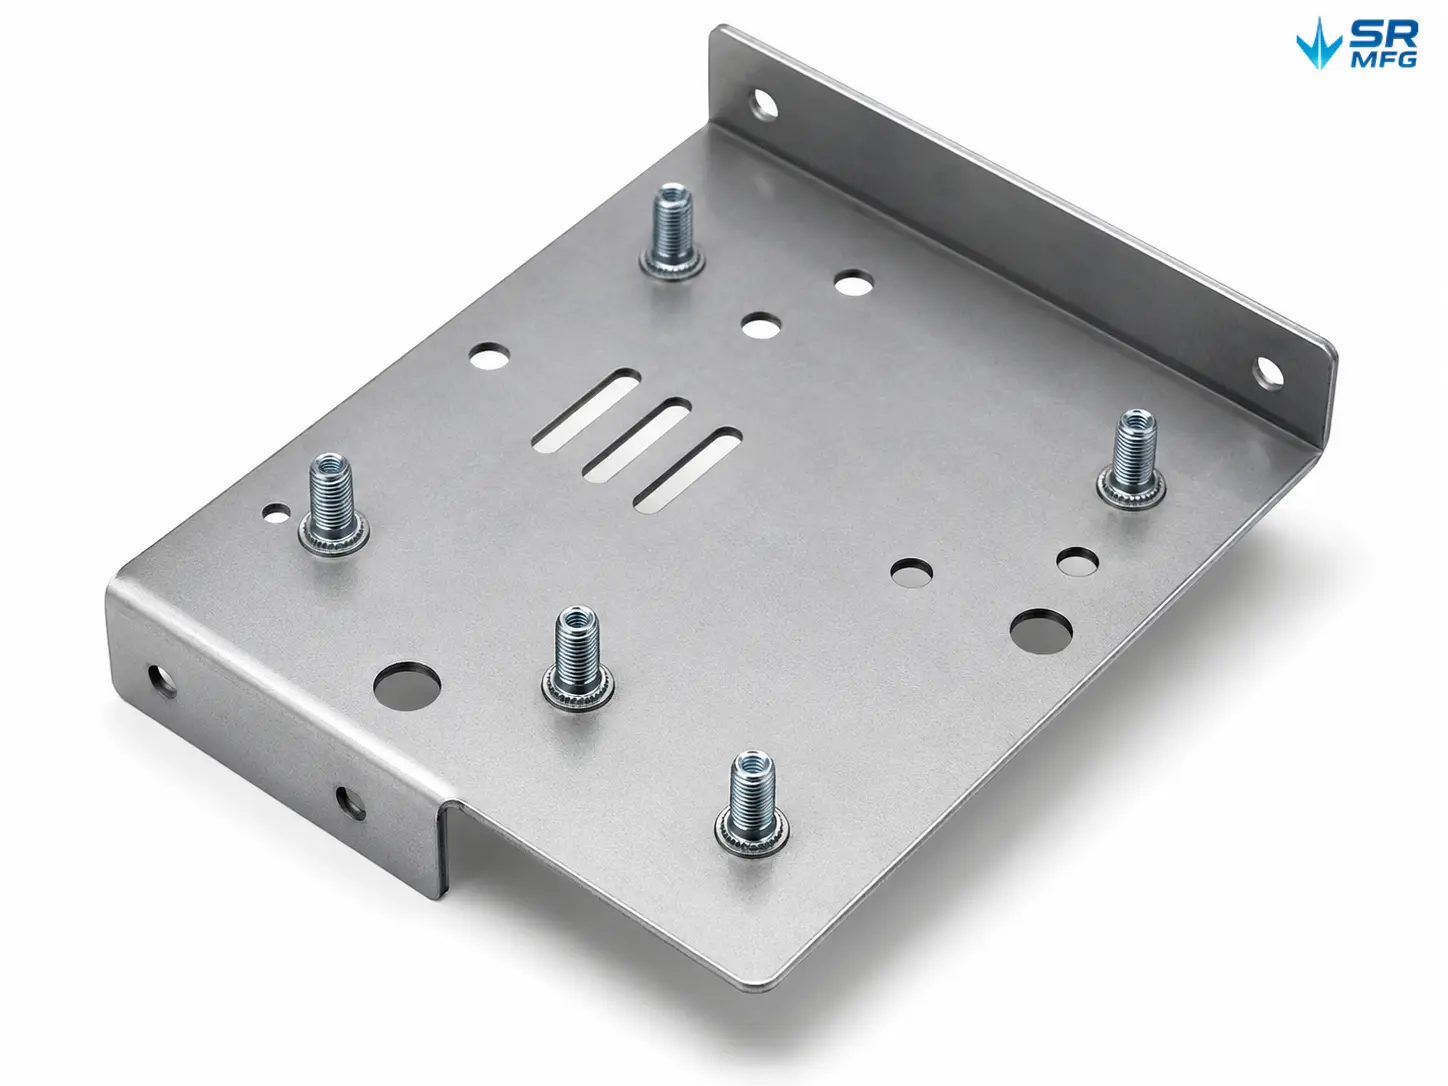
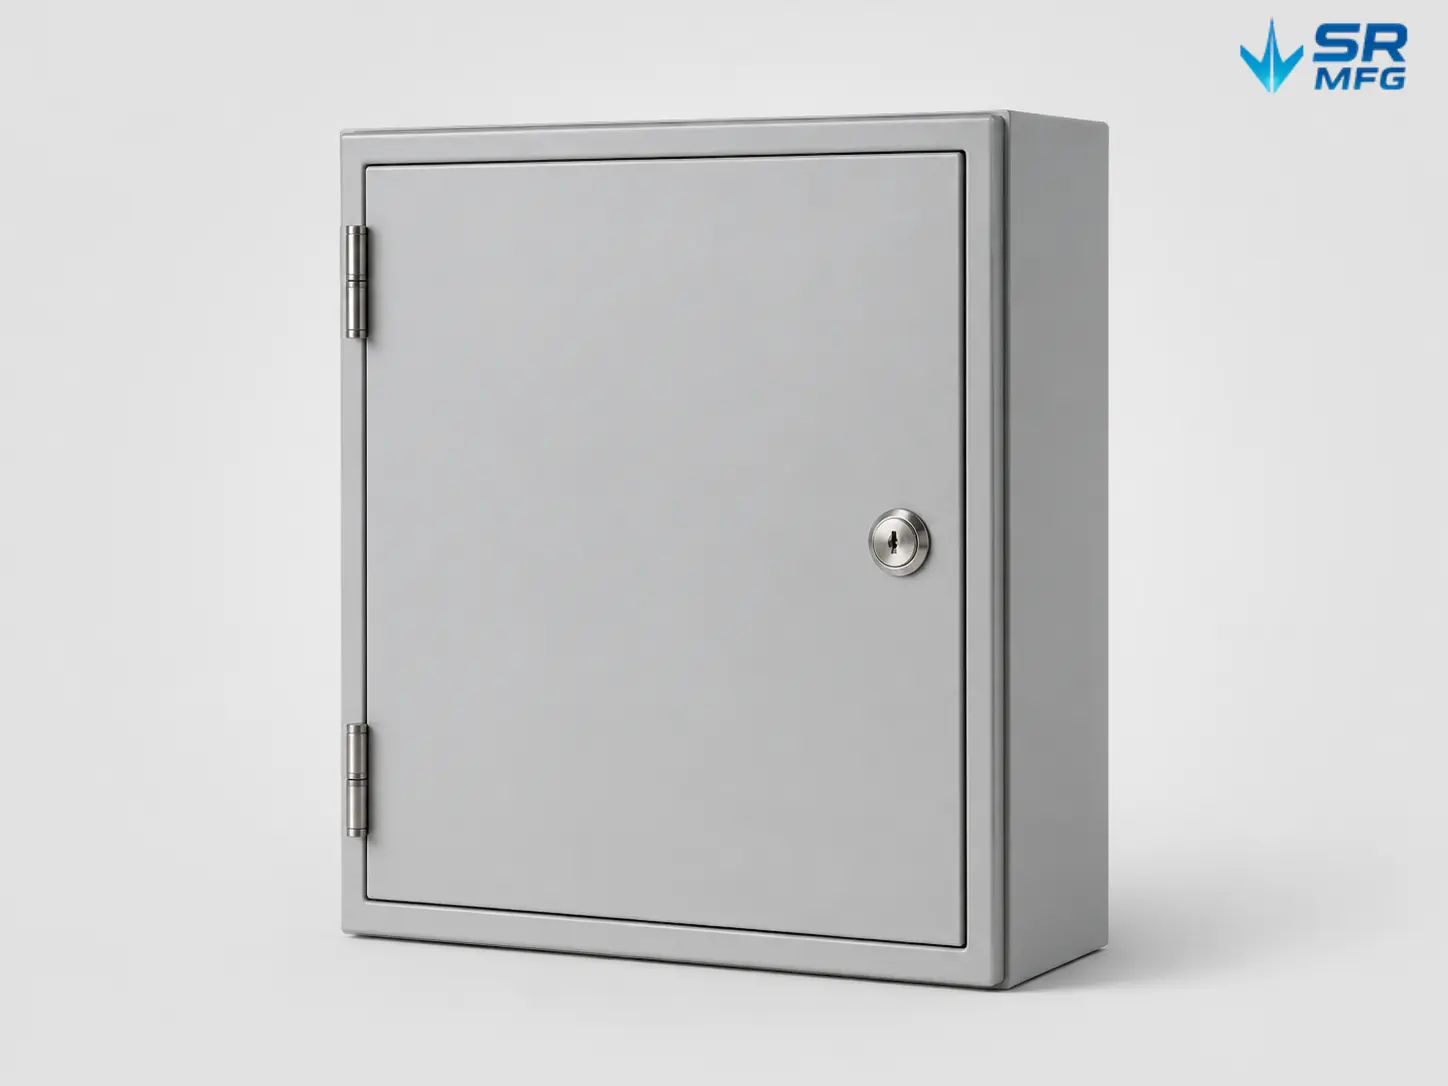
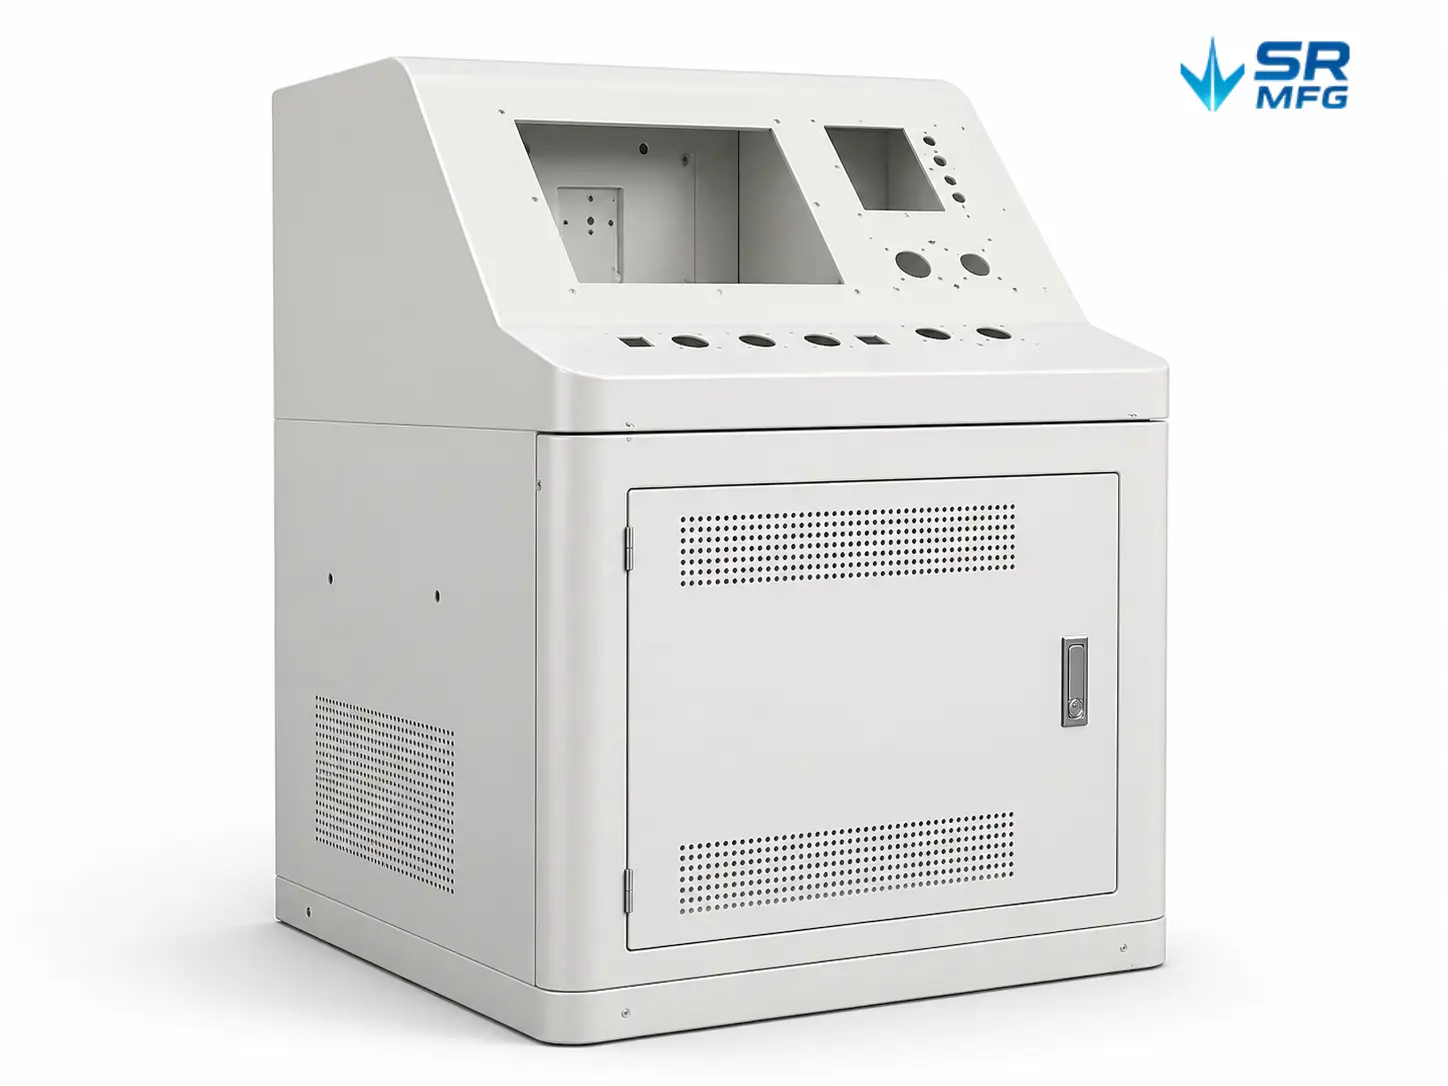
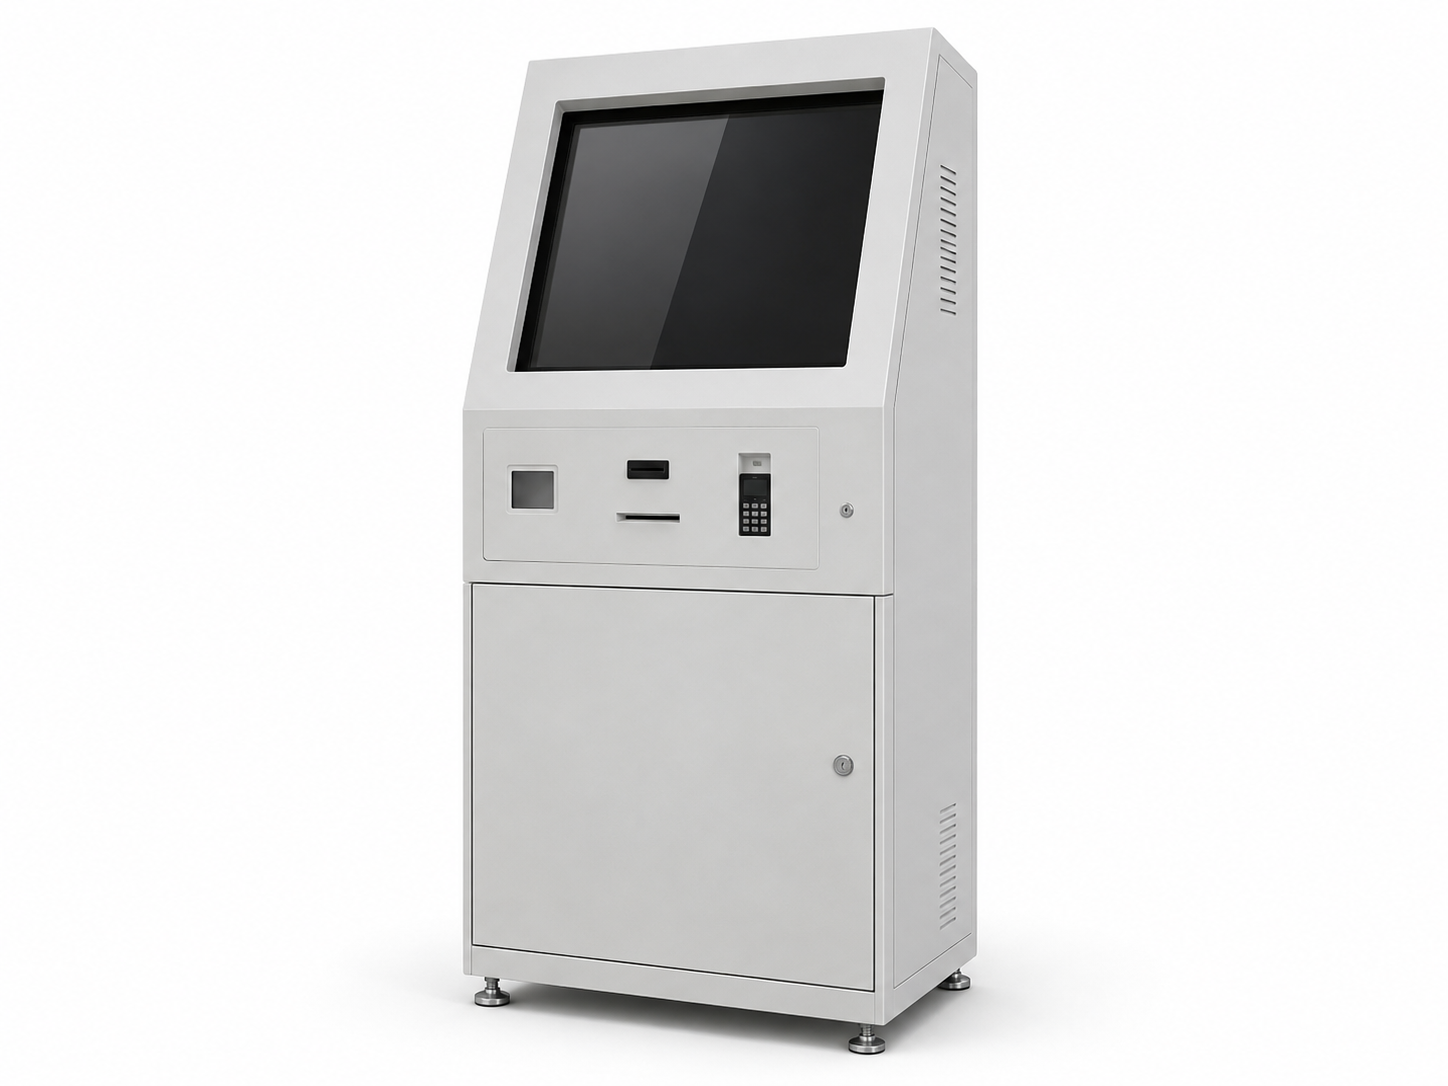
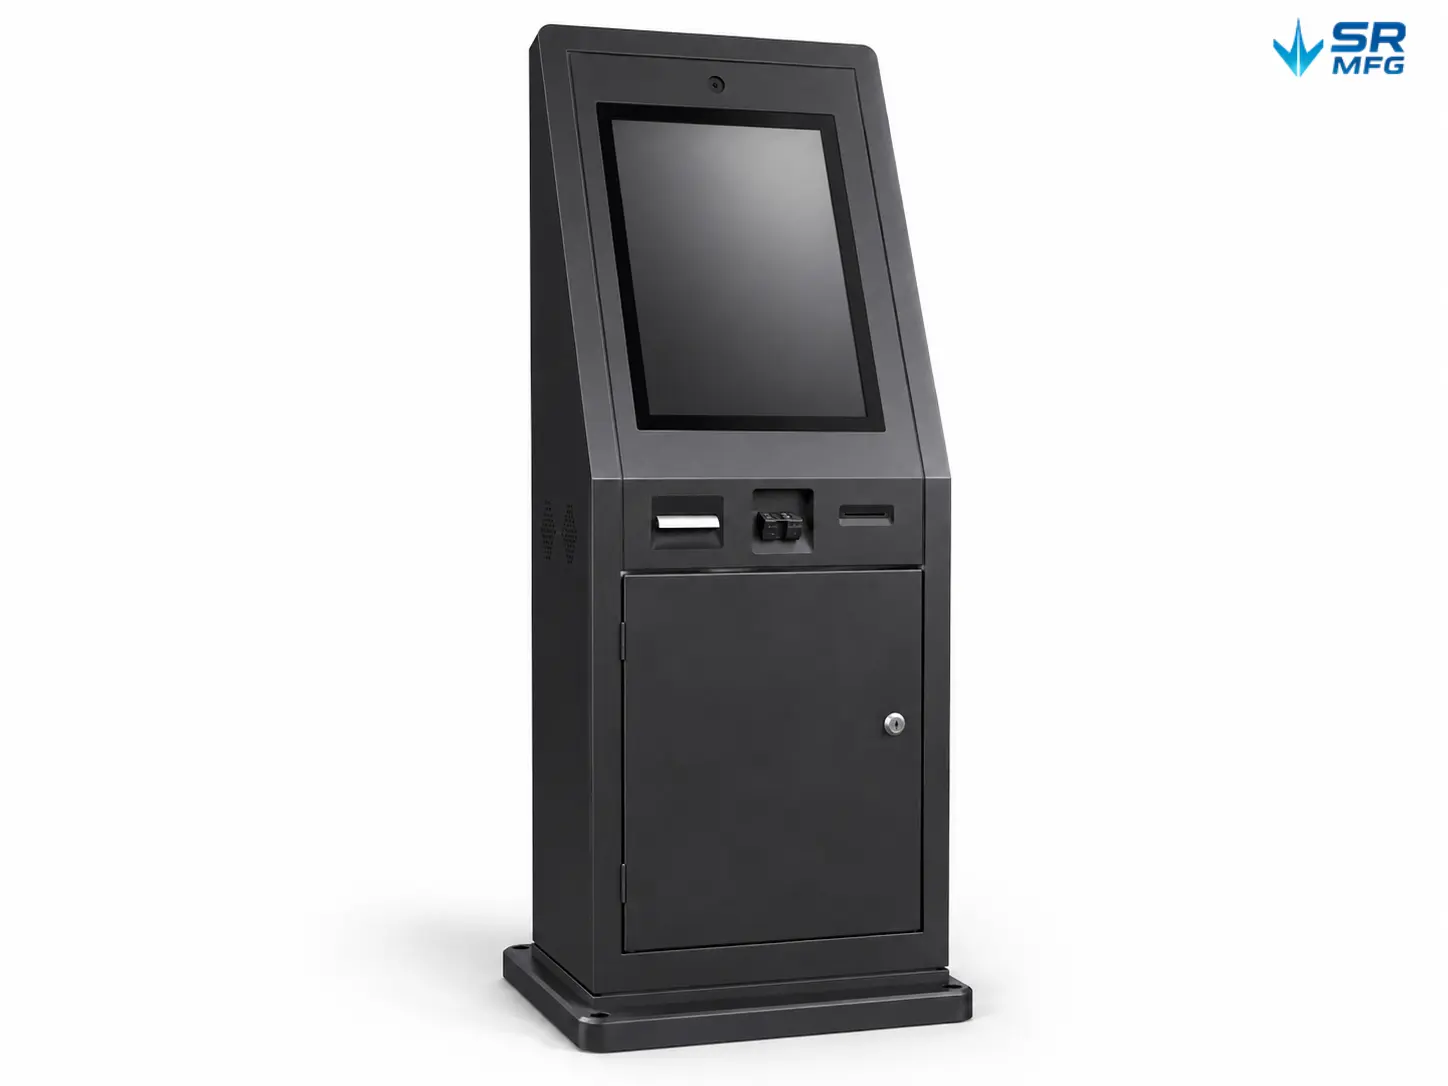
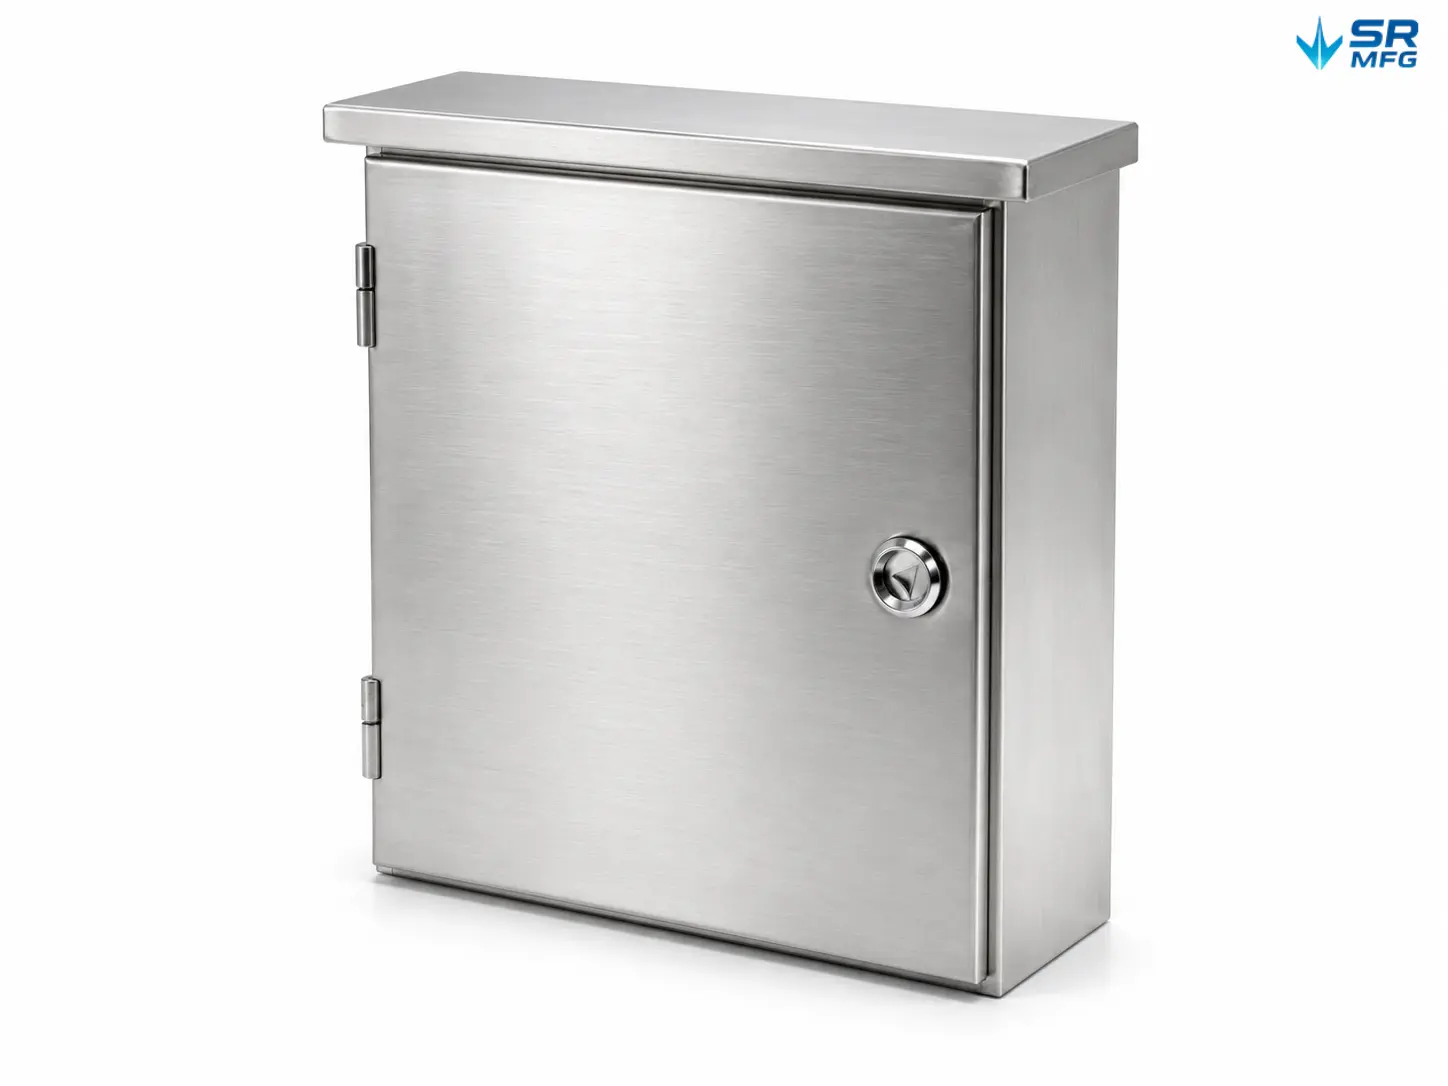
SR MFG Powder Coating Product Showcase
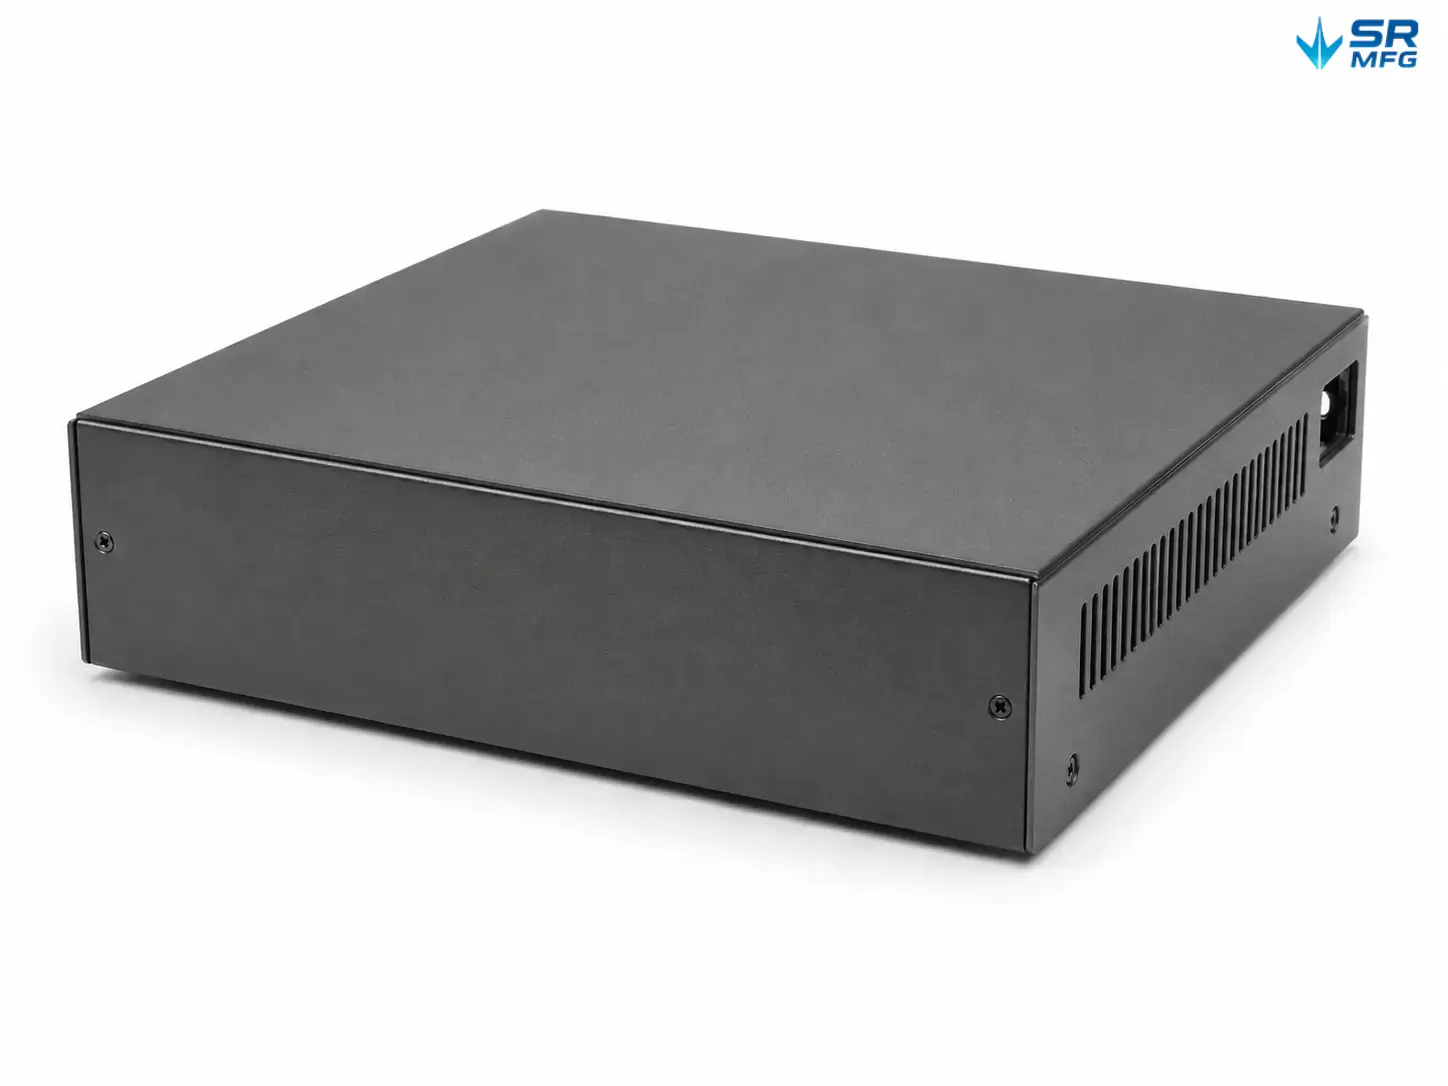
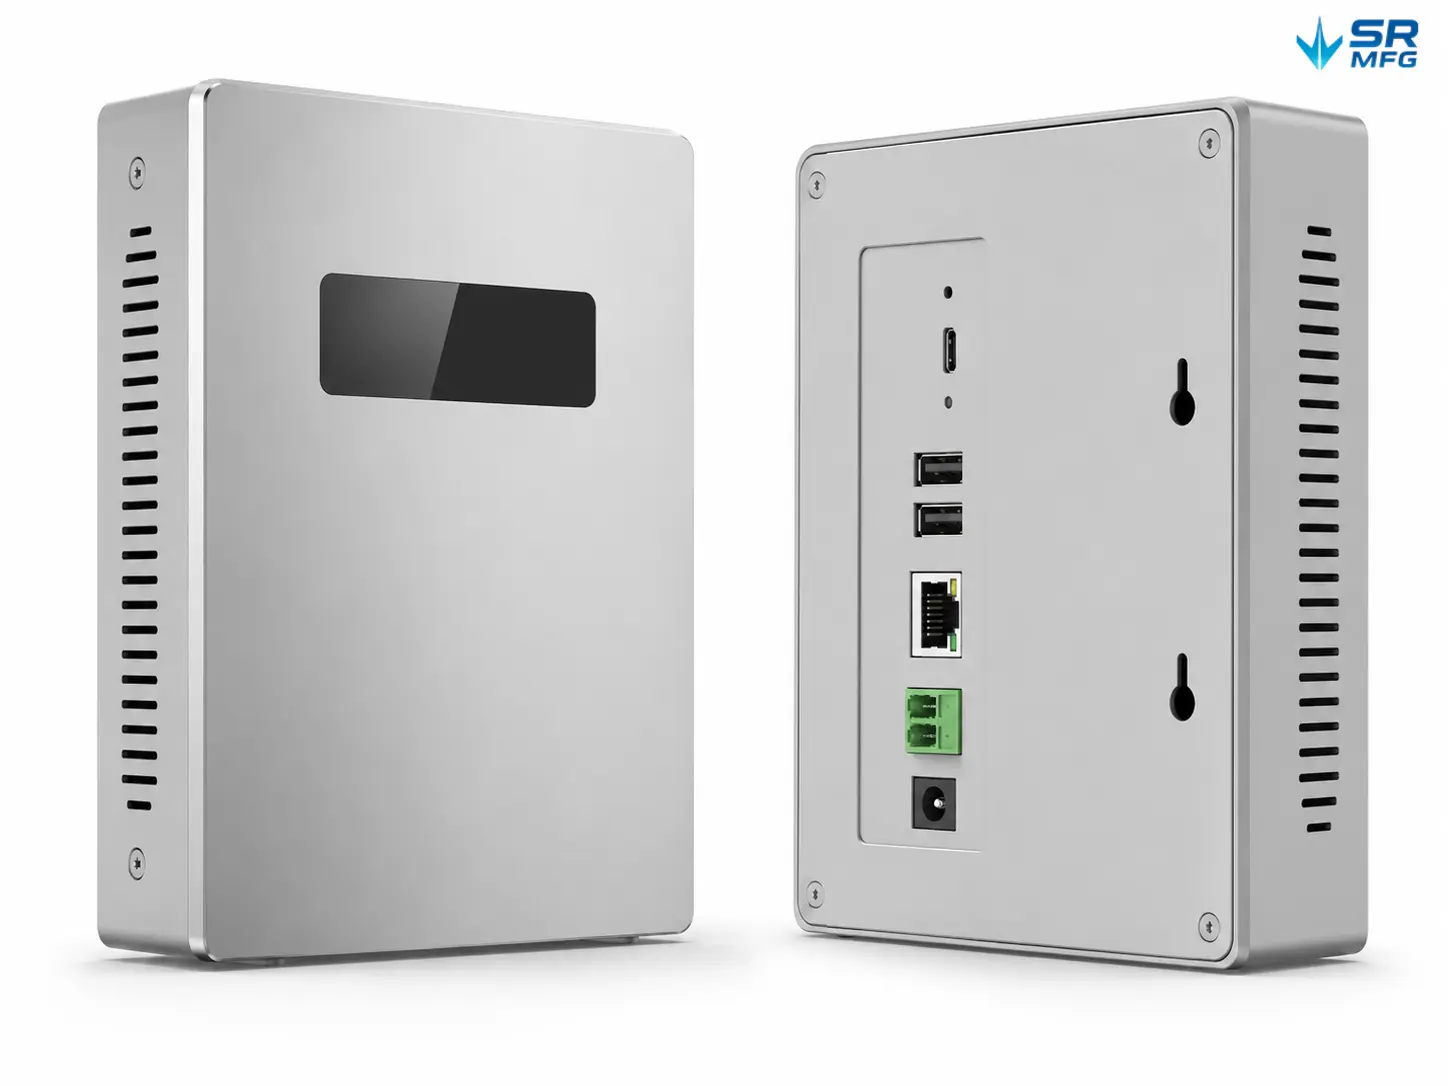
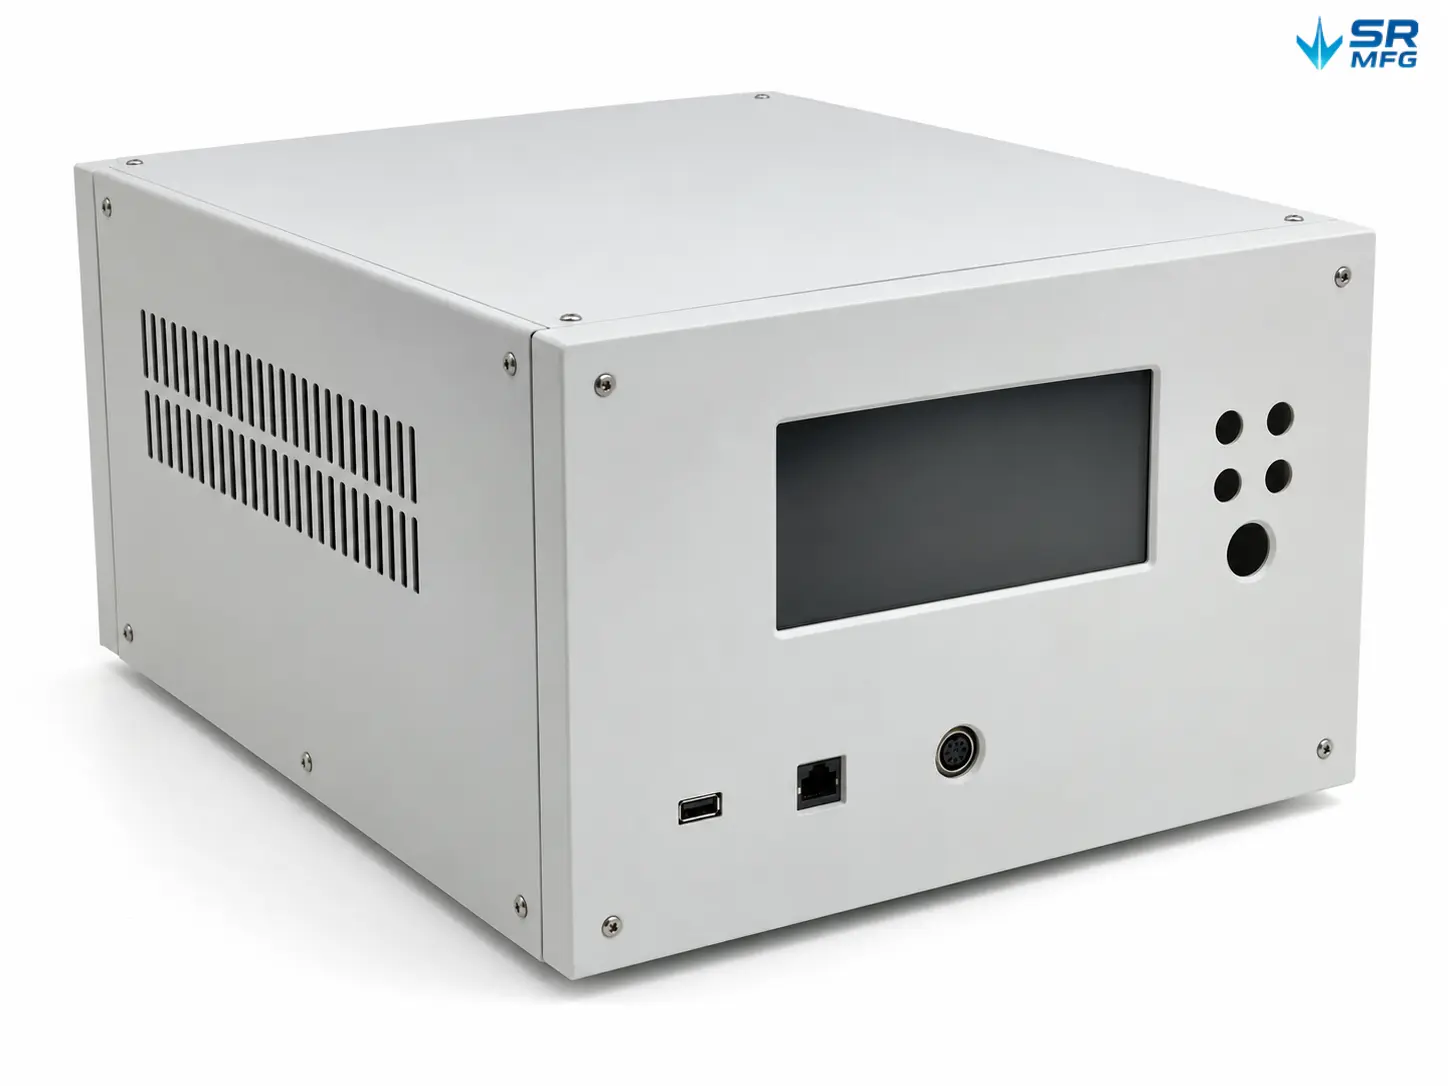
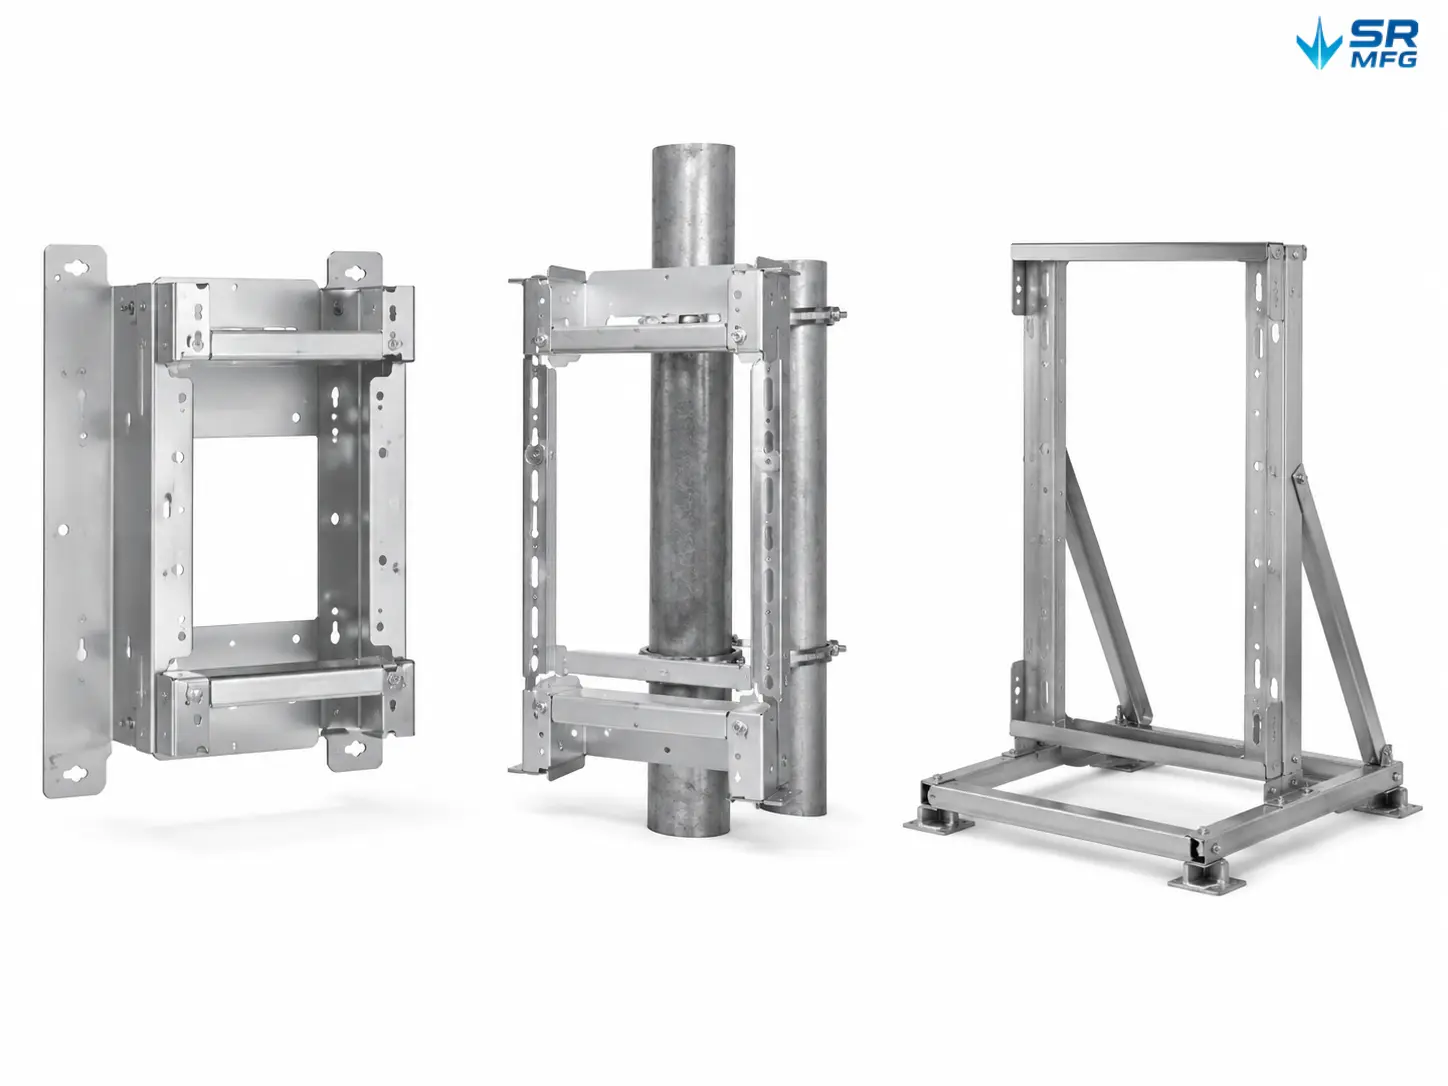
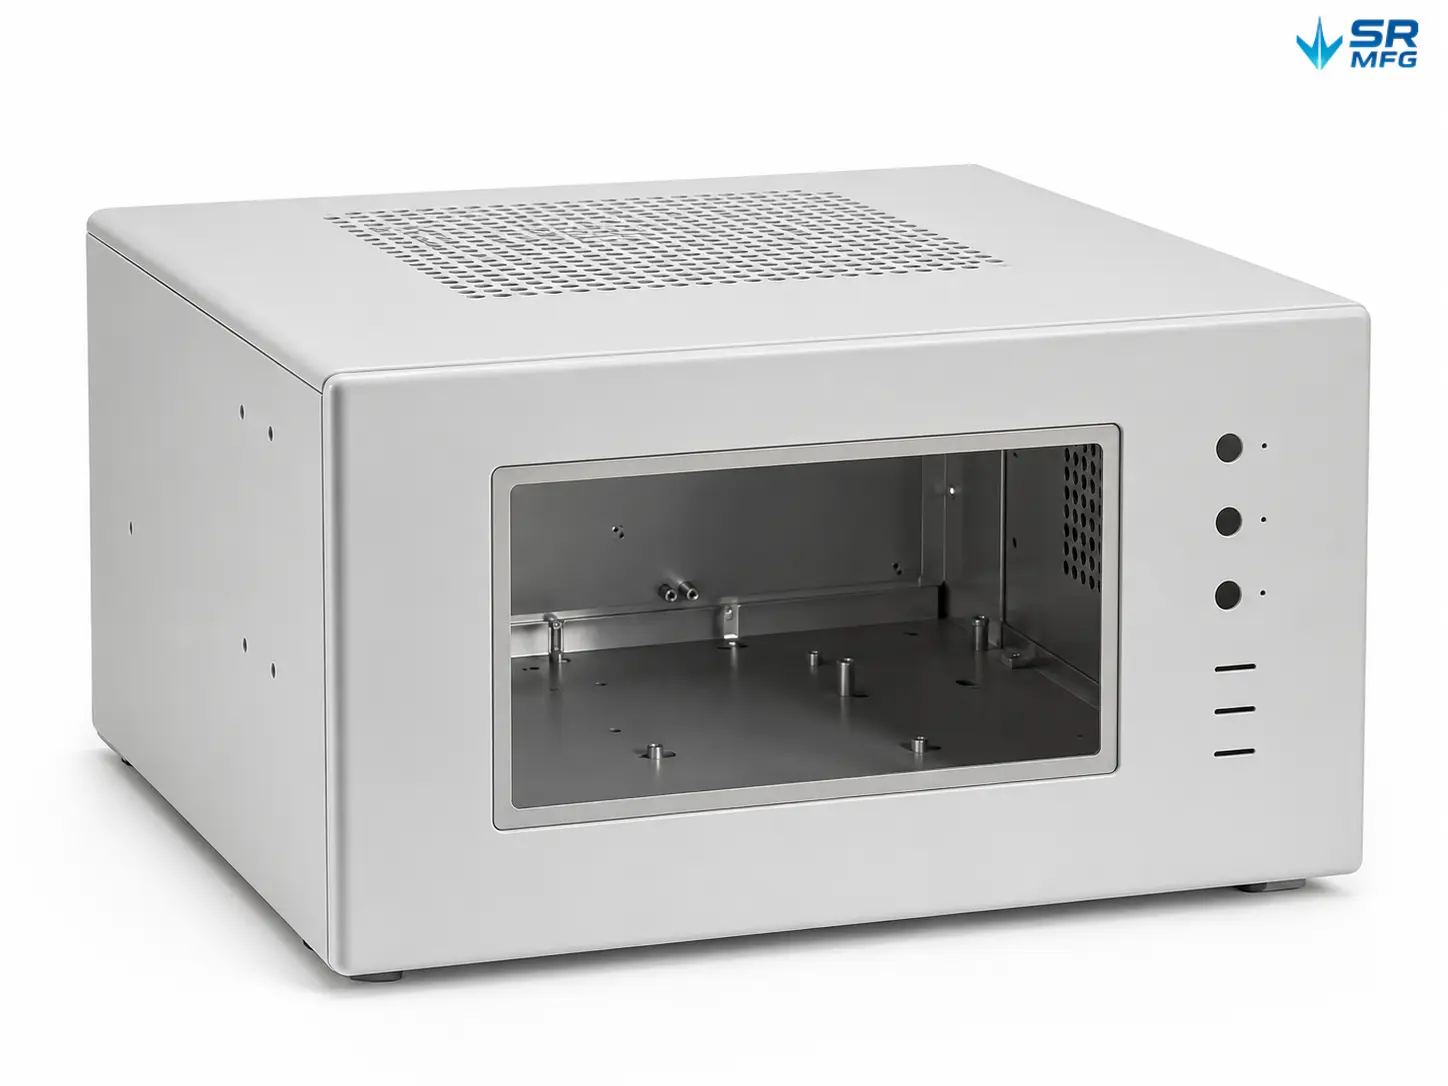
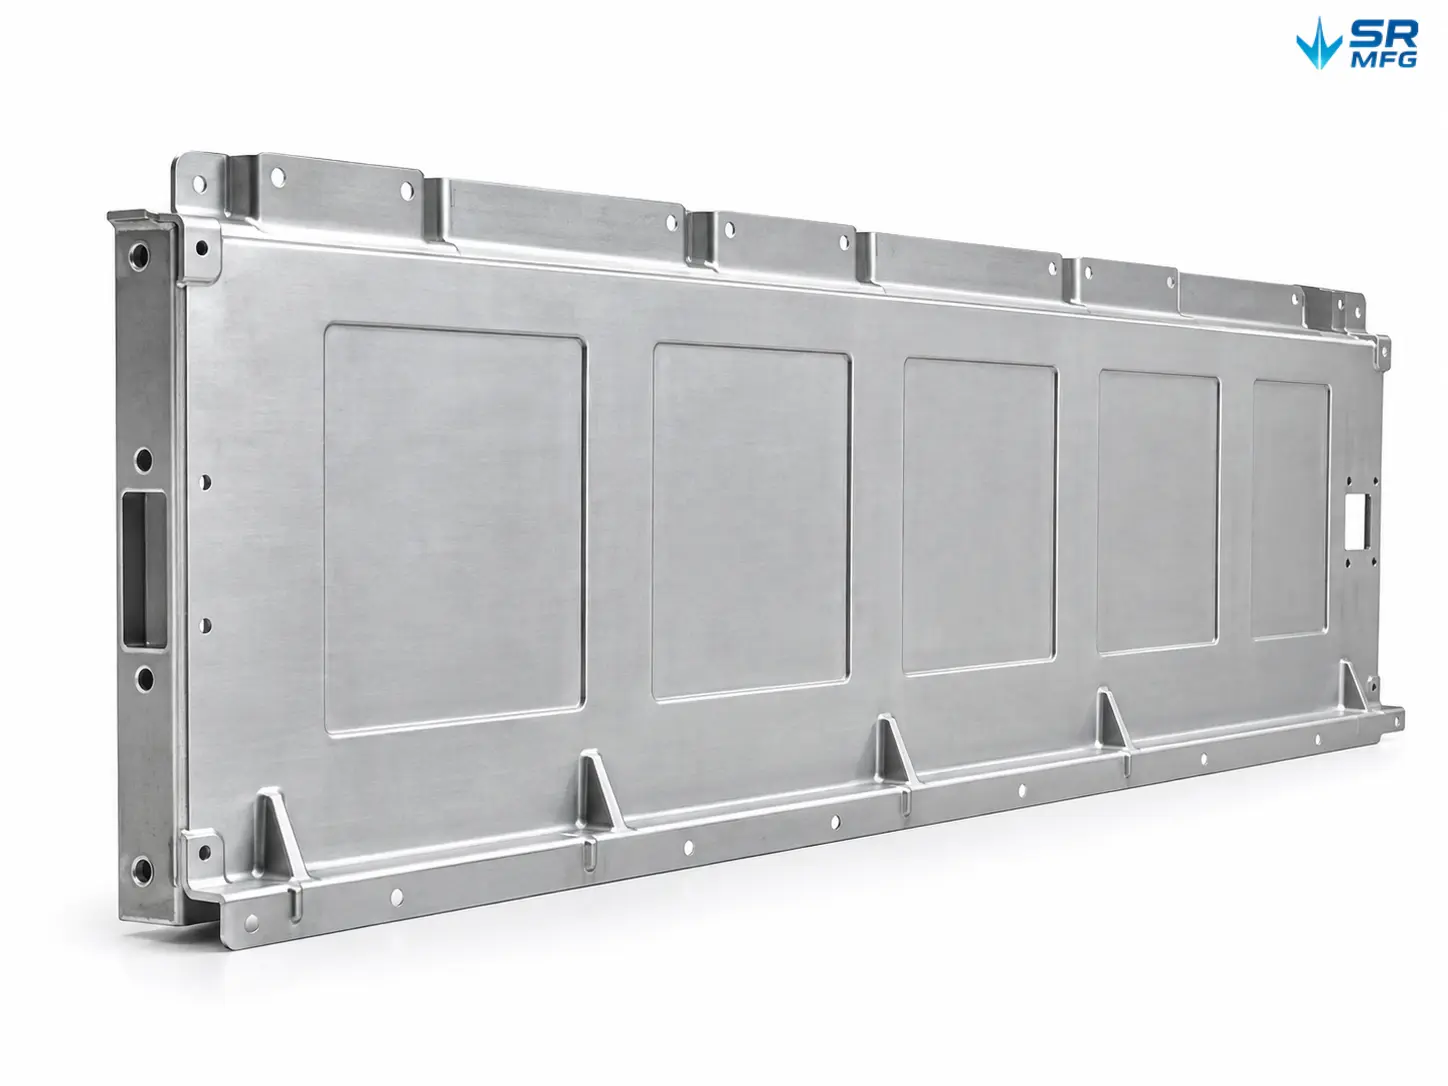
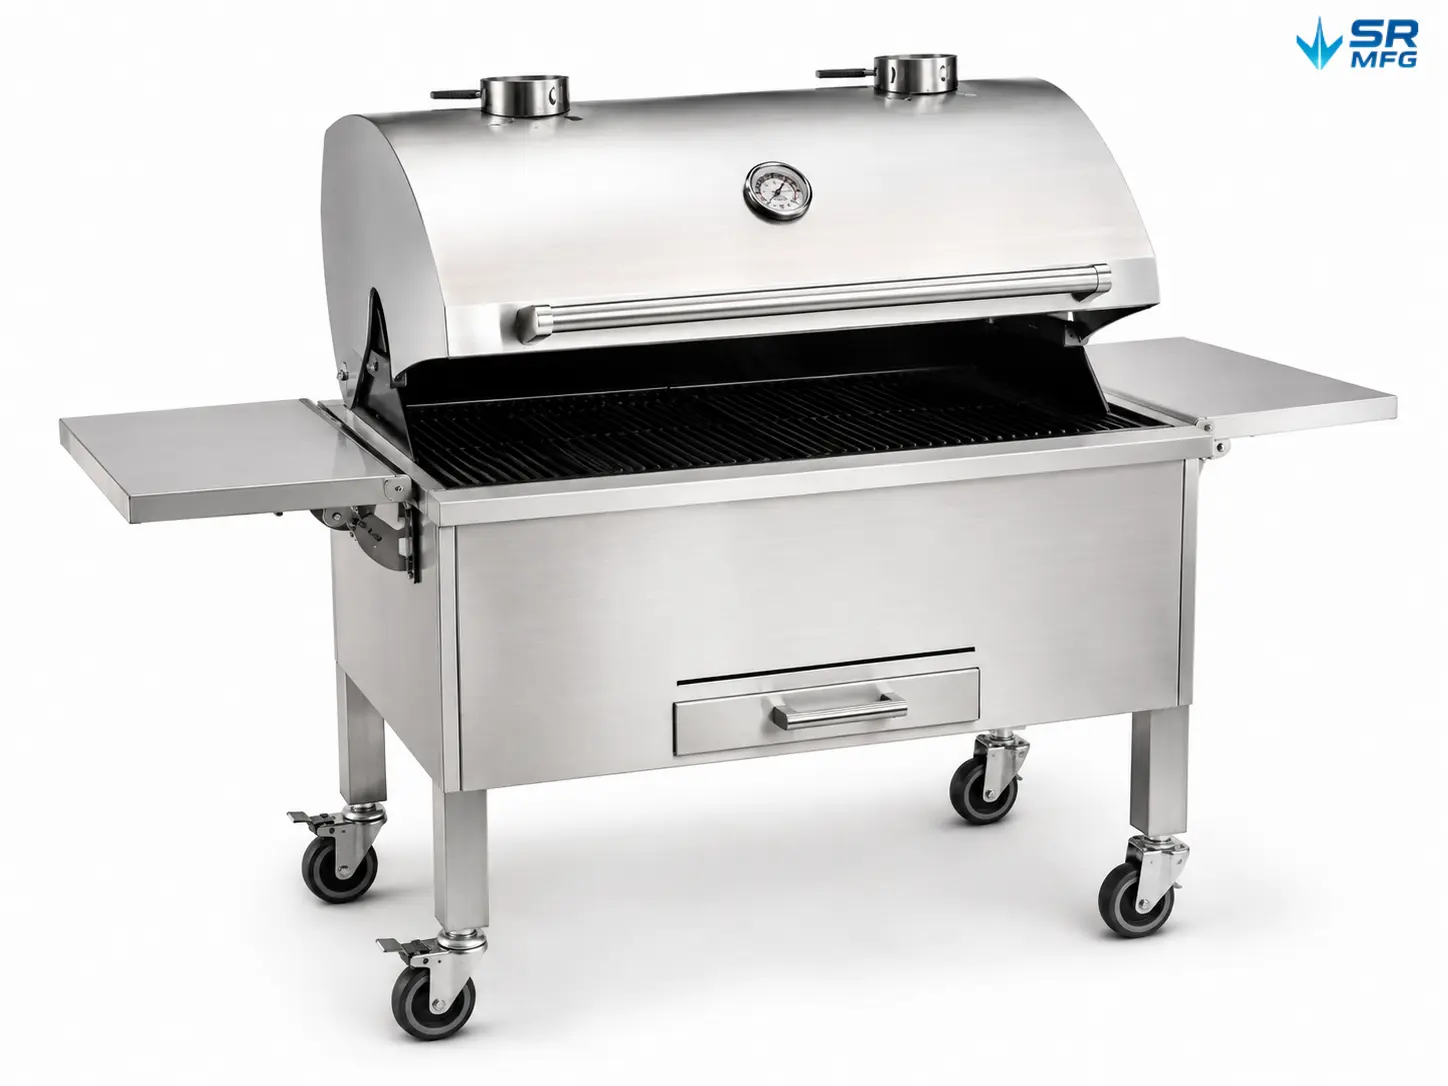
Sheet Metal Powder Coating Häufig gestellte Fragen
-
Typical DFT range: 50–100 μm
-
Typical build: 60 ± 10 μm
-
Recommended target: 60–80 μm (balanced corrosion protection and cost)
If a critical mating/locating surface needs thickness control or must be left uncoated, we typically use a combination of:
-
Masking for thickness control: High-temperature masking film/tape creates a controlled “window” to prevent build-up that could affect fit.
-
Built-in process allowance: Add a small masking step/ledge in the design so the masking edge doesn’t land on a Class A surface.
-
Closed-loop verification: DFT can be measured per ASTM D7091 (calibration/verification/adjustment + compliant measurements) with records retained to ensure reliable production readings.
We support RAL / Pantone matching, and production is controlled to the approved sample. During production we compare under standardized lighting, and the ΔE target can be defined per project (down to ≤ 1.0 when required).
The main limitation with metallics and pearlescents is visual physics: flake orientation can create angle-dependent color shift, sparkle differences, and higher sensitivity to batch and application parameters. To manage this, we typically:
-
Use the same powder lot for the same assembly or cosmetic surface whenever possible.
-
Define a clearer acceptance method for effect colors (specified light source, viewing angle, allowable color/appearance tolerances).
We can arrange testing per ASTM B117 or ISO 9227 (NSS/AASS/CASS), as required.
Key notes:
-
ASTM B117 defines the test environment, but does not specify test duration or pass/fail criteria. Duration and acceptance criteria must come from your spec or a mutually signed inspection standard.
-
ISO 9227 defines frameworks for NSS (neutral salt spray), AASS (acetic acid salt spray), und CASS (copper-accelerated acetic acid salt spray), including method and condition requirements.
A typical salt spray report can include (formatted to your template if needed): sample and lot information, pretreatment/coating system and DFT, test method and parameters, duration, inspection frequency, photos, and your specified acceptance items (e.g., blister rating, rust area, scribe creep/undercut, etc.).
In deep recesses and inside corners, electric field lines favor the shortest path to ground. Powder builds on outer edges while recesses become hard to coat—this is the classic Faraday cage effect.
Our typical combined approach:
-
Lower kV and limit µA (many practical setups reduce recess spraying to roughly 40–60 kV, then fine-tune).
-
Reduce powder output and airflow, and adjust gun distance/angle to “feed” a softer cloud into corners.
-
If needed, use strategies better suited for complex geometry (pulse control, different nozzles/patterns, or evaluating tribo application where appropriate and validated).
Pinholes/blisters are most often caused by outgassing: gas or moisture trapped in the substrate/surface layer (porosity, zinc layer, oxides, residual water/contamination) is released during curing and breaks through the molten film.
When we strongly recommend (or require) a pre-bake / outgas bake:
-
Galvanized parts: the zinc layer and surface oxides can trap moisture/air that releases during heating.
-
Castings/die cast/porous substrates and welded structures: porosity can release gas rapidly during cure—pre-bake is recommended, and outgas-forgiving powder (OGF) may be evaluated.
We also emphasize curing to verified PMT (Part Metal Temperature) and recording the cure curve—avoiding situations where air temperature reaches target but the part does not.
We first assess defect type and scope:
-
Minor scuffs/small defects: may be repairable with a matching touch-up system (liquid touch-up is common for field repair).
-
Class A cosmetic surfaces or corrosion-critical defects: typically recommend stripping, re-pretreating, and re-coating, then repeating key inspections (DFT/adhesion/appearance).
For color consistency: solid colors are generally easier to match. Metallics/pearls are more sensitive because flake orientation and gloss/texture affect appearance—repairs are more visible. We usually define the rework strategy and acceptance method during sample approval.
Wear resistance doesn’t mean a coating is immune to rub marks. Our common approach:
-
Pack only after parts cool to room temperature to avoid tape/film imprints and condensation issues.
-
Isolate Class A surfaces: non-woven sleeves/bags, foam separators, layered pads—no face-to-face stacking.
-
Transit protection: edge guards and custom dunnage to reduce vibration-driven abrasion.
-
MOQ: 100 pcs per batch (small runs negotiable; custom colors may be limited by powder supplier MOQ).
-
Changeover time: standard colors ≤ 30 minutes; metallic/special-effect colors ≤ 60 minutes (depends on scheduling).
-
Standard lead time: typically 3–7 days, depending on quantity, geometry, masking tooling, and validation requirements.
If salt spray/weathering validation is required, please specify method + duration + acceptance criteria in the PO/inspection standard—lead time will be adjusted accordingly.
Yes—on a project basis. We first confirm:
-
AAMA 2604/2605 are common benchmarks for performance and test methods for factory-applied organic coatings used in architectural exterior applications (typically aluminum extrusions and panels).
-
Whether you need 2604 vs. 2605 depends on service-life targets, color/gloss requirements, and exposure environment.
We select an appropriate powder system (e.g., super-durable polyester or higher-performance systems), define the validation plan (DFT, adhesion, corrosion resistance, weathering/color & gloss retention, etc.) in the inspection standard, and can support third-party lab reports when required.
Powder Coating Technical Resources
Unit Price in Manufacturing: How It’s Calculated and What B2B Buyers Should Compare
ShuangRui2026-08-27T03:41:28+00:00August 21, 2026|
When a supplier sends you a quote for 5,000 sheet metal brackets, the number that matters most is [...]
Gasket Installation Inspection for Sheet Metal Assemblies: Step-by-Step Checks & Acceptance Criteria
ShuangRui2026-08-27T06:35:41+00:00August 26, 2026|
A gasket is seated, the bolts are torqued, and the flange gap looks even. The assembly moves to [...]
Nidec Scandal Deepens: 844 Misconduct Cases, Accounting Probe and Governance Questions
ShuangRui2026-09-09T02:07:12+00:00September 11, 2026|
According to CCTV Finance, an external investigation report released on September 4 by Japanese motor manufacturing giant Nidec [...]
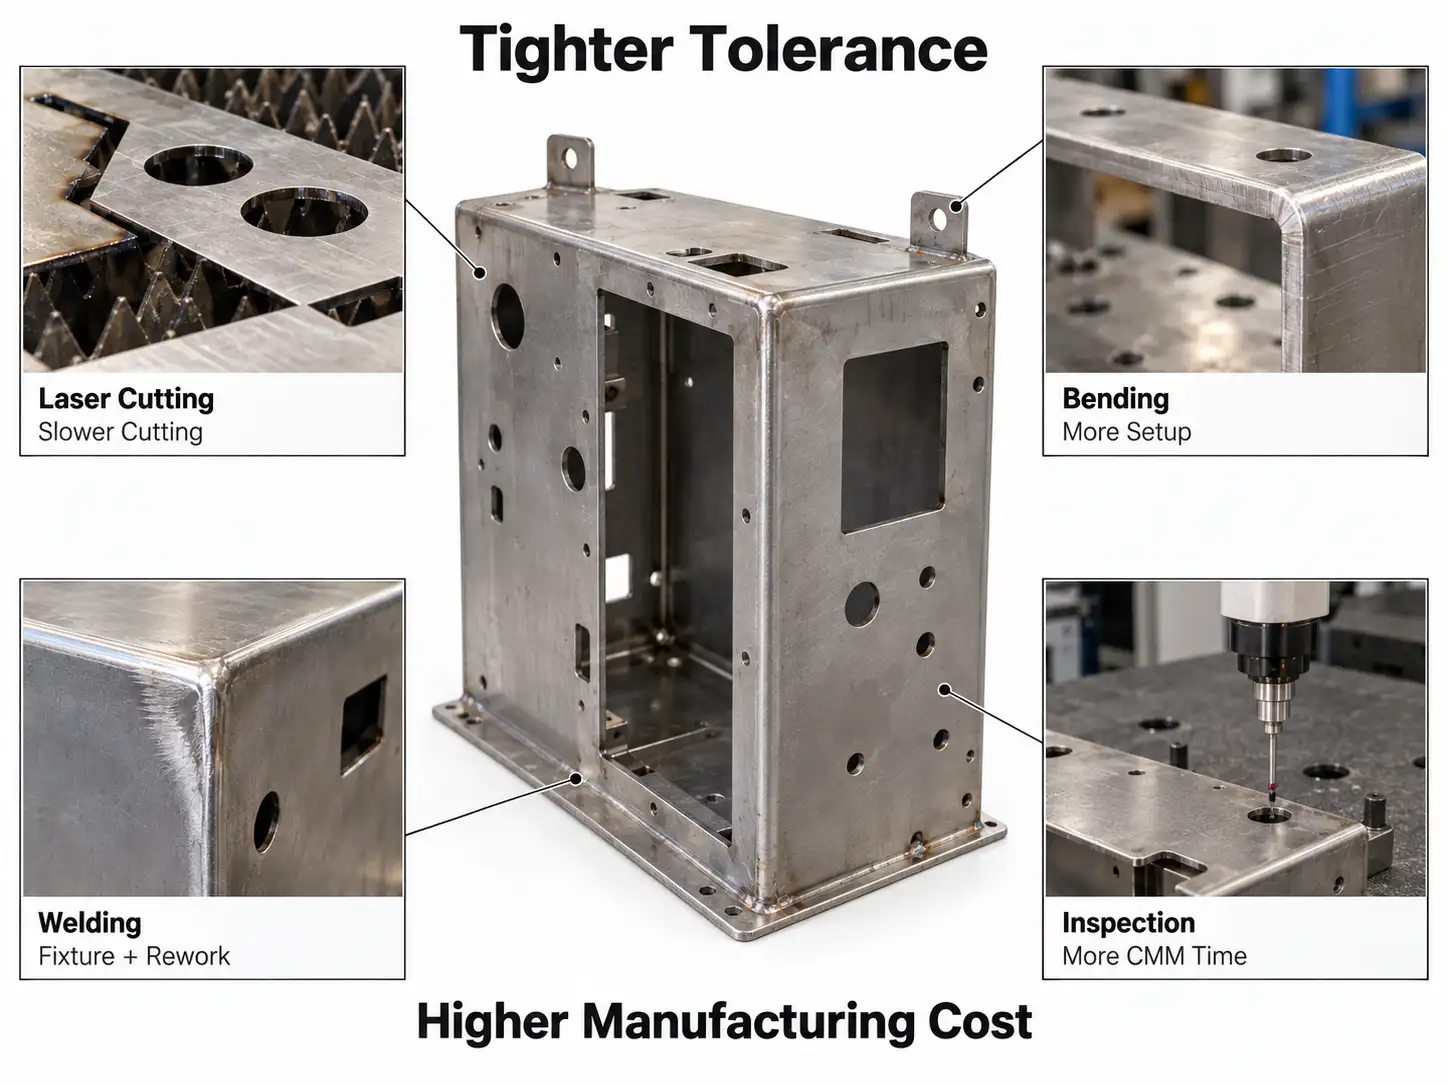
Blech-Toleranzoptimierung: Wo enge Toleranzen Kosten verursachen und wann Optimierung sich lohnt
ShuangRui2026-09-14T05:53:38+00:00September 16, 2026|
A single tolerance callout on a sheet metal drawing can add 20–40% to the quoted price — or [...]
