Mit Shuangrui zusammenarbeiten, um die Herstellungskosten zu senken durch 30% und die Effizienz zu steigern.

Blechschweißdienstleistungen2026-08-14T02:15:07+00:00

Blechschweißdienstleistungen für OEM-Programme

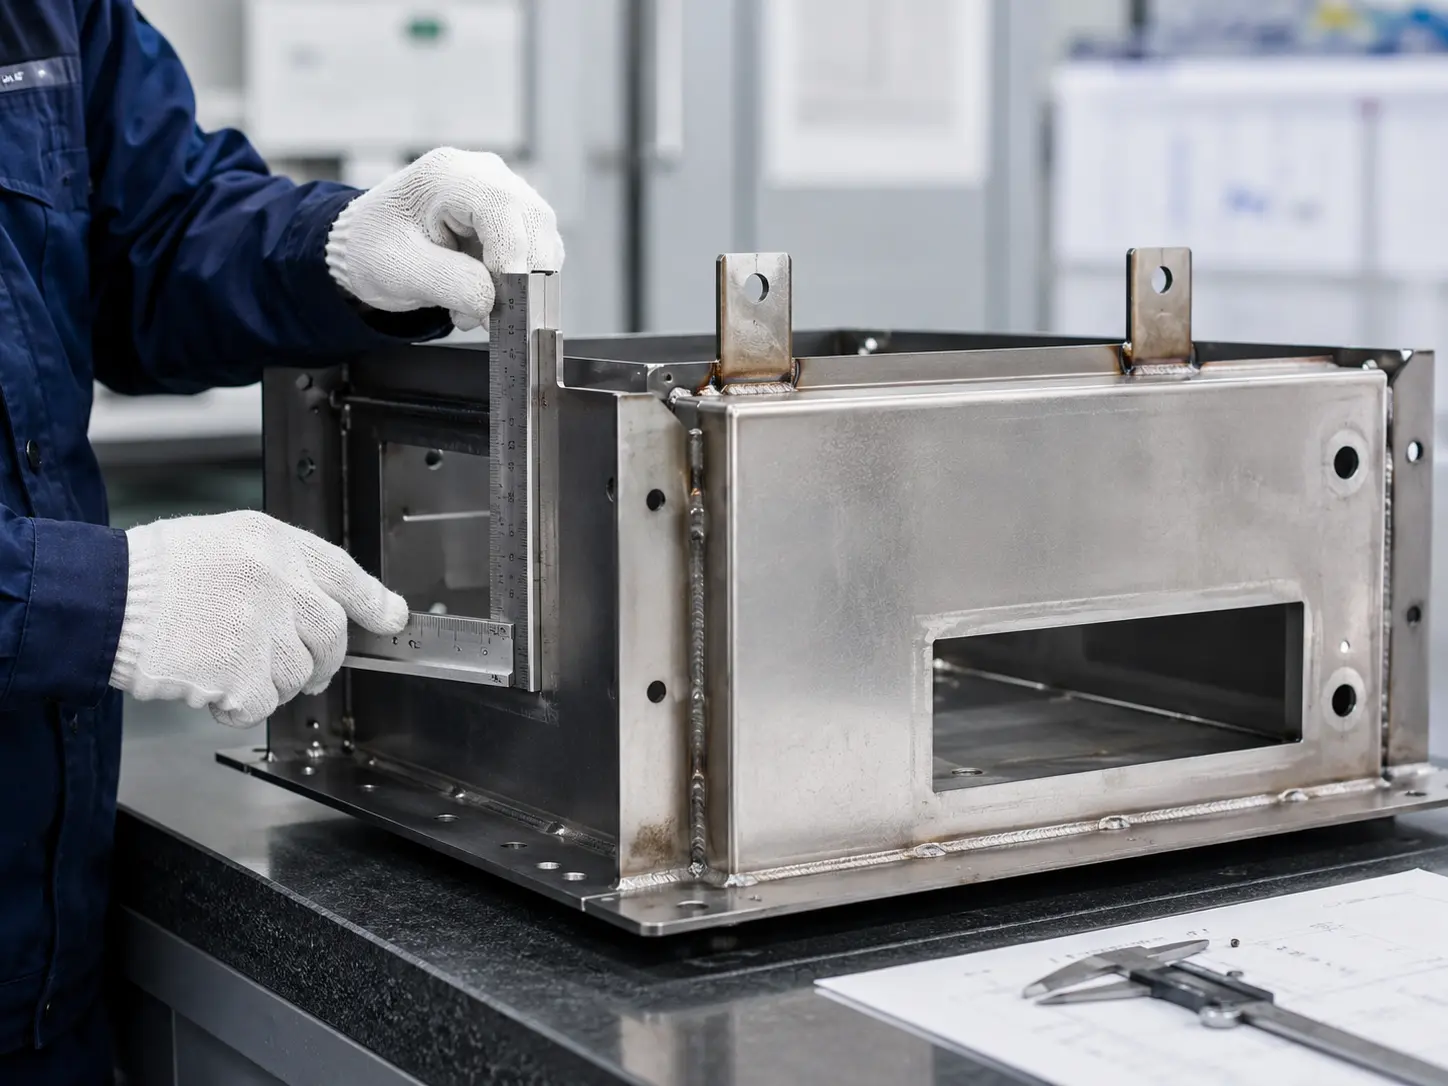
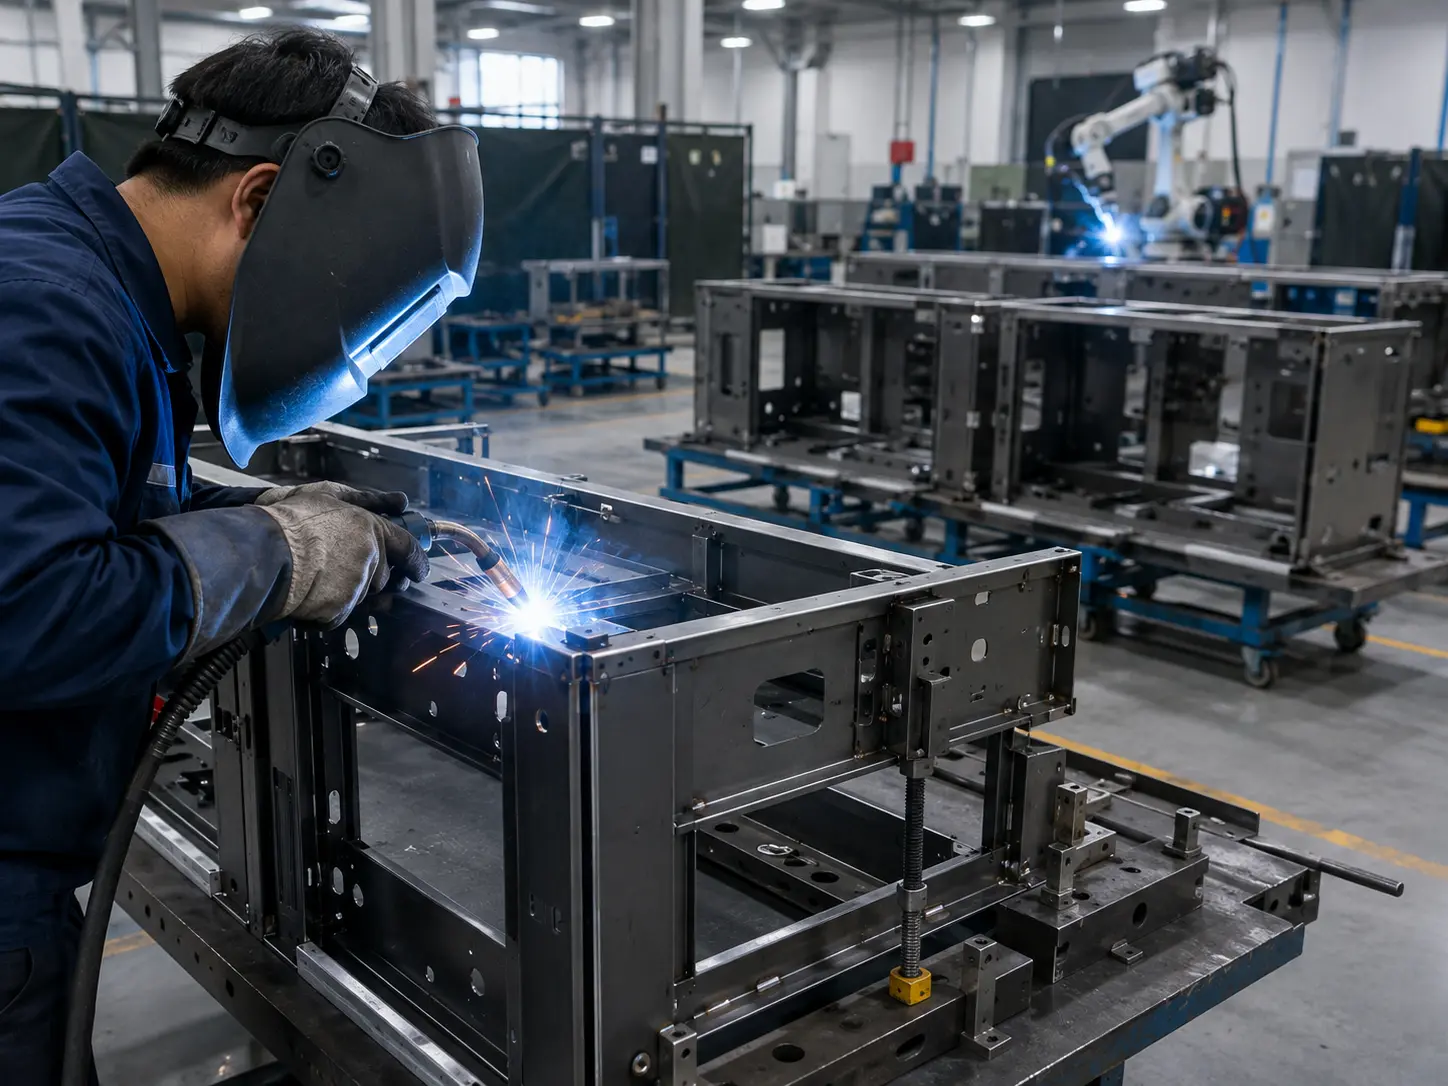
SR MFG bietet Blechschweißdienstleistungen für OEM-Programme und kombiniert Roboterschweißen, manuelles Schweißen, Vorrichtungssteuerung und In-Prozess-Prüfung, um Schweißfestigkeit, Erscheinungsbild und Maße stabil zu halten.

Unsere Schweißprozesse sind mit Laserschneiden, Biegen, Oberflächenveredelung und Endmontage integriert, wodurch Kunden Nacharbeit reduzieren, die Lieferantenkoordination vereinfachen und eine stabile Produktion vom Prototyp bis zur Serienfertigung unterstützen können.
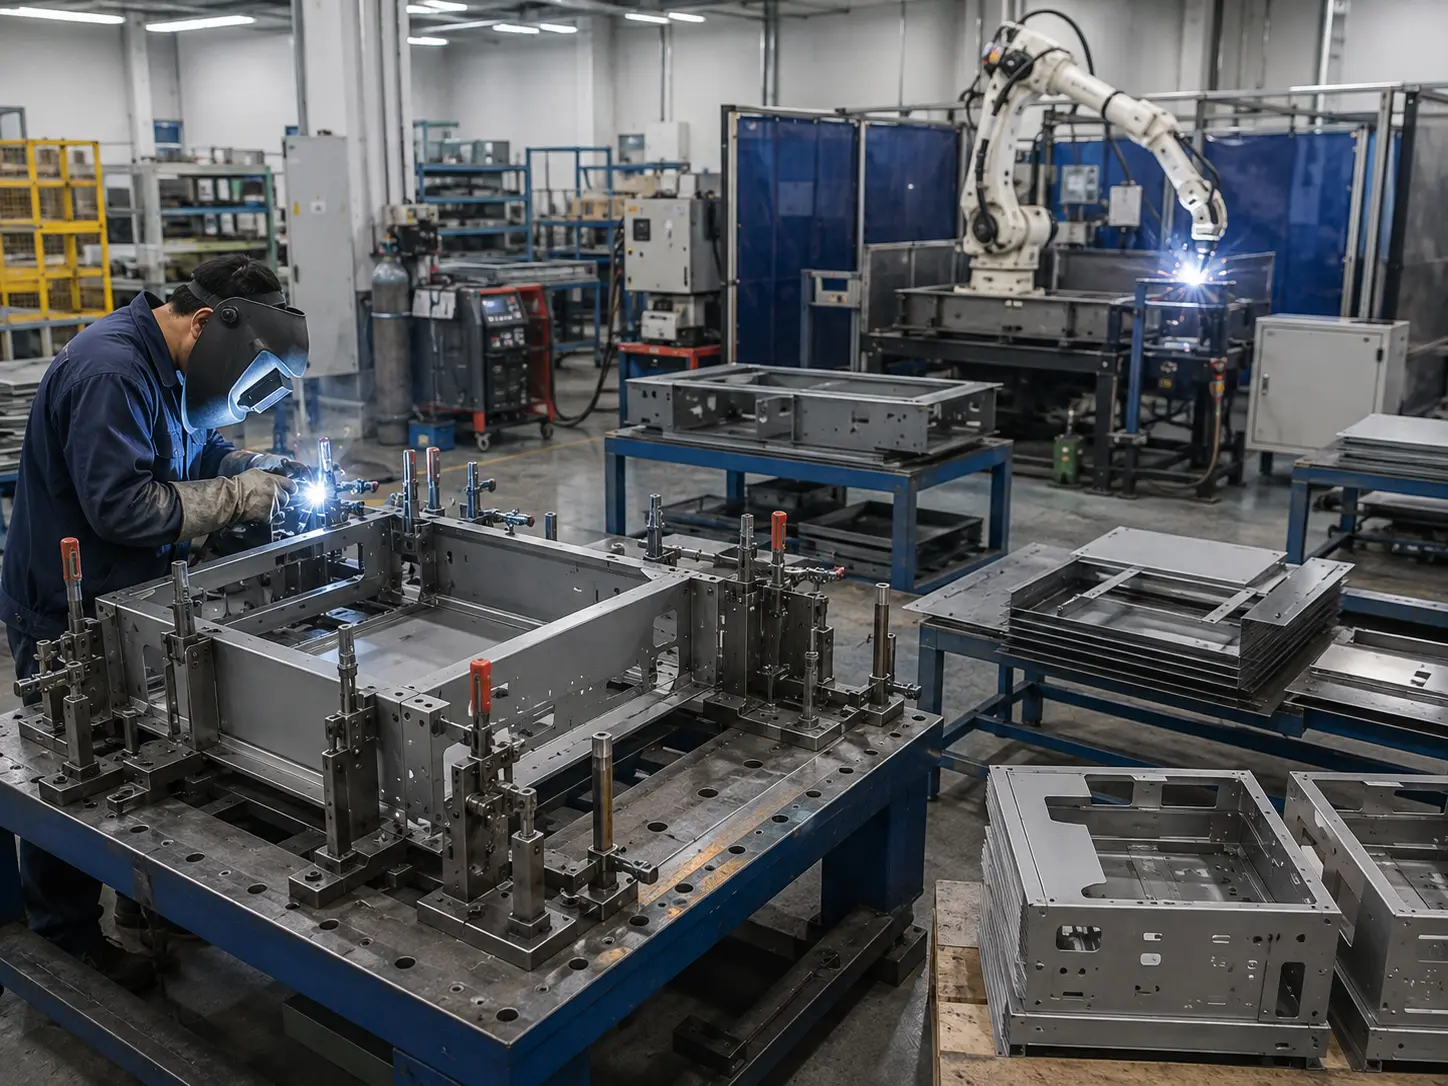
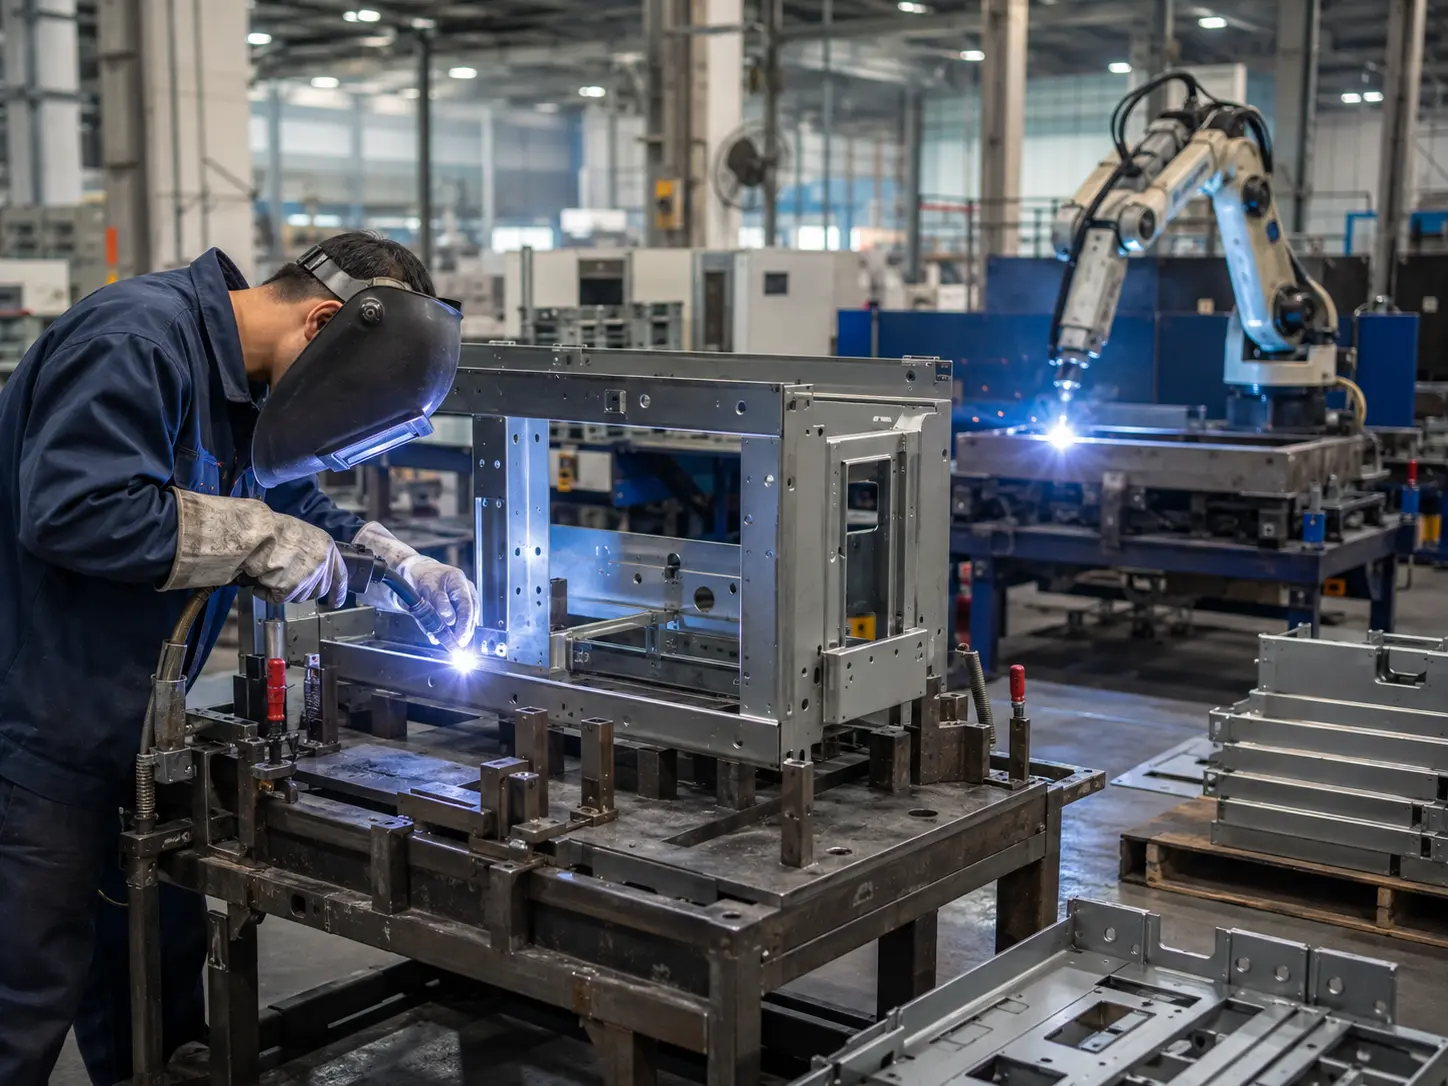
Roboterschweißen & manuelles Schweißen
Vorrichtungsgesteuerte Präzision
OEM-Serienfertigung

Erhalten Sie ein individuelles Angebot in 24 Stunden

Laden Sie Ihre Zeichnungen zur technischen Prüfung hoch.

Leeres Formular (#4)

Warum SR MFG für Blechschweißen wählen

Wir kontrollieren die Schweißqualität von der Vorrichtungsplanung bis zur Endmontage und helfen OEM-Projekten, Verzug, Nacharbeit und Chargenschwankungen zu reduzieren.

Blechschweißdienstleistungen

Verzugskontrolle

Schweißreihenfolge, Vorrichtungen und Wärmeeintrag werden vor der Produktion geplant, um Verzug und Nacharbeit zu minimieren.

Roboterschweißen + manuelles Schweißen

Roboterschweißen gewährleistet Konsistenz bei wiederholbaren Teilen, während manuelles Schweißen komplexe Baugruppen und enge Bereiche bewältigt.

Konsistenz vom Prototyp bis zur Produktion

Freigegebene Schweißparameter und Prozessstandards gewährleisten stabile Qualität von Prototypen bis zur Massenproduktion.

Integrierter Blechfertigungsfluss

Das Schweißen ist mit Schneiden, Biegen, Oberflächenveredelung und Montage integriert, um Handhabungsfehler und Durchlaufzeit zu reduzieren.

Ihre Bedenken (Schweißen) Typischer Schweißlieferant SR MFG Schweißansatz
Schweißverzug &
Montagepassung
Das Schweißen hängt stark von der Erfahrung des Bedieners ab. Verzug wird oft später durch Hämmern, Richten oder das Hinzufügen von Ausgleichsblechen korrigiert. Schweißreihenfolge, Vorrichtungen und ausgewogener Wärmeeintrag werden im Voraus geplant, um Verzug zu minimieren und eine präzise Passung vor der Montage zu gewährleisten.
Prototyp vs.
Massenproduktion
Konsistenz
Prototypen werden vom erfahrensten Schweißer geschweißt, aber die Massenproduktion variiert je nach Bediener oder Station, was zu Unterschieden im Erscheinungsbild und in den Maßen führt. Roboterschweißen, Parameterbibliotheken und Erstmusterfreigabe halten denselben Prozess und Prüfstandard von Pilotläufen bis zur Langzeitproduktion aufrecht.
Integration mit
Blech-
prozess
Das Schweißen wird als separater Schritt behandelt, wobei nachgelagerte Biegekorrekturen, Beschichtung oder Endmontageanforderungen ignoriert werden. Das Schweißen ist mit Laserschneiden, Biegen, Veredelung und Montage unter Verwendung gemeinsamer Bezugspunkte und Positionierelemente integriert, um Nacharbeit zu reduzieren und die Lieferung zu beschleunigen.

Bereit für Ihr Schweißangebot?

Laden Sie Ihre Zeichnungen hoch und teilen Sie uns Ihre Anforderungen mit. Unser Engineering-Team prüft Ihr Projekt und antwortet innerhalb von 24 Stunden.

Schweißangebot anfordern →
Sheet metal welding capabilities with robotic welding, manual welding, and welded metal assemblies
Fähigkeiten

Präzisions-Blechschweißfähigkeiten von SR MFG

SR MFG bietet professionelle Schweißdienstleistungen für Blechstrukturen und -gehäuse. Wir verwenden MIG-, TIG-, Widerstands-, Punktschweiß- und Bolzenschweißverfahren, um starke, saubere und konsistente Schweißnähte zu liefern. Unser Engineering-Team wählt die am besten geeignete Methode basierend auf Teiledesign und Montageanforderungen aus, um die Strukturfestigkeit zu verbessern und die Gesamtkosten zu senken.

Mehrere Schweißverfahren

MIG-, TIG-, Widerstands-, Punkt- und Bolzenschweißen für unterschiedliche Anwendungsanforderungen.

Roboterschweißen & manuelles Schweißen

Roboterschweißen unterstützt wiederholbare Teile, während manuelles Schweißen komplexe Strukturen und enge Bereiche bewältigt.

Schweißqualitätssicherung

Arbeitsanweisungen, Parameterkontrolle und Prüfung helfen, eine stabile Schweißqualität in der Produktion aufrechtzuerhalten.

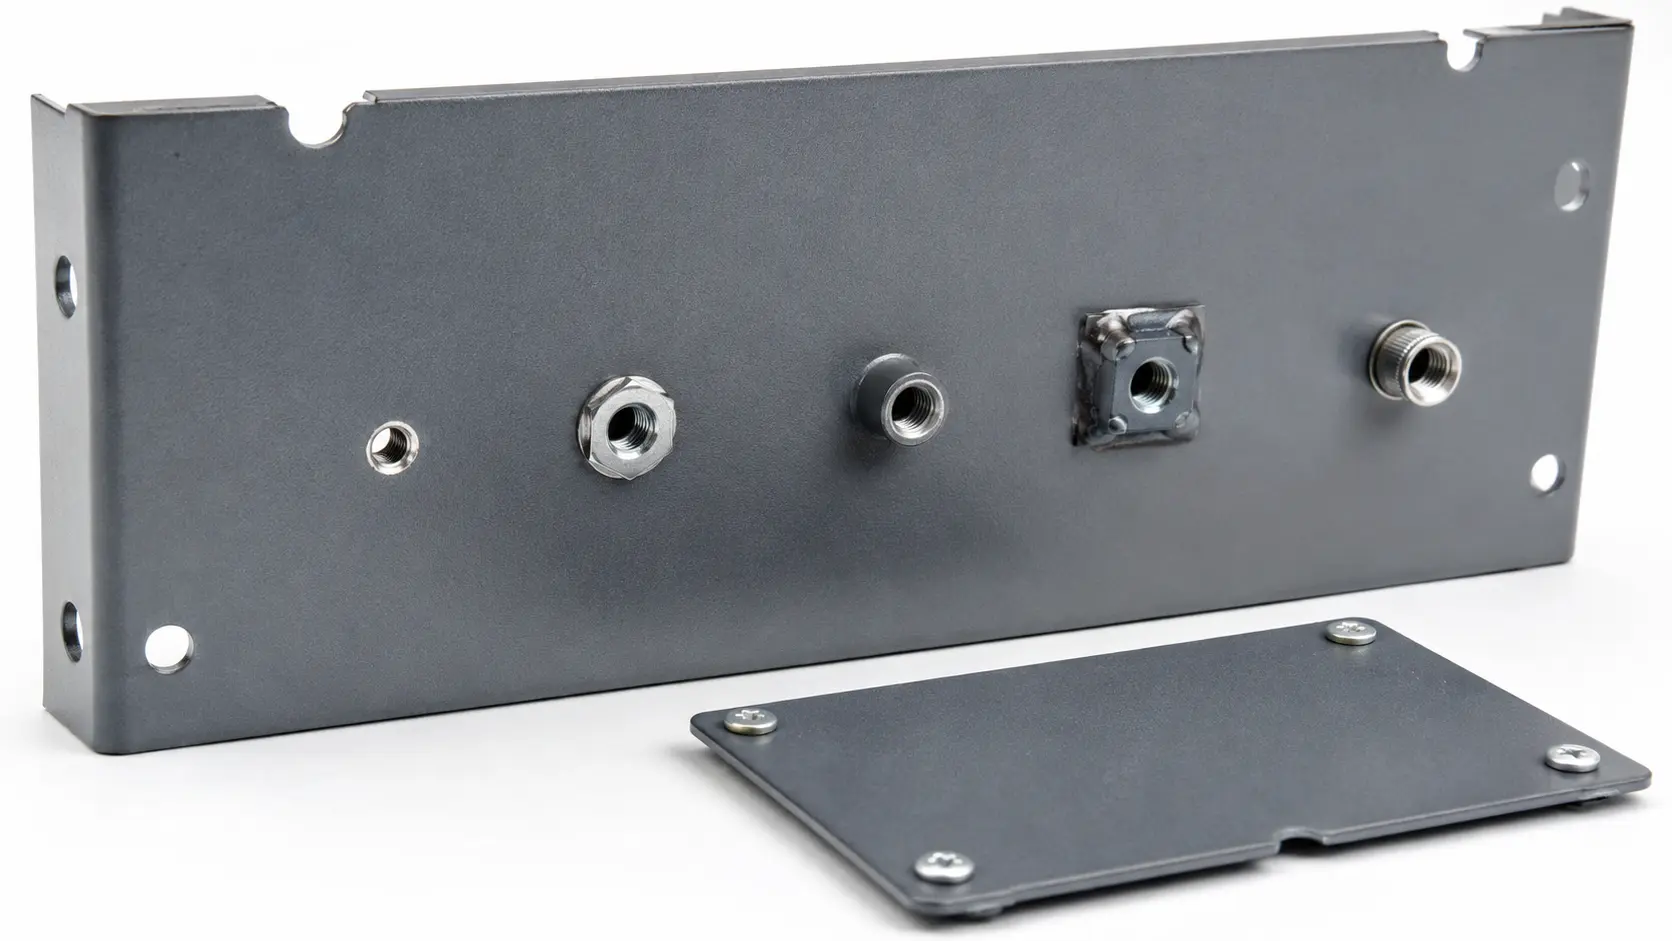
Integrierte Montageunterstützung

Das Schweißen arbeitet mit Biegen, Veredelung und Montage zusammen, um Nacharbeit zu reduzieren und die Durchlaufzeit zu verkürzen.

Schweißausrüstung & Produktionskapazität

Kernschweißanlagen und Kapazitätsbasis für OEM-Blechprojekte.

Kernschweißmaschinen

Fenghuo CO₂-Schweißgerät

  • Stromanpassungsgenauigkeit: ±5 A
  • Nahtüberhöhung: ≤ 1,5 mm
  • Einschaltdauer: 60%; Abschmelzleistung: 8 kg/h
  • Werkstoffe: Kohlenstoffstahl / niedriglegierter Stahl, 2–30 mm

Hanwang CO₂-Schweißgerät

  • Stromstabilität: ±3%
  • Nahtgeradheitsfehler: ≤ 0,5 mm/m
  • Max. Ausgangsstrom: 500 A; Einschaltdauer: 60%
  • Mittelstarke Bleche; 1,2–1,6 mm Massivdraht

Fenghuo Argon-Lichtbogenschweißgerät (WIG)

  • Zündungserfolgsrate: > 99%
  • Schweißverzug: < 0,5 mm/m
  • HF-Zündung: < 0,1 s; 8 h Dauerbetrieb
  • Werkstoffe: Edelstahl / Kupfer / Titan, 1–8 mm

Jasicfeng Argon-Lichtbogenschweißgerät (WIG)

  • Rechtwinkligkeitsfehler: ≤ 0,3 mm
  • Schweißpunktabweichung: ±0,2 mm
  • Typische Schweißgeschwindigkeit: 30–50 cm/min
  • Werkstoffe: kohlenstoffarmer Stahl / Edelstahl, 0,5–10 mm

Schweißroboter

CO₂-Schweißroboter FANUC 6-Achsen

  • Wiederholgenauigkeit: ±0,05 mm
  • Max. Reichweite: 3103 mm
  • Zykluszeit: < 45 s/Teil
  • Unterstützt Nahtverfolgung und Prozessüberwachung

Laser-Schweißroboter FANUC 6-Achsen

  • Bahngenauigkeit: ±0,15 mm
  • Schweißgeschwindigkeit: 5–15 m/min
  • WEZ: < 0,3 mm
  • Laserleistungsbereich: 100–3000 W

WIG-Schweißroboter FANUC 6-Achsen

  • Bahnwiederholgenauigkeit: ±0,03 mm
  • Hohlhandgelenk: 57 mm Bohrung
  • Unterstützt WIG-Impulsschweißen
  • Unterstützt Nahtverfolgung und visionsgestütztes Schweißen
Basiskapazität für Blechschweißen
300 × 300 mm Referenzteilgröße
3 × 100 mm Referenzschweißnähte
60% Anlagenauslastung
(Einschichtbetrieb)
60,000+ Standardteile / Monat
0.5–0.8 Umrechnungsfaktor für
komplexe Teile
i Capacity is assessed by part size, weld length, material thickness, fixture complexity, and order quantity.

Welding Types

Sheet Metal Welding ProcessOptions

SR MFG supports TIG, MIG / CO2, laser welding, and spot welding for different materials,
part structures, appearance requirements, and production volumes.
TIG Welding

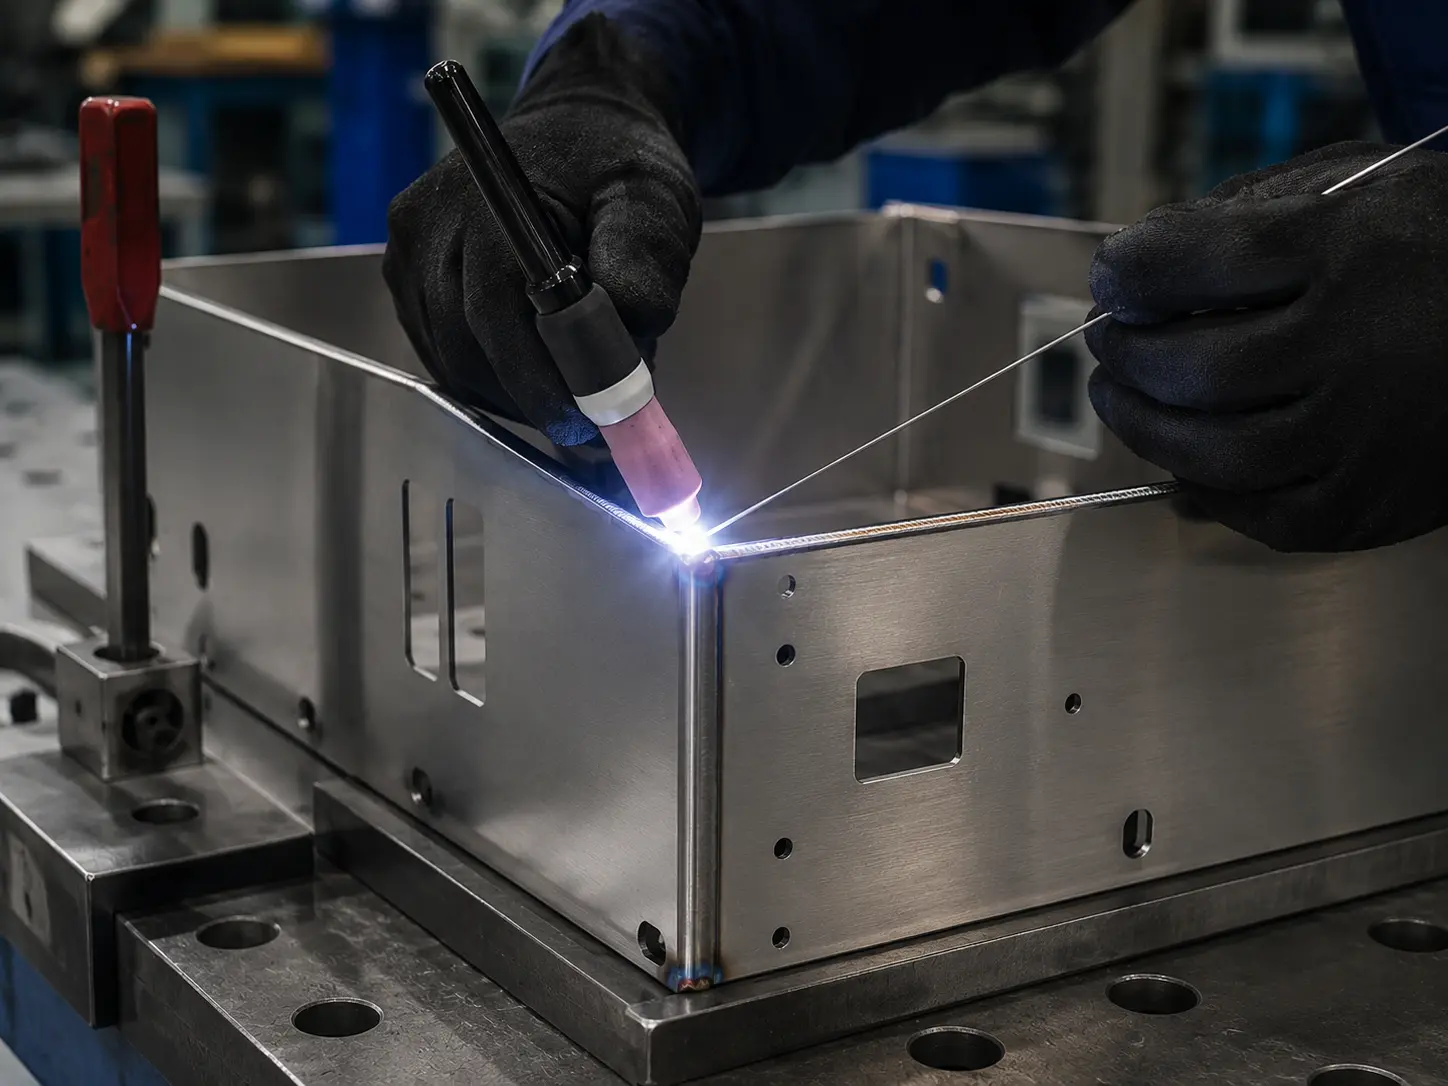
TIG Welding

Clean and precise welding for stainless steel, aluminum, and thin sheet metal. Ideal for appearance-critical components.
Thin Sheet Clean Welds Edelstahl
MIG CO2 Welding

MIG / CO2 Schweißen

Efficient welding for carbon steel frames, cabinets, brackets, and structural assemblies. Suitable for batch production.
Kohlenstoffstahl Rahmen Batch Production
Laser Welding

Laser Welding

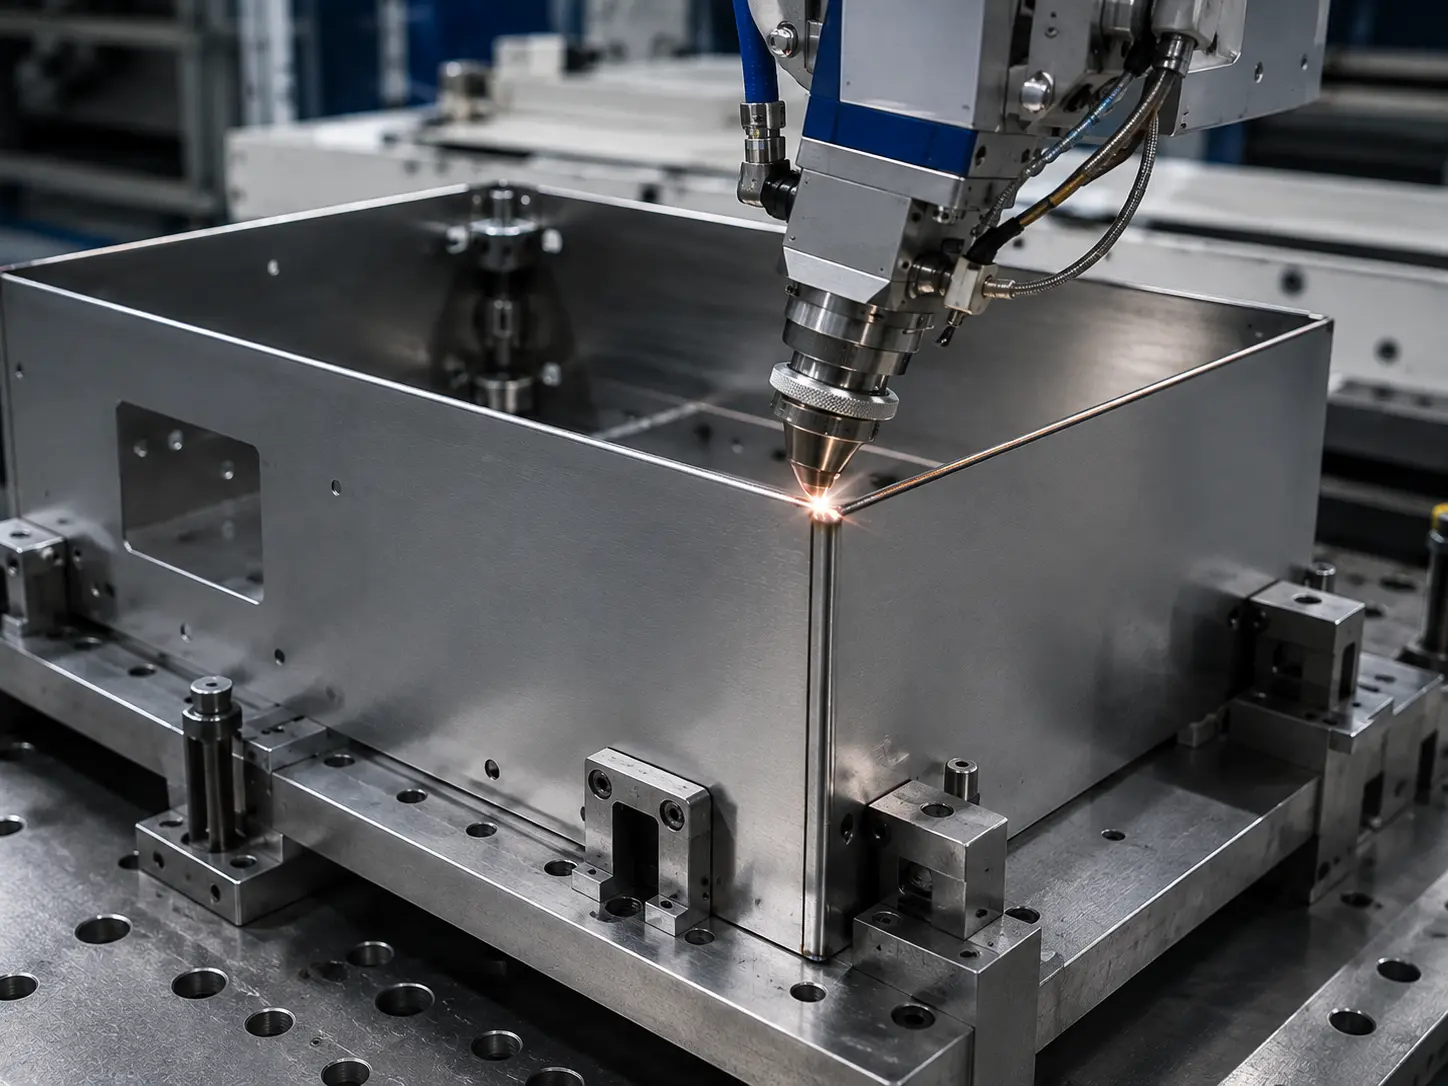
Low-distortion welding for precision housings, battery boxes, and thin sheet assemblies with narrow weld seams.
Low Distortion Precision Parts Narrow Welds
Spot Projection Welding

Spot / Projection Welding

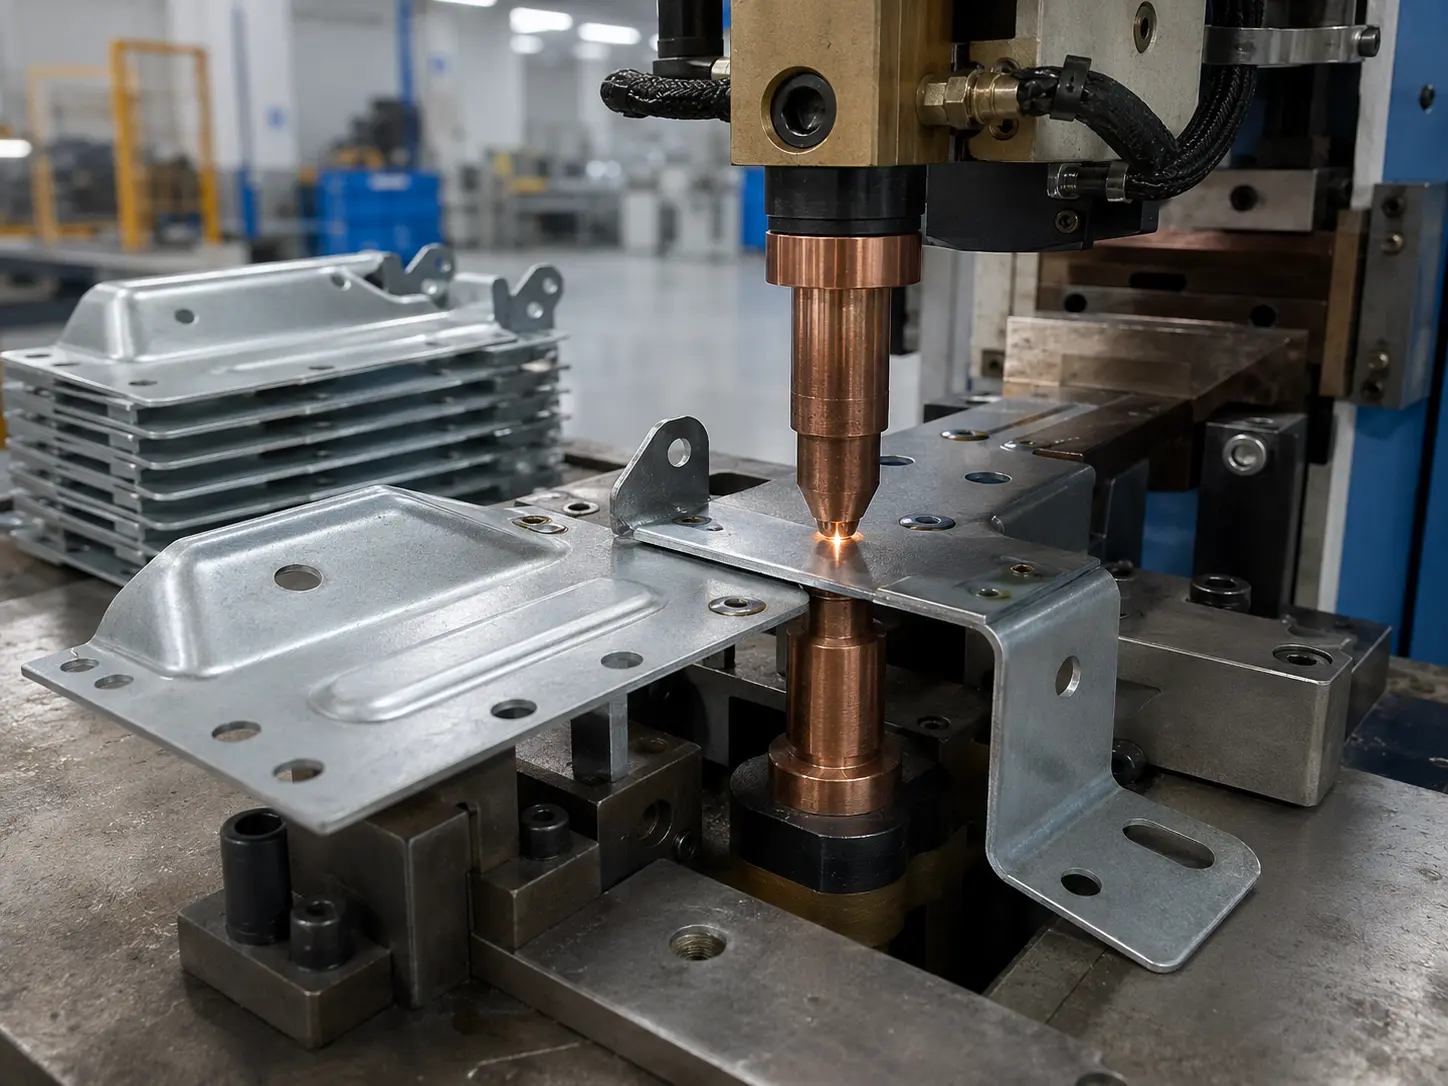
Fast joining for overlapping sheet metal parts, stiffeners, tabs, and brackets in high-efficiency production.

Lap Joints Stamped Parts High Efficiency

Not sure which welding process fits your part? Send your drawings and our engineers will recommend the right method.

Send Drawings for Welding Review →
TOLERANCES & STANDARDS

Sheet Metal Welding
Tolerances & Inspection Standards

SR MFG references ISO 13920:2023 and applies internal inspection controls for welded sheet metal parts. Tolerances are evaluated based on part size, welding method, fixture design, material thickness, and final assembly requirements.

Reference Standard ISO 13920:2023

+ SR MFG Internal Process Control

Sheet metal welding tolerance inspection
±0.8 mm Automated welding
linear tolerance ≤ 1 m
±1.5 mm Manual welding tolerance
for parts ≤ 1 m
≤ 1 mm/m Flatness / perpendicularity
control target
0–1.5 mm Typical weld reinforcement
control range
Tolerance Category Parameter Automated Welding Manual Welding Inspection Tools Applicable Process / Equipment
Linear
Abmessungen
Length/Width (≤ 1 m) ±0.8 mm ±1.5 mm Laser length measuring device / vernier caliper Robotic welding / CO₂ welding
(FANUC robot / Fenghuo welder)
Length/Width (1–3 m) ±1.2 mm ±2.5 mm Steel tape measure + feeler gauges Laser welding platform / Hanwang welder
Angular
Tolerance
Short side ≤ 500 mm ±15′ (0.25°) ±30′ (0.5°) Universal bevel protractor Automated fixturing system / general-purpose welding machine
Short side 500–1000 mm ±20′ (0.33°) ±45′ (0.75°) Angle gauge Positioner / Jasicfeng welder
Form
Tolerance
Flatness (per meter) ≤ 1 mm ≤ 2 mm Optical level Robotic welding workstation
Straightness (per meter) ≤ 0.8 mm ≤ 1.5 mm Tensioned wire + dial indicator Manual welding platform
Positional
Tolerance
Parallelism ≤ 1 mm/m ≤ 2 mm/m Granite surface plate + dial test indicator Laser tracking system
Perpendicularity ≤ 1 mm/m ≤ 2 mm/m Try square + feeler gauges Welding fixtures and tooling
Weld
Quality
Reinforcement (butt joint) 0–1.2 mm 0–1.5 mm Weld gauge All welding equipment
Reinforcement (fillet joint) 0–1.5 mm 0–2.0 mm Weld gauge All welding equipment
Undercut depth ≤ 0.2 mm ≤ 0.5 mm Depth caliper All welding equipment
Porosity allowance None (critical welds) ≤ 1 pore per 100 mm
(Ø ≤ 0.5 mm)
X-ray radiographic testing / dye penetrant inspection All welding equipment
i Final tolerances depend on drawing requirements, material thickness, weld length, fixture design, part structure, and inspection method.

WELDING MATERIALS

Metal Welding Materials

SR MFG supports welding for carbon steel, stainless steel, galvanized steel,aluminum, copper, titanium, magnesium, and high-strength steels. Our engineersmatch the right welding processes and quality controls to each material’scharacteristics-delivering strong, consistent results you can trust.

A. Carbon Steel / Low-Alloy Steel

Common grades:

Q235, SS400, A36

Weldability:

★★★★★

Recommended processes:

MIG/MAG, CO₂ welding, SMAW

Key considerations:

Excellent weldability; remove rust and oil before welding; control distortion in large frames.

Typical applications:

Frames, brackets, cabinets, structural parts

B. Stainless Steel

Common grades:

304, 316, 301, 201, 430

Weldability:

★★★★

Recommended processes:

TIG welding, laser welding, MIG welding

Key considerations:

Control heat input and maintain clean shielding to protect appearance and corrosion resistance.

Typical applications:

Enclosures, food equipment, appearance parts

C. Galvanized Steel Sheet

Common grades:

SGCC, DX51D+Z

Weldability:

★★★☆☆

Recommended processes:

MIG welding, spot welding

Key considerations:

Zinc coating can generate fumes and porosity; local zinc removal or ventilation is recommended.

Typical applications:

Outdoor cabinets, chassis components, sheet metal panels

D. Aluminum and Aluminum Alloys

Common grades:

1060, 1100, 3003, 5052, 6061

Weldability:

★★★☆☆

Recommended processes:

TIG welding, aluminum MIG welding

Key considerations:

High thermal conductivity and distortion tendency; requires dedicated filler wire, argon shielding, and precise heat control.

Typical applications:

Lightweight enclosures, aerospace parts, aluminum housings

Special Materials

Mg
Magnesium Alloys

Process review recommended

+

Highly reactive material. Welding process, shielding, and safety controls should be reviewed case by case.

Ti
Titanium and Titanium Alloys

Process review recommended

+
Cu
Copper and Copper Alloys

Process review recommended

+
HS
High-Strength Steels

Process review recommended

+

Preheating, low-hydrogen consumables, and post-weld heat treatment may be required depending on strength grade and thickness.

Need more material selection details?

Explore SR MFG’s material library for sheet metal grades, properties, processing notes, and application guidance.

Explore the material library of SR MFG →

Are you ready to get started on your metal fabrication project?

Not sure which material is ideal for your project? Feel free to contact us.Our engineering team will recommend suitable material grades and sheet thicknesses based on strength, weight, corrosion resistance and overall cost.

Industries & Metal Welding Applications

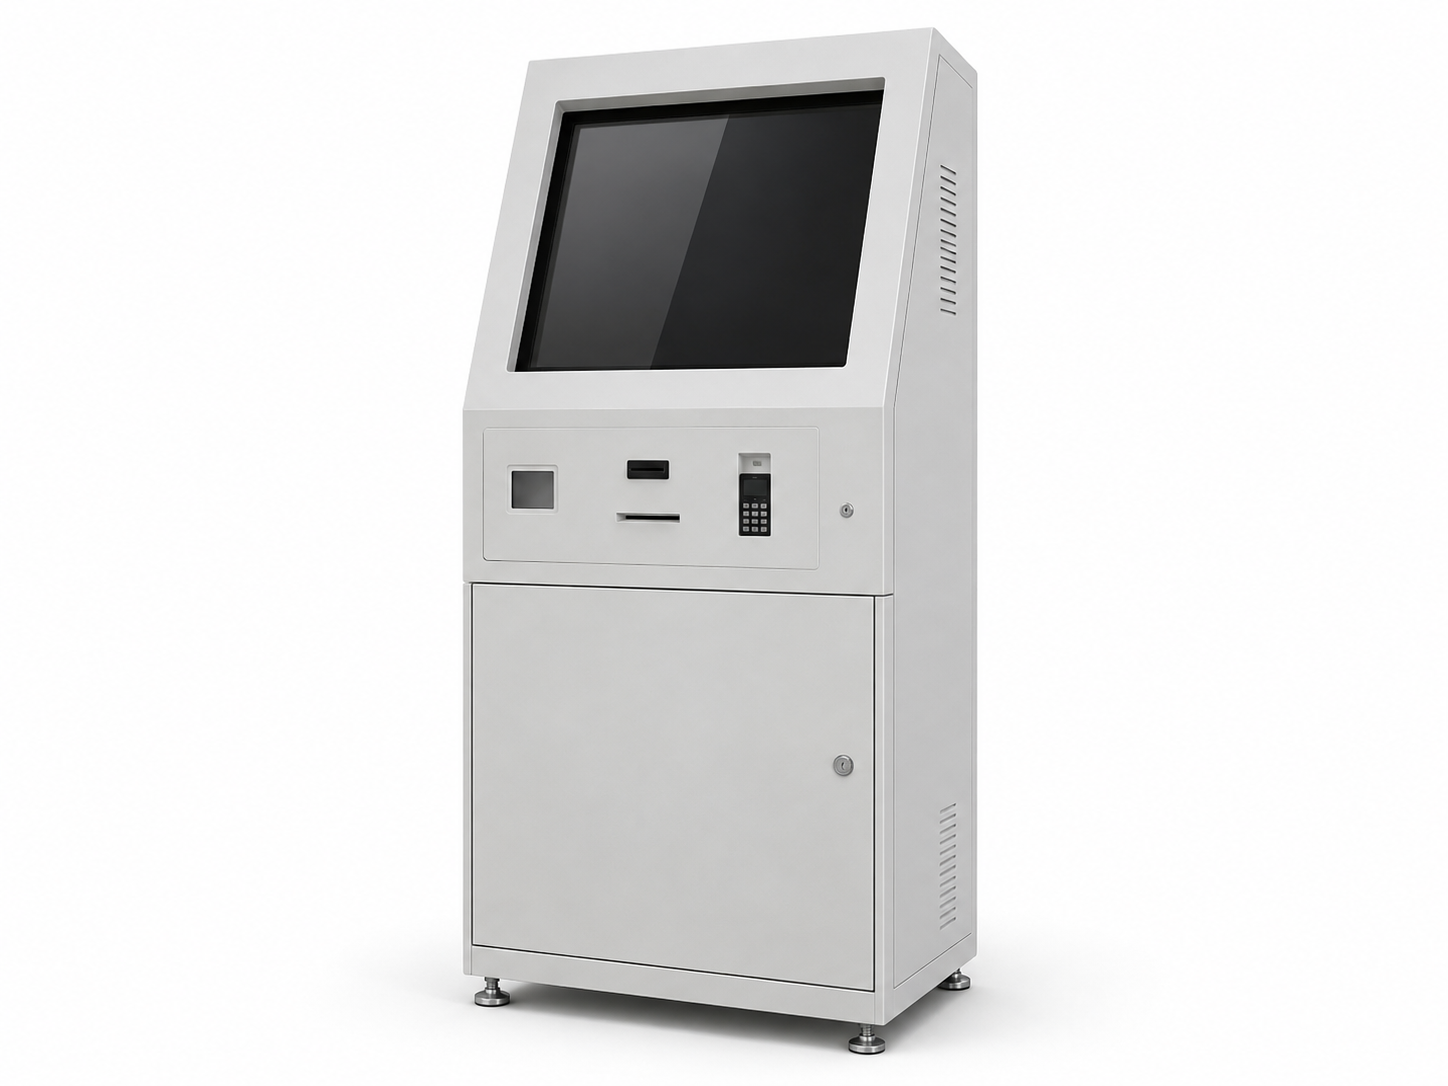
SR MFG provides metal welding services for sheet metal parts and fabricated assemblies used in data center equipment, consumer electronics, electrical systems, industrial equipment, new energy systems, and outdoor products. Metal welding helps join cut, bent, formed, or machined metal parts into stronger structures, enclosures, frames, brackets, and functional assemblies.

We support both prototype validation and stable batch production for welded metal parts that require structural strength, accurate alignment, clean weld appearance, controlled distortion, and reliable assembly performance.
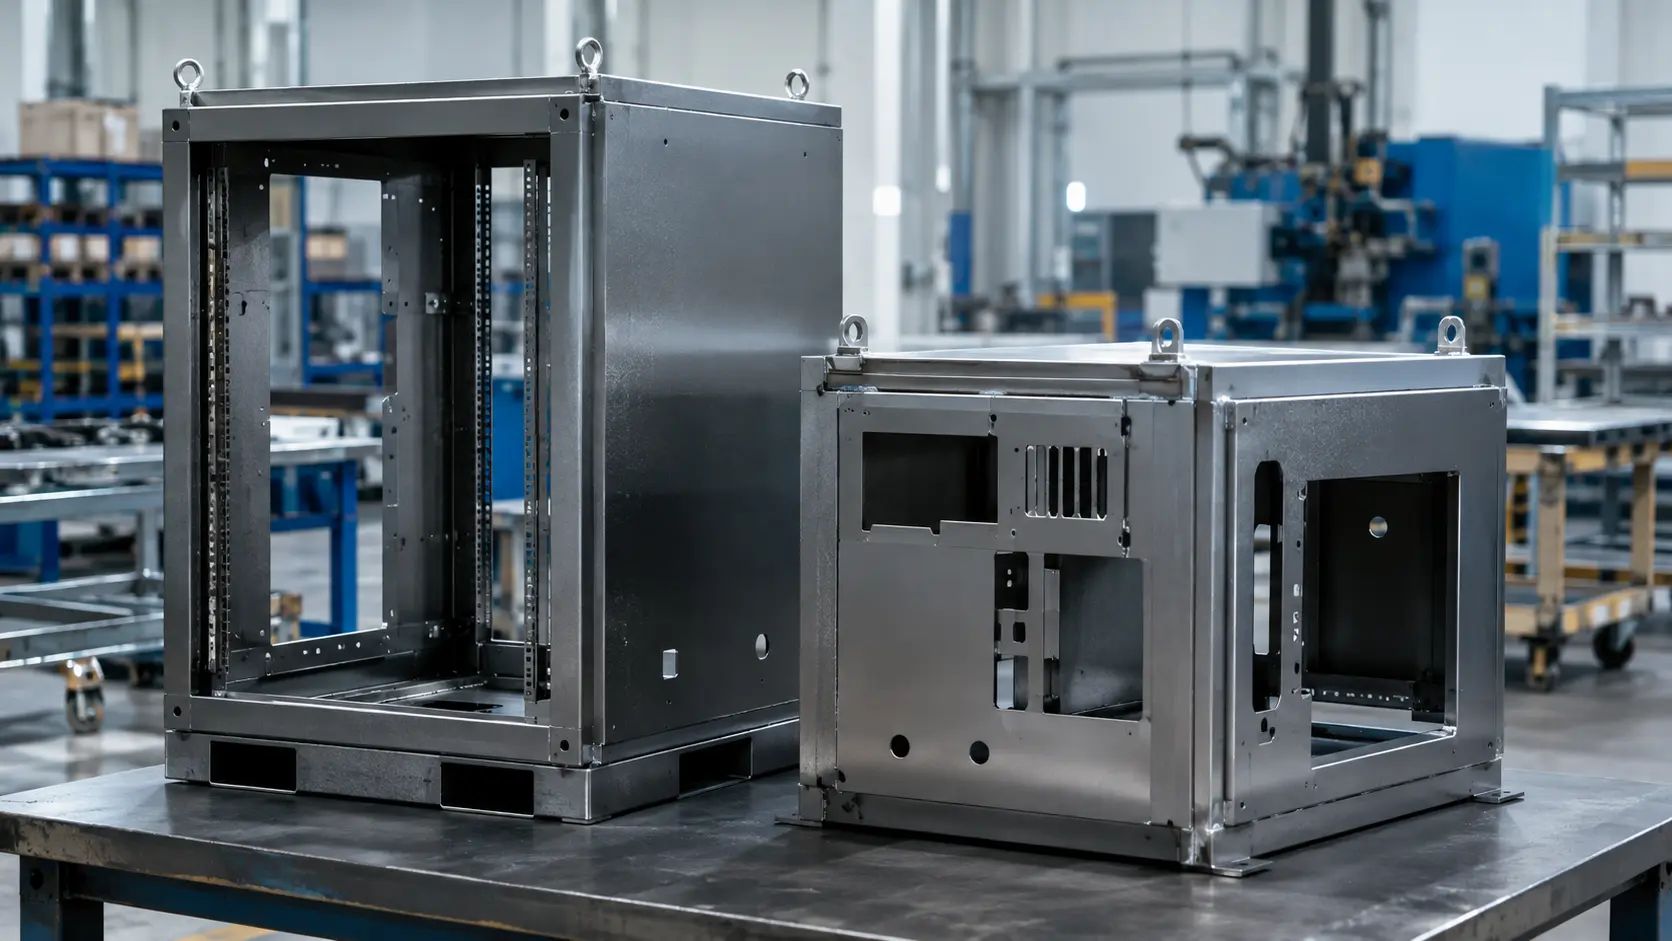
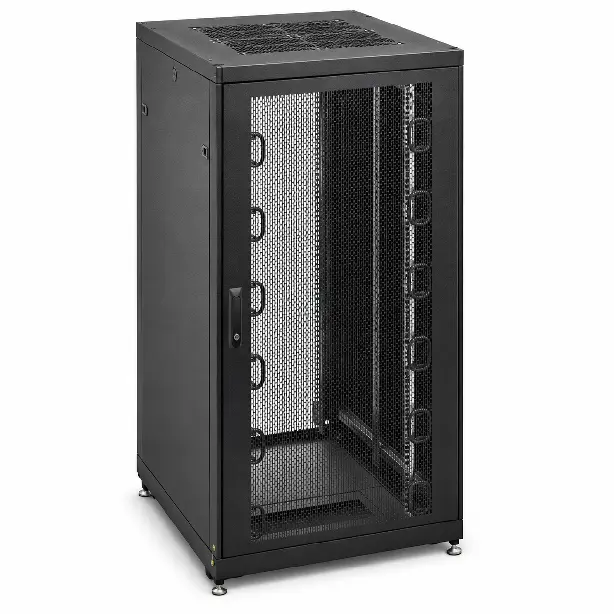
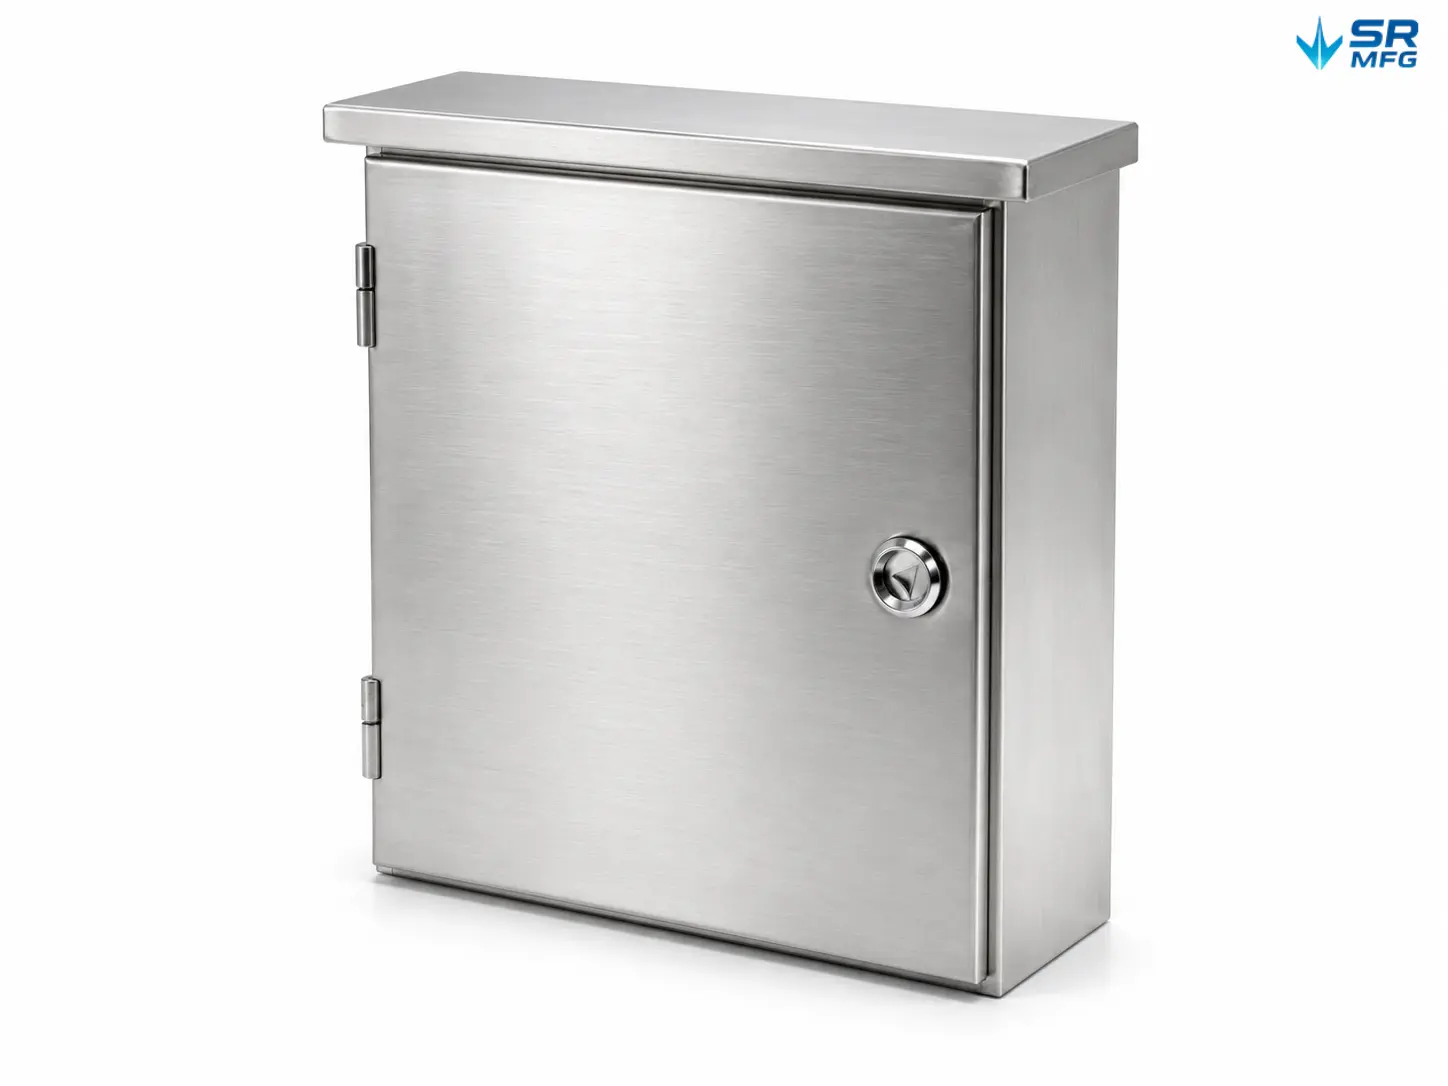
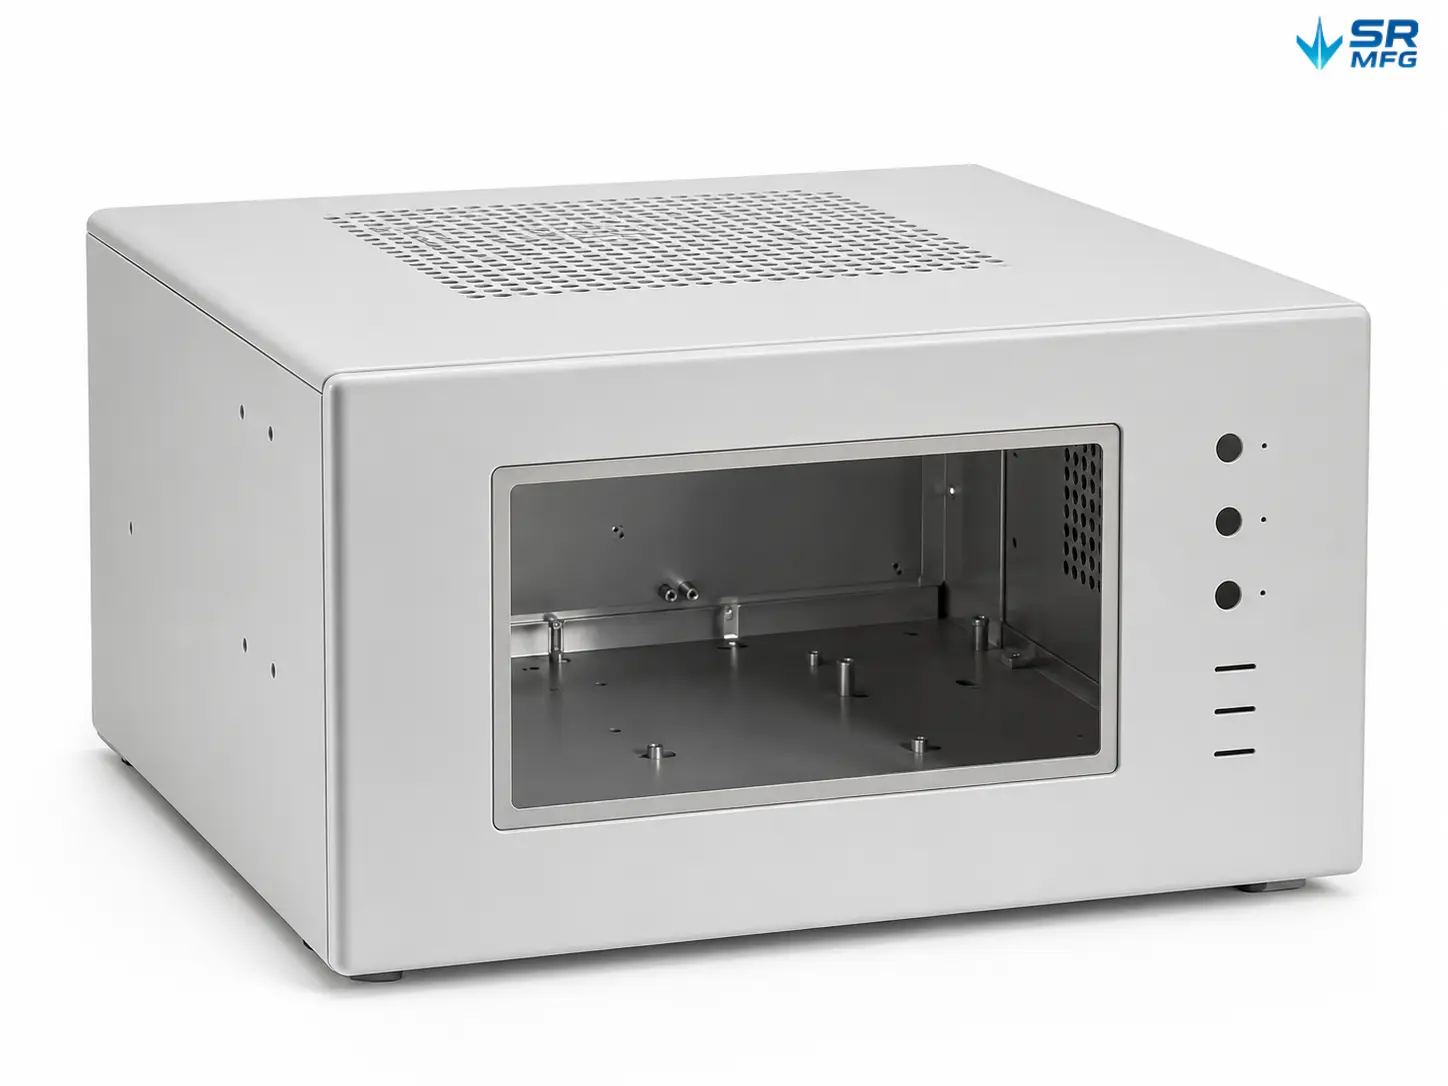
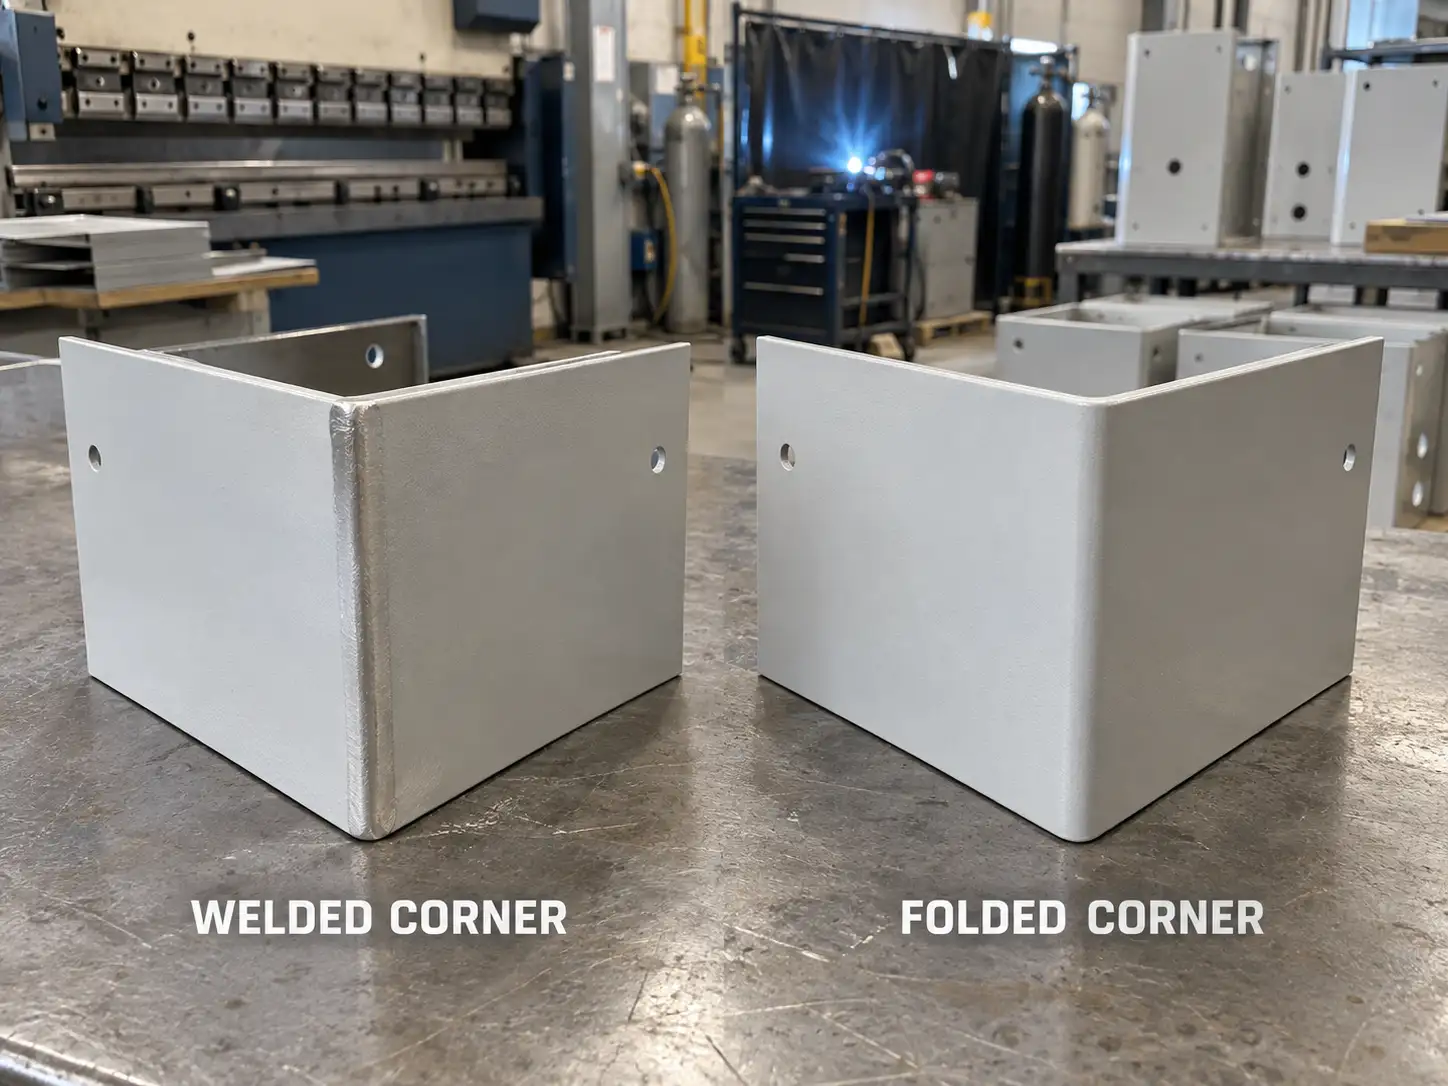
Welded sheet metal enclosure and fabricated assemblies for industrial applications

Data Centers & IT Equipment

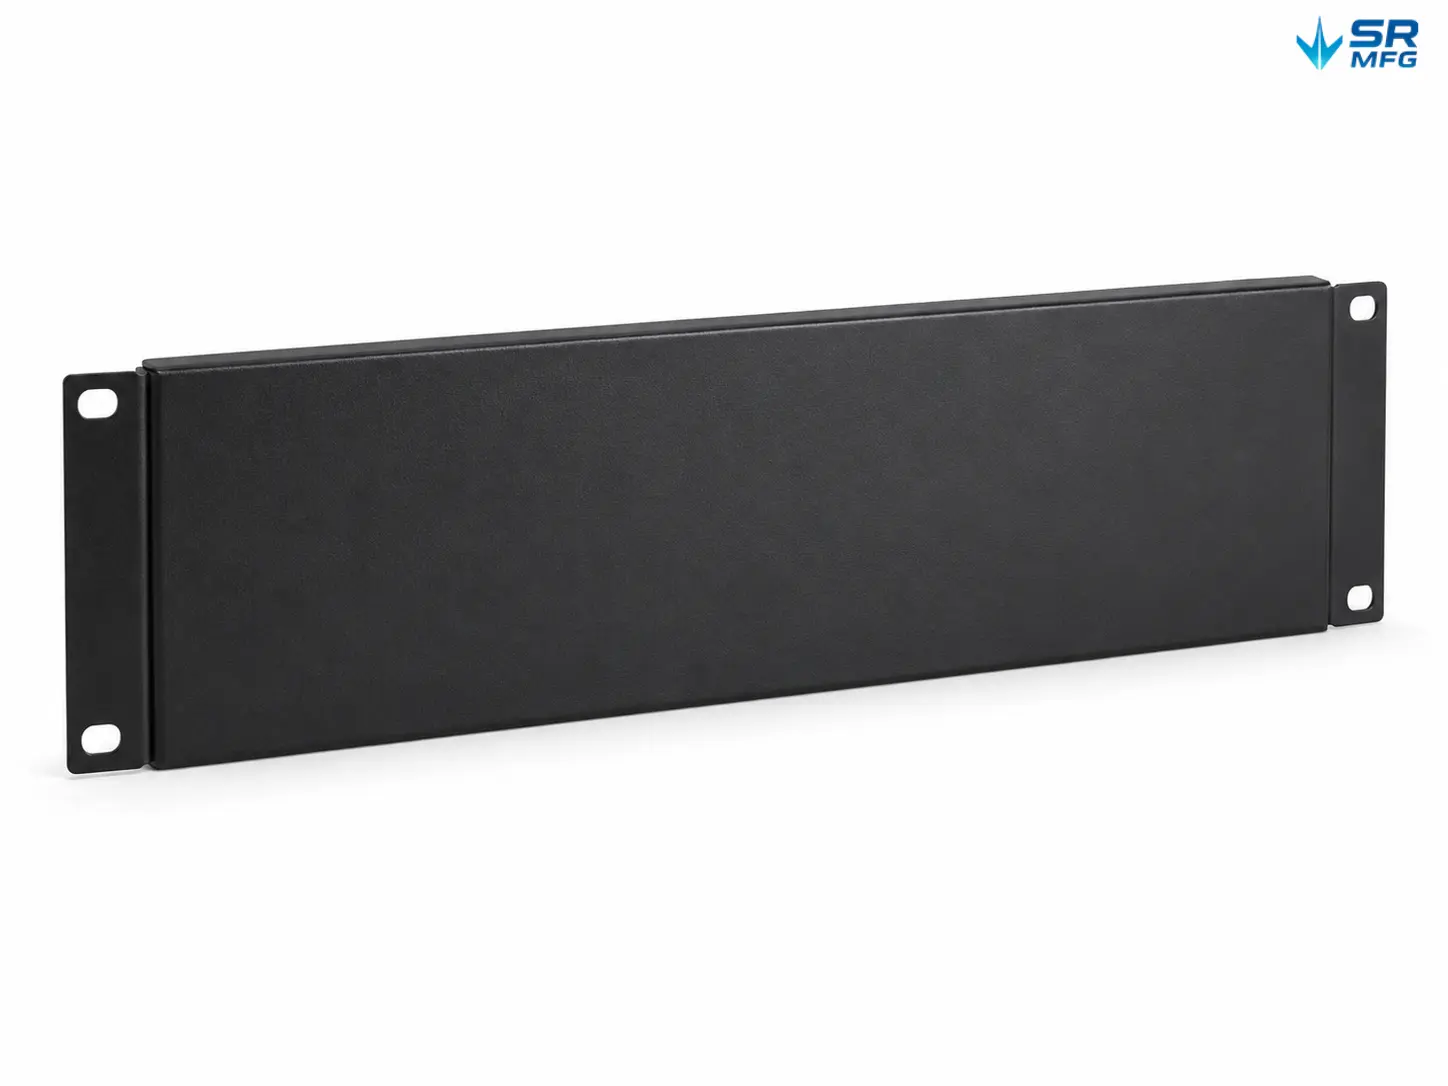
Metal welding for data center, network infrastructure, and IT hardware parts where stable frames, strong joints, and accurate installation features are required.

  • Server rack frames & rails
  • Cable management trays
  • Cabinet panels & doors
  • Mounting brackets & plates

Unterhaltungselektronik

Welding solutions for consumer electronics housings, internal brackets, display structures, and precision sheet metal assemblies that require clean joints and controlled appearance.

  • Device housings & covers
  • Internal support brackets
  • Display mounting structures
  • Speaker & audio metal parts
  • Small precision formed parts

Elektrische Geräte

Metal welding for electrical enclosures, control cabinets, power distribution units, and industrial electrical systems where structural stability, panel alignment, and durable joints are important.

  • Electrical cabinet enclosures
  • Control box panels
  • Terminal mounting plates
  • DIN rail brackets
  • Ventilation and access panels

Industrieausrüstung

Welding services for machinery, automation systems, production equipment, and structural machine assemblies that require strong connections and long-term durability.

  • Machine covers & guards
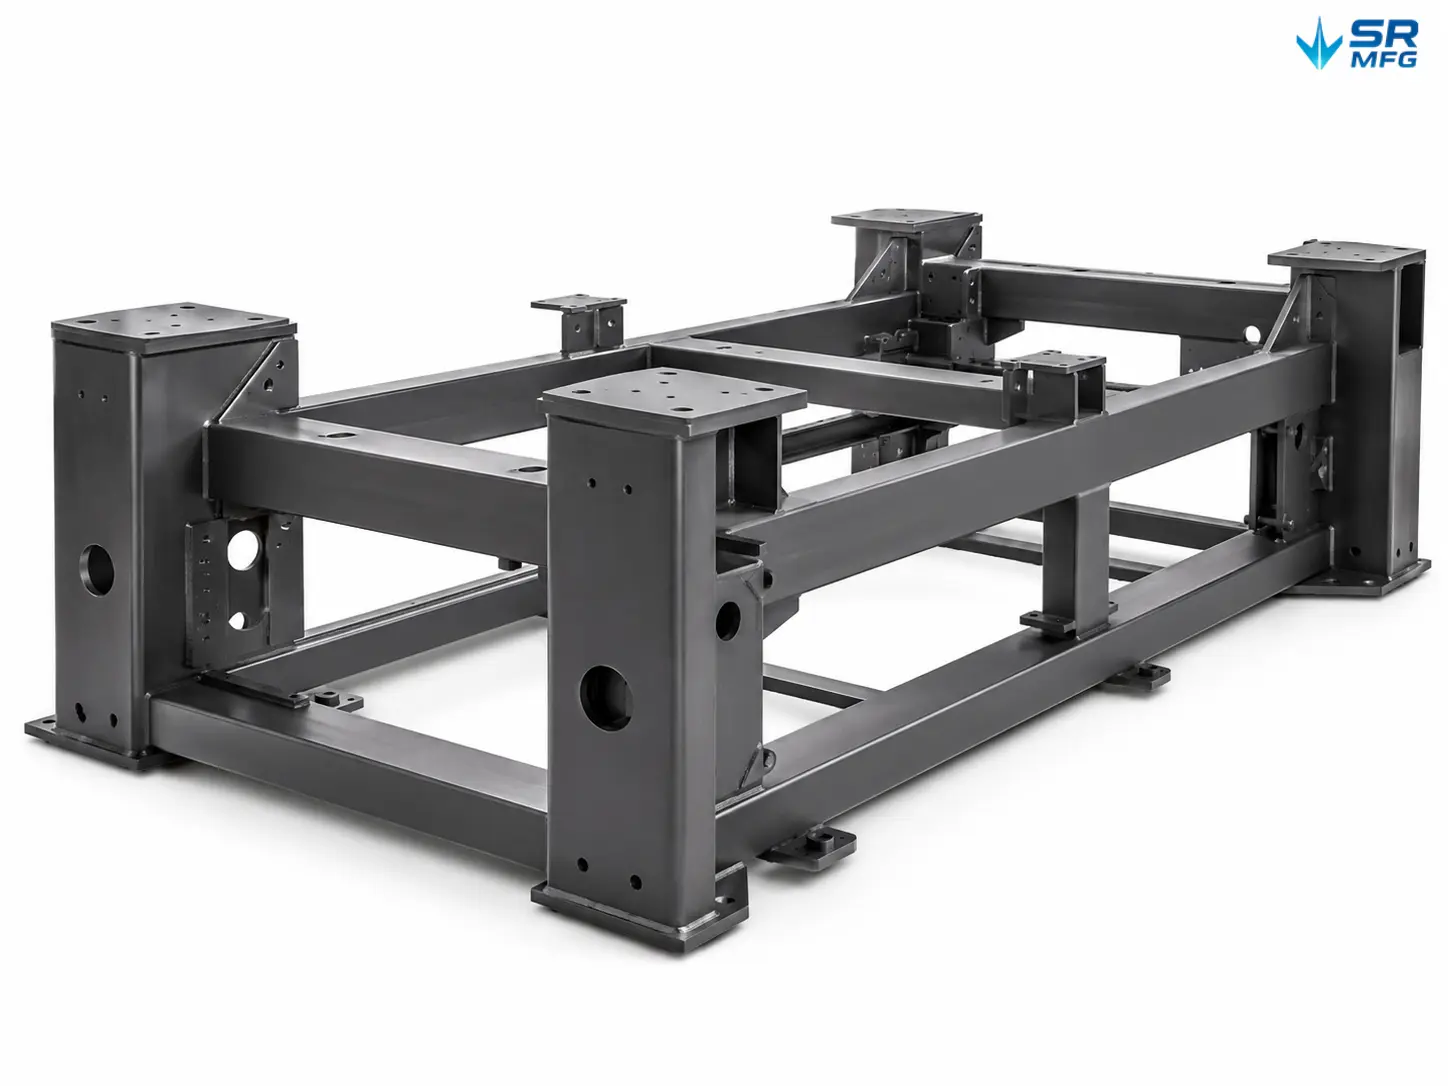
  • Equipment frames
  • Conveyor brackets
  • Sensor mounting plates
  • Protective panels & shields

New Energy Systems

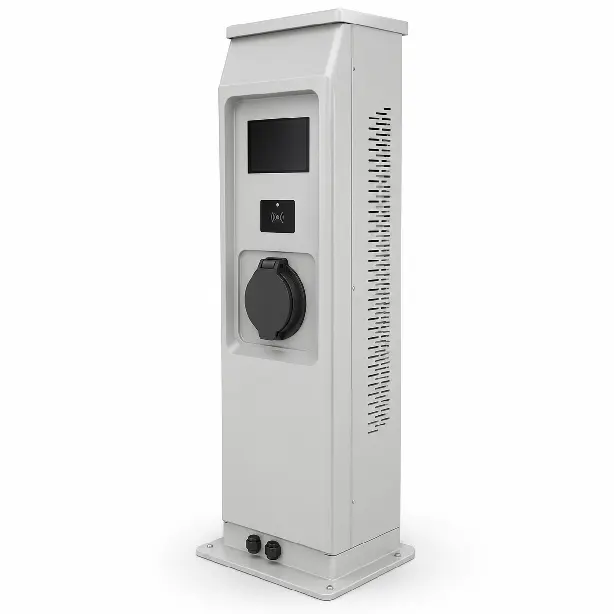
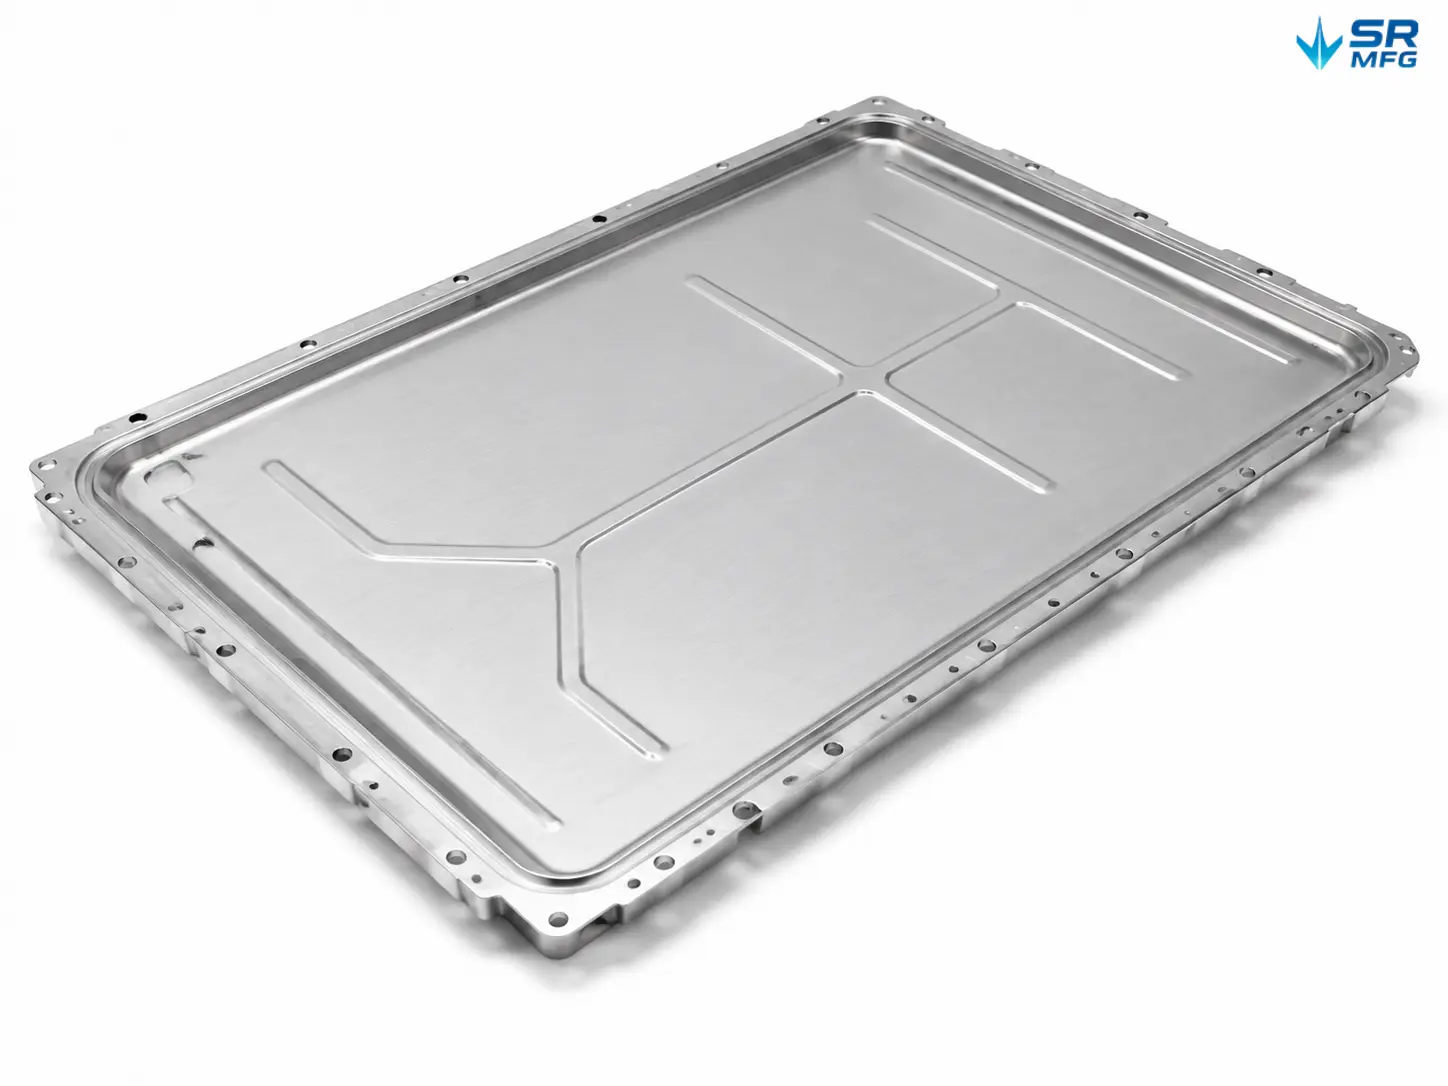
Metal welding for EV charging equipment, battery systems, energy storage cabinets, and power conversion units where enclosure strength, mounting stability, and assembly reliability are required.

  • Battery enclosure parts
  • Charging station cabinets
  • Energy storage cabinet panels
  • Busbar support brackets
  • Power module housings

Outdoor Equipment

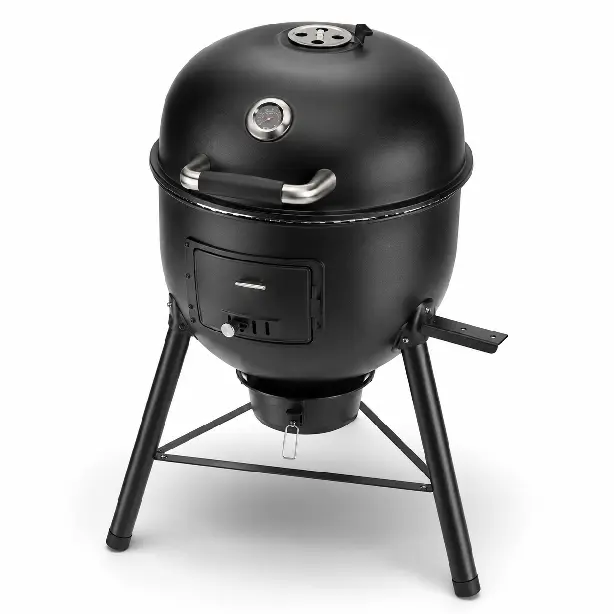
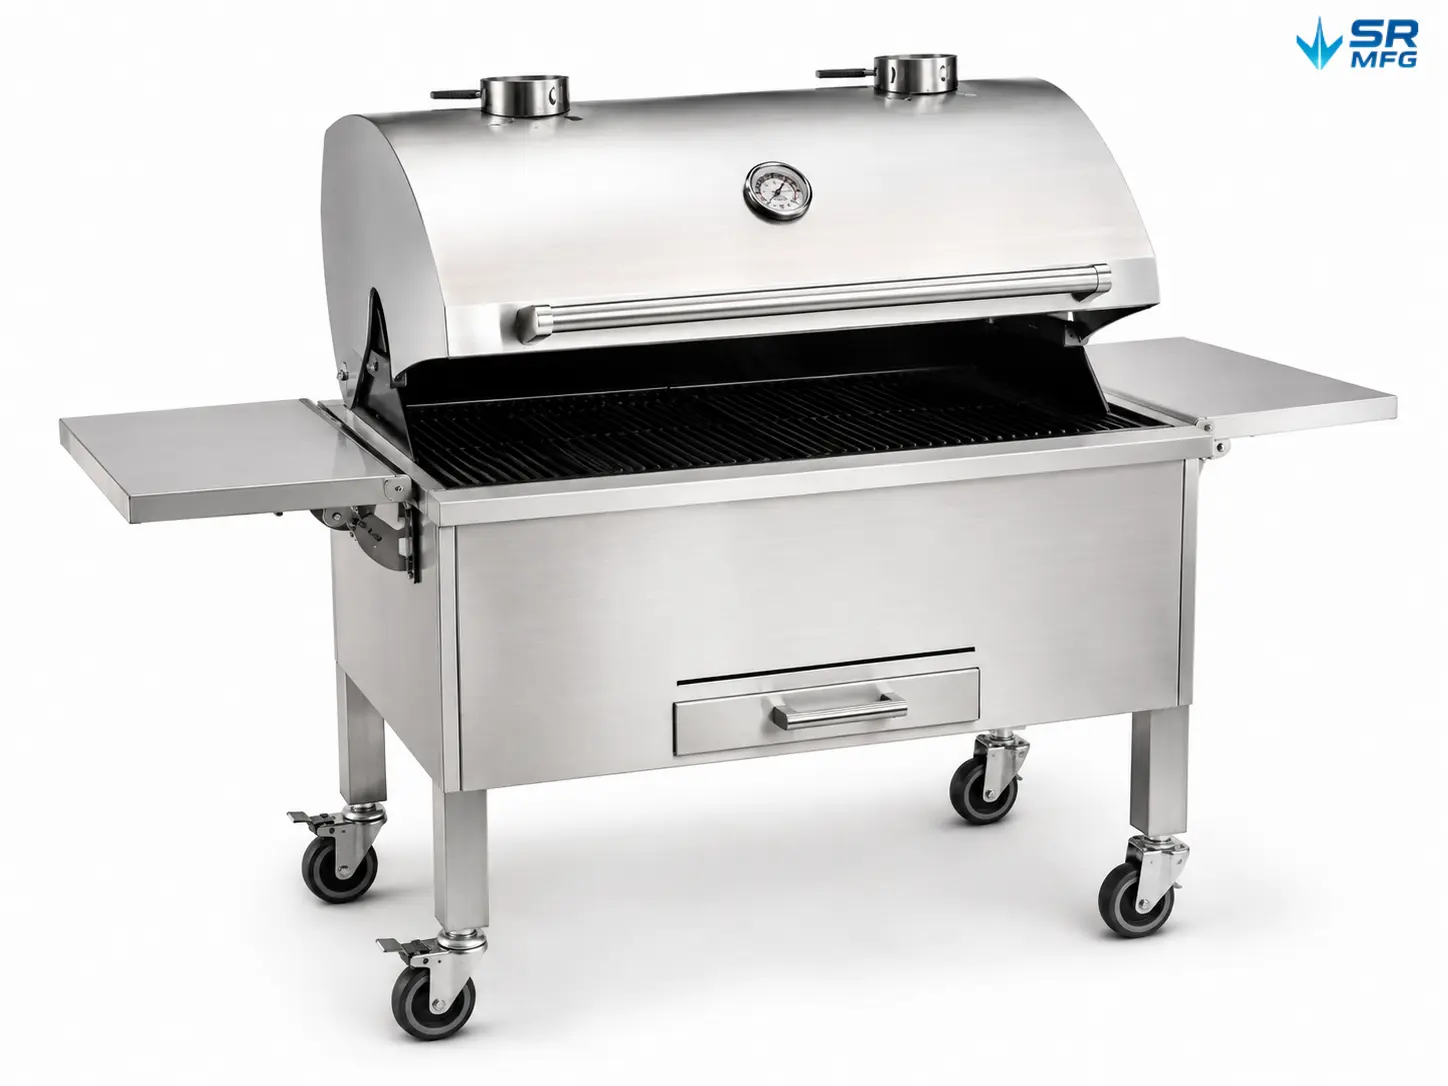
Welded metal parts for outdoor enclosures, equipment covers, BBQ grills, lighting systems, and structural fixtures exposed to real-use environments.

  • Outdoor equipment housings
  • BBQ grill sheet metal bodies
  • Protective covers & panels
  • Mounting brackets
  • Weather-resistant structural parts

Built for Your Application

Whether you need a single prototype or stable batch production, SR MFG provides reliable metal welding services to improve structural strength, assembly stability, joint quality, and final product durability.

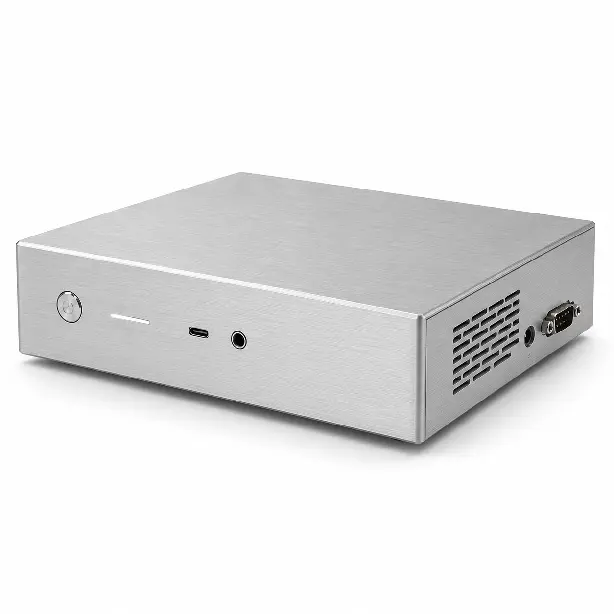
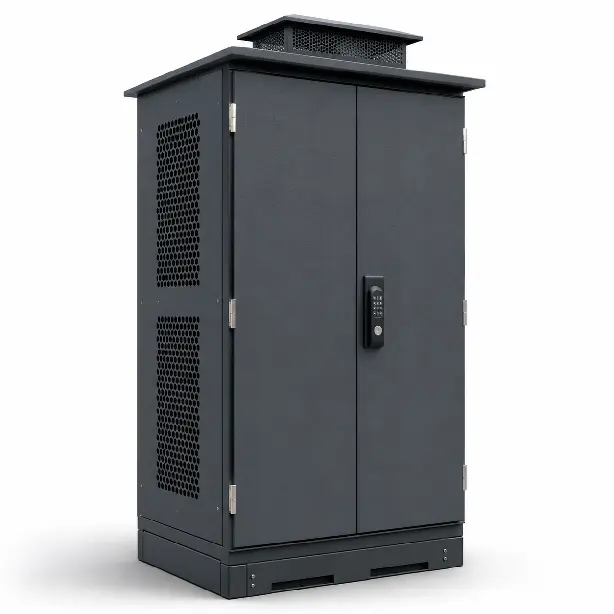
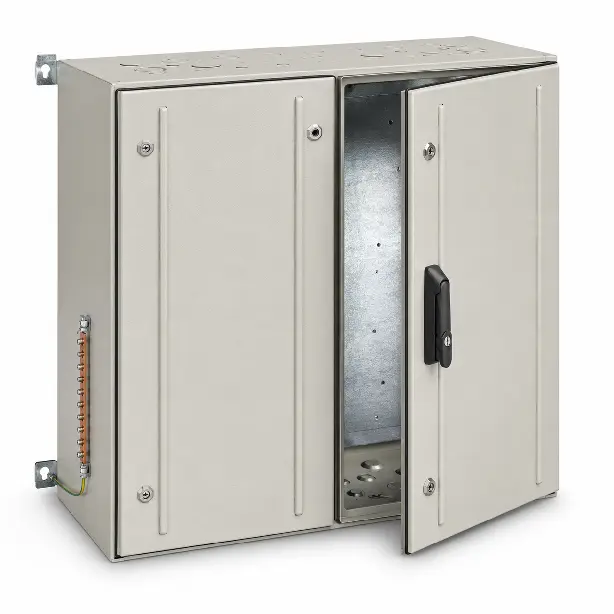
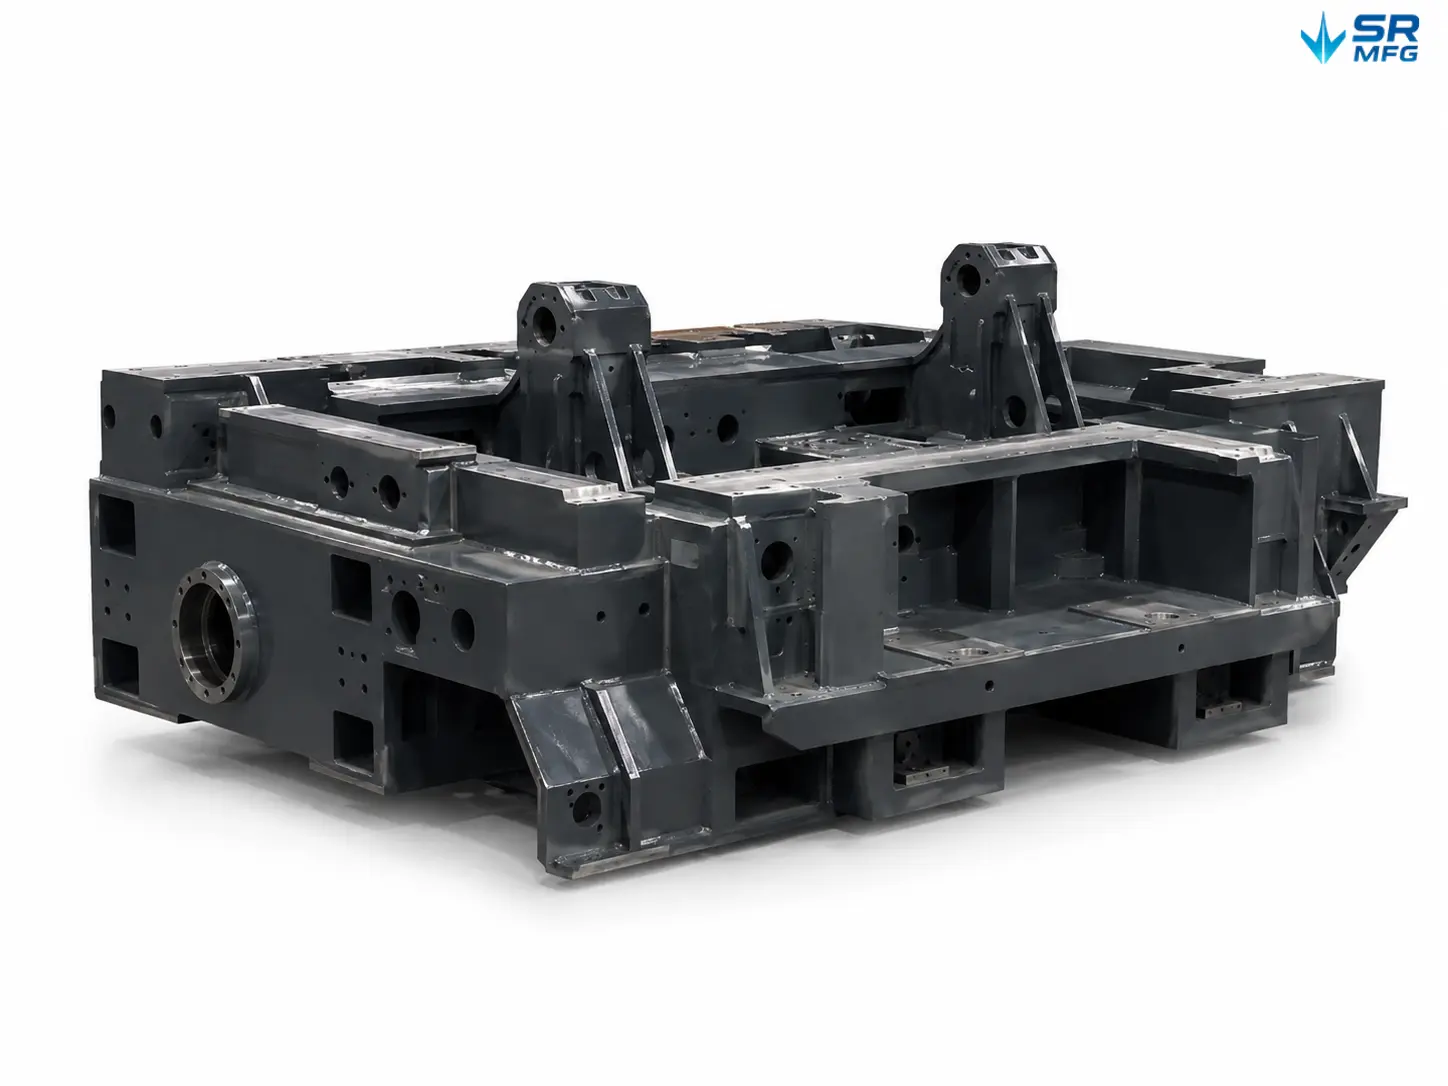
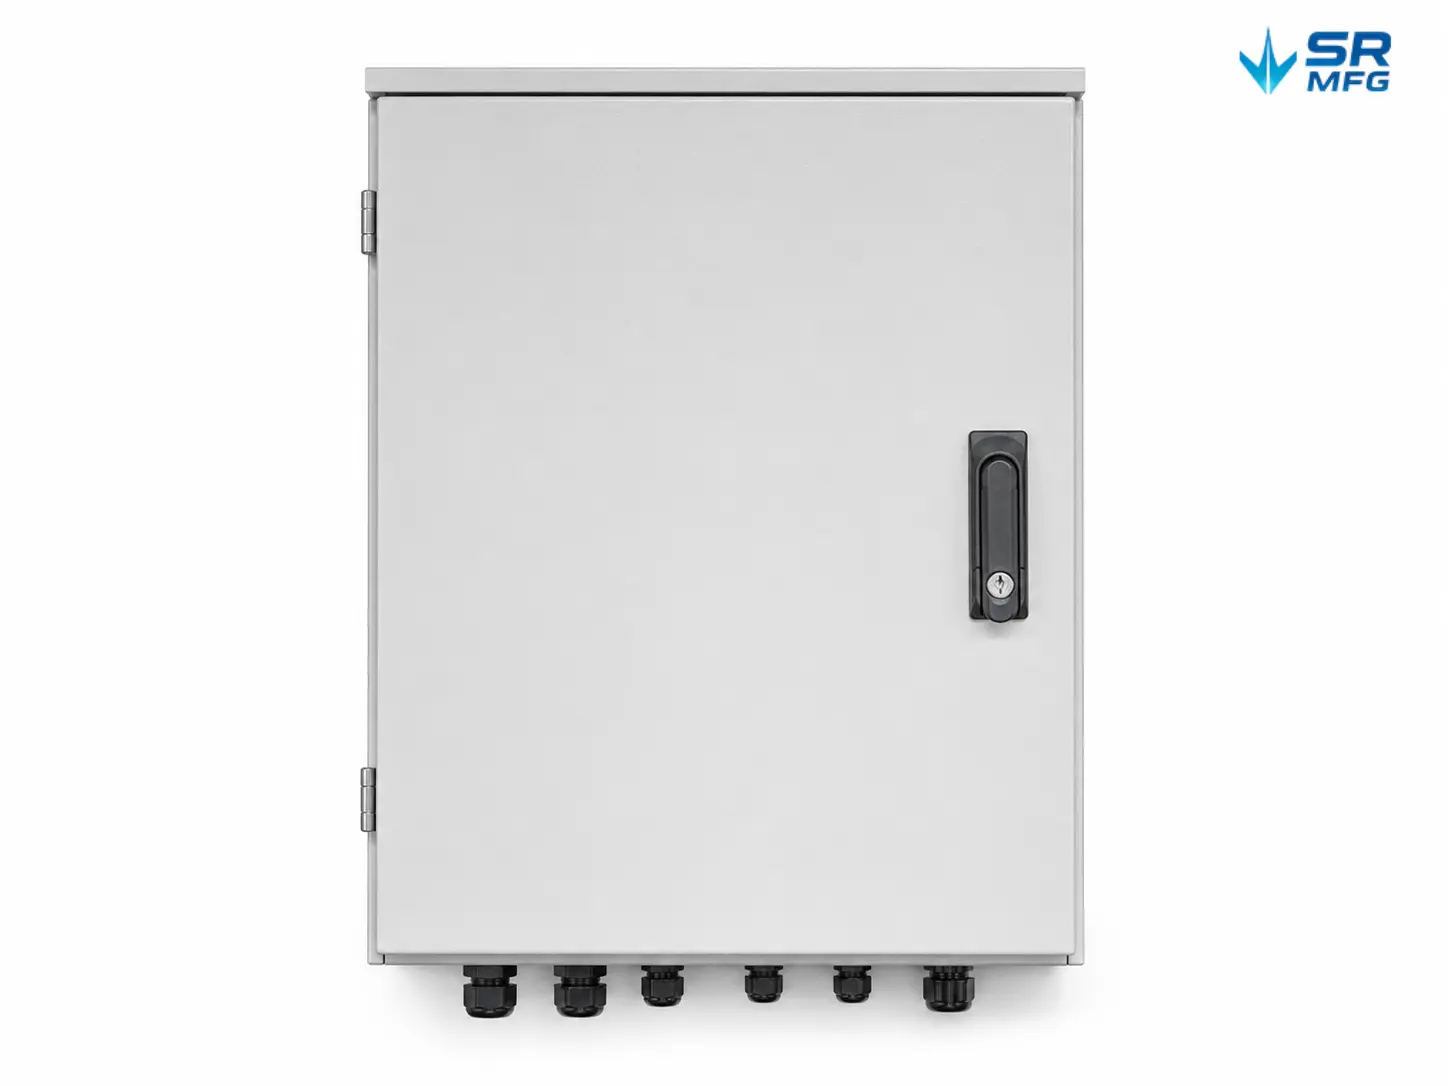
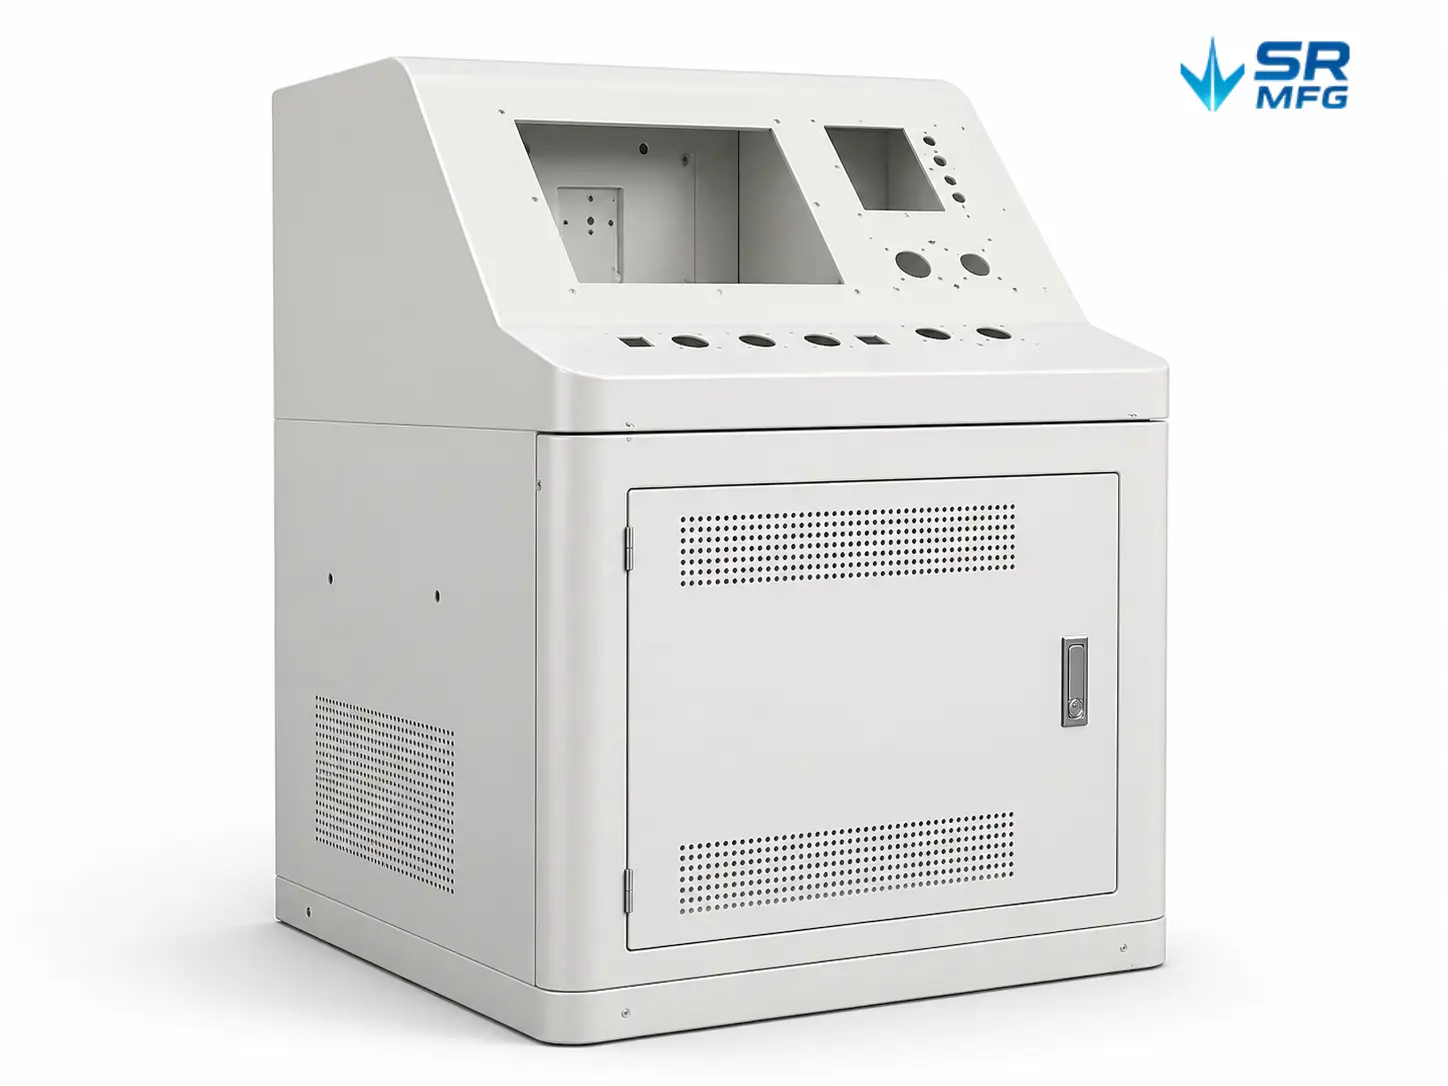
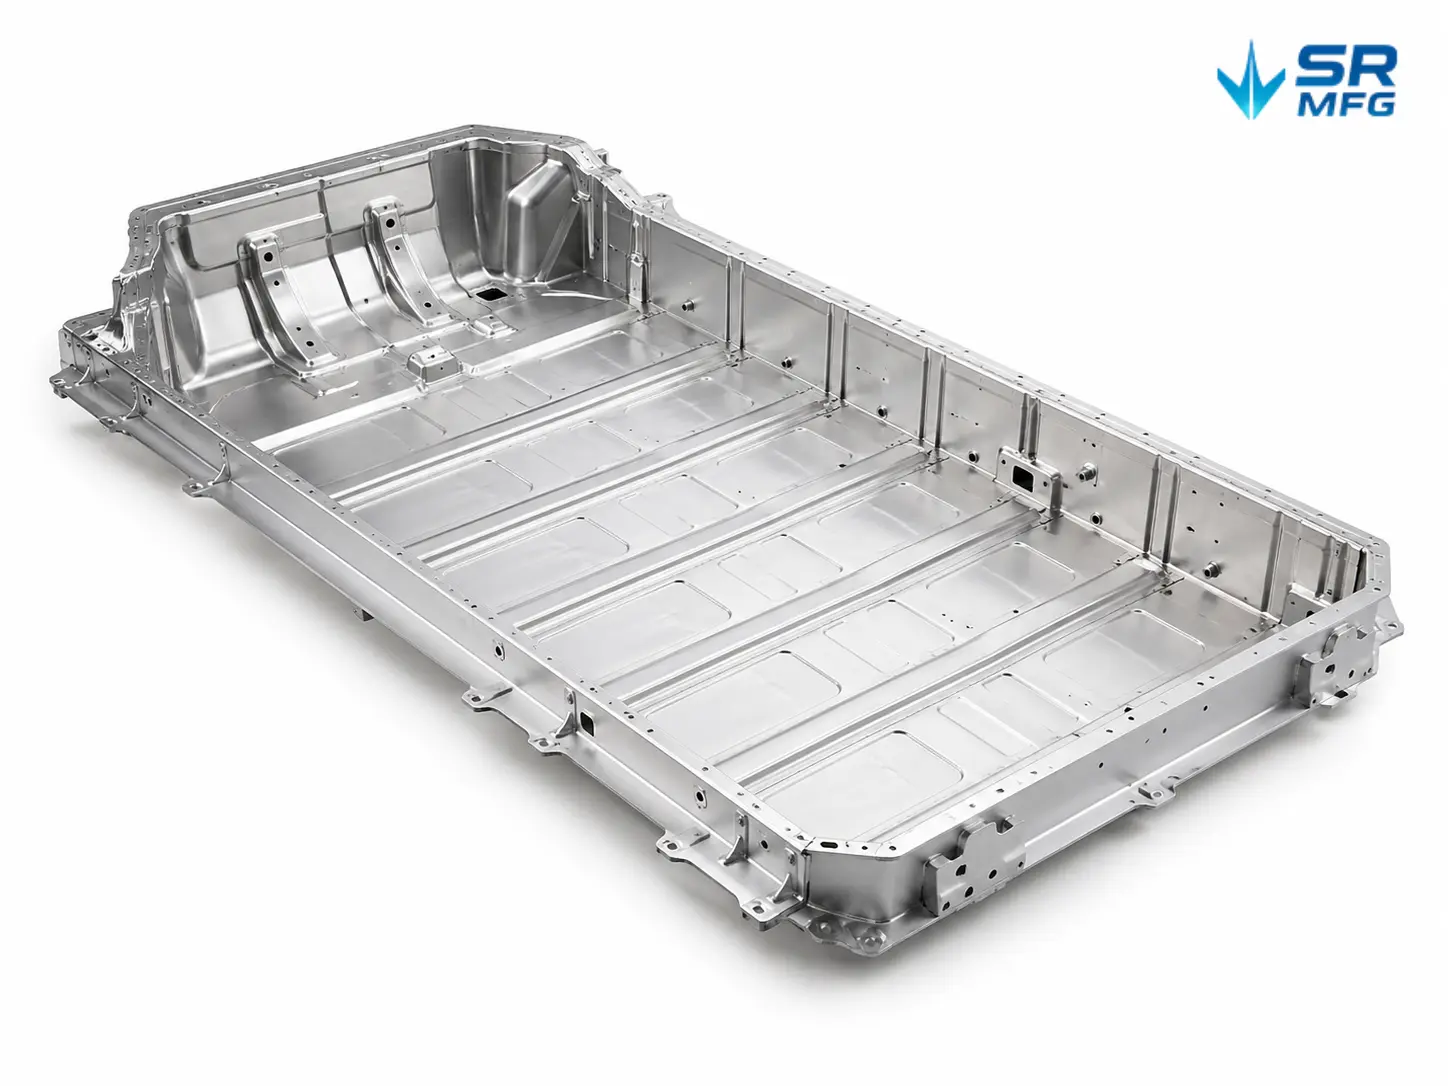
Sheet Metal Welding Products Designed and Manufactured by SR MFG

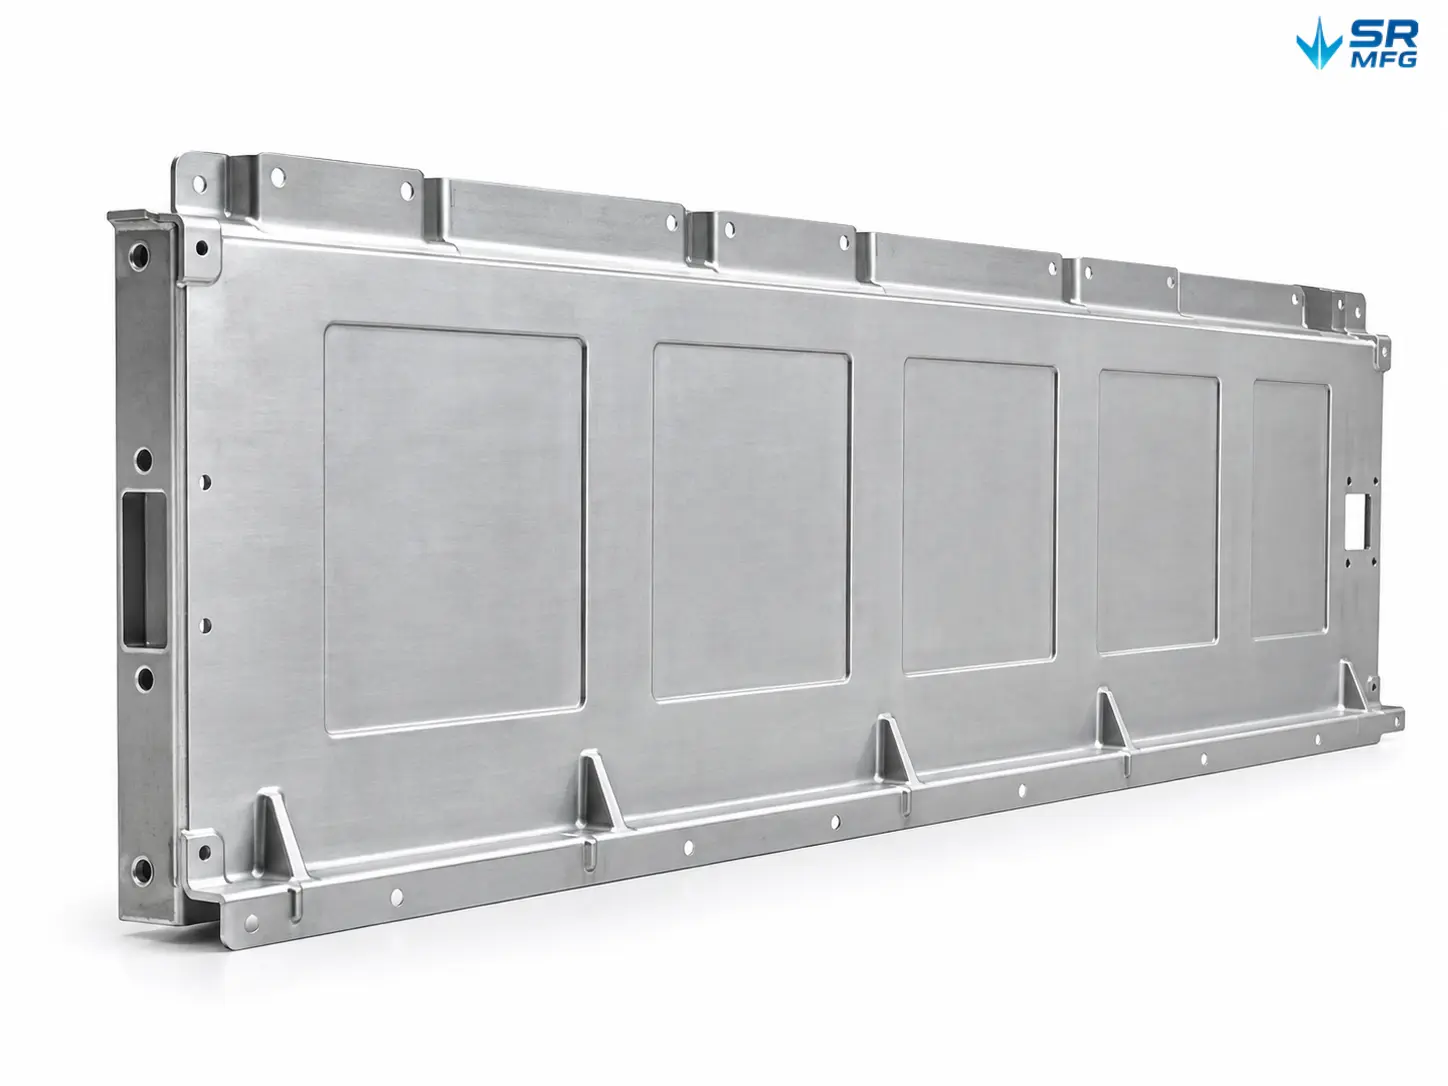
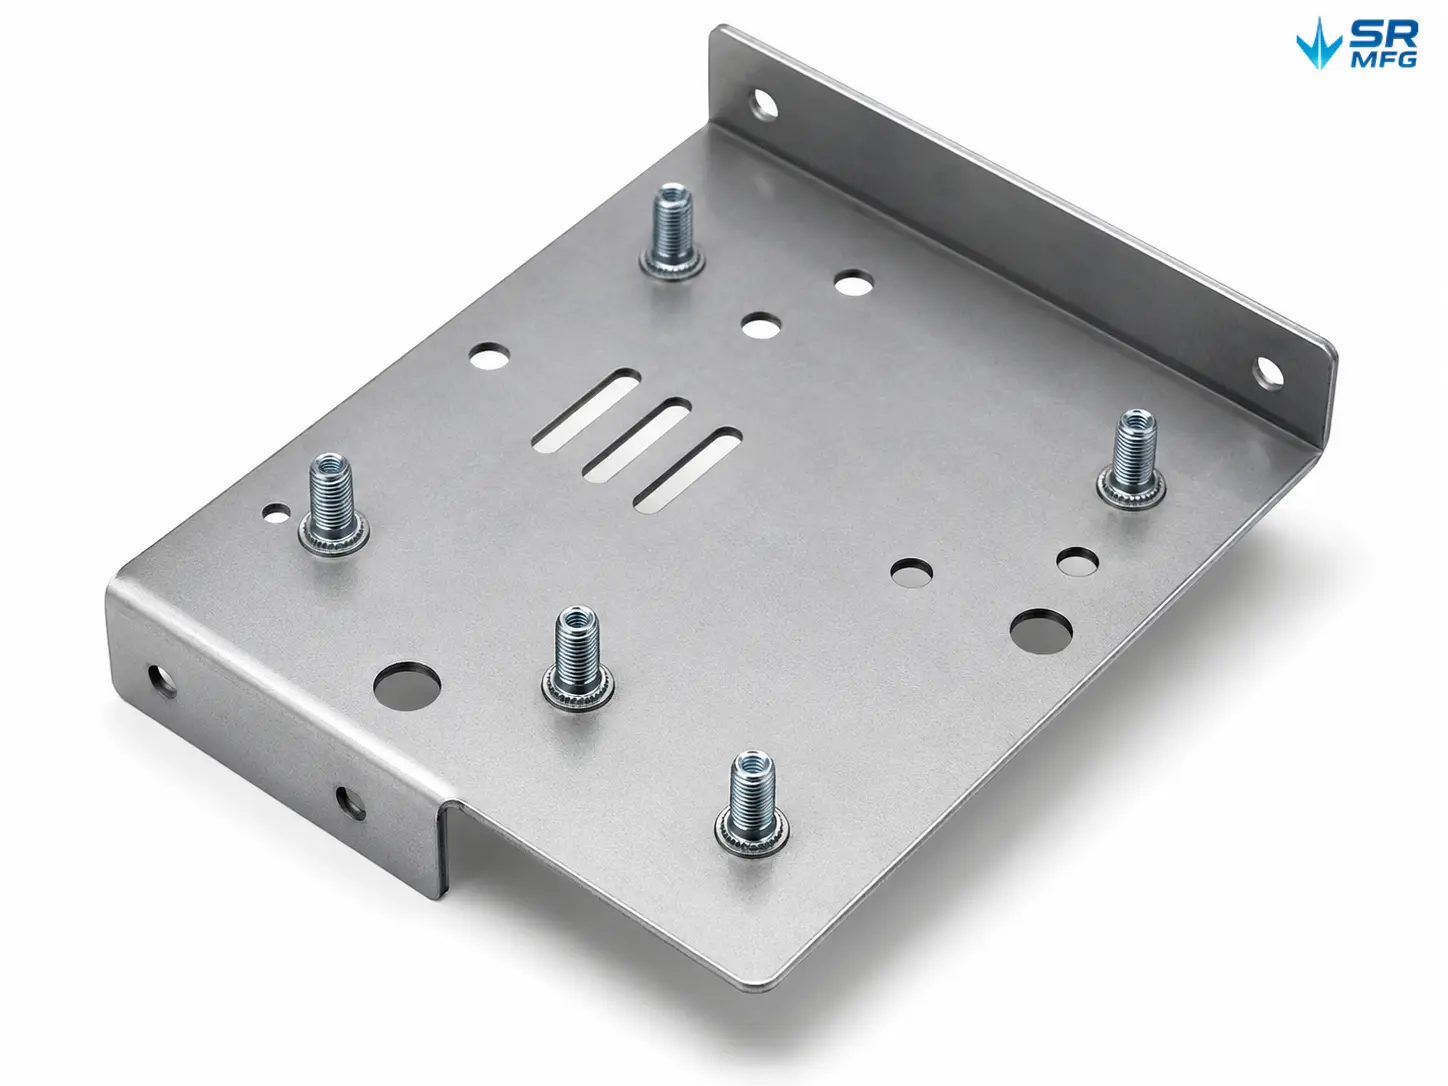
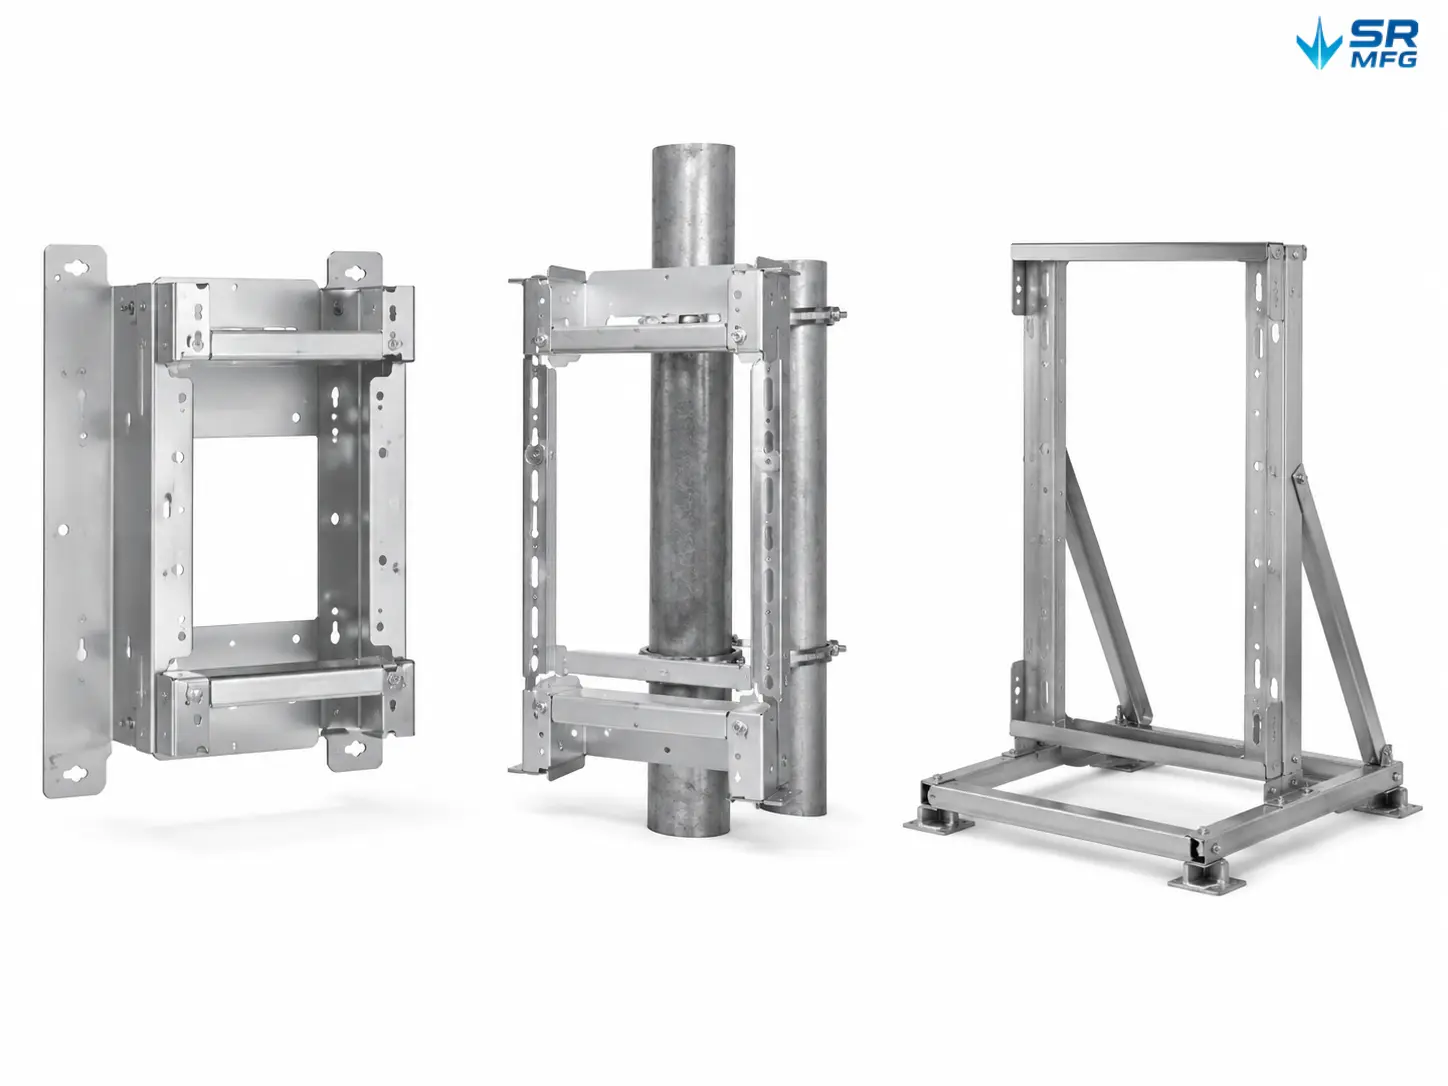
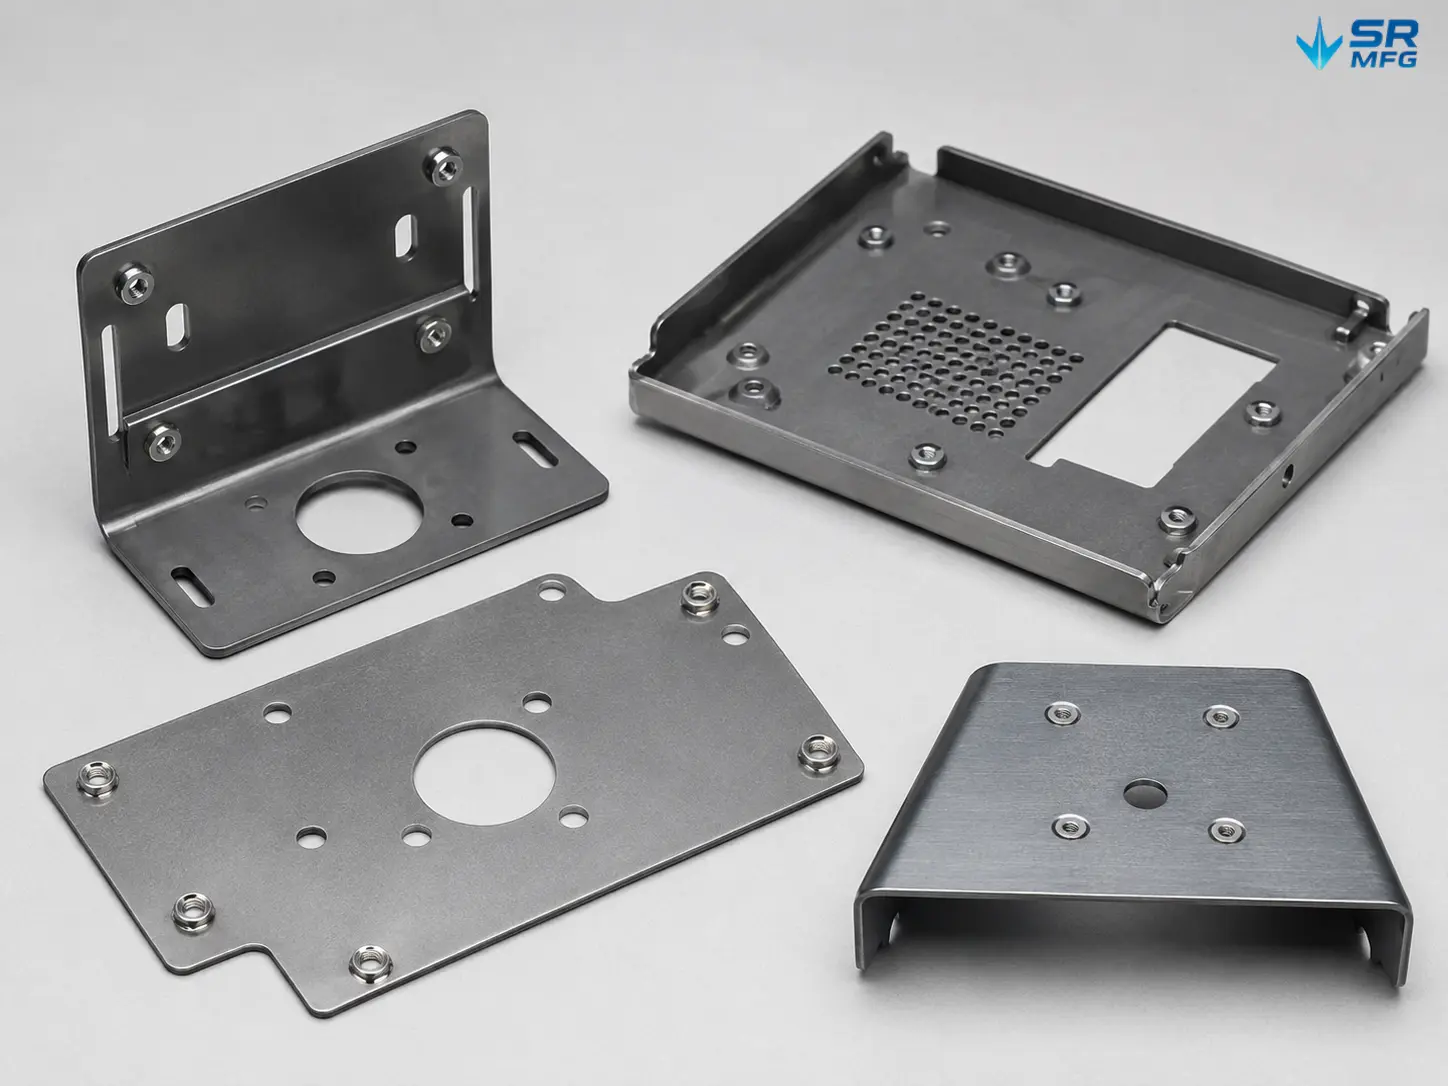
SR MFG has collaborated with global OEMs to co-design and manufacture a variety of custom sheet metal products, covering enclosures, chassis, panels, brackets, and structural components.

Häufig gestellte Fragen​ About Sheet Metal Welding

Welding distortion mainly results from uneven heat input and insufficient structural restraint. During continuous welding of thin sheet metal, localized temperature rise causes plastic deformation that cannot be fully recovered after cooling. In real production, distortion is rarely caused by a single factor; it is usually the combined effect of welding sequence, fixture positioning, and weld distribution. For this reason, distortion must be controlled during the process-planning stage rather than corrected afterward.

Inconsistent weld appearance is usually related to the welding parameter window, operational stability, and material surface condition. For example, insufficient surface cleanliness on stainless steel directly affects weld pool behavior. When parameters are not fully standardized, differences between operators or shifts can further amplify variation. As a result, appearance consistency depends more on parameter standardization and process control than on one-time manual adjustments.

Stable welding tolerances depend on whether post-weld dimensions are predictable. In batch production, this is typically achieved by locking in the welding sequence and fixture datums during first-article approval, then monitoring dimensional trends through in-process sampling. Compared with single-part inspection, this approach focuses more on overall drift ranges. At present, there is no widely recognized authoritative statistical data that quantitatively defines tolerance performance across different welded structures.

Yes, the differences are significant. Carbon steel is relatively tolerant of heat input and offers a wide welding window. Stainless steel has lower thermal conductivity, making it more prone to heat concentration and discoloration. Aluminum alloys, affected by oxide layers and high thermal conductivity, place higher demands on process stability. In sheet metal welding services, material differences directly determine the welding method, parameter range, and fixture design strategy.

During the prototype stage, production pace is slower and allows greater manual intervention, whereas batch production emphasizes efficiency and continuity. If welding sequences, fixture repeatability, or parameter documentation are not fully standardized, variations can quickly be amplified. Therefore, batch stability is not a natural extension of prototype capability; it must be deliberately established through process solidification and systematic production control.

Sheet Metal Welding Technical Resources

Go to Top