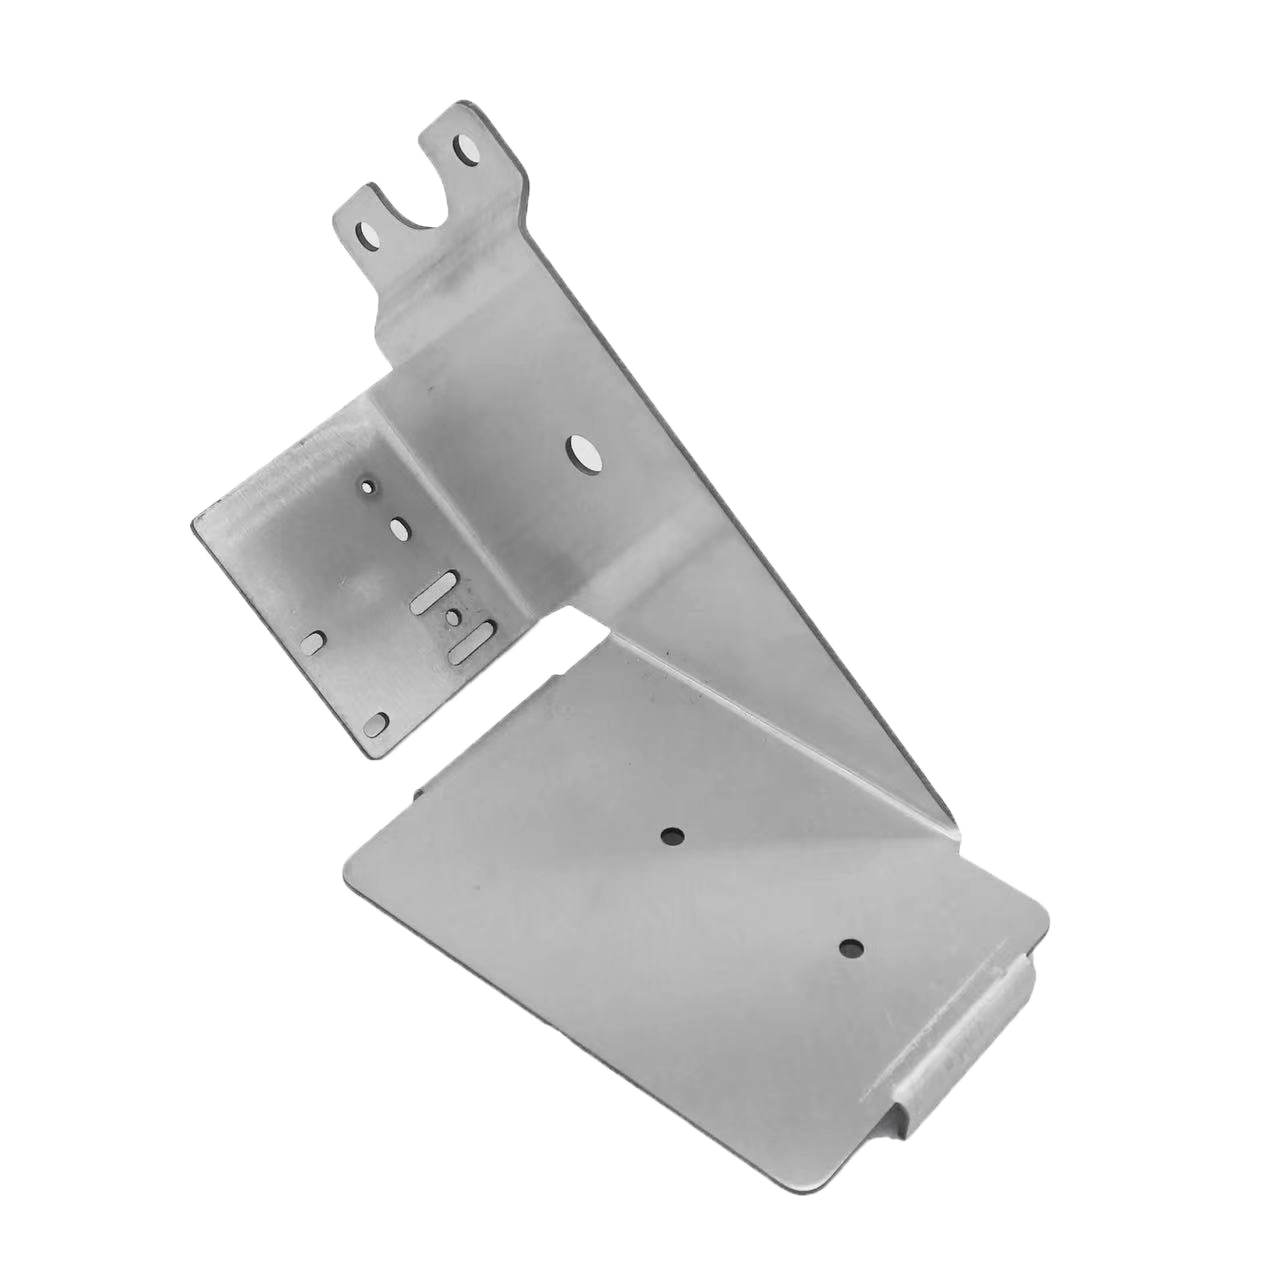
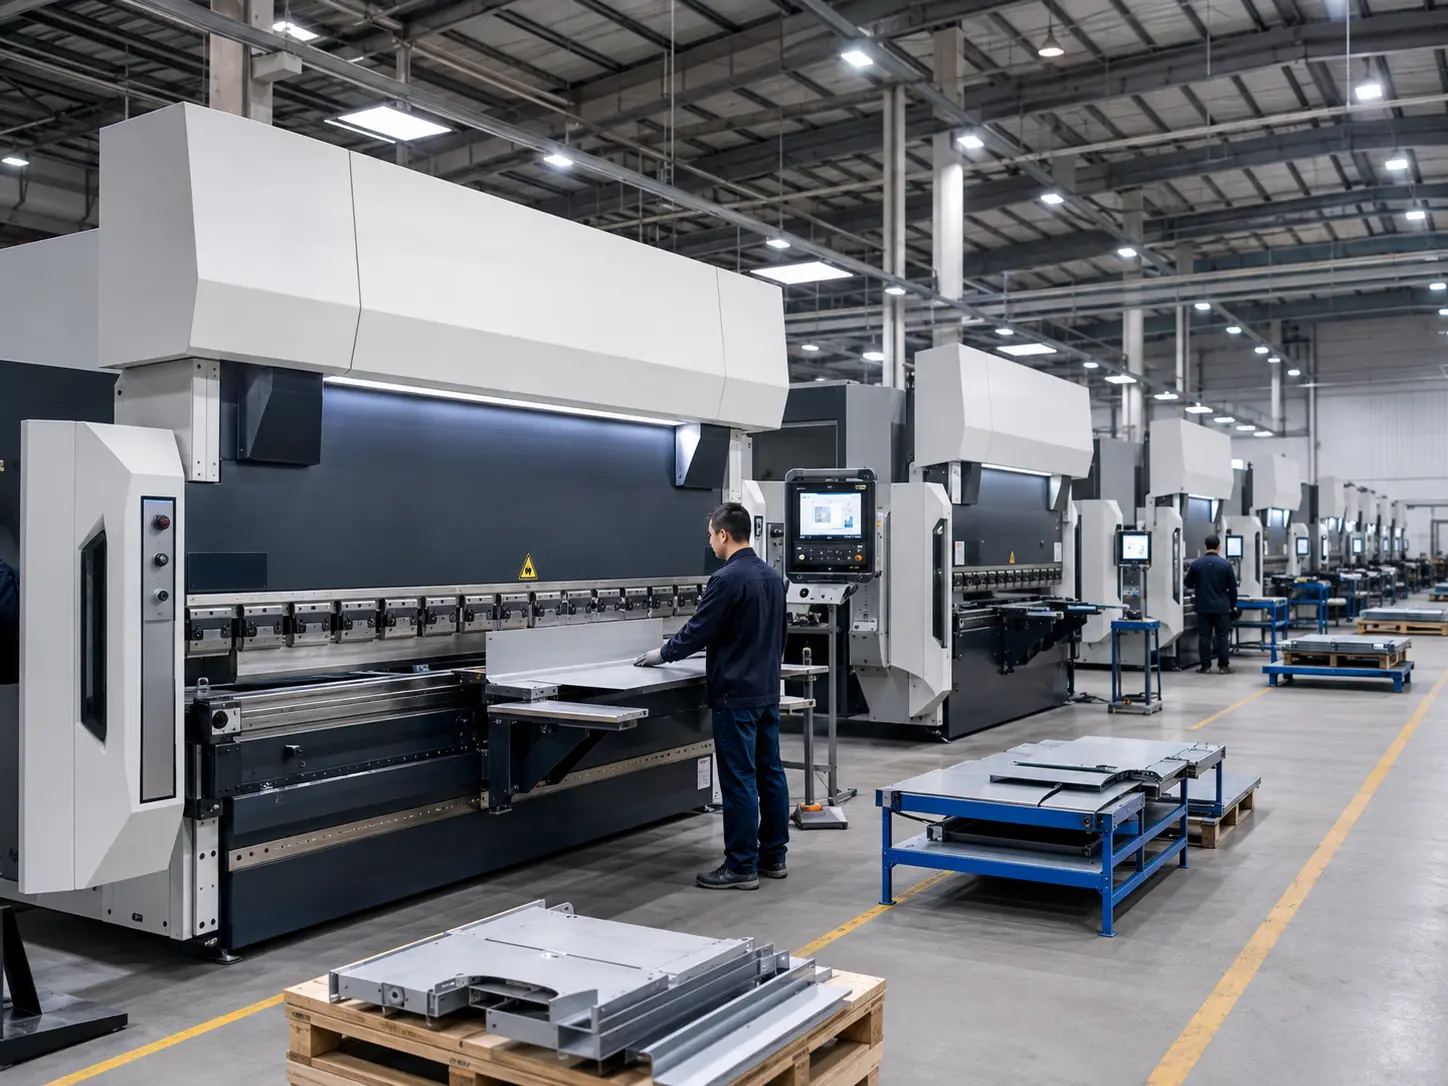
Mit Shuangrui zusammenarbeiten, um die Herstellungskosten zu senken durch 30% und die Effizienz zu steigern.

Metallbiege-Services2026-08-14T02:07:49+00:00

Metallbiege-Services für präzise Blechbauteile

OEM-Blechbiegen für kundenspezifisch geformte Teile, Prototypen und Serienproduktion.

±0,1 mm
Biegegenauigkeit
3–5 Tage
Prototypen-Vorlaufzeit
Prototyp
bis Serienproduktion

Erhalten Sie ein individuelles Angebot in 12 Stunden

Laden Sie Ihre Zeichnungen zur technischen Prüfung hoch.

Leeres Formular (#4)

Warum SR MFG für Metallbiegen wählen

Stabile Biegequalität für Prototypen und Serien-Blechbauteile, mit Kontrolle vom Prozess-Setup bis zur Endlieferung.

Stabile Serienproduktion

Gewährleisten Sie eine konsistente Serienproduktion durch rückverfolgbare Fertigungsprozesse und ein strukturiertes Qualitätskontrollsystem.

DFM-Zusammenarbeit

Durch engineering-geführte DFM-Zusammenarbeit optimieren wir Metallbiegeprozesse und Fertigungskosten bereits in der Designphase.

metal bent parts

One-Stop-Fertigung

Wir bieten ein Komplettangebot an Blechfertigungsdienstleistungen vom Metallbiegen bis zum finalen Versand.

Prozessoptimierung

Wir optimieren Werkzeug-Setup, Biegefolge und Prozessparameter, um die Wiederholbarkeit zu verbessern und Nacharbeit in der Serienproduktion zu reduzieren.

Biegeproblem Häufige Herausforderung SR MFG-Ansatz
Biegewinkel-Konsistenz Biegewinkel können zwischen Chargen variieren und Montagenacharbeit verursachen. Standardisierte Gesenkbiegeparameter und Inspektion halten geformte Teile konsistent.
Teilegröße & Dickenbereich Kleine Werkstätten vergeben große oder komplexe Biegeaufträge möglicherweise an Dritte. Mehrere Gesenkbiegemaschinen unterstützen kleine Präzisionsteile, Paneele, Rahmen und Schweißkonstruktionen.
Biege- + Schweißverzug Biegen wird getrennt vom Schweißen durchgeführt, was später Ausrichtungs- oder Schrumpfungsprobleme verursacht. Biegen, Schweißen und Montage werden gemeinsam geprüft, um Verzugsrisiken zu reduzieren.
Prototypen-zu-Serien-Reproduzierbarkeit Prototypenmuster bestehen, aber die Serienproduktion kann aufgrund unterschiedlicher Maschinen oder Bediener variieren. Dasselbe Prozessfenster, Werkzeug-Setup und dieselben Inspektionsregeln werden vom Prototyp bis zur Serienproduktion übernommen.
Fähigkeiten

SR MFG's Präzisions-Metallbiege-Fähigkeiten

Für OEM-Blechbauteile wie Halterungen, Rahmen, Gehäuse, Paneele und Schweißkonstruktionen bewerten wir Materialdicke, Biegeradius, Werkzeug-Setup, effektive Biegelänge und nachgelagerte Schweiß- oder Montageanforderungen vor der Produktion.

CNC-Gesenkbiegen

Automatische
Biegezentren

Winkelmessung & Kompensation

Prototyp bis Serienproduktion

Macro view of tool marks and pressure impressions left on 1.2mm polished stainless steel sheet after press brake bending

Maschinen und Produktion

SR MFG betreibt mehrere CNC-Gesenkbiegemaschinen und automatische Biegezentren für Bauteile aus Kohlenstoffstahl, Edelstahl und Aluminium. Mit Offline-Programmierung, Winkelmessung und Biegekompensation unterstützen wir stabile Biegegenauigkeit von Prototypen bis zur Serienproduktion.

Wichtige Highlights

  • 2× vollautomatische Biegezentren für hochreproduzierbare Serienproduktion

  • 22× CNC- & Hydraulik-Gesenkbiegemaschinen für Biegen von kleiner bis großer Tonnage

  • Unterstützt Kohlenstoffstahl, Edelstahl, Aluminium

  • Offline-Programmierung, Winkelmessung & Biegekompensation

  • Planned production by tonnage & effective bending length

Processing capacity: stainless steel 1.2 mm, cold-rolled steel 1.5 mm, aluminum 2.0 mm

Bending length: 1,500 mm
Minimum formed size: 350 × 150 mm (four sides), 150 mm (two sides)
Operating efficiency: 0.5 s/stroke (maximum continuous bending speed)
CNC system: STAR300-LGX

Processing capacity: stainless steel 6 mm / cold-rolled steel 8 mm / aluminum 10 mm
Bending length: 4,000 mm
Minimum formed size: 200 × 150 mm
Operating efficiency: 5 mm/s (4+1 axes)
CNC system: DELEM DA58T

Processing capacity: stainless steel 2 mm / cold-rolled steel 3 mm / aluminum 4 mm
Bending length: 2,000 mm
Minimum formed size: 100 × 80 mm
Operating efficiency: 10 mm/s (4 axes)
CNC system: CYBELEC CT12

Processing capacity: stainless steel 3 mm / cold-rolled steel 4 mm / aluminum 5 mm
Bending length: 3,200 mm
Minimum formed size: 120 mm (two sides)
Operating efficiency: 8 mm/s (3+1 axes)
CNC system: ESA S540

Processing capacity: stainless steel 2 mm / cold-rolled steel 3 mm / aluminum 4 mm
Bending length: 3,200 mm
Minimum formed size: 200 × 150 mm
Operating efficiency: 6 mm/s (6 axes)
CNC system: STAR300-LGX

Estimated Daily Bending Capacity

Estimated capacity varies depending on part size, material thickness, bend complexity, tooling setup and inspection requirements.

Equipment Category Quantity (Units) Capacity / Unit (pcs/day) Estimated Daily Output (pcs/day)
Automatic bending centers 2 1,536 3,072
Servo CNC press brakes 5 960 4,800
Large hydraulic press brakes 4 384 1,536
Medium & small press brakes 11 132 1,452
Total bending capacity 22 10,860 pcs/day

* Capacity is estimated under standard production planning. Actual output may vary.

Common Sheet Metal Bending Methods

In many sheet metal projects, metal bending is the key process that turns a laser-cut flat blank into a functional bracket, cover or tray-like structural part. If bending is not performed consistently, problems such as gaps, distortion and misaligned holes will quickly appear during assembly.
At SR MFG, metal bending is not a secondary operation. It is a tightly controlled quality-critical step within our integrated sheet metal production line.
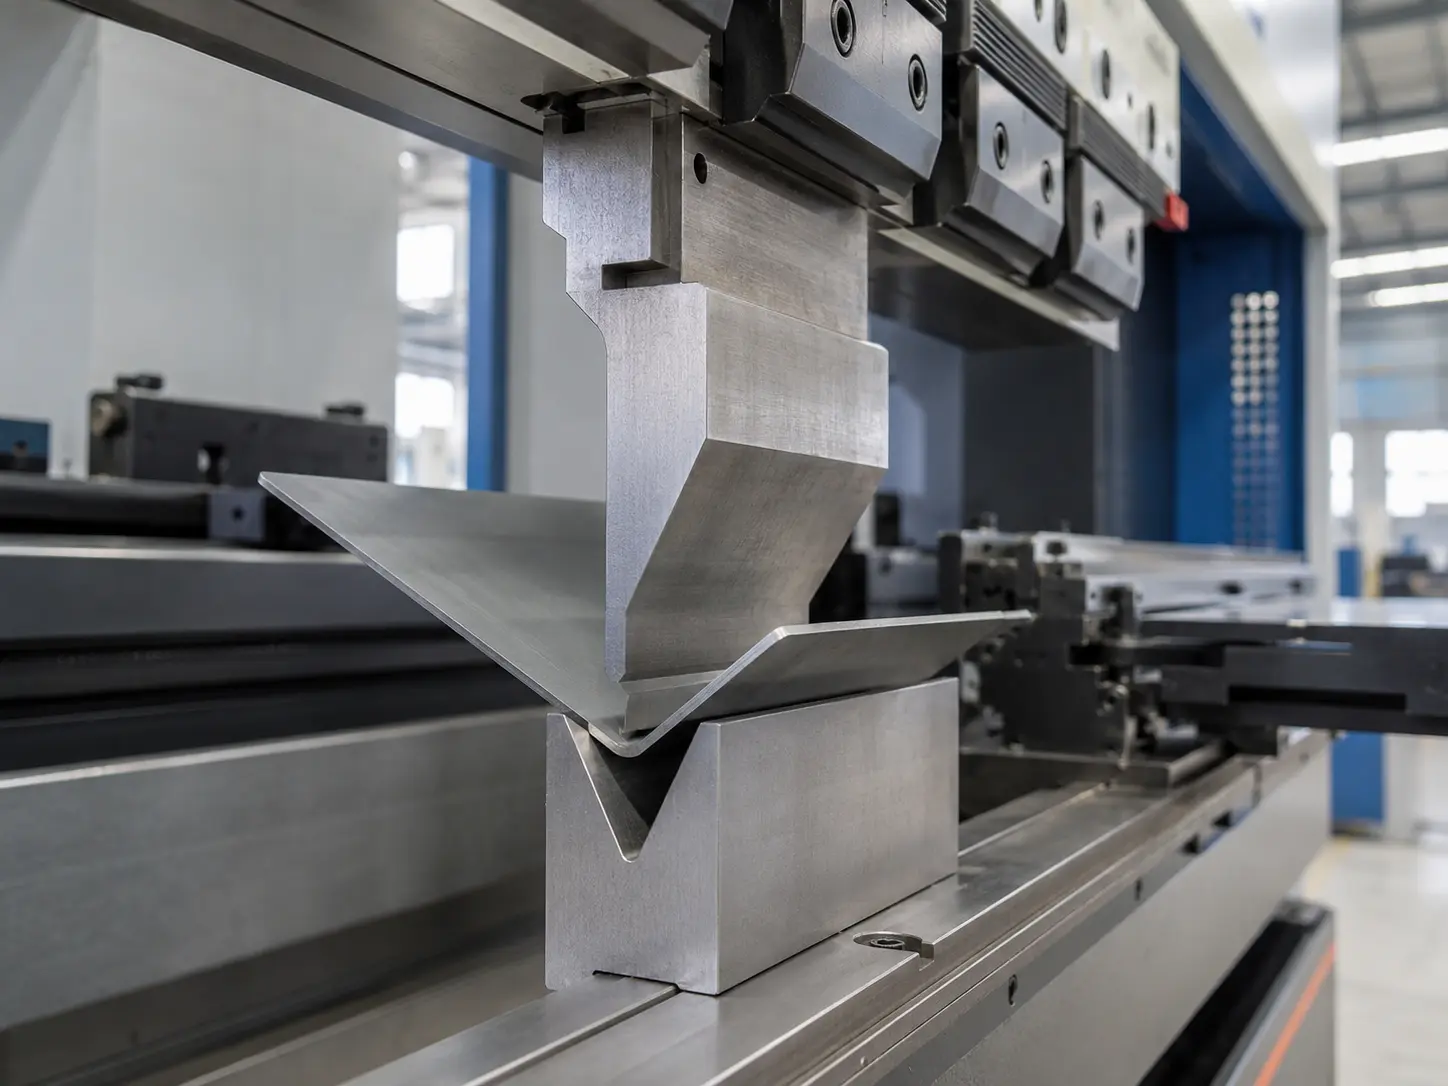
V-bending

V-bending uses a V-shaped punch and die to form straight bends. It is the most common method for brackets, covers, trays, enclosures, and general sheet metal parts requiring consistent bend angles.
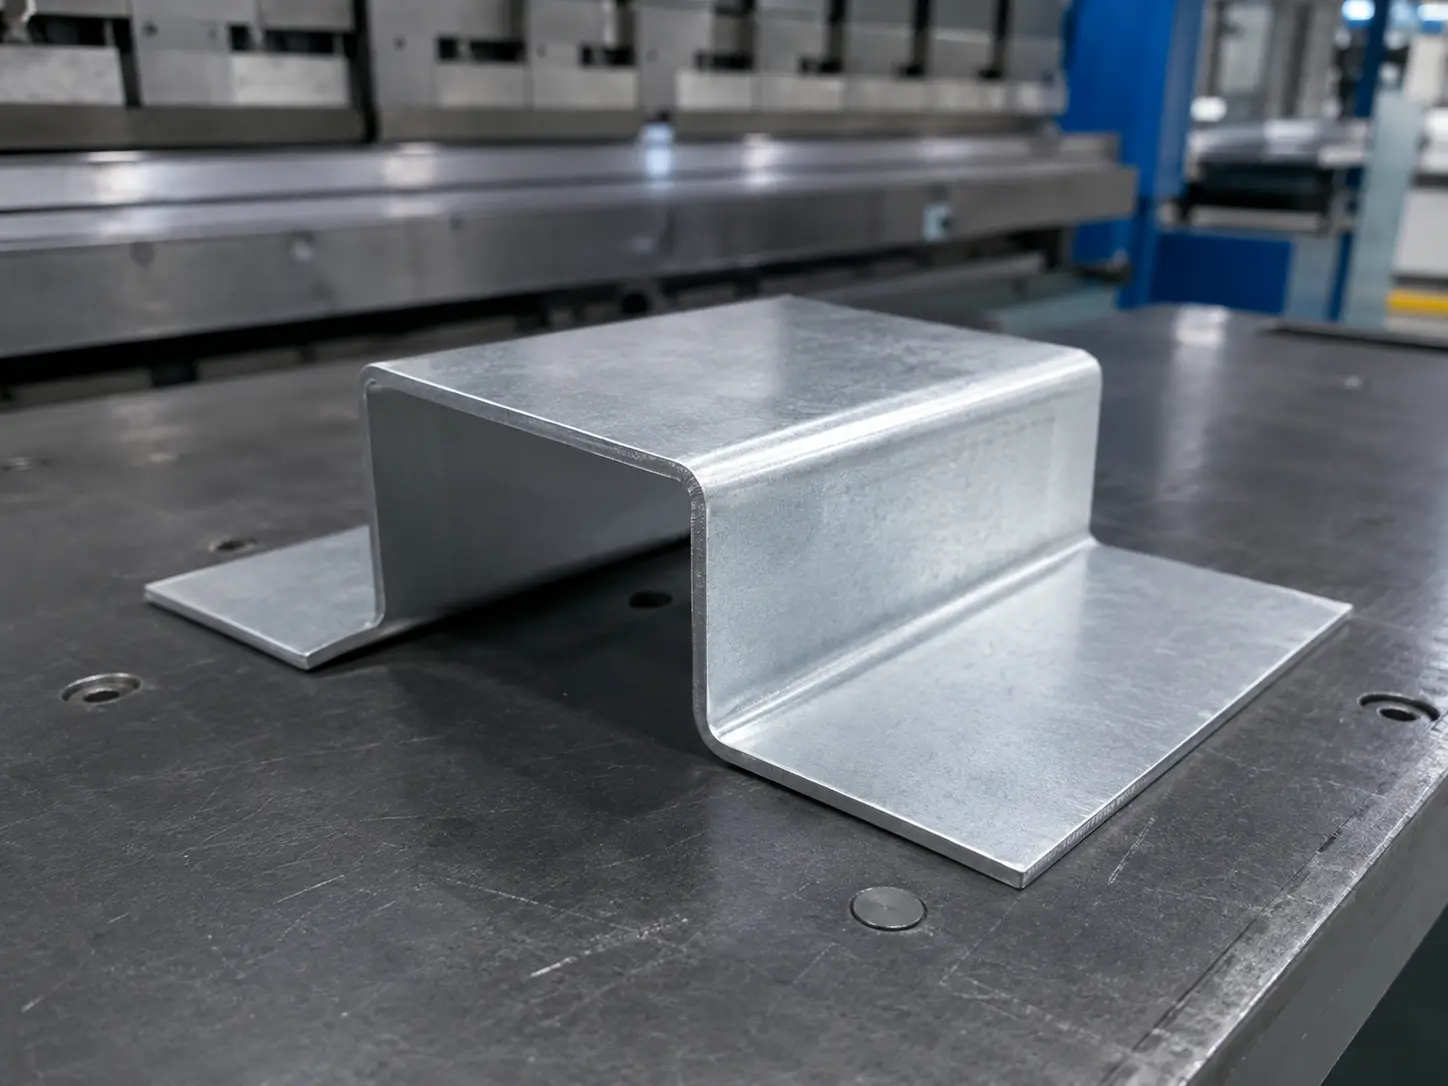
Z-bending

Z-bending forms two opposite-direction bends with a step between them. It is used for offset brackets, mounting flanges, covers, and assembled sheet metal structures where clearance and alignment matter.
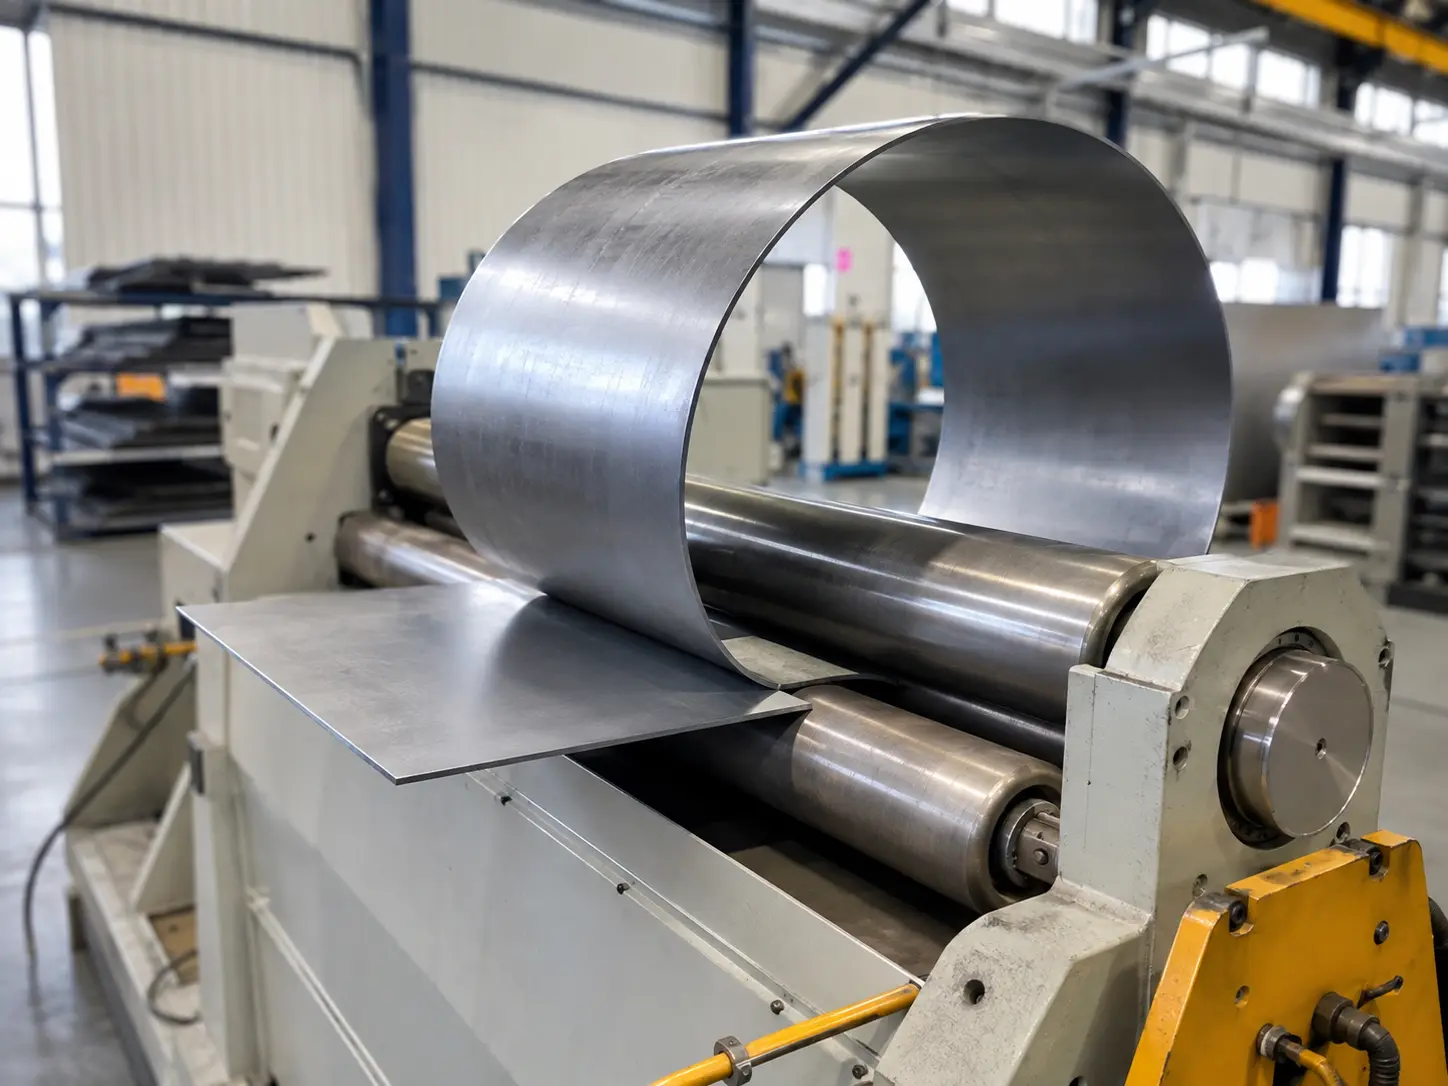
Roll bending (curving)

Roll bending uses rotating rolls to create large-radius curves, arcs, rings, or cylindrical shapes. It is suitable for curved covers, guards, panels, and parts requiring smooth continuous forming.

Typical Metal Bending Tolerances

Bending tolerance depends on material thickness, bend length,bend radius, tooling, part geometry, and inspection requirements.
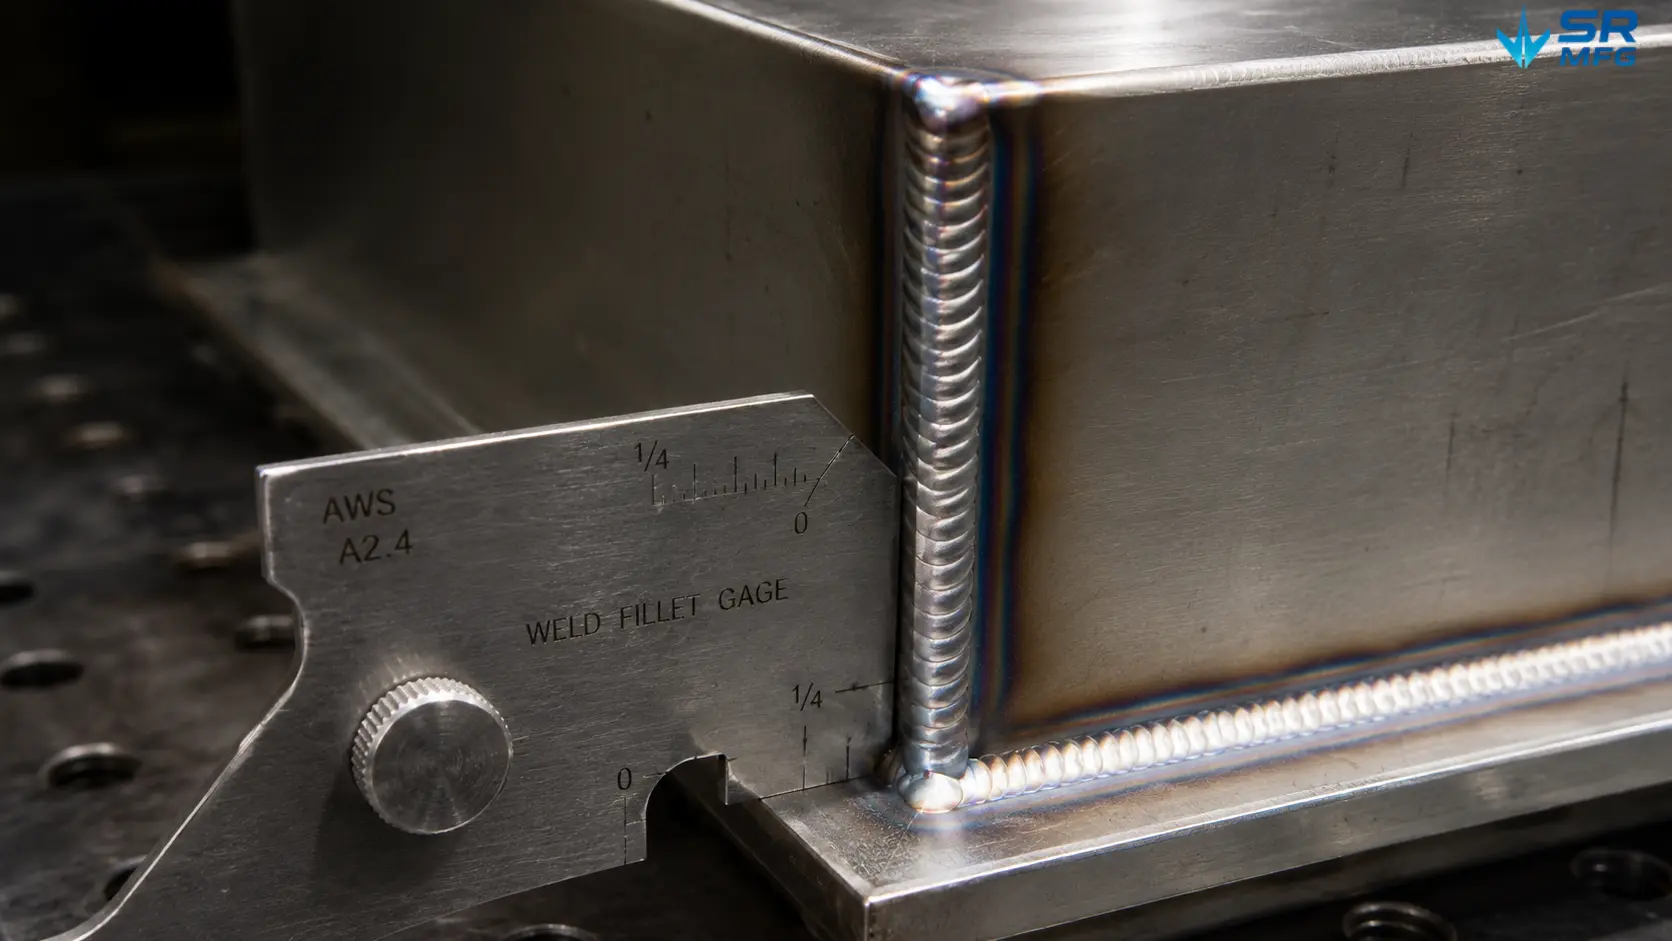
Weld fillet gauge measuring leg length on a TIG-welded stainless steel corner joint during visual weld inspection

Dimensional Tolerance

Typical formed-part dimensions can becontrolled based on drawing requirements,material behavior, and inspectioncheckpoints.

  • Linear dimension:±0.10 mm (standard)
  • Hole position:±0.10 mm
  • Flange length:±0.10 mm
  • Flatness: ≤0.20 mm over 300 mm

*Tighter tolerance can be achieved upon drawing review.

Bend Angle Tolerance

Bend angle consistency is maintainedthrough press brake setup, anglemeasurement, and bendingcompensation.

  • Standard angle tolerance:±1.0°
  • Precision angle tolerance:±0.5° (upon request)
  • Repeatability (same part):±0.5°

*Actual angle tolerance depends on material and thickness.

Critical Features

Key features that affect assembly orfunction are reviewed and controlledwith higher attention.

  • Bend radius:±0.20 mm
  • Edge distance:±0.10 mm
  • Perpendicularity: ≤0.10 mm over 100 mm
  • Twist:
    ≤0.20 mm over 300 mm

*Based on stable process and qualified tooling.

Common Materials for Metal Bending

SR MFG’s metal bending services cover common industrial sheet metals for prototypes, small batches, and high-volume production. Material selection affects bending radius, springback, surface protection, finishing options, and final assembly quality.

Materials We Commonly Bend

Common materials for metal bending include carbon steel, galvanized steel, aluminum alloys, and stainless steels. For best results, bending thickness, minimum bend radius, surface finish, and post-processing requirements should be reviewed together before production.

  • Carbon Steel

  • Verzinkter Stahl

  • Aluminiumlegierungen

  • Stainless Steels

  • Specialty Coated Steels

Carbon Steel

Recommended bending thickness: 0.5–3.0 mm

Typical applications: equipment enclosures, cabinets, brackets, automotive components

Bending note: good dimensional stability and surface quality; suitable for precision formed parts.

Relative cost: Low

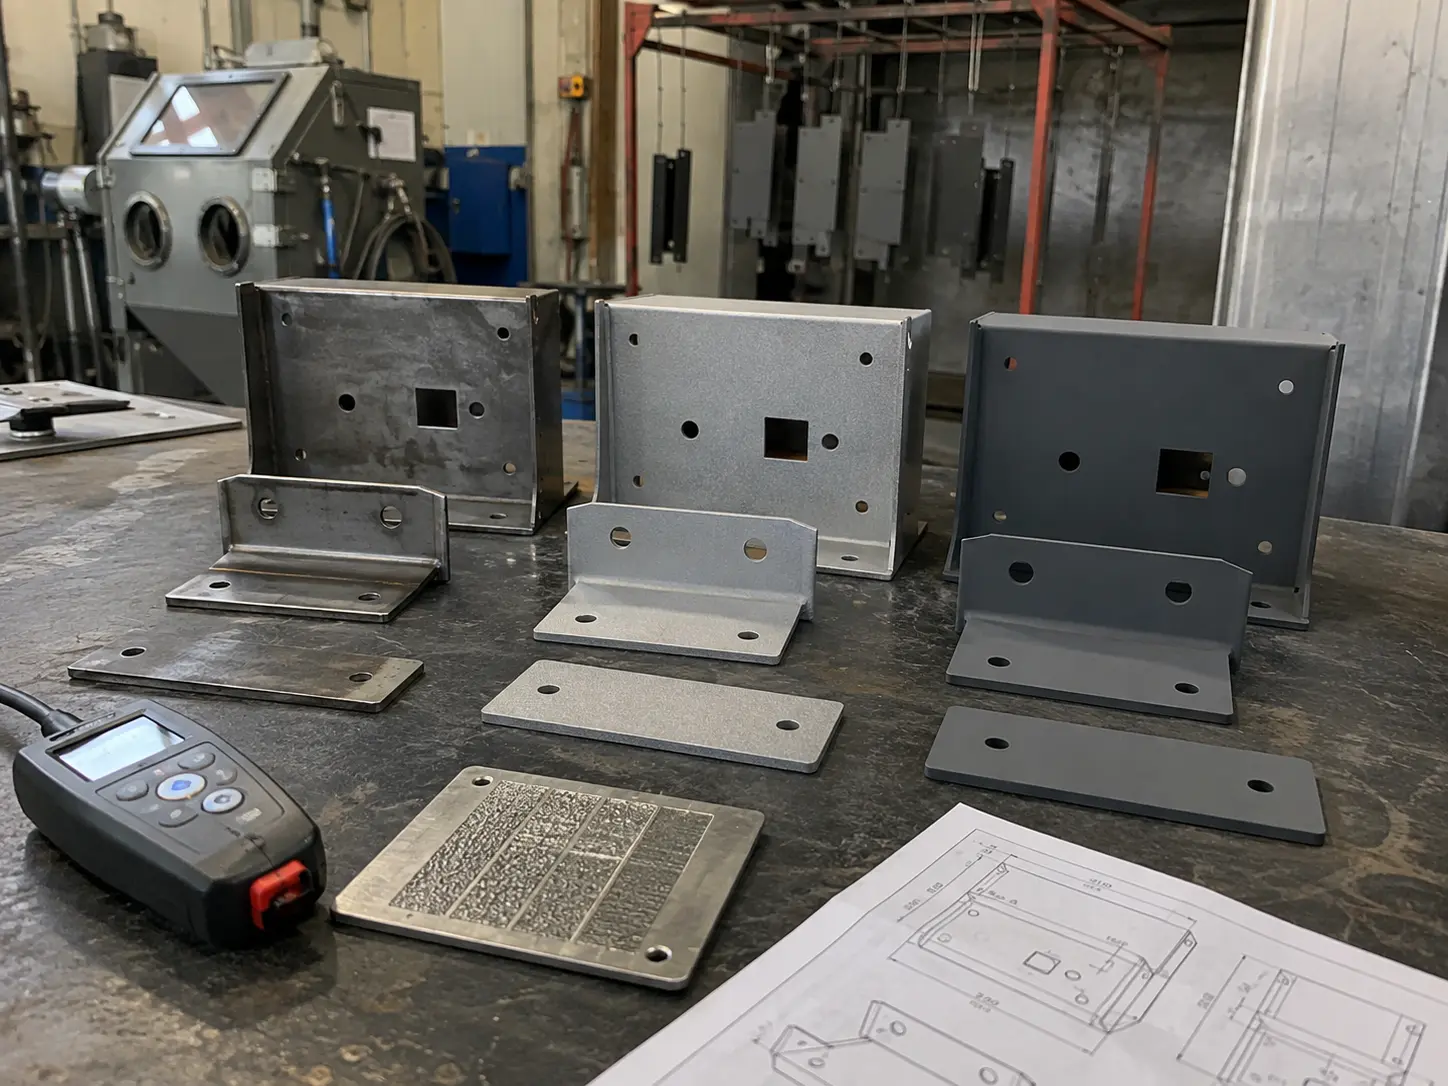
Compatible finishes: powder coating, baking paint, electrophoresis, plating

Corrosion resistance: Fair; usually requires surface protection.

View material details →

Recommended bending thickness: 1.5–6.0 mm

Typical applications: structural parts, heavy machinery components, brackets, frames

Bending note: suitable for stronger formed parts, but surface scale and bend cracking risk should be considered.

Relative cost: Low

Compatible finishes: anti-rust oil, painting, powder coating after pretreatment

Corrosion resistance: Fair; surface treatment is usually required.

View material details →

Galvanized Materials

Recommended bending thickness: 0.5–2.5 mm

Typical applications: outdoor equipment covers, electrical cabinets, HVAC parts, appliance panels

Bending note: bending radius and tooling should protect the zinc layer and reduce coating flaking.

Relative cost: Medium

Compatible finishes: as-galvanized, powder coating, painting

Corrosion resistance: Good

View material details →

Recommended bending thickness: 0.5–2.0 mm

Typical applications: computer chassis, electronics housings, small appliance enclosures

Bending note: offers good surface uniformity for formed parts; avoid repeated bending in the same area.

Relative cost: Medium

Compatible finishes: plating, powder coating, painting, electrophoresis

Corrosion resistance: Good

View material details →

Recommended bending thickness: 0.8–2.0 mm

Typical applications: roofing panels, outdoor covers, appliance back panels, signage parts

Bending note: coated surface should be protected during bending; hard tooling may damage the coating.

Relative cost: Medium

Compatible finishes: as-coated, color-coated, protective coating

Corrosion resistance: Good

View material details →

Aluminiumlegierungen

Recommended bending thickness: 0.8–4.0 mm

Typical applications: marine parts, outdoor enclosures, decorative panels, lightweight brackets

Bending note: good formability and corrosion resistance; suitable for many bent aluminum sheet parts.

Relative cost: Medium

Compatible finishes: anodizing, powder coating, electrophoretic coating

Corrosion resistance: Excellent

View material details →

Recommended bending thickness: 1.0–3.0 mm

Typical applications: structural parts, rail transit components, heat sinks, mechanical frames

Bending note: higher strength but lower bendability than 5052; larger bend radius or heat treatment may be required.

Relative cost: Medium–High

Compatible finishes: anodizing, powder coating, fluorocarbon coating

Corrosion resistance: Excellent

View material details →

Stainless Steels

Recommended bending thickness: 0.5–2.0 mm

Typical applications: food-processing equipment, kitchen equipment, medical parts, general equipment covers

Bending note: higher bending force than carbon steel; grain direction and surface protection should be considered.

Relative cost: High

Compatible finishes: brushing, mirror polishing, passivation

Corrosion resistance: Excellent

View material details →

Recommended bending thickness: 0.5–1.5 mm

Typical applications: decorative parts, cost-sensitive stainless steel products, indoor enclosures

Bending note: lower ductility and corrosion resistance than 304; not recommended for coastal or high salt-spray environments.

Relative cost: Medium–High

Compatible finishes: brushing, powder coating, painting

Corrosion resistance: Good

View material details →

Note: Recommended bending thickness and bend radius depend on material grade, temper, thickness, tooling, bend length, and part geometry. Please share drawings for engineering review before production.

Are you ready to get started on your metal fabrication project?

Not sure which material is ideal for your project? Feel free to contact us.Our engineering team will recommend suitable material grades and sheet thicknesses based on strength, weight, corrosion resistance and overall cost.

Industries & Metal Bending Applications

SR MFG provides metal bending services for OEM sheet metal parts used in industrial equipment, cabinets, brackets, frames, enclosures, and structural assemblies. We support both prototype validation and stable batch production across multiple application sectors.
Industrieausrüstung

Data Centers & IT Equipment

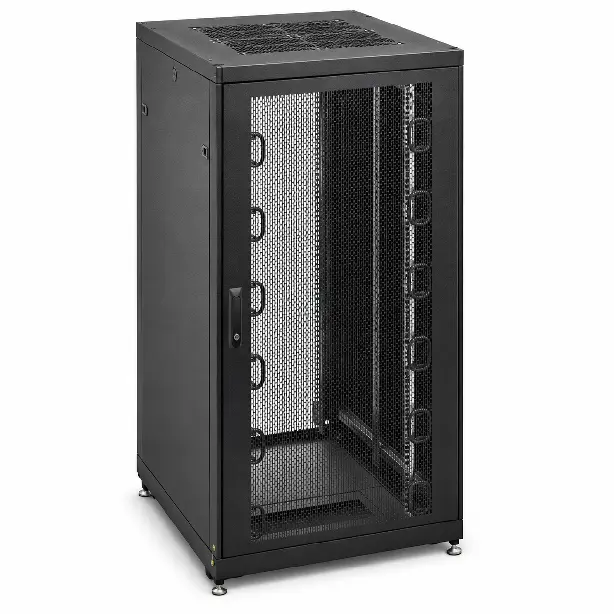
Sheet metal bending parts for data centers, network infrastructure, and IT hardware.

  • Server rack frames & rails
  • Cable management trays
  • Cabinet panels & doors
  • Mounting brackets & plates

Unterhaltungselektronik

Custom metal bending parts for consumer electronics housings, internal brackets, display structures, and precision sheet metal assemblies.

  • Device housings & covers
  • Internal support brackets
  • Display mounting structures
  • Speaker & audio metal parts
  • Small precision formed parts

Elektrische Geräte

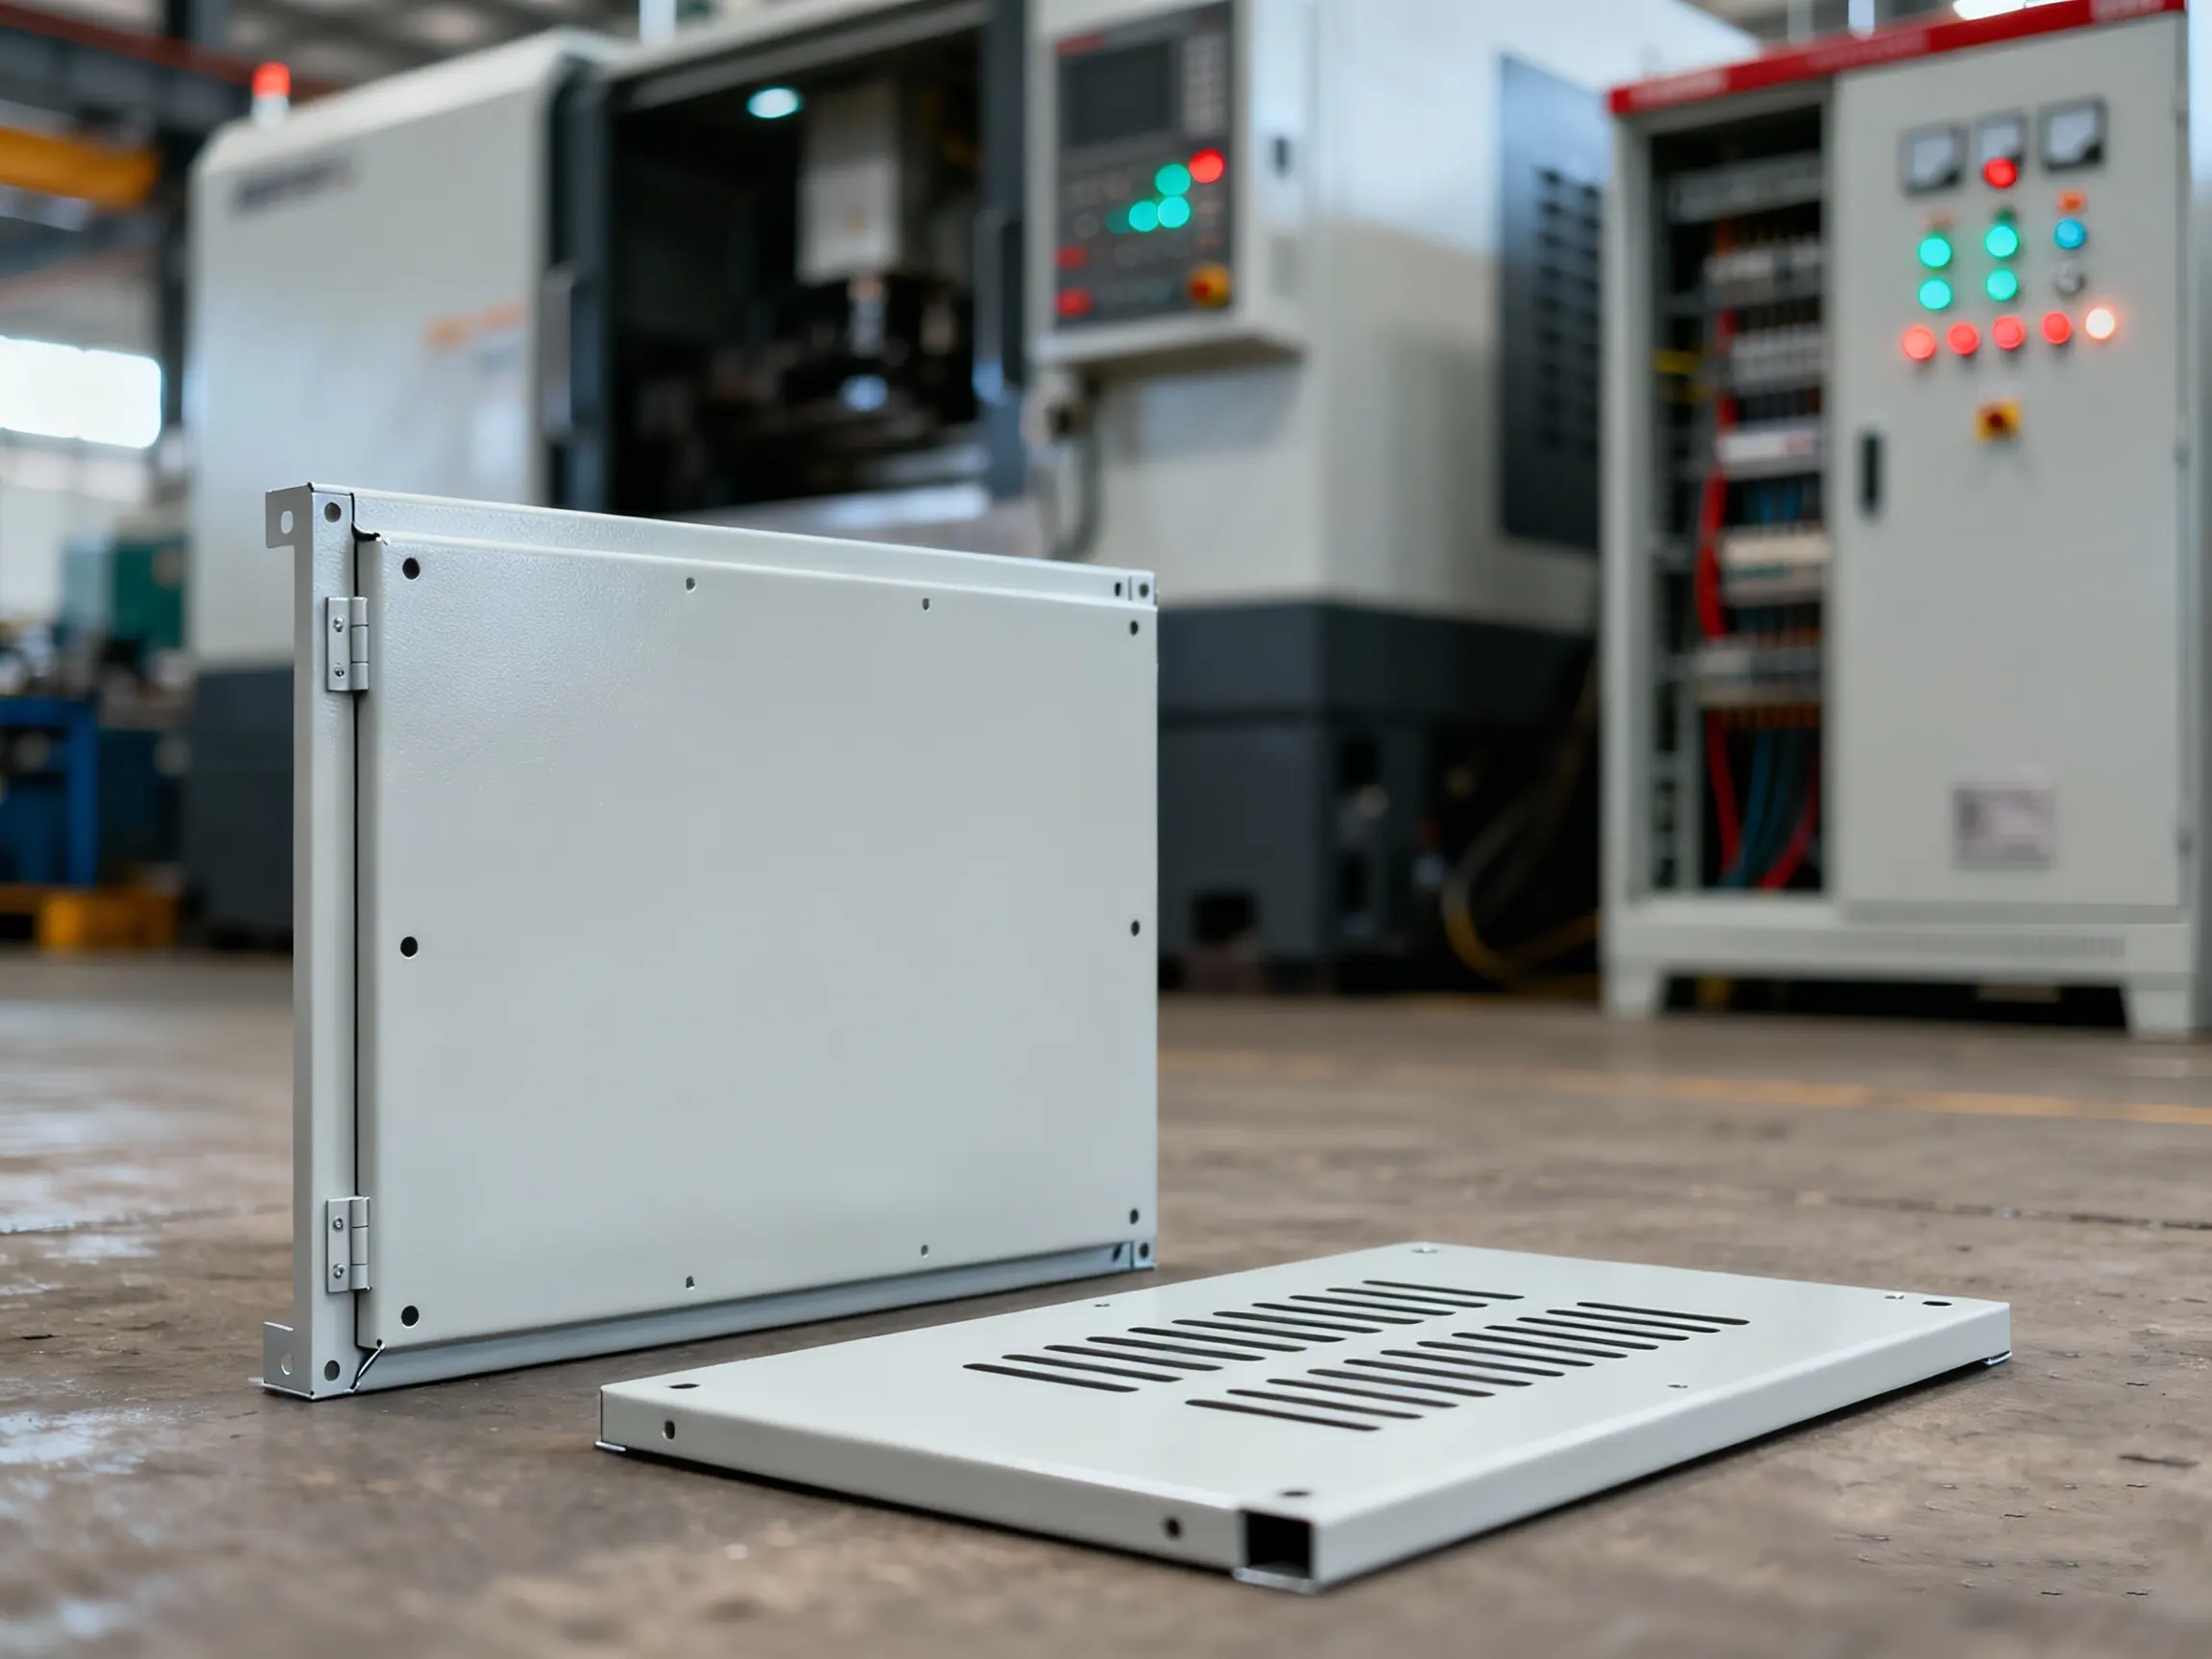
Bent sheet metal components for electrical enclosures, control cabinets, power distribution units, and industrial electrical systems.

  • Electrical cabinet enclosures
  • Control box panels
  • Terminal mounting plates
  • DIN rail brackets
  • Ventilation and access panels

Industrieausrüstung

Metal bending parts for machinery, automation systems, production equipment, and structural machine assemblies.

  • Machine covers & guards
  • Equipment frames
  • Conveyor brackets
  • Sensor mounting plates
  • Protective panels & shields

New Energy Systems

Sheet metal bending solutions for EV charging equipment, battery systems, energy storage cabinets, and power conversion units.

  • Battery enclosure parts
  • Charging station cabinets
  • Energy storage cabinet panels
  • Busbar support brackets
  • Power module housings

Outdoor Equipment

Weather-resistant bent sheet metal parts for outdoor enclosures, equipment covers, BBQ grills, lighting systems, and structural fixtures.

  • Outdoor equipment housings
  • BBQ grill sheet metal bodies
  • Protective covers & panels
  • Mounting brackets
  • Weather-resistant structural parts

Built for Your Application

Whether you need a single prototype or high-volume production, SR MFG ensures consistent quality,tight tolerances, and reliable delivery for your metal bending parts.

OUR WORKFLOW

From Drawings to Finished Bent Sheet Metal Parts

A clear workflow helps reduce bending risks, confirm manufacturability,and keep prototype-to-production delivery under control.
  • 1

    Provide Drawings or Samples
    Send your 2D/3D files, such as STEP, DXF, DWG, or PDF, together with quantity, material, surface finish, and target delivery requirements.

  • 2

    Engineering Review & DFM Recommendations
    Our engineers review bend radii, hole-to-bend distances, forming feasibility, material selection, and potential risks before production starts.

  • 3

    Quotation & Lead Time Confirmation
    We provide a detailed quotation with unit price, tooling cost if required, estimated lead time, and recommended delivery method.

  • 4

    Prototyping & Validation
    For new projects, prototype parts can be produced first to verify dimensions, function, assembly fit, and forming stability.

  • 5

    Mass Production & Quality Management
    During batch production, we monitor bend angles, key dimensions, compensation settings, and surface quality according to agreed inspection standards.

  • 6

    Finishing, Packaging & Shipment
    Optional finishing services include deburring, powder coating, painting, electroplating, and sub-assembly. Finished parts are packed and shipped according to customer requirements.

Design Considerations for Metallbiegen

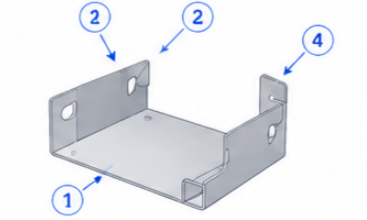
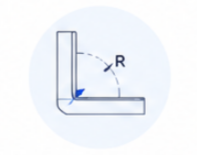
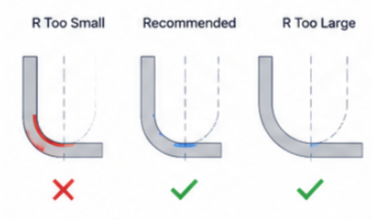
Metal bending affects structural strength, assembly accuracy, and manufacturability. SR MFG reviews bend radius, flange length, hole position, and bend sequence before production to help reduce distortion, cracking, and tooling interference.
01

Bend Radius

Use an appropriate bend radius for each material and thickness to reduce cracking risk and improve forming stability.

02

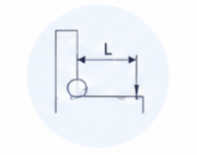
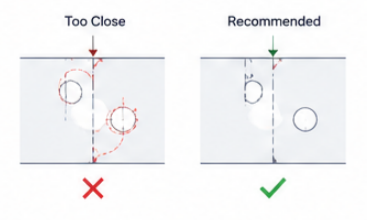
Hole-to-Bend Distance

Keep holes, slots, and notches away from bend lines to prevent deformation during forming.

03

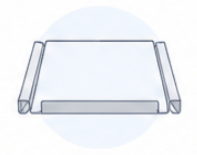
Flange Length & Flatness

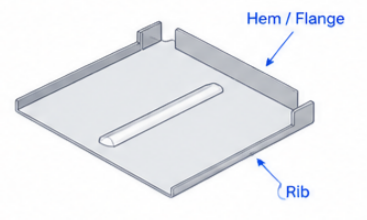
Use enough flange length for tooling contact, and add hems, ribs, or flanges to improve panel flatness.

04

Bend Sequence

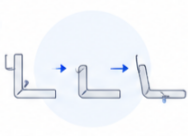
For parts with multiple bends, plan the bend direction and sequence early to avoid tolerance buildup and tooling interference.

-PRICING FACTORS

Pricing for Metal Bending:What Determines the Cost?

Metal bending cost is influenced by material, thickness, part geometry,tolerance requirements, surface finish, and production volume.
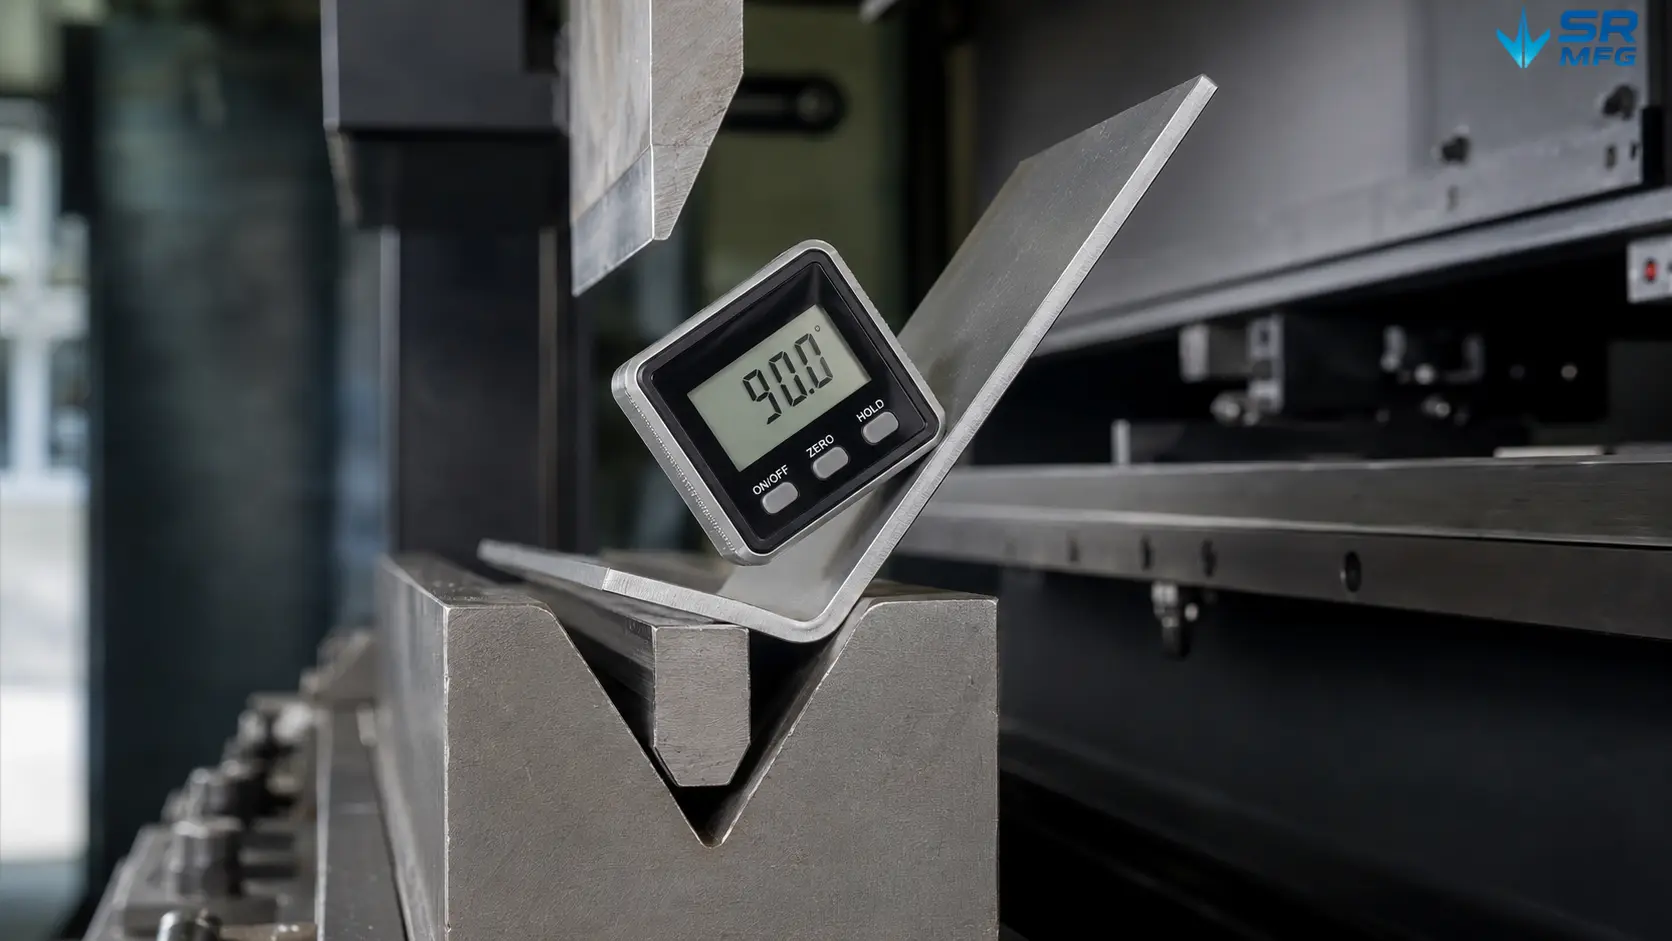
Digital angle gauge measuring bend accuracy on a sheet metal bracket during press brake forming inspection
  • Our pricing model reflects real manufacturing drivers,not just a “per-bend” number-so cost and qualitystay predictable for OEM customers.

Material & Thickness

Thicker or harder materials requirehigher bending force, special tooling,and longer setup time.

Part Geometry & Bending Complexity

Multiple bend directions, short flanges, small radii, and holes near bend lines increase forming difficulty.

Tolerance & Appearance Requirements

Tight angle tolerance, flatness, visible surfaces, and no-scratch requirements add inspection and handling cost.

Batch Size & Repeat Orders

Larger repeat orders can reduce unit cost by spreading programming, setup, and inspection time across more parts.
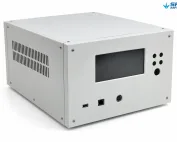
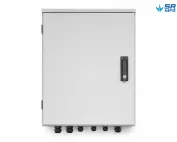
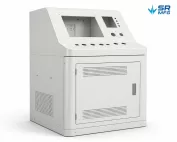
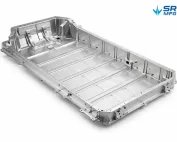
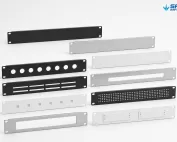
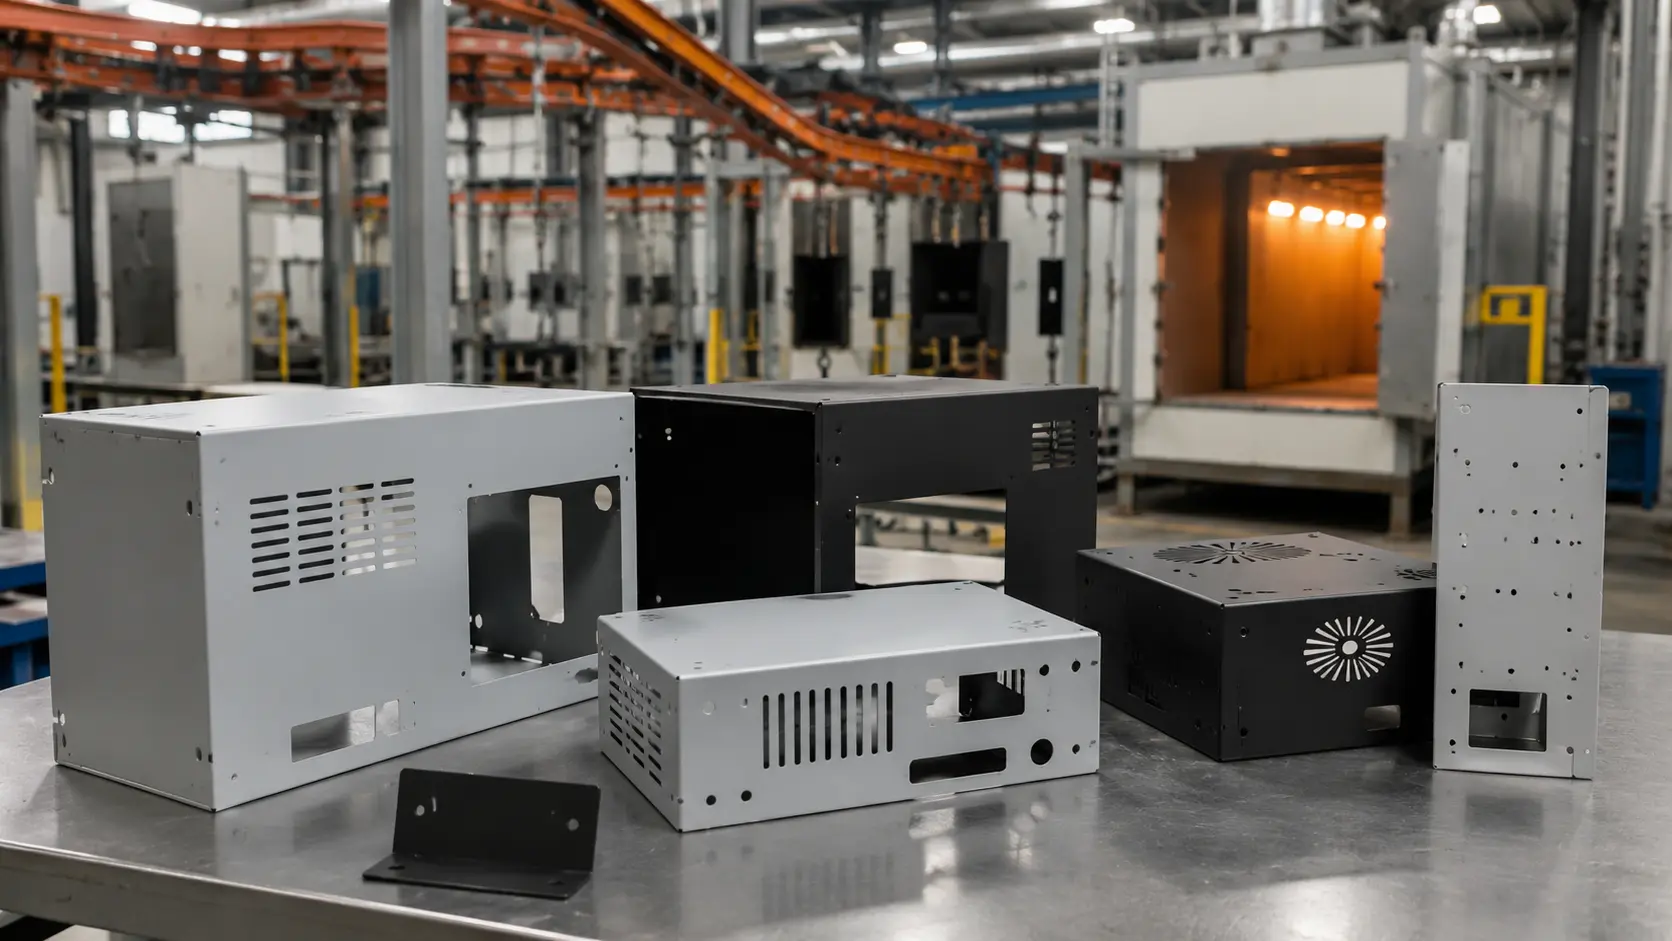
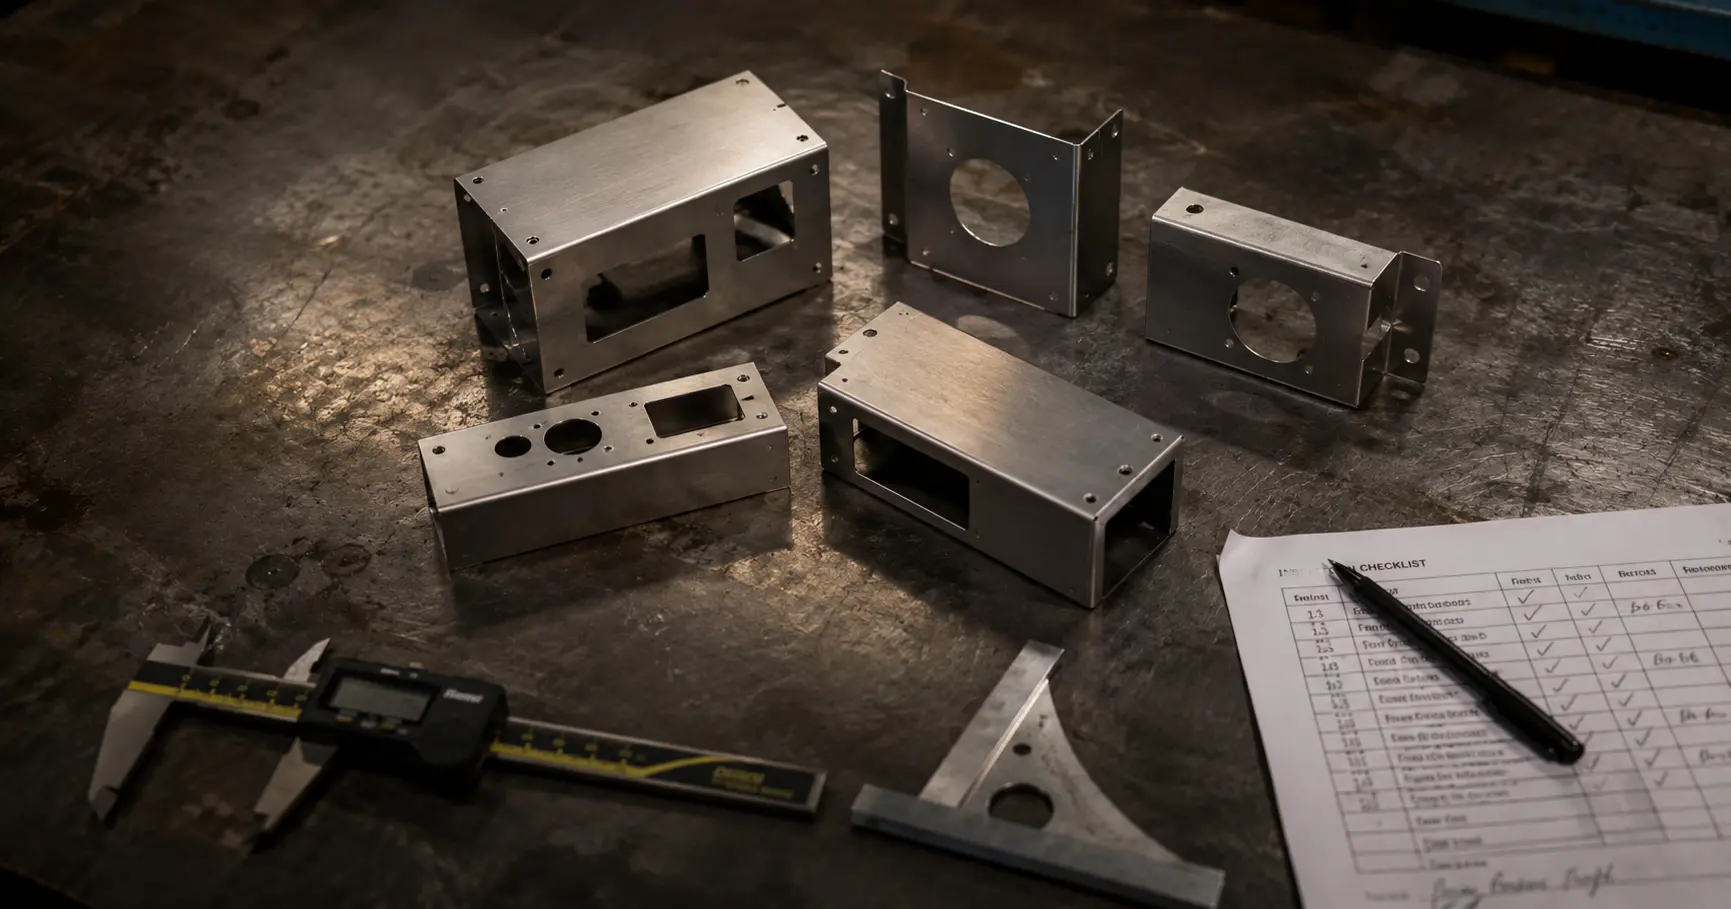
Metal bending products designed and manufactured by SR MFG

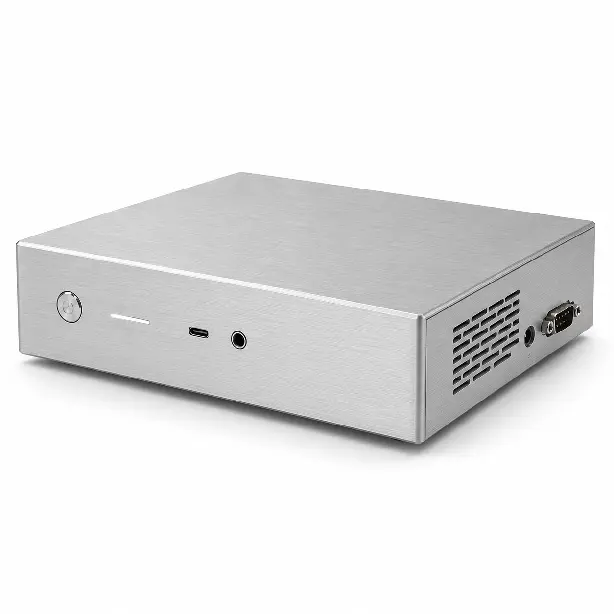
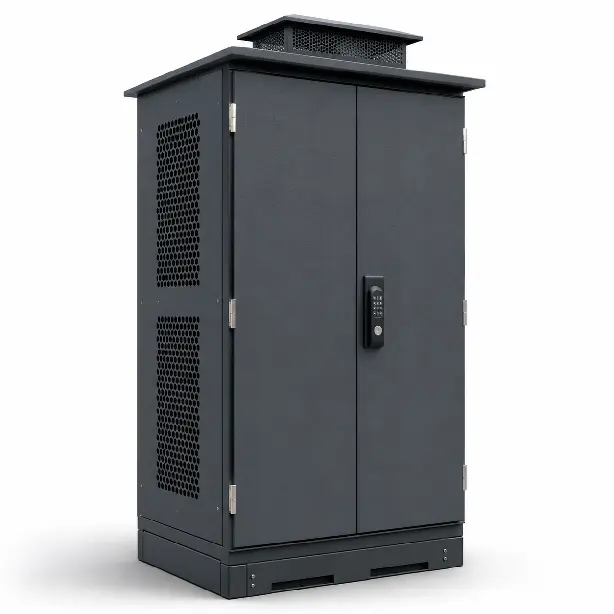
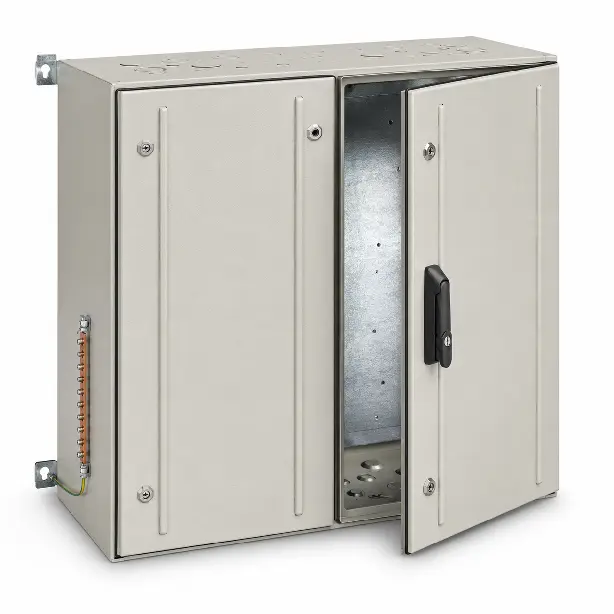
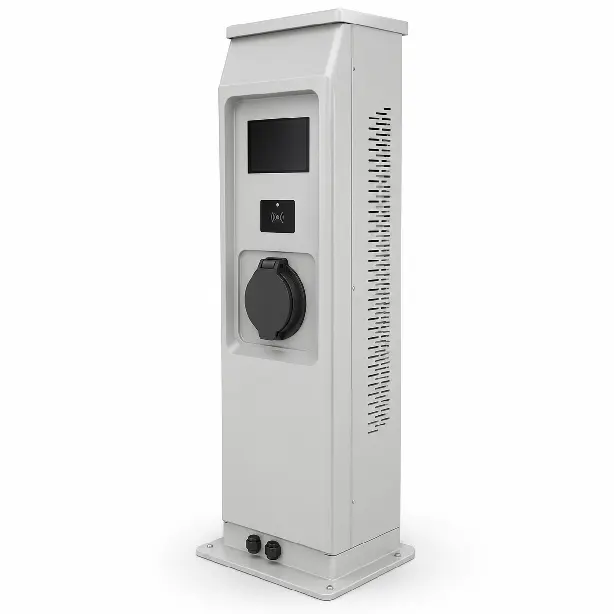
SR MFG has collaborated with global OEMs to co-design and manufacture a variety of custom sheet metal products, covering enclosures, chassis, panels, brackets, and structural components.

Häufig gestellte Fragen Common Problems Regarding Metal Bending

An accurate quote depends on complete technical data, including:

  • 3D models and 2D drawings with tolerances

  • Material grade and thickness

  • Expected surface finish and coating

  • Yearly or batch quantities

  • Any special tests, certifications, or compliance needs

With this package, we can define the bending/fabrication route, estimate cycle times, and give a realistic cost and lead-time window.

Capacity is defined by press brake tonnage, maximum bend length, and open height. In practice, this covers:

  • Thin-gauge doors and covers for cabinets

  • Medium-gauge structural members for frames

  • Thicker brackets and bases

all handled on the same platform, as long as each design stays within the validated material–thickness–length window (confirmed during RFQ and DFM review for each project).

Bending tolerances are first validated on prototypes using agreed measurement points for angles, flatness, and critical interfaces.
Once approved, these checkpoints are built into in-process inspection at the press brake and periodic dimensional audits, with FAI/PPAP-style documentation and SPC where volumes justify it—so the same tolerance scheme stays in place as production scales up.

Yes. In many OEM projects, bending is one step in a chain including laser cutting, welding, surface finishing, and assembly. We define a single integrated route so bent parts move through predefined workcentres and fixtures with common datums and reference edges, reducing handling, shortening lead times, and improving consistency at enclosure or frame level.

Yes. Bent sheet metal parts can be combined with deburring, welding, surface finishing, hardware installation, and assembly according to the project requirements. Keeping these processes with one supplier helps maintain dimensional consistency and reduces additional handling between production stages.

Bending creates a local plastic deformation zone where hardness and yield strength increase slightly, while ductility decreases; away from the bend, properties remain close to the base material.
For static housings and light brackets this is usually beneficial. For dynamic or safety-critical structures, bend radii, material grades, and load paths are defined more conservatively—sometimes supported by testing or simulation—to avoid fatigue or cracking issues.

Related Sheet Metal Manufacturing Resources

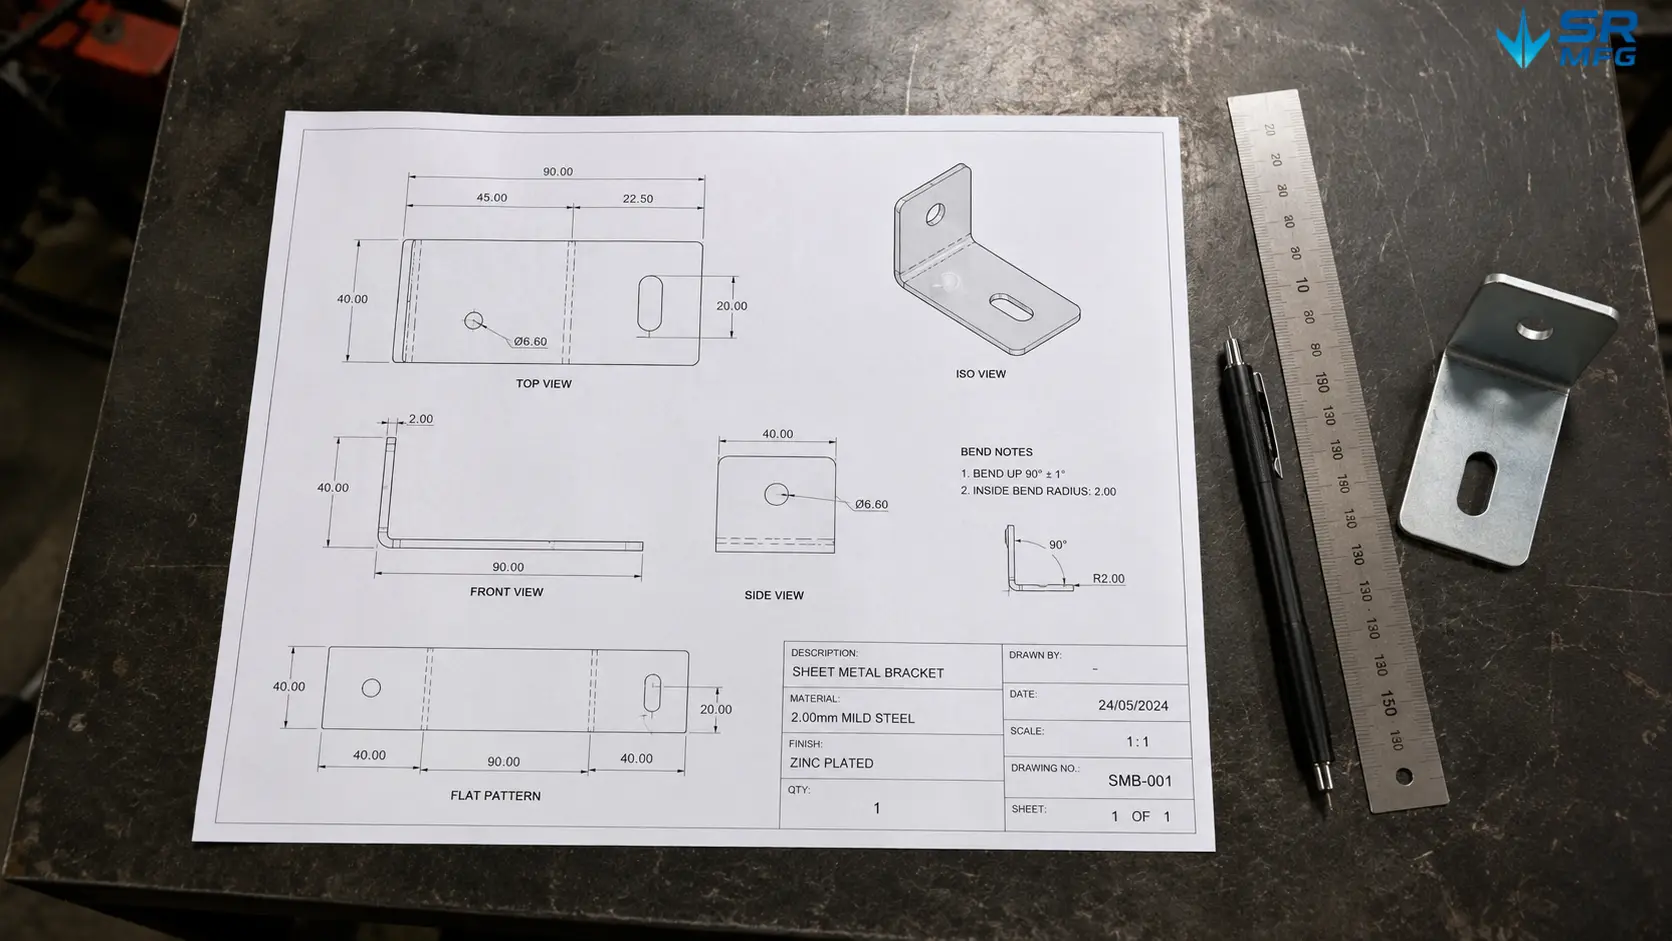
Technical Drawing

Mai 19, 2026|

A technical drawing is a standardized, dimensioned document used to communicate the exact geometry, material, tolerances, and manufacturing [...]

Go to Top