Mit Shuangrui zusammenarbeiten, um die Herstellungskosten zu senken durch 30% und die Effizienz zu steigern.

Metallstanzen-Services2026-08-14T00:53:03+00:00

Präzisions-Metallstanzen für die OEM-Produktion

SR MFG bietet kundenspezifische Metallstanzen-Services für OEM-Blechbauteile und unterstützt Prototypen, Kleinserien und Großserienproduktion. Unser Stanzproduktions-Workflow hilft Kunden, konsistente Teile mit stabilen Abmessungen, effizienten Zykluszeiten und kontrollierten Produktionskosten zu fertigen.
Basierend auf Ihren Zeichnungen, Material, Dicke, Toleranzanforderungen und Produktionsvolumen kann unser Engineering-Team das am besten geeignete Stanzverfahren, die Werkzeuglösung und den Produktionsplan für Ihr Projekt empfehlen.

Hochvolumen-Stanzproduktion

Effiziente Stanzunterstützung für Wiederholbestellungen, große Serien und stabile OEM-Produktion.

Werkzeug- & Prozessunterstützung

Engineering-Prüfung für Werkzeugauswahl, Umformbarkeit, Toleranzen und Produktionskostenkontrolle.

Vom Prototyp zur Serienproduktion

Von der Mustervalidierung bis zur Serienproduktion halten wir Abmessungen und Prozessstandards konsistent.
Erhalten Sie ein individuelles Angebot in 24 Stunden

Laden Sie Ihre Zeichnungen zur technischen Prüfung hoch.

Leeres Formular (#4)

Warum OEM-Kunden SR MFG für Metallstanzen wählen

SR MFG kombiniert Stanzprozessplanung, Werkzeugunterstützung, In-Prozess-Überwachung und integrierte Blechfertigung, um OEM-Kunden stabile Abmessungen, effiziente Produktion und zuverlässige Serienqualität zu ermöglichen.

Maßstabilität & Prozesskontrolle
Wir validieren Schlüsselparameter während der Werkzeugkonstruktion und legen den Basiswert mit First Article Inspection (FAI) fest. In Kombination mit In-Prozess-SPC-Überwachung kann SR MFG Cpk ≥ 1,33 bei Schlüsselmerkmalen für freigegebene Produktionsprogramme einhalten.

Integrierte Umformfähigkeit
Durch die Kombination von Stanzen, Lochen, Biegen, Bördeln und Umformen in Einzelhub- oder Folgeverbundwerkzeug-Operationen reduzieren wir Handhabungsschritte, verkürzen Durchlaufzeiten und minimieren Maßabweichungen zwischen den Operationen.

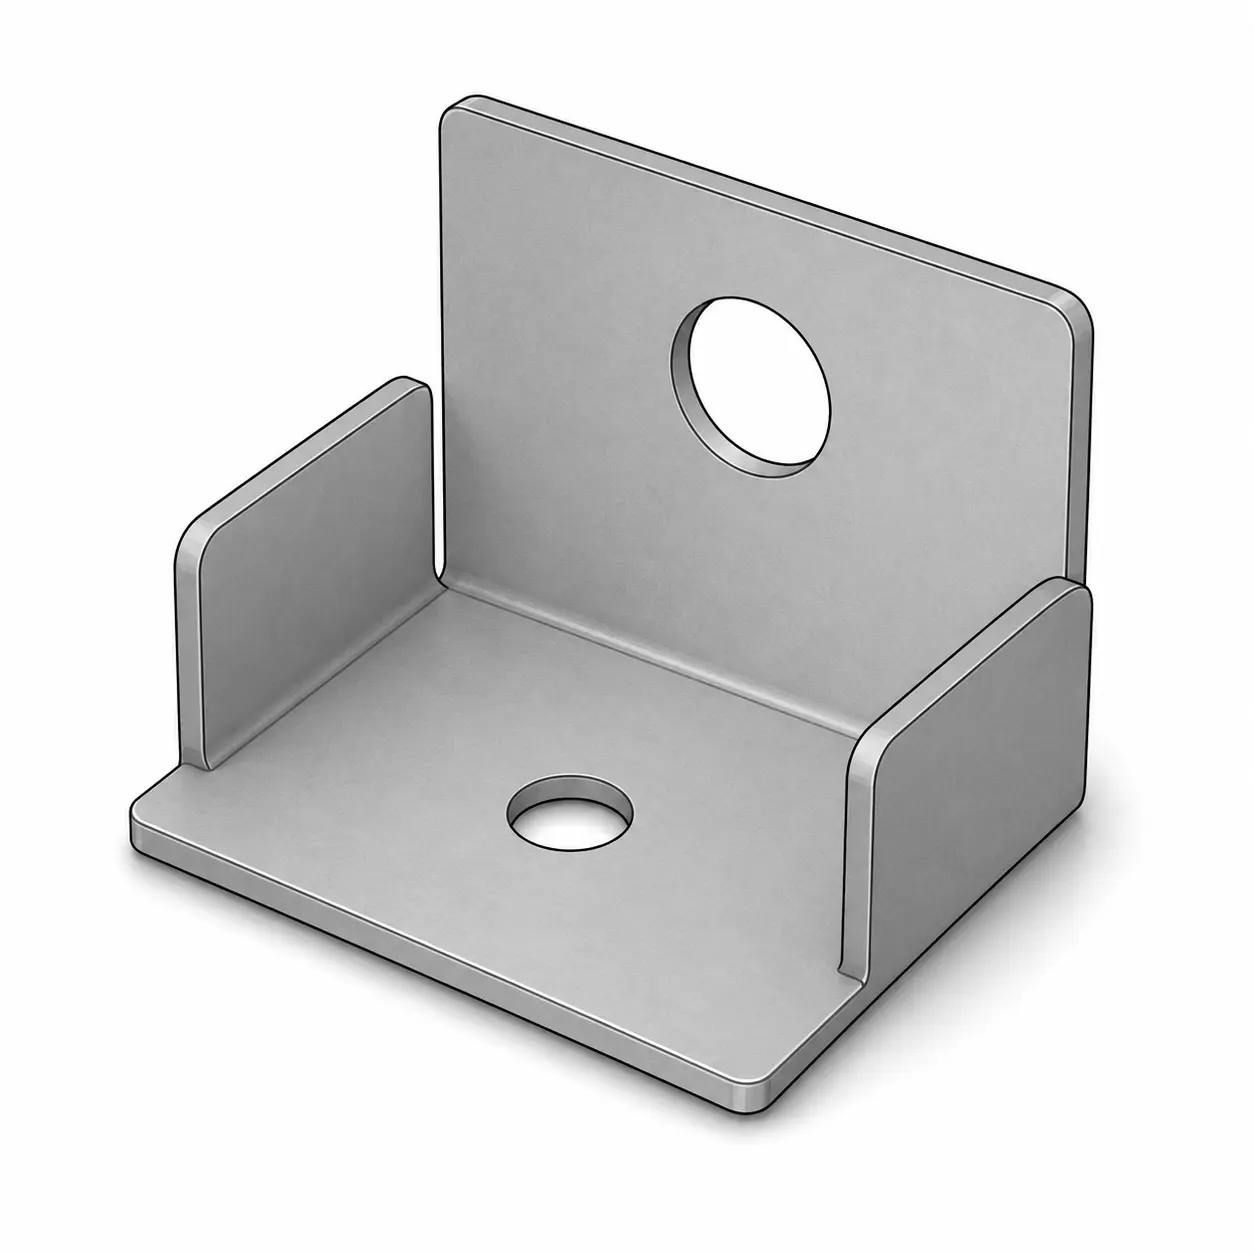
Metal stamped parts

Materialoptimierung & Kostenreduzierung
Durch optimierte Verschachtelung und Folgeverbundwerkzeug-Design kann die Materialausnutzung bis zu 95% in geeigneten Projekten erreichen, was hilft, Ausschuss, Nachbearbeitung und Stückproduktionskosten um 8–12% im Durchschnitt zu reduzieren.

Qualitätssicherung & Vollständige Rückverfolgbarkeit
FAI, IPQC, OQC, Prüfprotokolle, Materialchargen und Produktionsdaten sind rückverfolgbar. Bei Abweichungen unterstützen Rückverfolgbarkeitsdaten die Ursachenidentifikation innerhalb von 2 Stunden unter kontrollierten Produktionsaufzeichnungen.

SR MFG Metallstanzen vs. Konventionelle Lieferanten

Merkmal / Aspekt SR MFG Metallstanzen Konventionelle Lieferanten
Maßstabilität FAI + In-Prozess-SPC-Überwachung; Cpk ≥ 1,33 kann bei Schlüsselmerkmalen für freigegebene Produktionsprogramme eingehalten werden. Verlässt sich oft auf Endprüfungs-Stichproben; Maßabweichungen werden möglicherweise spät erkannt.
Werkzeug- & Prozesskontrolle Werkzeugkonstruktion, Prozessparameter und regelmäßige Werkzeugprüfungen werden gemeinsam verwaltet, um Variationen zu reduzieren. Werkzeugverschleiß und Prozessdrift werden oft reaktiv nach Auftreten von Defekten behandelt.
Verbundoperationen Stanzen, Lochen, Biegen, Bördeln und Umformen können in Einzelhub- oder Folgeverbundwerkzeug-Operationen integriert werden. Mehrere Prozesse können über verschiedene Werkzeuge oder Stationen aufgeteilt sein.
Materialausnutzung Optimierte Verschachtelung und Folgeverbundwerkzeug-Design können bis zu 95% Materialausnutzung in geeigneten Projekten erreichen. Standard-Layouts können höheren Ausschuss und geringere Materialeffizienz verursachen.
Qualität & Rückverfolgbarkeit FAI, IPQC, OQC, Chargenprotokolle, Formdaten und Prüfdaten unterstützen die vollständige Prozessrückverfolgbarkeit. Aufzeichnungen können fragmentiert, unvollständig oder auf Endprüfungsergebnisse beschränkt sein.
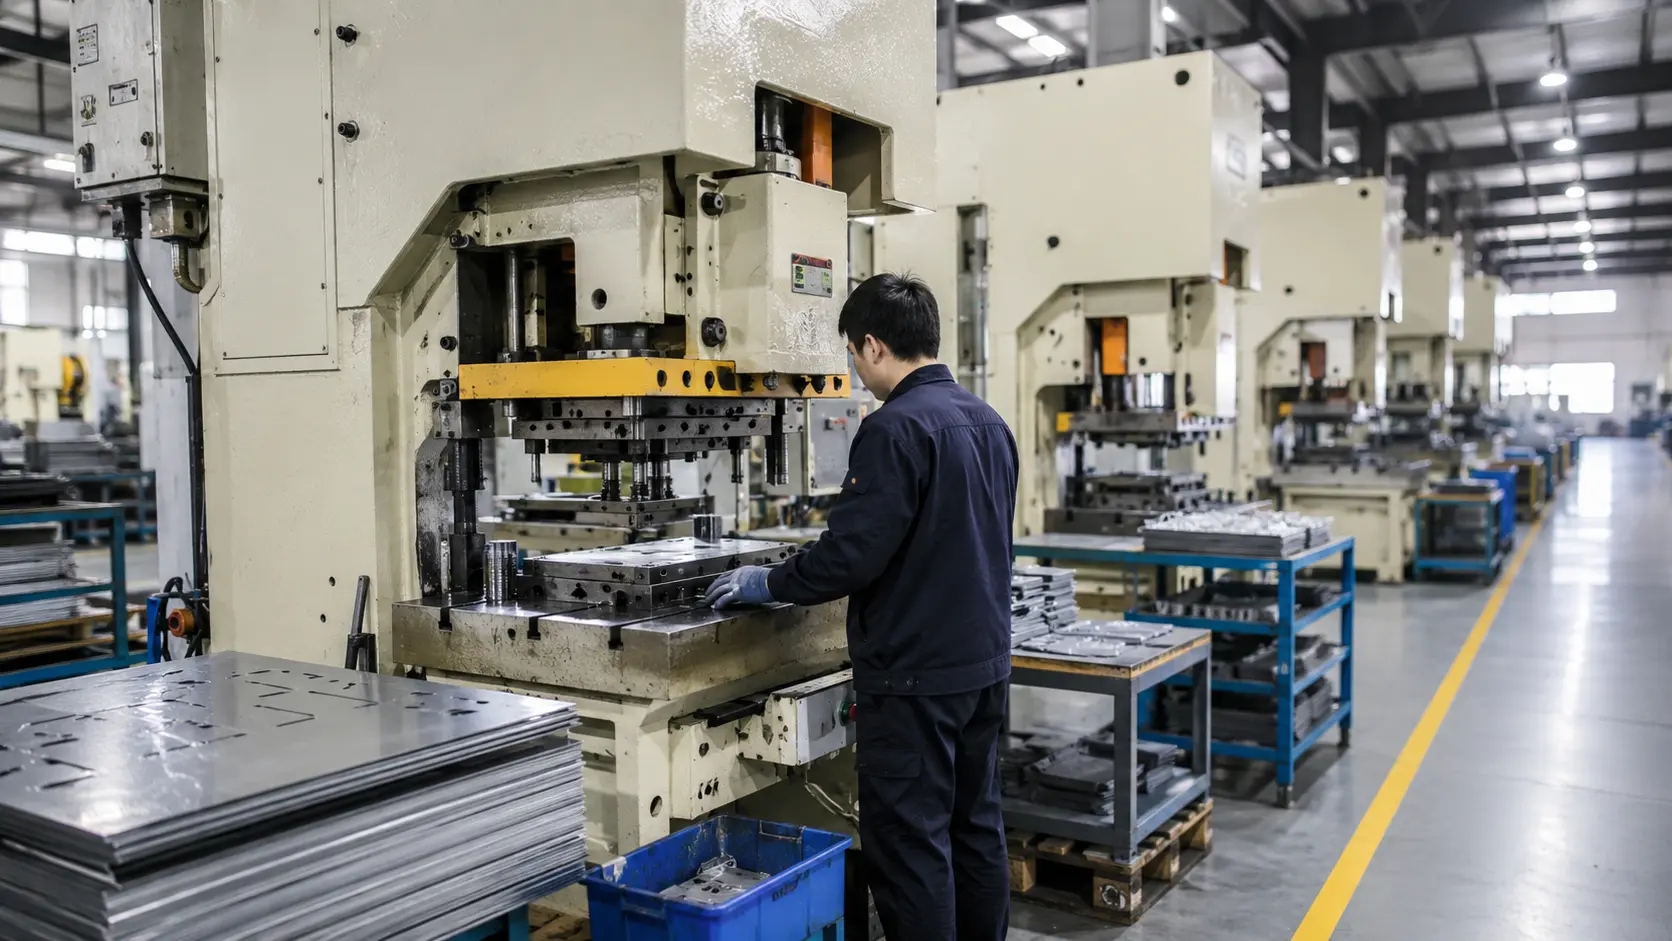
Metal stamping press production line in a sheet metal manufacturing workshop
Fähigkeiten

SR MFGs Stanzfähigkeiten

SR MFG betreibt mehr als 27 professionelle Stanzmaschinen mit Pressenkraft von 40T bis 425T und unterstützt Präzisionskleinteile, strukturelle Stanzkomponenten und Hochvolumen-OEM-Produktion.

Unsere Stanzausrüstung unterstützt Kohlenstoffstahl, Edelstahl, Aluminiumlegierungen und andere Blechmaterialien mit Dicken bis zu 8 mm. Basierend auf realen Produktionsdaten können unsere allgemeinen Stanzlinien bis zu 450 Teile pro Stunde und eine Monatskapazität von bis zu 99.000 Teilen unter validierten Produktionsbedingungen erreichen.

27 +

Stanzmaschinen

Professionelle Ausrüstung für verschiedene Teilegrößen und Komplexität.

40T-425T

Press Range

Wide tonnage range tomeet various formingrequirements.

Up to 8 mm

Materialstärke

Supports a variety ofmaterials and thicknessesfor OEM projects.

Up to 99,000

pcs/MonthUp

Up to 450 pcs/hourand monthly capacity upto 99,000 pieces.

Comprehensive Equipment Portfolio& Process Adaptability

Multiple stamping lines, progressive diecapability, and specialized hydraulic pressessupport a wide range of forming processes,including deep drawing, bending, flanging.embossing, and complex stamping.

Proven High Capacity &Delivery Reliability

Stable high-volume production, strict qualitycontrol, and efficient production managementensure on-time delivery and consistentquality for repeat orders.

Stamping Equipment & Capacity Benchmark

Professional Stamping Presses  |   Actual Capacity Data  |  Reliable Delivery

SR MFG operates 27 professional stamping presses ranging from 40T to 425T. Our equipment covers small precision stamped parts, medium-thick sheet metal parts, and larger formed components.
Capacity planning is based on 2024 actual production data, including equipment operating cycles, effective working hours, qualified output, and work order execution. This helps us provide realistic delivery planning instead of relying only on theoretical stroke rates.
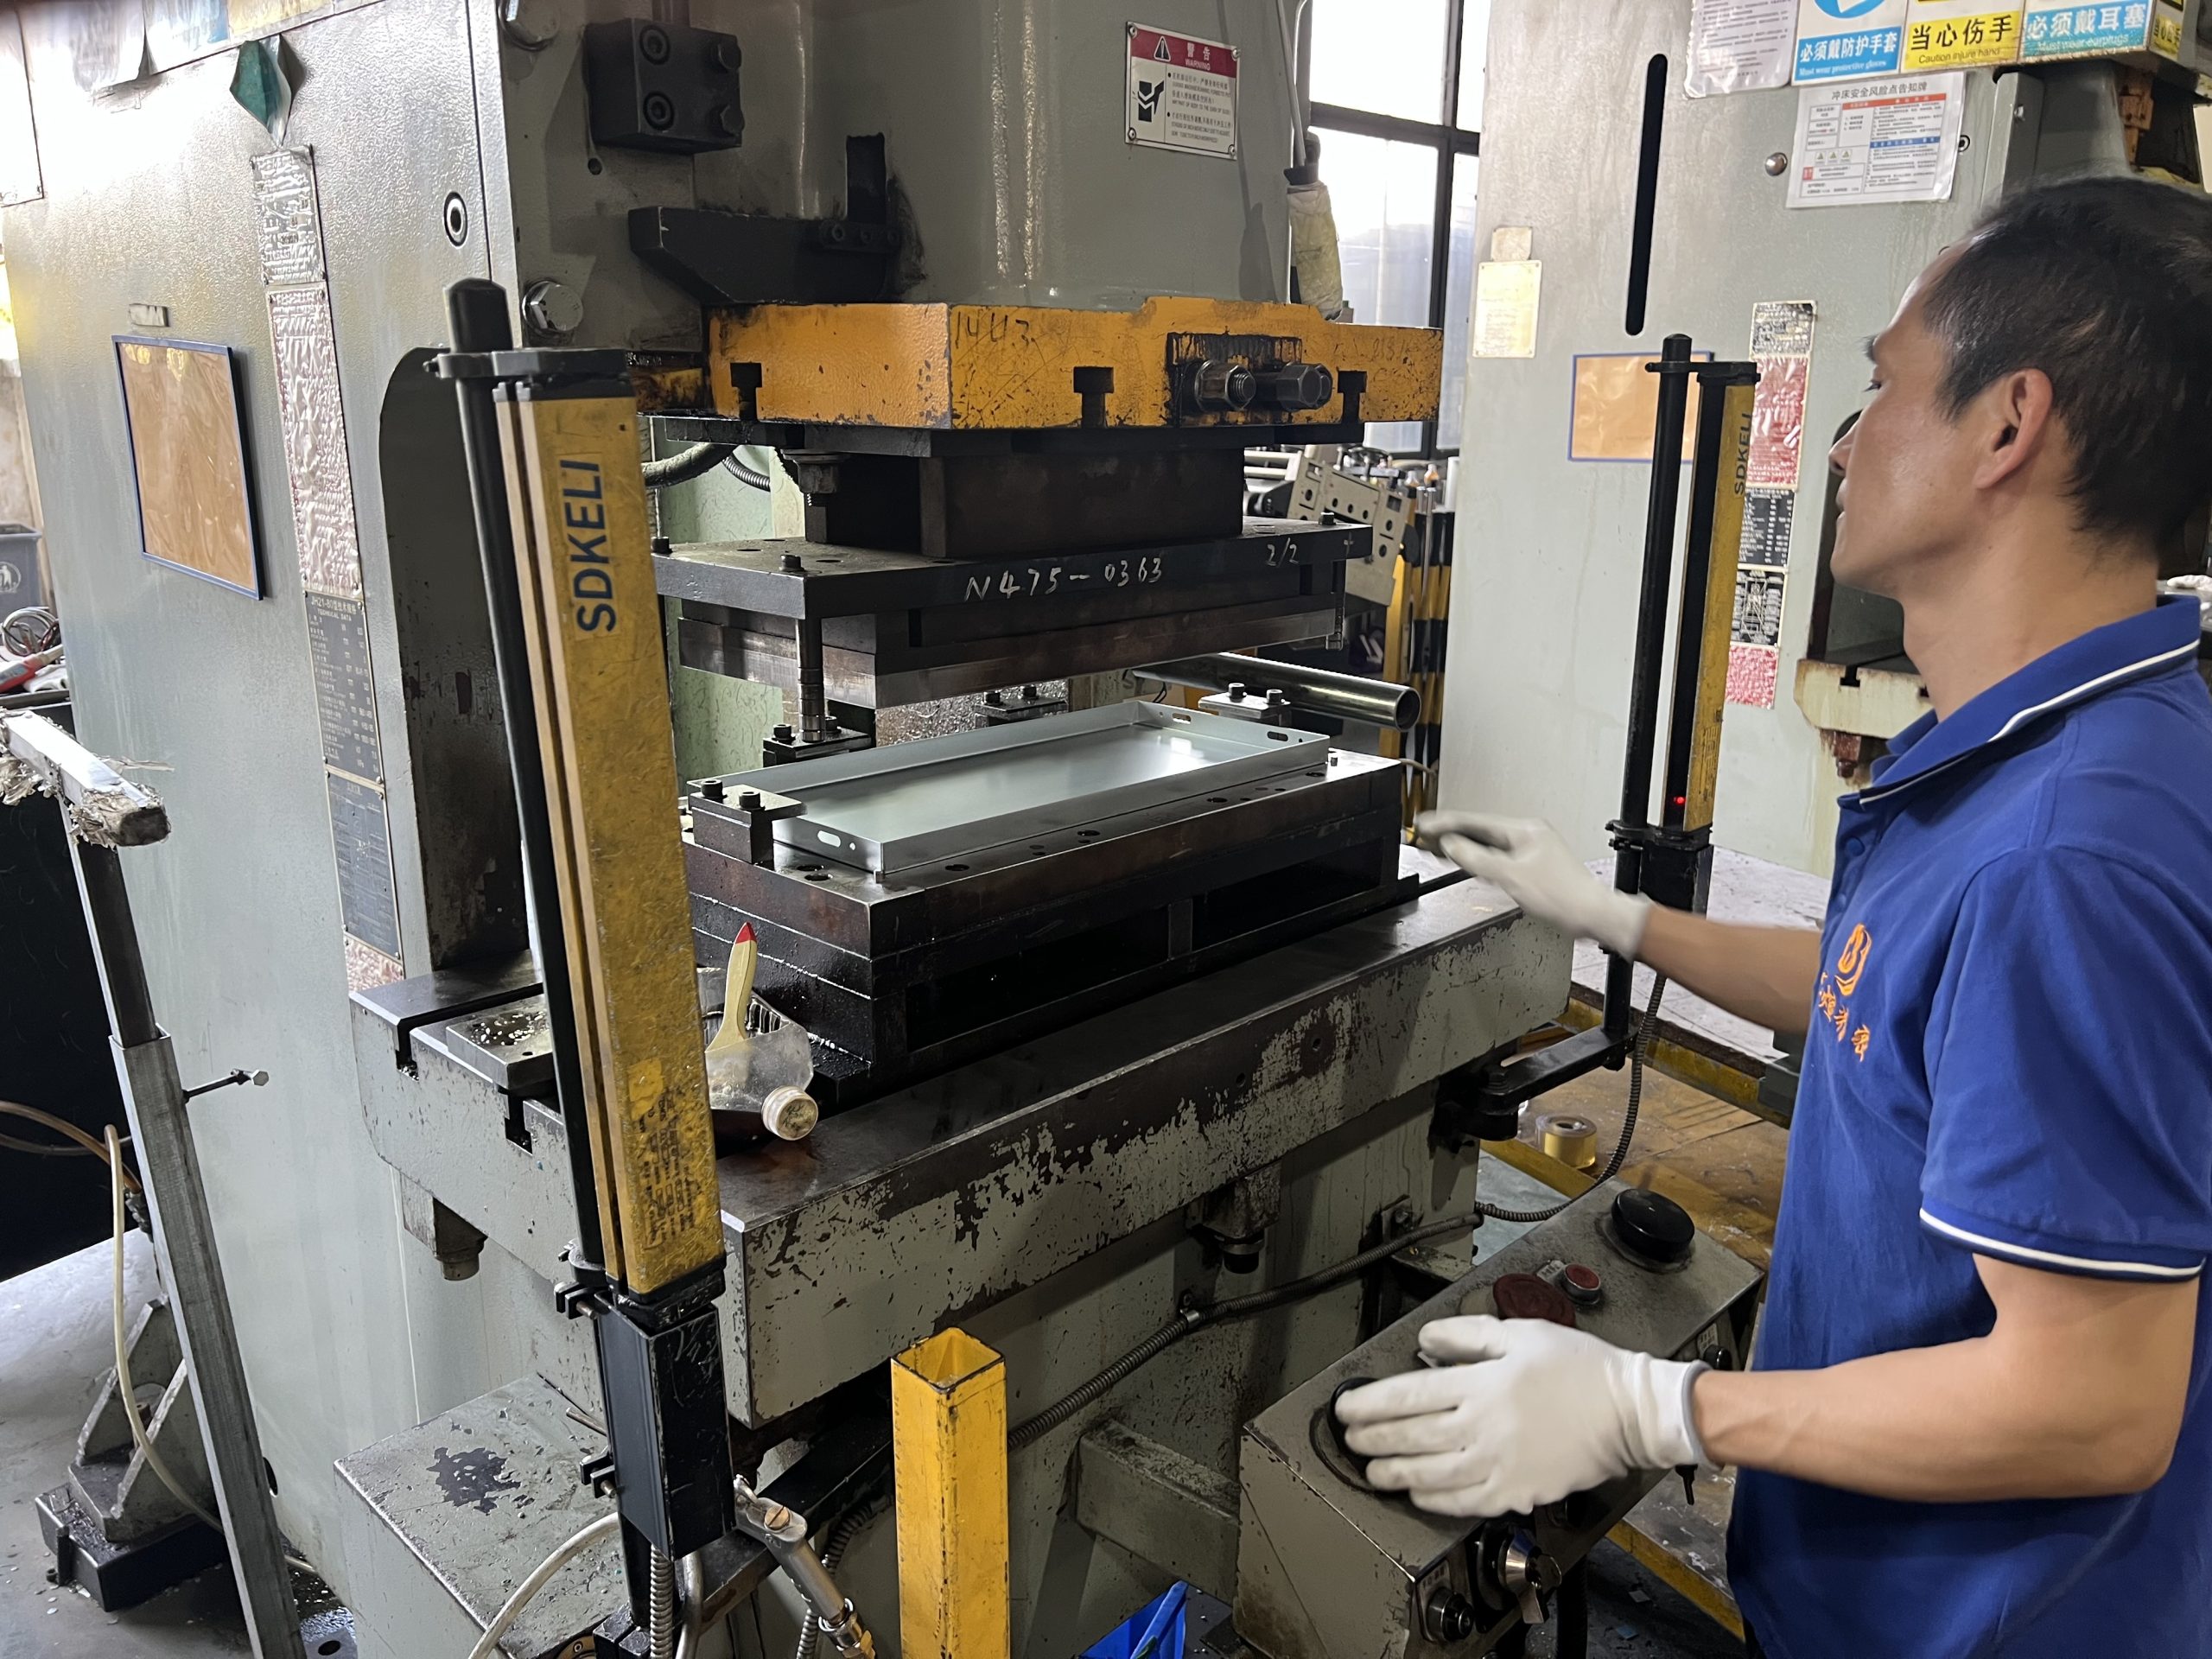
Working drawing of punching machine

Core Stamping Equipment

Common Materials & Thickness Range: Steel/Carbon Steel/Stainless Steel: ≤~5mm; Aluminum Alloy: ≤~6mm

Typical Cycle Time / Operating Stroke Range: 40-75 S.P.M (cycle time varies with die and material) Primary

Capabilities: Medium to heavy gauge sheet metal stamping, bending/forming, structural component processing

Common Materials & Thickness Range: Steel/Carbon Steel/Stainless Steel: ≤~4mm; Aluminum Alloy: ≤~5mm

Typical Cycle Time / Operating Stroke Range: 55-85 S.P.M (typical high-speed stamping range)

Primary Capabilities: Medium gauge punching, blanking, light forming

Common Materials & Thickness Range: Steel/Carbon Steel/Stainless Steel: ≤~3mm; Aluminum Alloy: ≤~4mm (general punching/bending)

Typical Cycle Time / Operating Stroke Range: 60-90 S.P.M (standard operating range, e.g., ~60 S.P.M)

Primary Capabilities: Punching, blanking, bending, riveting, and general sheet metal stamping processes

Common Materials & Thickness Range: Steel/Carbon Steel/Stainless Steel: ≤~6-8mm; Aluminum Alloy: ≤~8mm

Typical Cycle Time / Operating Stroke Range: 30-65 S.P.M (large-tonnage stamping range)

Primary Capabilities: Large sheet metal punching, bending, large part forming

Common Materials & Thickness Range: Steel/Carbon Steel/Stainless Steel: ≤~3mm; Aluminum Alloy: ≤~4mm

Typical Cycle Time / Operating Stroke Range: ~50-80 S.P.M

Primary Capabilities: Punching/blanking/bending for small to medium sheet metal parts

Common Materials & Thickness Range: Steel/Carbon Steel/Stainless Steel: ≤~4mm; Aluminum Alloy: ≤~5mm

Typical Cycle Time / Operating Stroke Range: ~40-70 S.P.M

Primary Capabilities: Easy die setup, punching, blanking/forming (small to medium parts)


Common Materials & Thickness Range: Steel/Carbon Steel/Stainless Steel: ≤~3mm; Aluminum Alloy: ≤~4mm

Typical Production Rate:
~80–150 parts/hour, depending on part geometry, drawing depth, material, and die configuration.

Primary Capabilities:
Deep drawing and forming of large or complex sheet metal parts, including enclosures, covers, housings, trays, and structural components.

+
Metal Stamping Capacity Benchmark Click to expand and view detailed 2024 actual production capacity data.

Our stamping capacity assessment is based on 2024 actual production data statistics. We evaluate equipment operating cycles, effective working hours, work order execution, and qualified output to provide realistic capacity planning rather than relying only on theoretical stroke rates.

Gerätemodell Quantity
(Units)
Typical Actual Output
(Units/Hour)
Daily Capacity
(Units/Day, 10 Hours)
Monatliche Kapazität
(Units/22 Days)
Applicable Product Category
Qianniu JH21-160 6 ~350–450 ~3,500–4,500 ~77,000–99,000 Medium / large stamping parts
Qianniu JH21-125 5 ~350–450 ~3,500–4,500 ~77,000–99,000 Medium-thick plate stamping parts
Qianniu JH21-80 4 ~350–450 ~3,500–4,500 ~77,000–99,000 General sheet metal stamping
Foshan Shengchuan JH21-63 3 ~350–450 ~3,500–4,500 ~77,000–99,000 Small-medium stamping parts
Foshan Shengchuan J23-40 4 ~350–450 ~3,500–4,500 ~77,000–99,000 Small-medium / inclined stamping
Qianniu JH21-250 2 ~350–450 ~3,500–4,500 ~77,000–99,000 Large / middle-thick stamping parts
Guangduo YA28-425 Four-Column Hydraulic Press 3 ~80–150
(Cycle-based deep forming)
~800–1,500 ~17,600–33,000 Deep drawing / edge blanking / complex forming
Note: Capacity data is based on 2024 actual production records. Final capacity depends on material grade, thickness, part geometry, die structure, forming complexity, tolerance requirements, and inspection standards.

Metal Stamping Overview

High-precision stamping solutions for reliable performance and mass production.

Metal stamping uses a press and matched tooling to cut, punch, form, or shape sheet metal into repeatable parts. It is ideal for OEM projects that require stable dimensions, high production efficiency, and consistent part quality across batches.

Metal Stamping Process
1

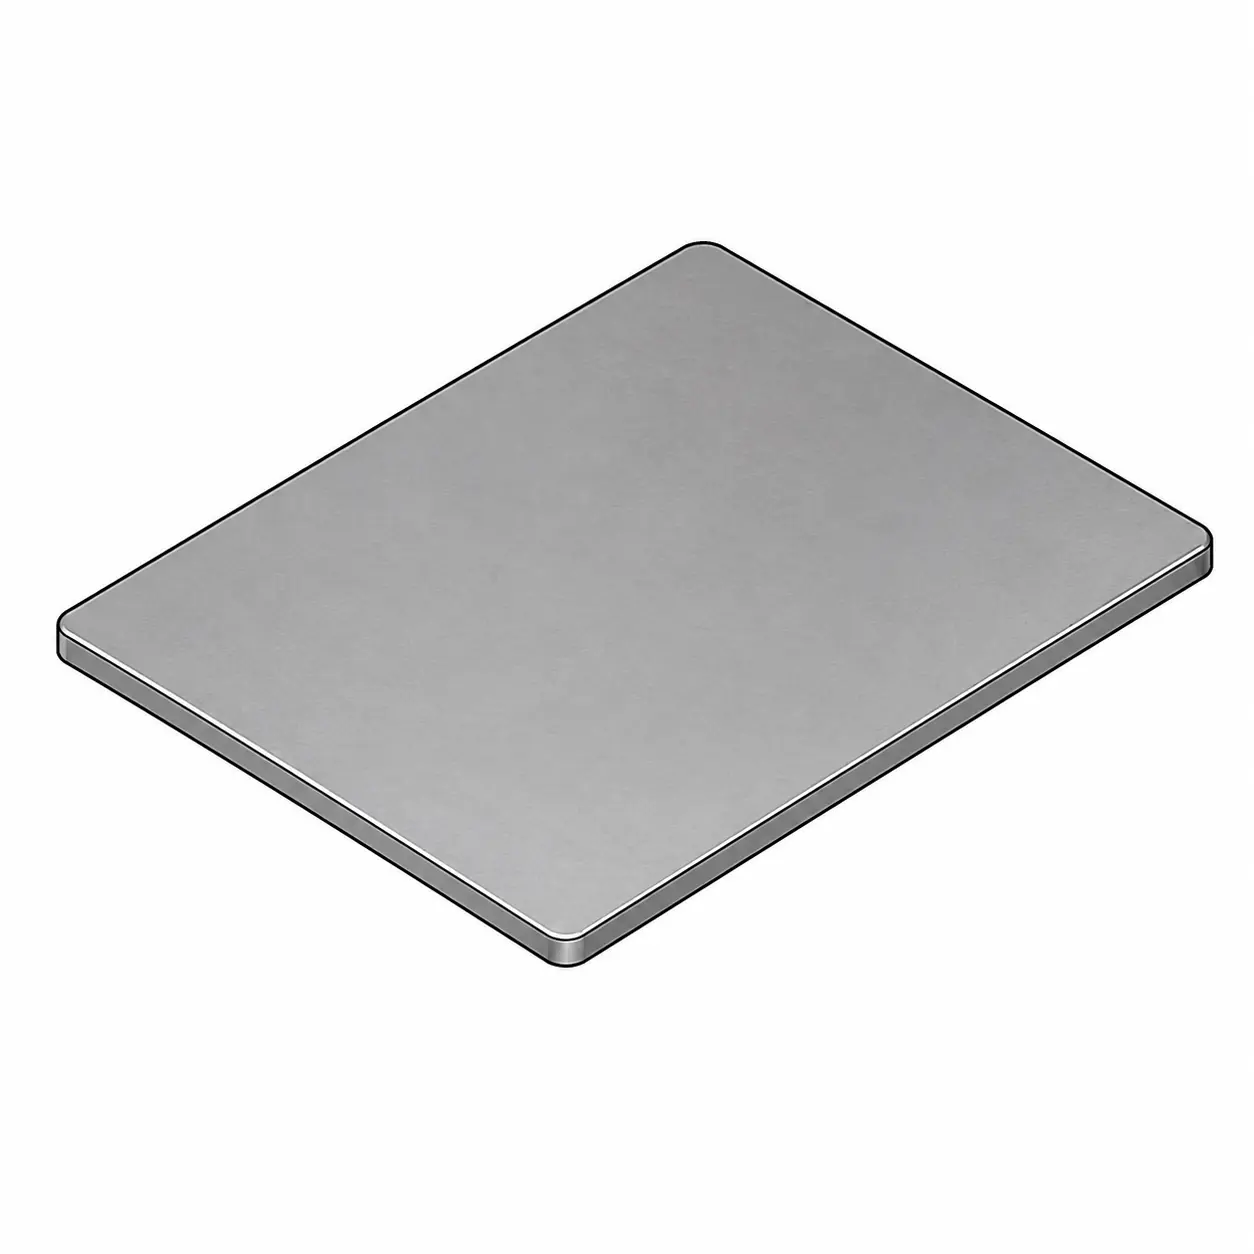
Flat Blank

Flat sheet metal blank

Sheet metal blank is prepared according to part design.

2

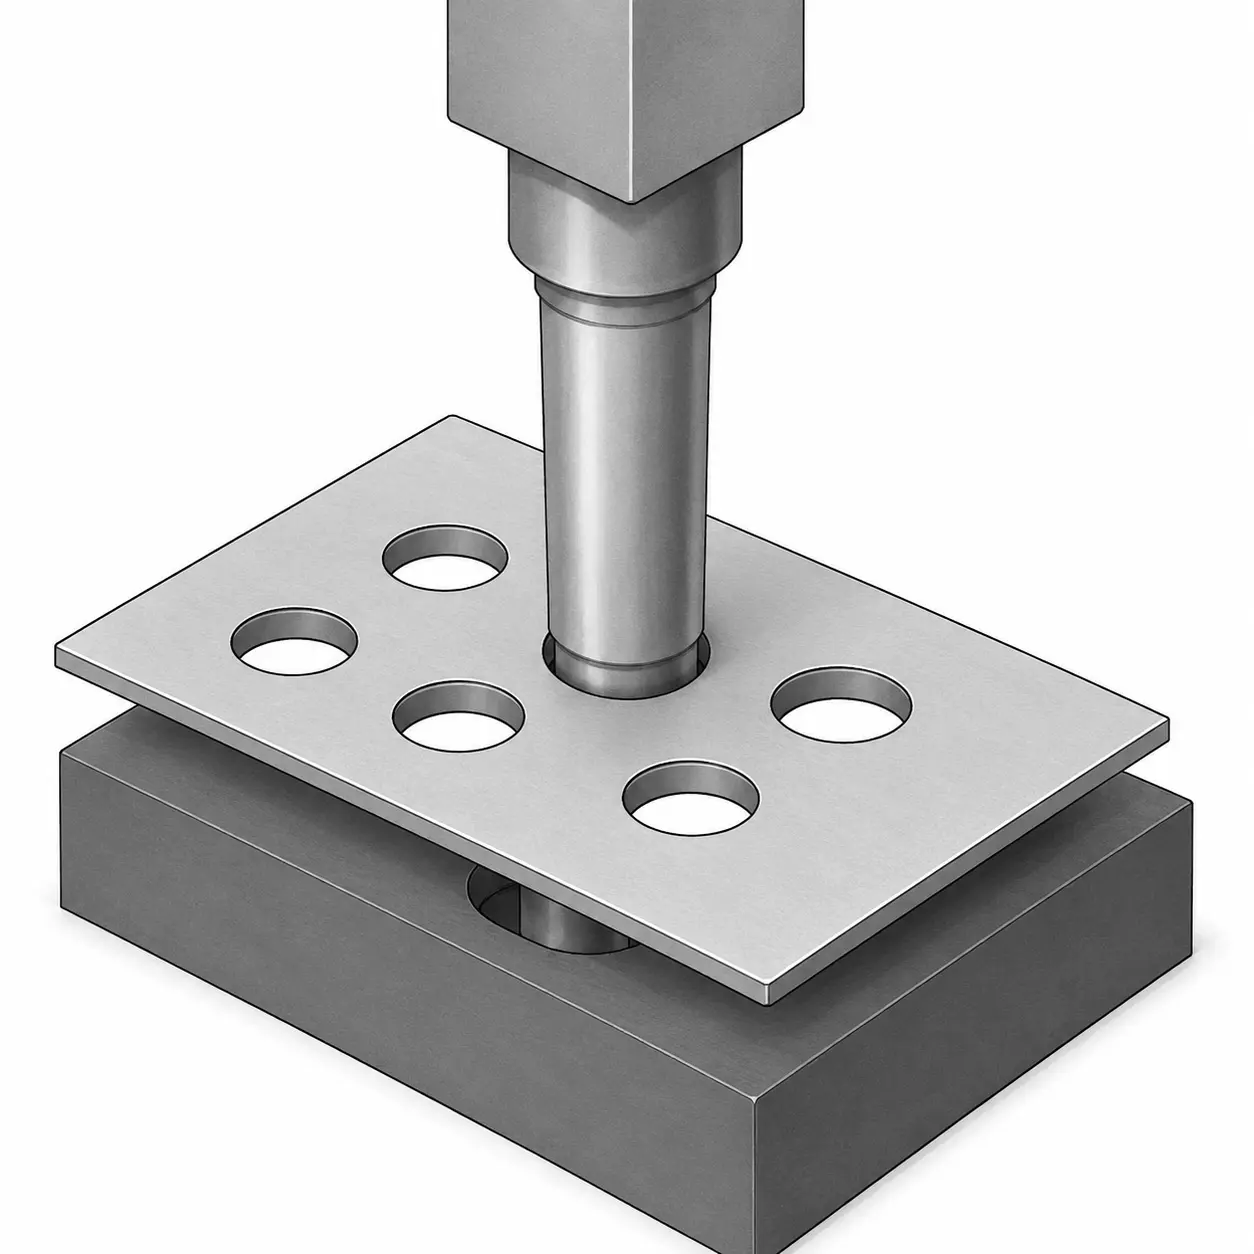
Punching

Punching sheet metal process

The punch and die cut or pierce the blank to create features.

3

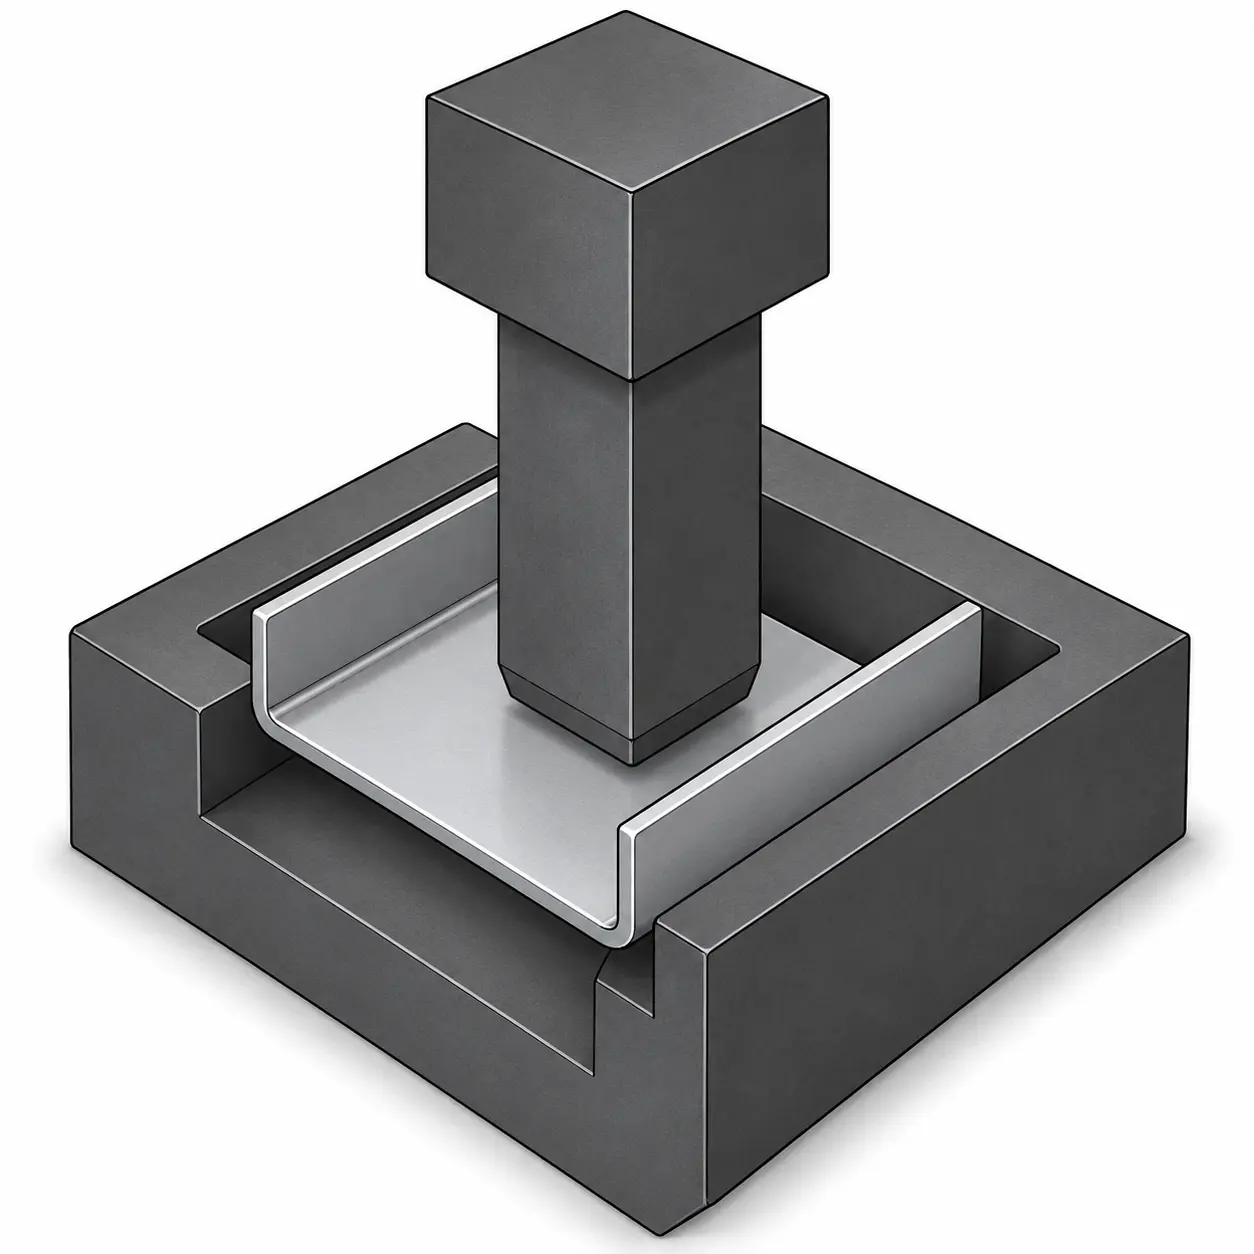
Forming

Sheet metal forming process

The material is formed into the required shape under pressure.

4

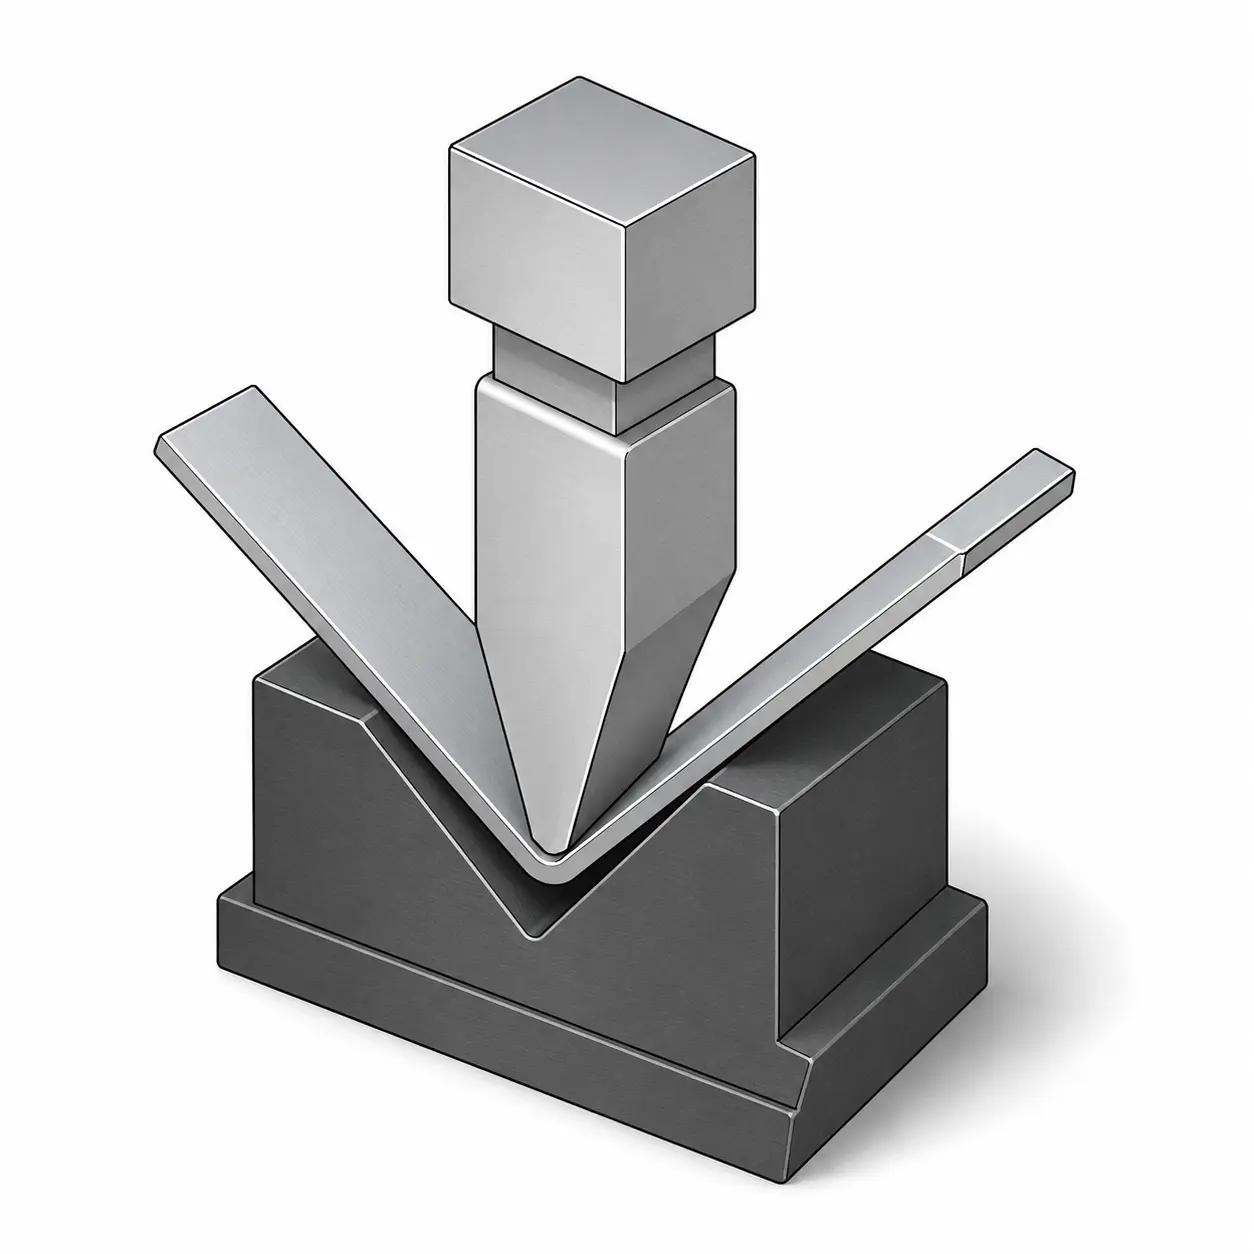
Flanging
or Bending

Sheet metal flanging or bending process

Edges are flanged or bent to add strength or assembly features.

5

Finished Part

Finished stamped sheet metal part

The stamped part is trimmed, inspected, and ready for assembly.

  • Cost-Effective for Volume
    Stamping is highly economical for mass production,offering low per-unit costs once tooling is established.

  • High Speed & Repeatability
    The process enables rapid production cycles andexcellent consistency across large batches.

  • Versatile Part Geometry
    It can produce a wide range of part geometries,from simple brackets to complex structural components.

  • Tooling Investment
    Custom dies require significant upfront investment,making the process less suitable for low-volumeor prototype work.

  • Design Change Control
    Once tooling is fabricated, design changes aredifficult and expensive to implement.

  • Material Consistency
    Part quality depends heavily on material consistency;variations in thickness or surface can lead to defectsand higher scrap rates.

Types of Metal Stamping

Custom Metal Stamping Built Around Your Drawings

Based on your drawings, part geometry, tolerance requirements, order volume, and lead time, SR MFG selects the most suitable stamping process and die strategy. For suitable production programs, stamping, bending, localized forming, and related operations can be integrated into a streamlined process to reduce handling, improve consistency, shorten lead times, and lower per-piece cost by 10–15%.
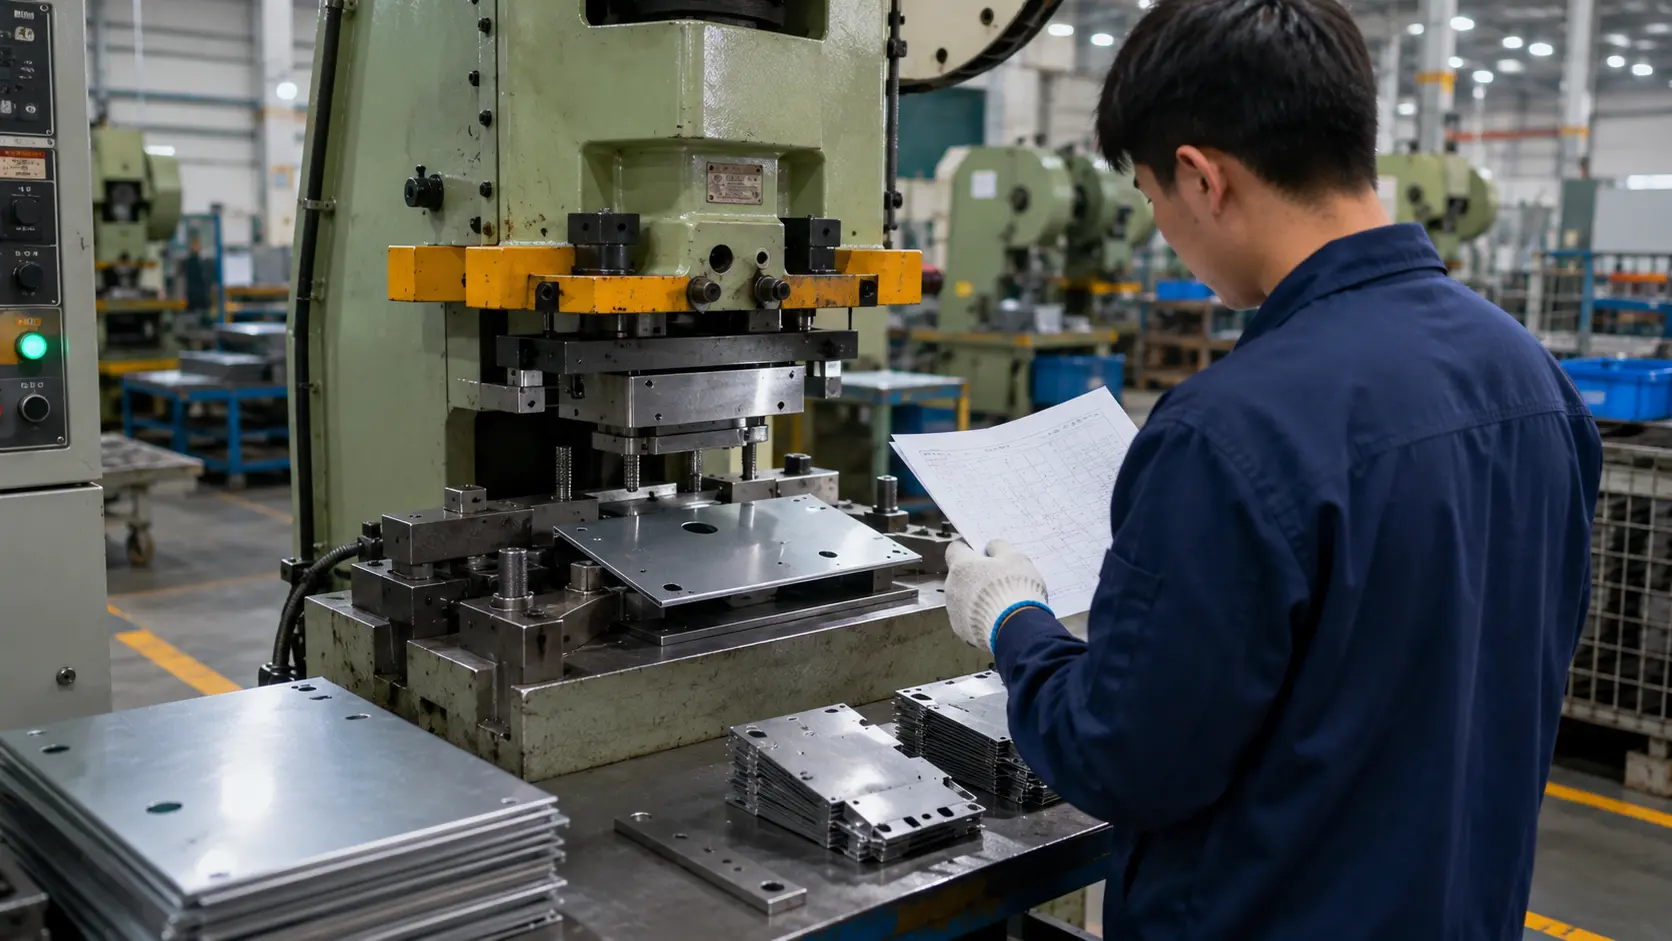
01
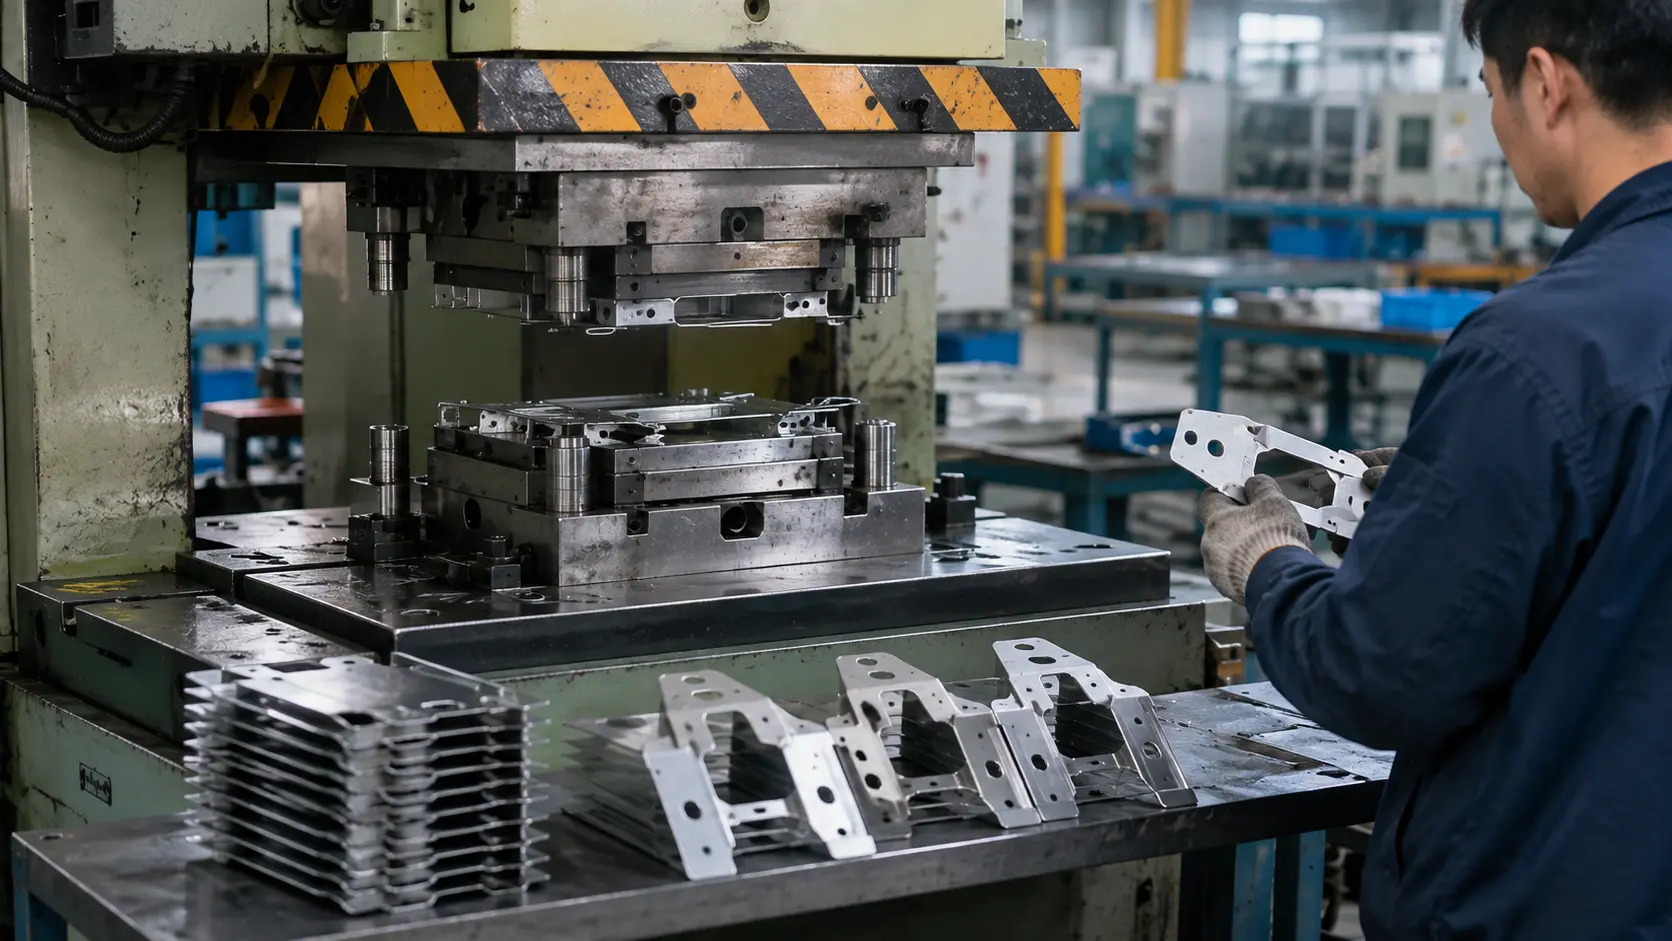
Single-operation stamping process for simple sheet metal parts

Single-Operation Stamping

Single-operation stamping uses one press stroke to complete one process, such as punching, blanking, trimming, or simple bending. It is suitable for simple parts, prototype validation, low-to-medium volume orders, or projects that require flexible tooling and faster design adjustments.

View Single-Operation Stamping →
02
Compound stamping process for combined punching and blanking operations

Compound Stamping

Compound stamping completes two or more operations in one press stroke, such as punching and blanking, or cutting and localized forming. It helps improve dimensional consistency, reduce secondary handling, and is suitable for parts with stable designs and medium-volume production requirements.

View Compound Stamping →
03
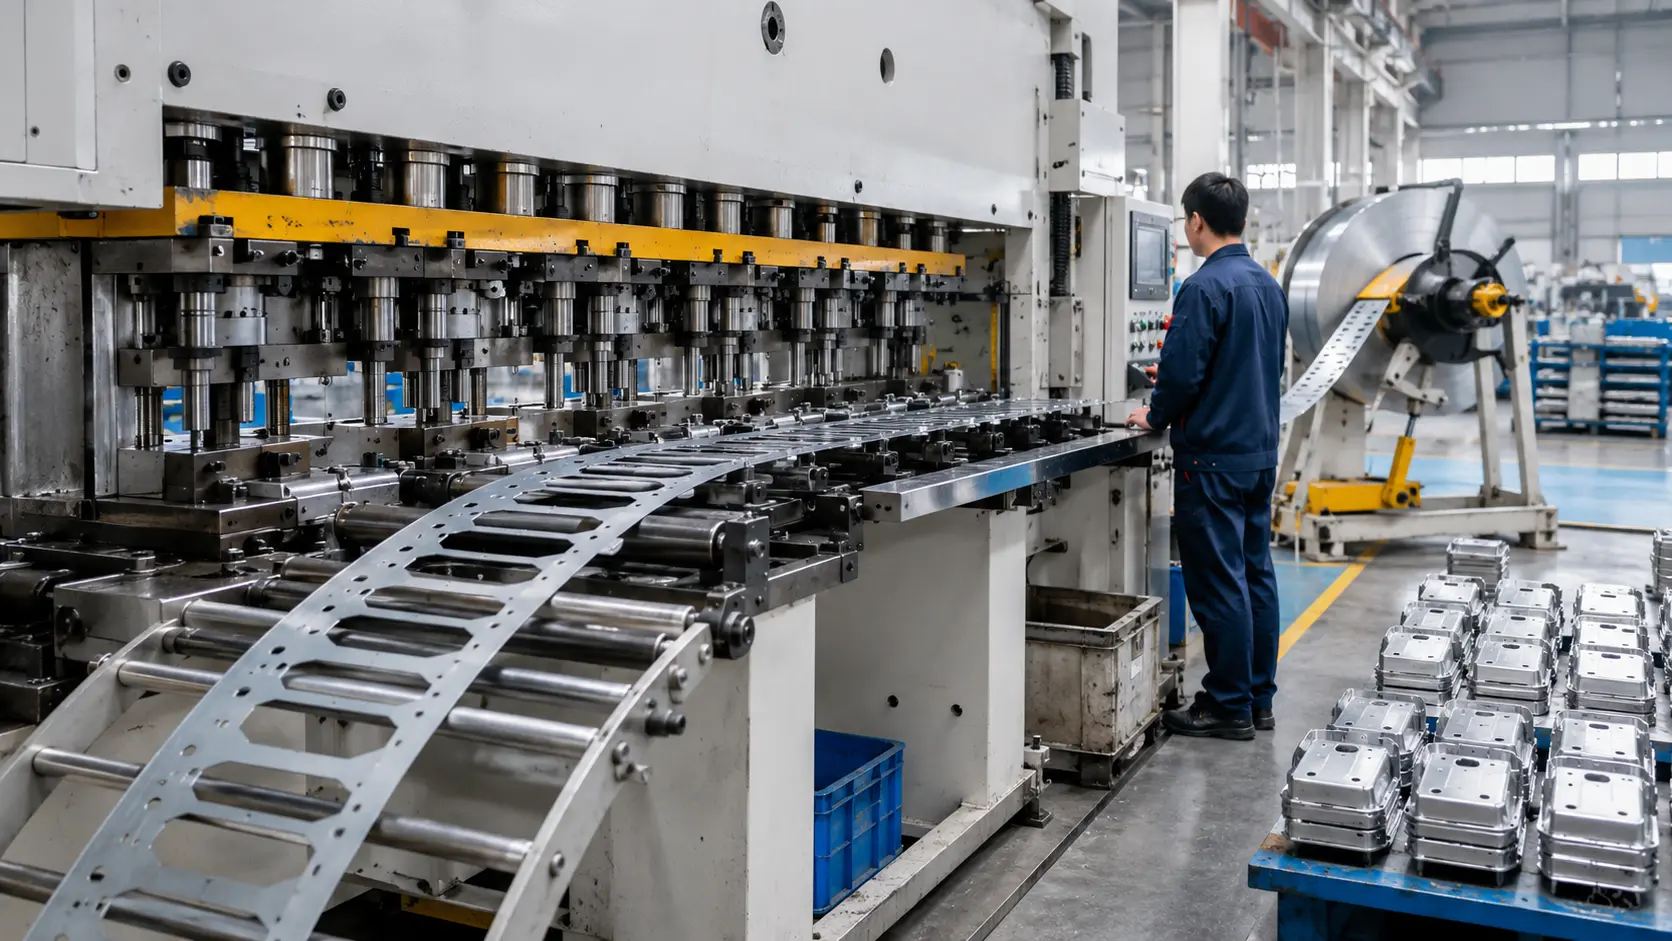
Progressive die stamping process with strip feed for high-volume production

Progressive Die Stamping

Progressive die stamping feeds strip material through multiple stations in one die. Each press stroke completes part of the process until the final part is formed. It is ideal for repeat parts, high-volume production, stable tolerances, and lower per-piece cost after tooling approval.

View Progressive Die Stamping →

Common Stamping Operations We Support

From basic cutting to complex forming, our stamping capabilities cover a wide range of operations to meet your product requirements and performance goals.
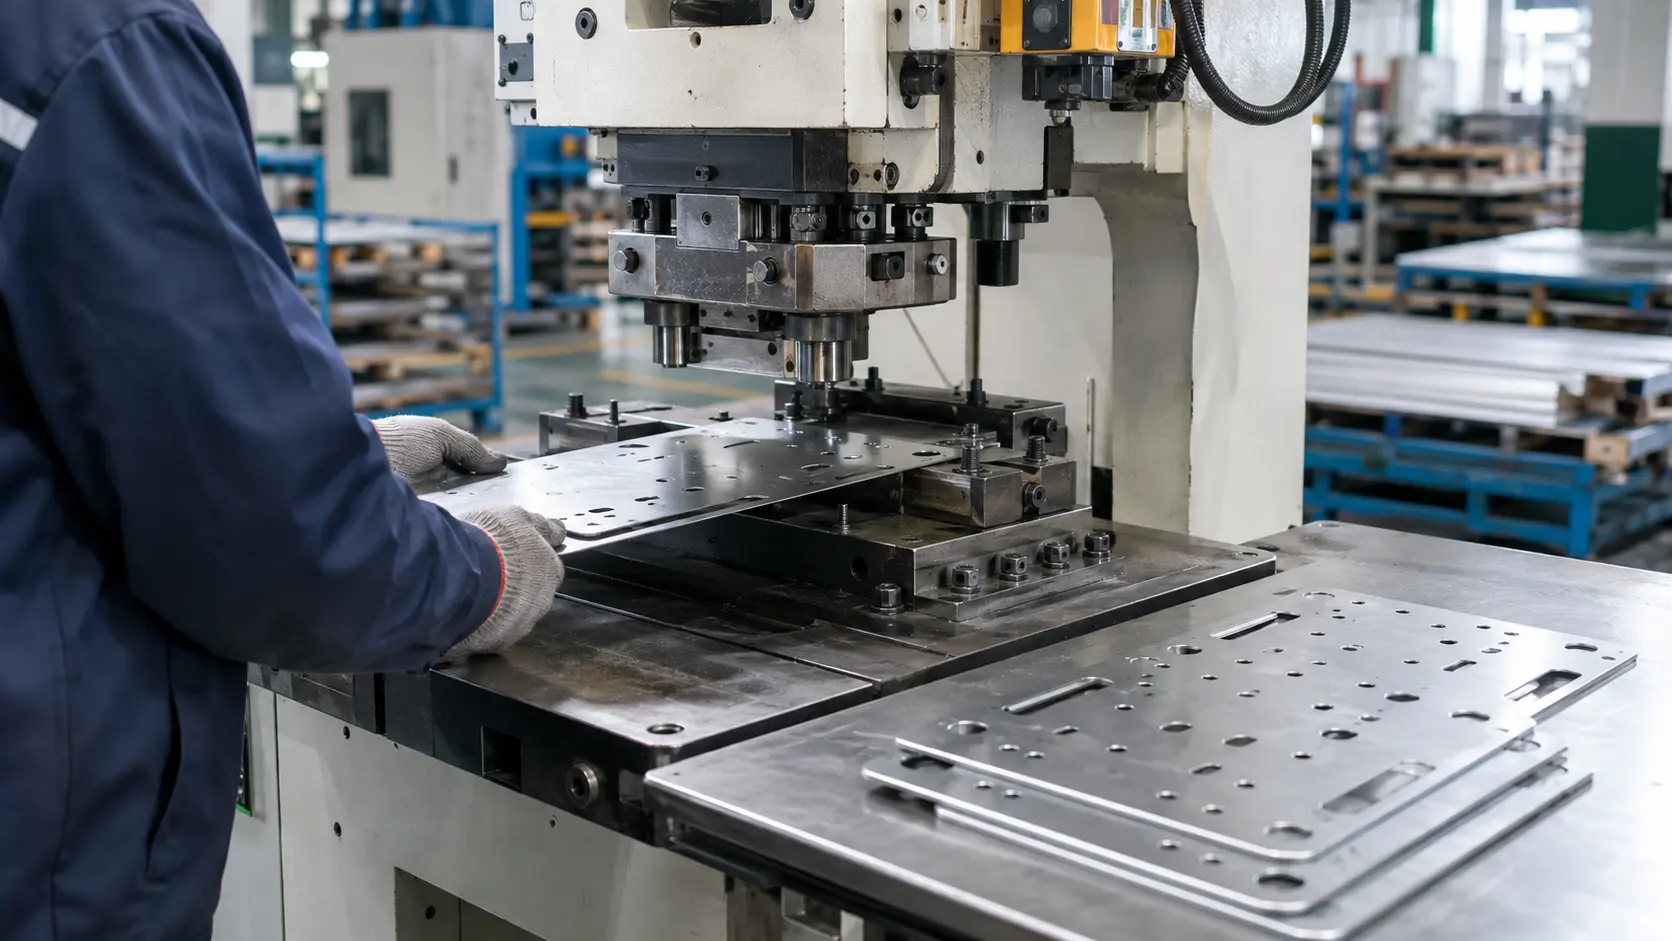
Punching metal stamping process

Punching

Punching uses a punch and die to create holes, slots, or cutouts in sheet metal. It is ideal for ventilation holes, mounting holes, slots, and other functional features.
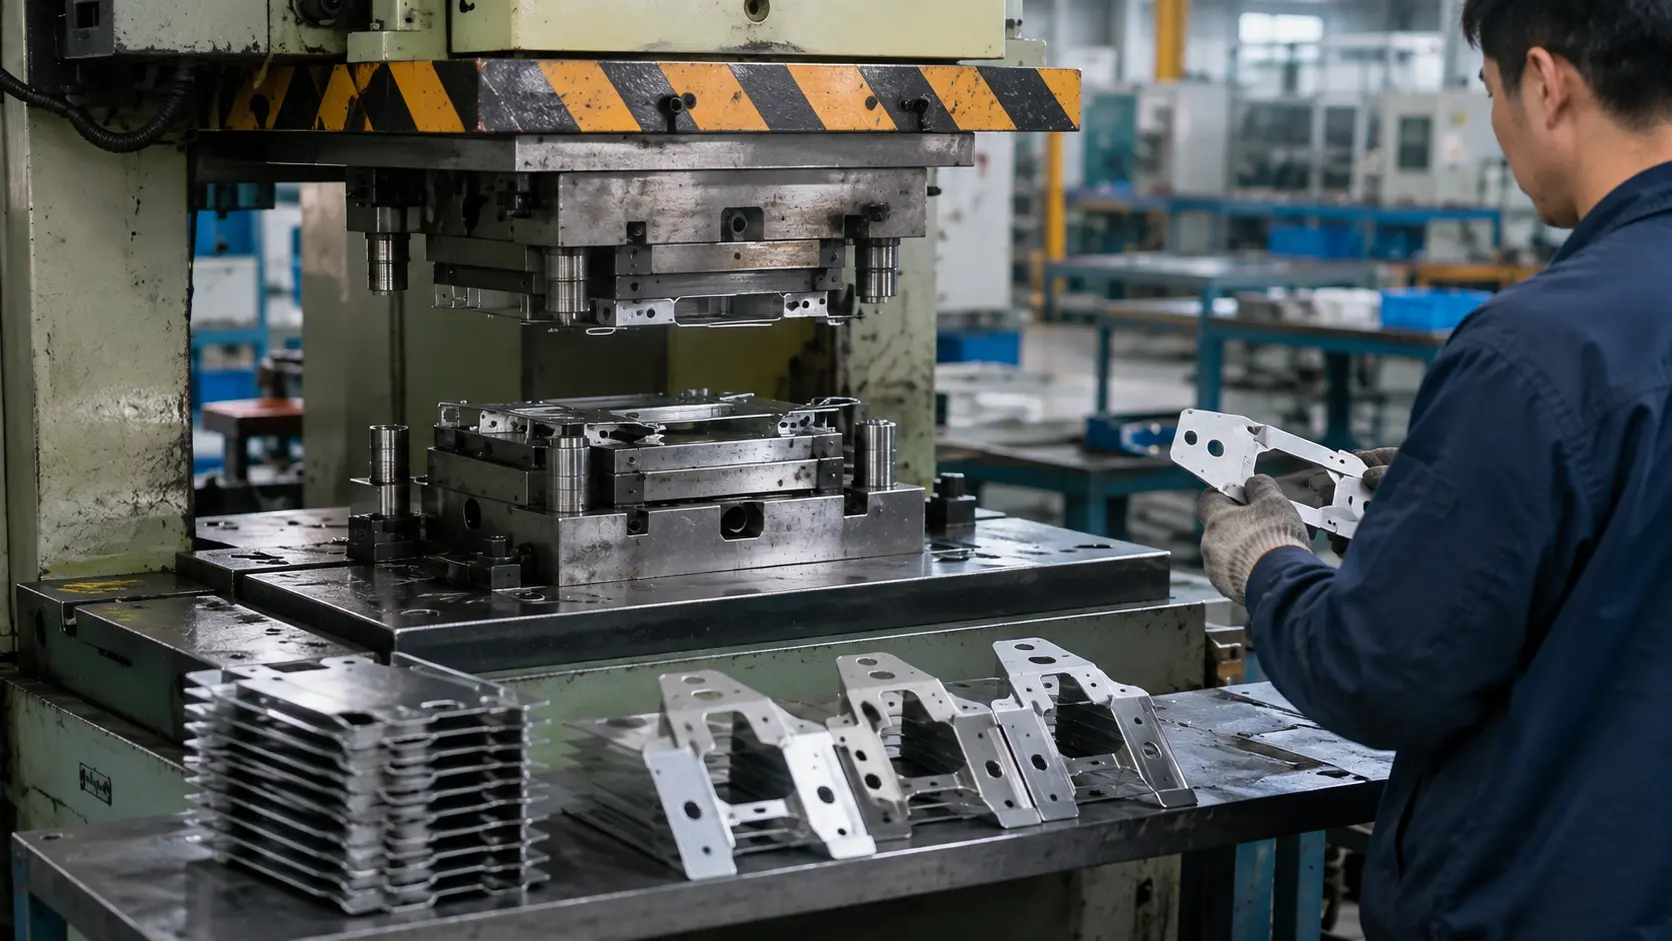
Blanking metal stamping process

Blanking

Blanking cuts the sheet or coil material along a closed contour to produce the required flat shape or profile. It ensures clean edges and consistent dimensions.
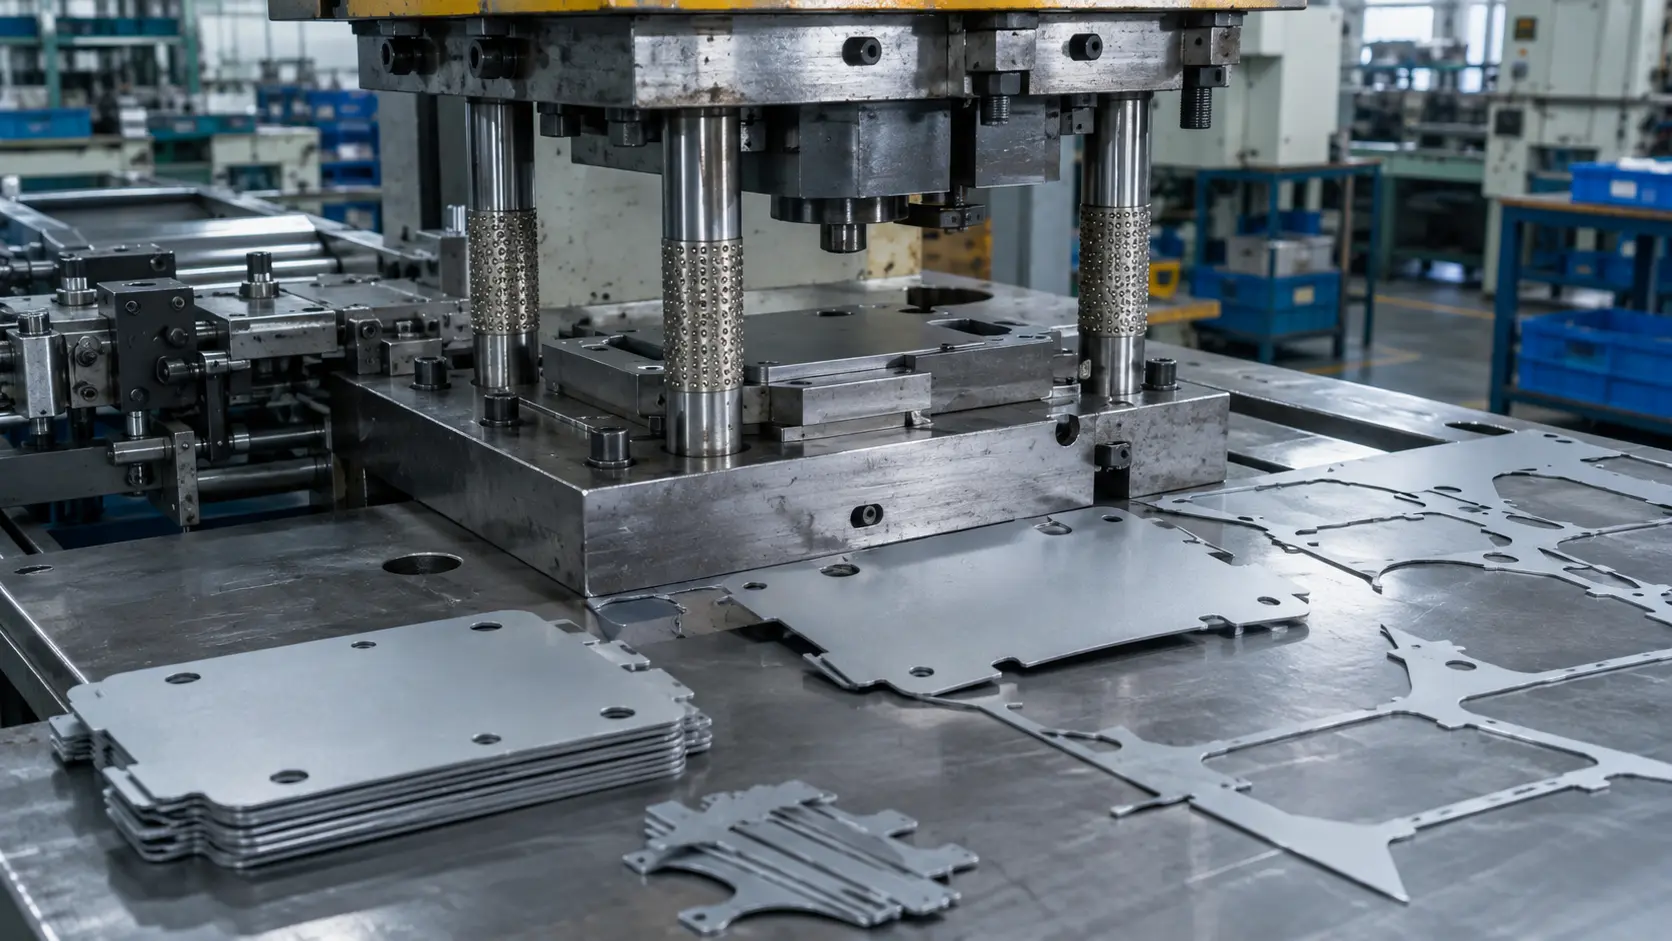
Flanging metal stamping process

Flanging

Flanging forms a raised edge along a hole or part perimeter to increase stiffness, improve alignment during assembly, or create surfaces for fastening, sealing, or reinforcement.
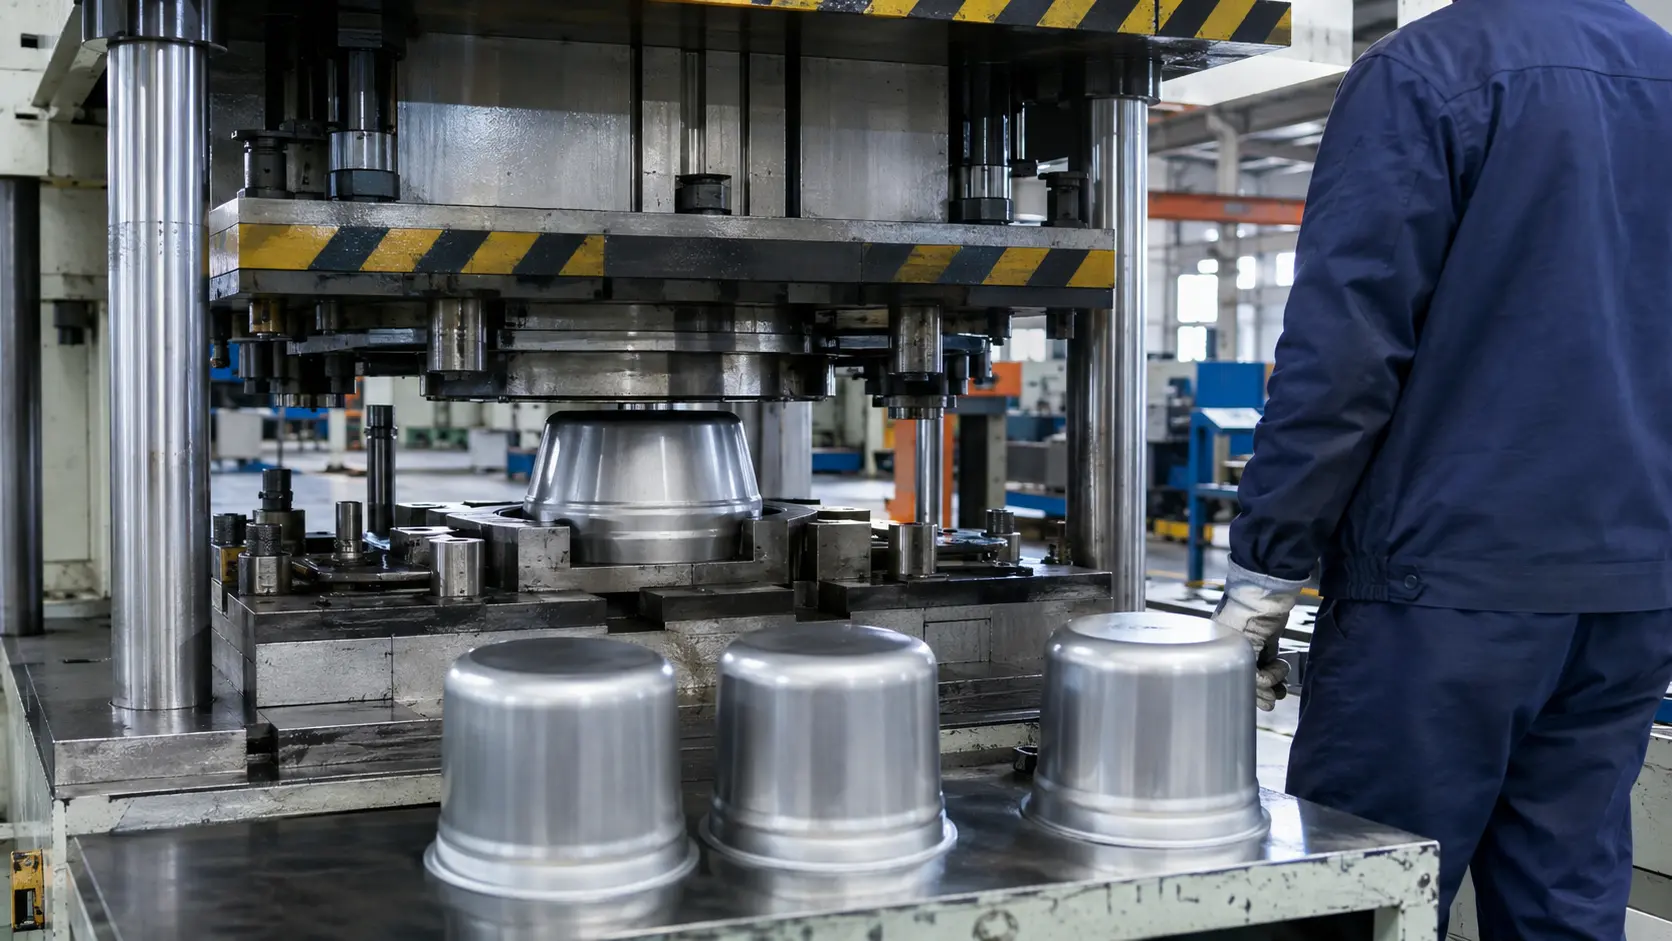
Deep drawing metal stamping process

Deep Drawing

Deep drawing forms sheet metal into three-dimensional shapes such as cups, enclosures, or housings. It is suitable for parts that require high strength and seamless walls.

Send us your drawings for process review and tooling recommendation.

Common Types of Stamped Parts 

  • Brackets

  • Plates

  • Stiffeners

  • Connectors

  • Metal housings

  • Metal enclosures

  • Paneele

  • Mounting frames

  • Structural supports

  • Fasteners

  • Retaining clips

  • And Perforated Filters And Screens

General Tolerance Reference for Metal Stamping

For dimensions without individually specified tolerances, ISO 2768-1 Class m can be used as a general reference when applicable. Final tolerances depend on part geometry, material thickness, tooling structure,forming complexity, and inspection requirements.

Linear Dimensions
+
Nominal Length L (mm) Default Tolerance (±mm)
0.5 – 60.10
>6 – 300.20
>30 – 1200.30
>120 – 4000.50
>400 – 10000.80
>1000 – 20001.20
>2000 – 40002.00
Angular Dimensions
+
Short Side Length L (mm) Default Angle Tolerance
≤10±1°
>10 – 50±0°30′
>50 – 120±0°20′
>120 – 400±0°10′
>400±0°5′
Outer Radius & Chamfer
+
R or C (mm) Default Tolerance (±mm)
0.5 – 30.20
>3 – 60.50
>6 – 301.00
i
Reference only. Project-specific tolerances should be confirmed based on drawings, materials, tooling, process conditions, and inspection requirements.

Metal Stamping Materials

Material selection directly impacts stamping feasibility, die life, dimensional stability, and total manufacturing cost over the long run. SR MFG supports a wide range of commonly used industrial stamping materials. Early in the project, we review your part geometry, strength requirements, and production volume to help you choose a material option that is stable and scalable for mass production.

Materials We Commonly Use for Metal Stamping

Common materials used in metal stamping include carbon steel, galvanized steel, aluminum alloys, stainless steel, and specialty coated steel.
Material selection should consider sheet thickness, stamping process type, die clearance, forming requirements, and downstream surface finishing. These factors directly affect forming quality, dimensional stability, tooling performance, production efficiency, and final part appearance.

  • Kohlenstoffstahl

  • Verzinkter Stahl

  • Aluminiumlegierungen

  • Edelstähle

  • Speziell beschichtete Stähle

Kohlenstoffstahl

Typical stampable thickness: 0.5–3.2 mm

Suitable processes: punching / blanking / bending / flanging / embossing; light deep drawing is possible

High-volume long-term production: Excellent fit

Impact on tooling & cost: Low material cost, stable supply, and a wide stamping process window; relatively die-friendly for long-term production

Forming risks & design limits: Control burr direction, hole-to-edge distance, minimum flange height, bend radius, and flatness after forming

Surface & downstream compatibility: Smooth surface; compatible with powder coating, painting, plating, electrophoresis, welding, and deburring

View cold-rolled steel material details →

Typical stampable thickness: 0.5–3.0 mm

Suitable processes: punching / blanking / bending / forming / shallow drawing / progressive die stamping

High-volume long-term production: Excellent fit

Impact on tooling & cost: Very cost-effective and easy to process; suitable for high-volume stamped brackets, clips, covers, and general sheet metal parts

Forming risks & design limits: Avoid overly tight bend radii, narrow slots, and sharp internal corners; springback is usually manageable

Surface & downstream compatibility: Compatible with painting, powder coating, plating, welding, and assembly operations

Typical stampable thickness: 1.5–6.0 mm

Suitable processes: blanking / punching / bending / flanging / forming / heavy-duty stamping

High-volume long-term production: Good fit for medium to thick stamped parts

Impact on tooling & cost: Lower cost than many alloy materials; thicker gauges increase press tonnage and die load

Forming risks & design limits: Edge quality, scale removal, hole deformation, and bend cracking should be controlled, especially in thicker parts

Surface & downstream compatibility: Better surface condition than ordinary hot rolled steel; compatible with painting, powder coating, welding, and zinc plating after cleaning

Typical stampable thickness: 1.5–6.0 mm

Suitable processes: blanking / punching / bending / forming / structural stamping

High-volume long-term production: Good fit when strength and weight reduction are important

Impact on tooling & cost: Higher strength can reduce part thickness, but increases die load, tool wear, and forming force

Forming risks & design limits: Higher springback and greater cracking risk than mild steel; bend radius, grain direction, and forming sequence should be reviewed carefully

Surface & downstream compatibility: Compatible with powder coating, painting, welding, and galvanizing; cleaning and edge deburring are recommended

Verzinkte Materialien

Typical stampable thickness: 0.5–3.2 mm

Suitable processes: punching / blanking / bending / flanging / embossing / light forming

High-volume long-term production: Excellent fit for corrosion-resistant stamped parts

Impact on tooling & cost: Cost-effective material with good corrosion protection; zinc coating may increase die maintenance requirements over long runs

Forming risks & design limits: Coating damage, powdering, galling, and cracking at tight bends should be controlled; avoid overly aggressive forming

Surface & downstream compatibility: Compatible with powder coating, painting, spot welding, and assembly; cut edges and formed areas may need corrosion protection

View hot-dip galvanized steel material details →

Typical stampable thickness: 0.5–2.5 mm

Suitable processes: punching / blanking / bending / flanging / precision stamping / light forming

High-volume long-term production: Excellent fit for cabinets, enclosures, appliance parts, and precision stamped panels

Impact on tooling & cost: More uniform coating than hot-dip galvanized steel; good for stable appearance and controlled stamping performance

Forming risks & design limits: Coating scratches, burrs, and tight bend cracking should be controlled; not ideal for very heavy forming

Surface & downstream compatibility: Good surface for painting, powder coating, electrophoresis, spot welding, and plated assemblies

View electro-galvanized steel material details →

Typical stampable thickness: 0.6–3.0 mm

Suitable processes: punching / blanking / bending / flanging / embossing / automotive stamping

High-volume long-term production: Excellent fit for stamped parts requiring painting after forming

Impact on tooling & cost: Good balance between corrosion protection, weldability, and paint adhesion; coating behavior should be considered in die design

Forming risks & design limits: Coating powdering may occur in severe forming; bend radius, forming depth, and die surface condition should be controlled

Surface & downstream compatibility: Excellent compatibility with painting, powder coating, electrophoresis, and spot welding

Aluminiumlegierungen

Typical stampable thickness: 0.5–4.0 mm

Suitable processes: punching / blanking / bending / flanging / embossing / moderate forming

High-volume long-term production: Good fit for lightweight stamped parts with corrosion resistance requirements

Impact on tooling & cost: Higher material cost than carbon steel; softer material reduces some die wear but requires control of galling and surface scratches

Forming risks & design limits: Springback, cracking at tight bends, and surface marking should be controlled; bend radius should be larger than mild steel

Surface & downstream compatibility: Compatible with anodizing, powder coating, brushing, polishing, welding, and adhesive bonding

View 5052-H32 aluminum material details →

Typical stampable thickness: 0.5–3.0 mm

Suitable processes: punching / blanking / bending / flanging / embossing / light deep drawing

High-volume long-term production: Good fit for light-duty stamped aluminum parts

Impact on tooling & cost: More economical than many structural aluminum alloys; easy to form and relatively friendly to stamping dies

Forming risks & design limits: Low strength limits load-bearing use; surface scratches and deformation should be controlled during forming

Surface & downstream compatibility: Compatible with anodizing, powder coating, painting, polishing, and light welding

View 3003 aluminum material details →

Typical stampable thickness: 0.3–2.5 mm

Suitable processes: punching / blanking / bending / embossing / shallow drawing / soft aluminum forming

High-volume long-term production: Good fit for non-structural stamped parts

Impact on tooling & cost: Good formability and moderate material cost; soft material may require careful control of die clearance and surface protection

Forming risks & design limits: Low mechanical strength; easy to dent, scratch, or deform if handling and die surface are not well controlled

Surface & downstream compatibility: Compatible with anodizing, polishing, brushing, painting, and powder coating

View 1060 / 1100 aluminum material details →

Typical stampable thickness: 0.8–4.0 mm

Suitable processes: punching / blanking / bending / flanging / forming / automotive and transportation stamping

High-volume long-term production: Good fit for stamped aluminum parts requiring better strength and corrosion resistance

Impact on tooling & cost: Higher material cost than 3003; good balance of formability, strength, and corrosion resistance

Forming risks & design limits: Springback and bend cracking should be controlled; forming direction and bend radius are important for stable production

Surface & downstream compatibility: Compatible with anodizing, powder coating, painting, brushing, polishing, and welding

Typical stampable thickness: 1.0–4.0 mm

Suitable processes: punching / blanking / bending with larger radius / light forming / structural stamped parts

High-volume long-term production: Suitable only when forming severity is controlled

Impact on tooling & cost: Higher material cost and narrower forming window than 5052 or 3003; better for structural parts with limited deformation

Forming risks & design limits: Higher cracking risk and springback; not ideal for deep drawing or tight-radius forming in T6 temper

Surface & downstream compatibility: Compatible with anodizing, powder coating, machining, brushing, and assembly operations

View 6061-T6 aluminum material details →

Edelstähle

Typical stampable thickness: 0.4–3.0 mm

Suitable processes: punching / blanking / bending / flanging / embossing / moderate deep drawing

High-volume long-term production: Good fit for corrosion-resistant stamped parts

Impact on tooling & cost: Higher material cost and higher tool wear than carbon steel; requires proper die material, clearance, and lubrication

Forming risks & design limits: Work hardening, springback, burr height, and surface scratching should be controlled during stamping

Surface & downstream compatibility: Compatible with brushing, polishing, passivation, bead blasting, welding, and assembly

View 304 stainless steel material details →

Typical stampable thickness: 0.4–3.0 mm

Suitable processes: punching / blanking / bending / flanging / embossing / moderate forming

High-volume long-term production: Good fit for corrosion-critical stamped parts

Impact on tooling & cost: Higher material and tooling cost than 304; more demanding on lubrication and tool wear control

Forming risks & design limits: Work hardening and springback are stronger than mild steel; sharp corners and tight bends should be avoided

Surface & downstream compatibility: Compatible with polishing, passivation, bead blasting, electropolishing, welding, and sanitary finishing

View 316L stainless steel material details →

Typical stampable thickness: 0.4–2.5 mm

Suitable processes: punching / blanking / bending / flanging / embossing / light forming

High-volume long-term production: Good fit for cost-sensitive stainless stamped parts

Impact on tooling & cost: Lower material cost than 304; harder than mild steel and still requires proper die clearance and lubrication

Forming risks & design limits: Lower corrosion resistance than 304; cracking, springback, and surface marking should be controlled

Surface & downstream compatibility: Compatible with brushing, polishing, bead blasting, passivation, and light welding

View 201 stainless steel material details →

Typical stampable thickness: 0.4–2.5 mm

Suitable processes: punching / blanking / bending / flanging / embossing / shallow forming

High-volume long-term production: Good fit for decorative and appliance stamped parts

Impact on tooling & cost: Lower cost than 304; moderate tool wear, suitable for high-volume flat and shallow-formed parts

Forming risks & design limits: Lower ductility than 304; not ideal for deep drawing or severe forming; bend cracking should be checked

Surface & downstream compatibility: Compatible with brushing, polishing, bead blasting, and decorative finishing

View 430 stainless steel material details →

Typical stampable thickness: 0.2–2.0 mm

Suitable processes: precision stamping / blanking / bending / spring clips / formed elastic parts

High-volume long-term production: Excellent fit for precision stamped spring-like components

Impact on tooling & cost: Higher strength improves part performance but increases forming force, springback, and tool wear

Forming risks & design limits: Strong work hardening and springback; bend radius, grain direction, and forming sequence must be carefully controlled

Surface & downstream compatibility: Compatible with polishing, passivation, precision deburring, and assembly operations

Typical stampable thickness: 0.5–3.0 mm

Suitable processes: punching / blanking / bending / flanging / forming / automotive stamping

High-volume long-term production: Good fit for automotive, exhaust, and heat-related stamped parts

Impact on tooling & cost: More cost-effective than 304 for heat-related applications; suitable for stamped parts where decorative appearance is not the main requirement

Forming risks & design limits: Formability is lower than 304 in some applications; cracking, edge quality, and bend performance should be checked

Surface & downstream compatibility: Compatible with welding, brushing, passivation, and heat-resistant assemblies

Note: Recommended stamping thickness and forming parameters depend on material grade, hardness condition, sheet thickness, die design, stamping process type, and part geometry. Please share drawings for engineering review before production.

Are you ready to get started on your metal fabrication project?

Not sure which material is ideal for your project? Feel free to contact us.Our engineering team will recommend suitable material grades and sheet thicknesses based on strength, weight, corrosion resistance and overall cost.

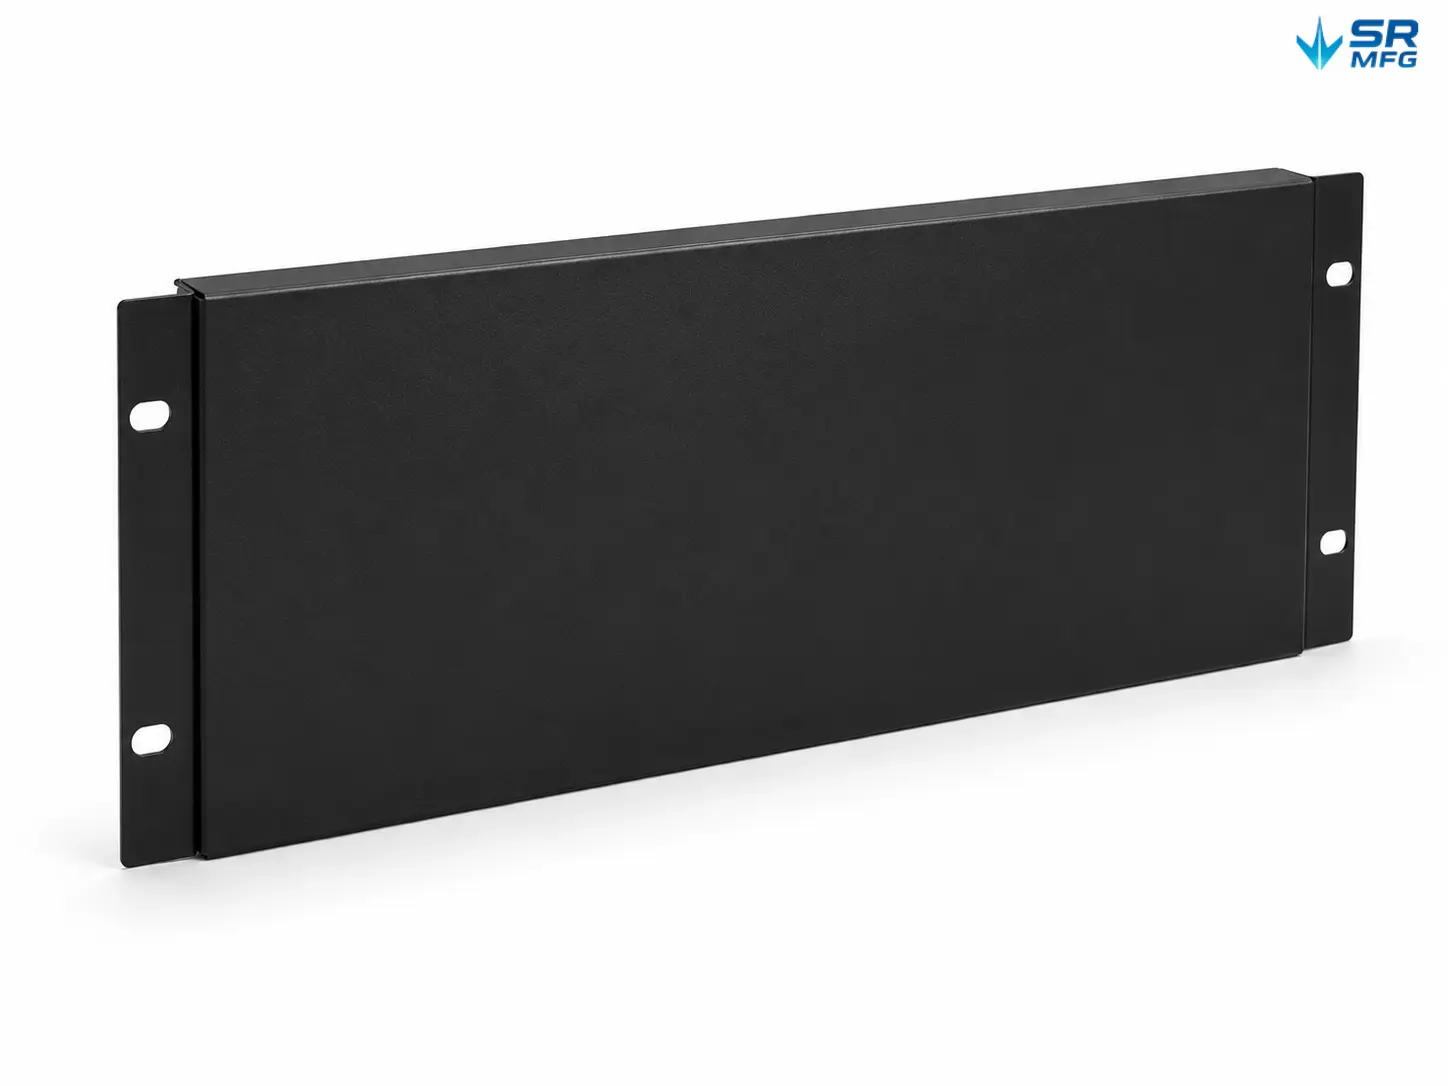
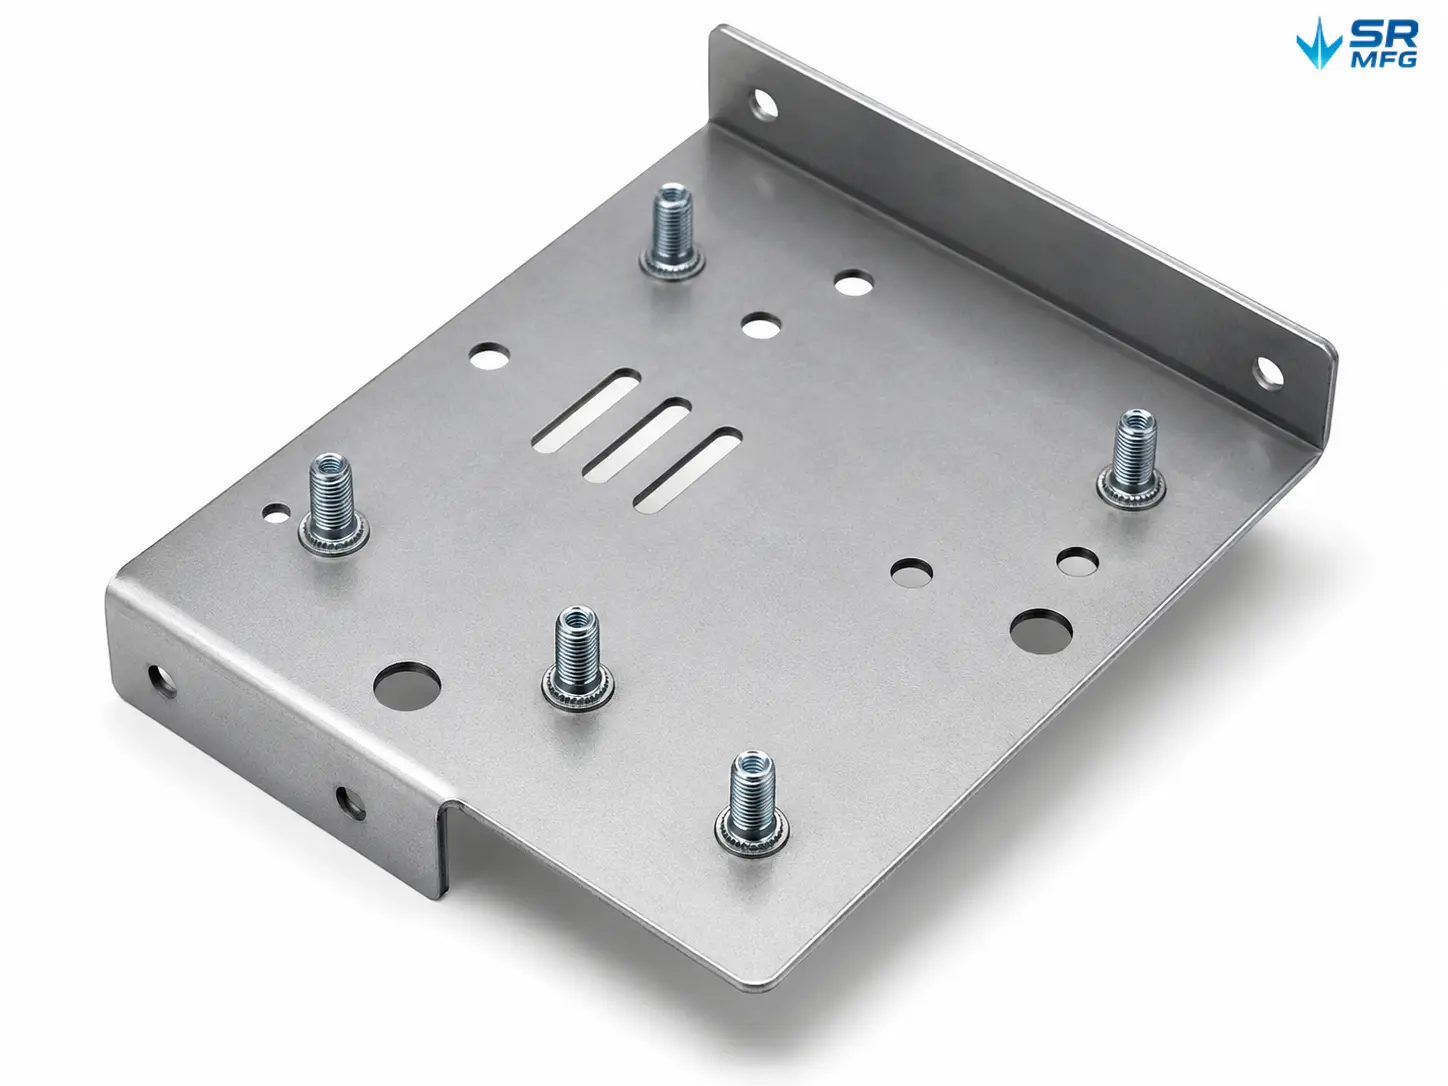
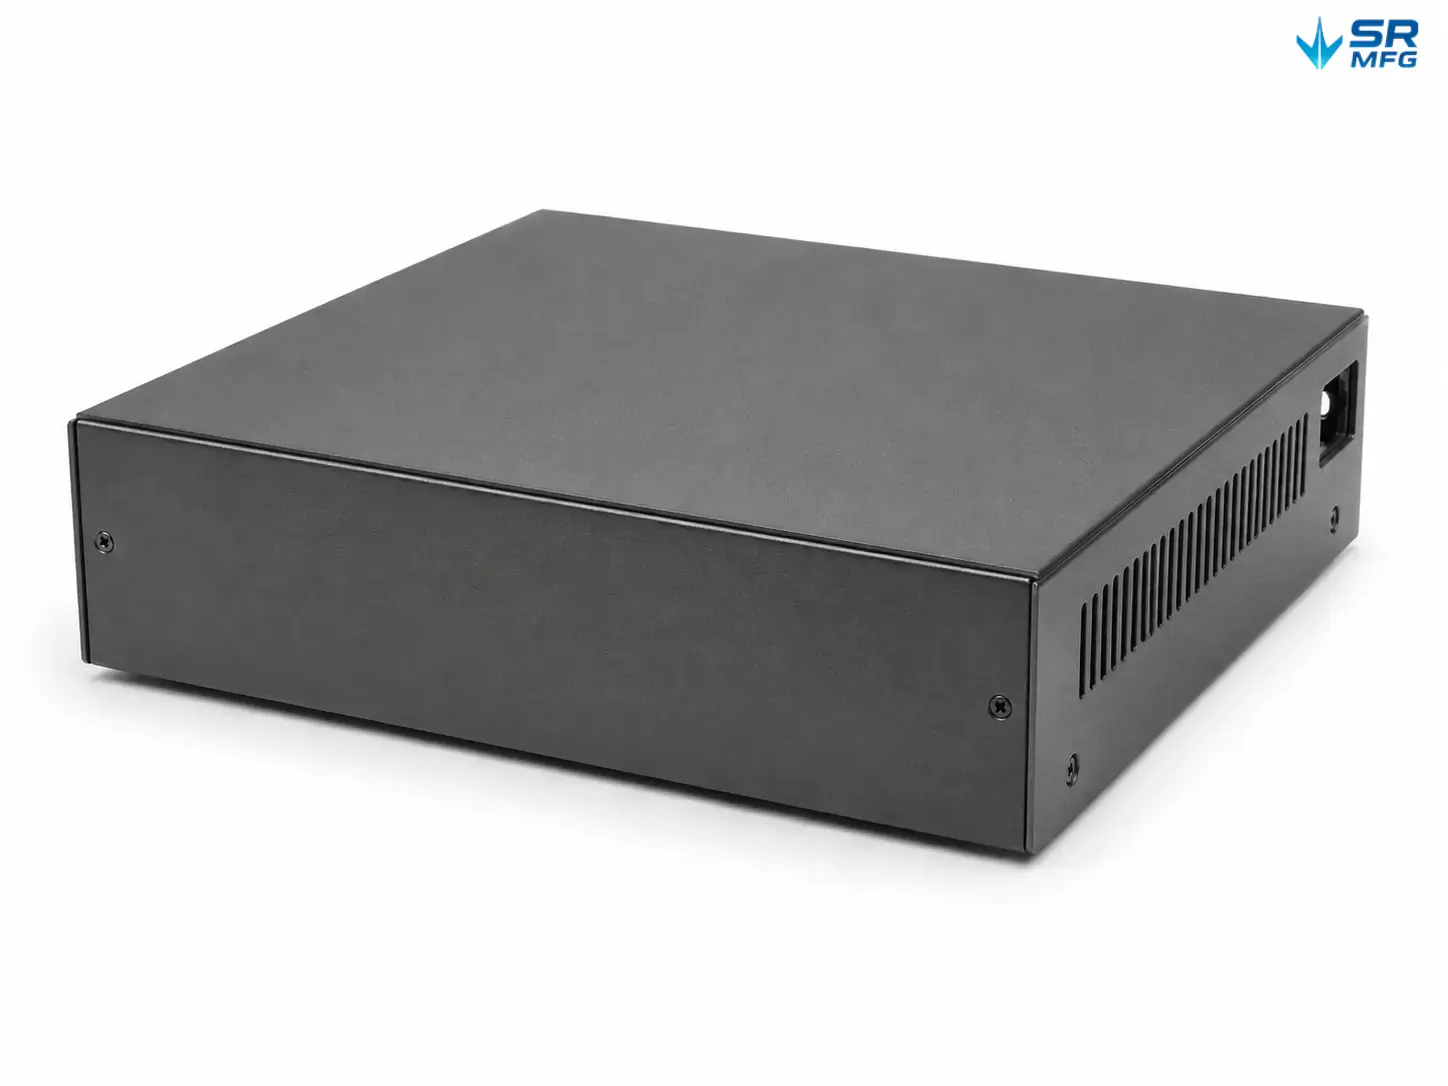
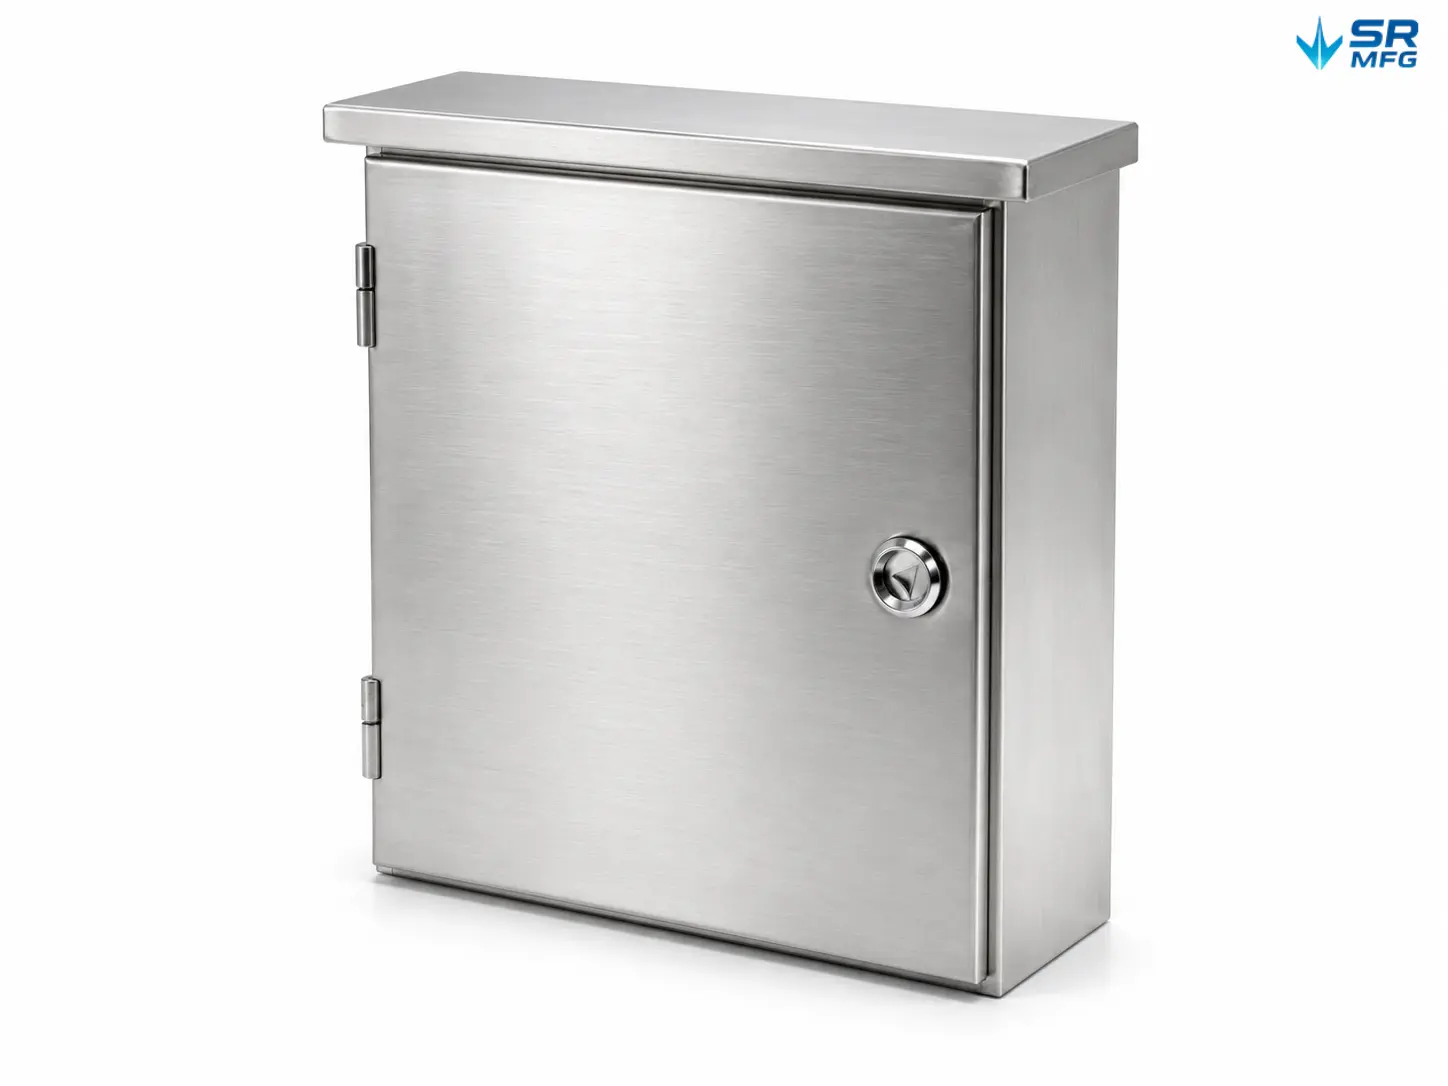
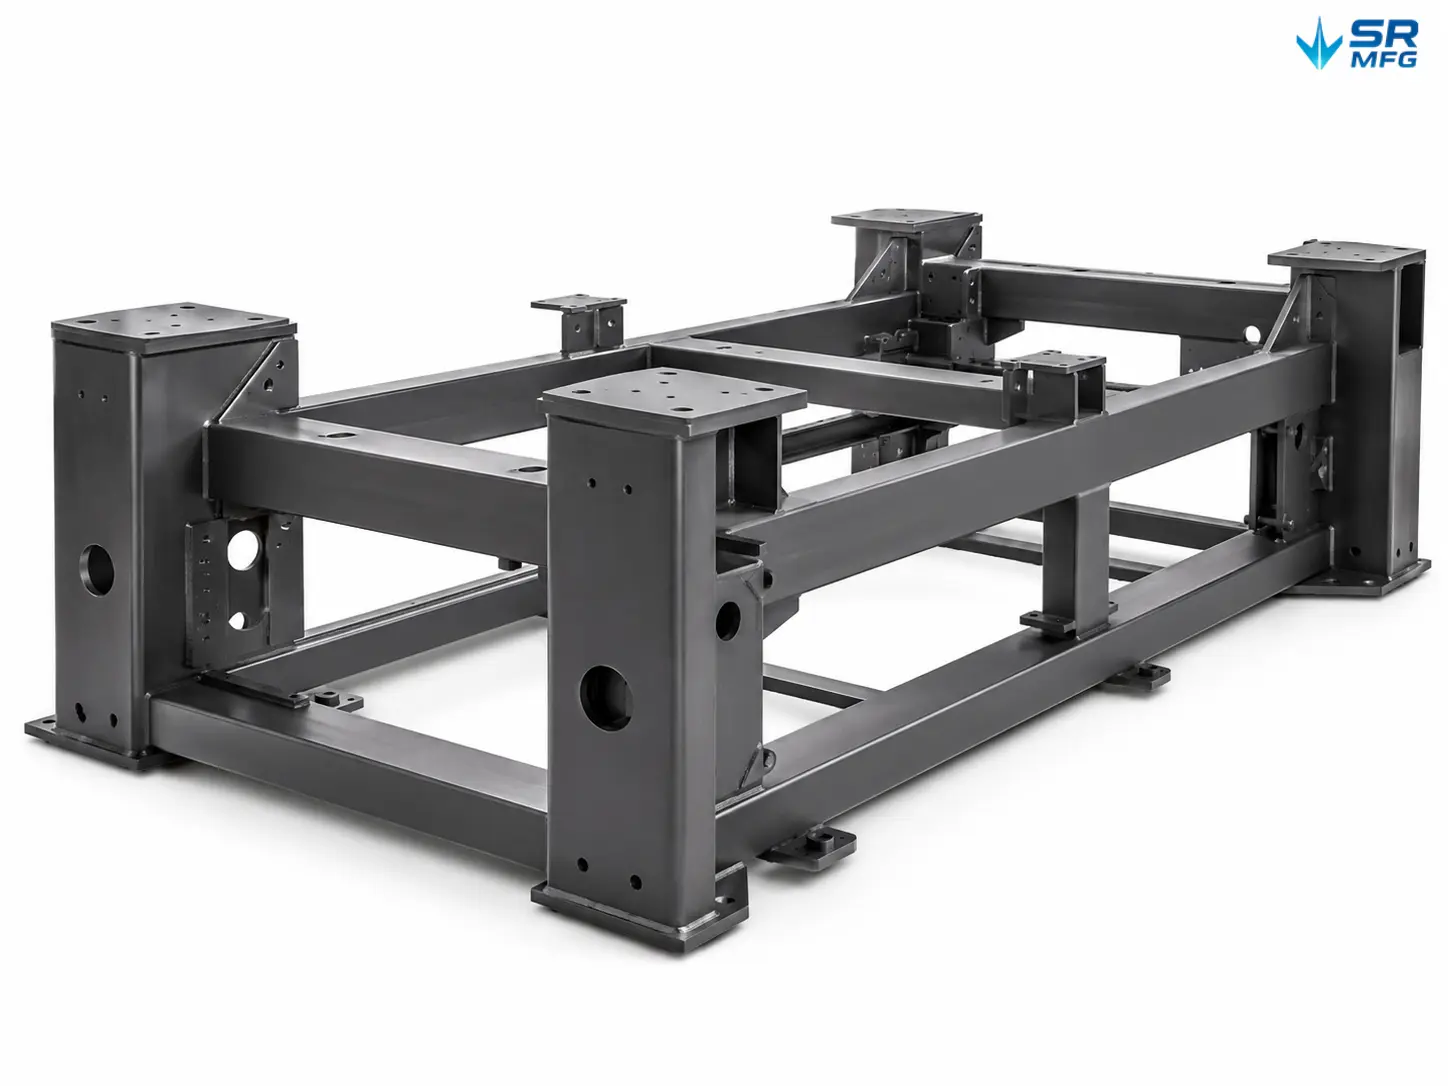
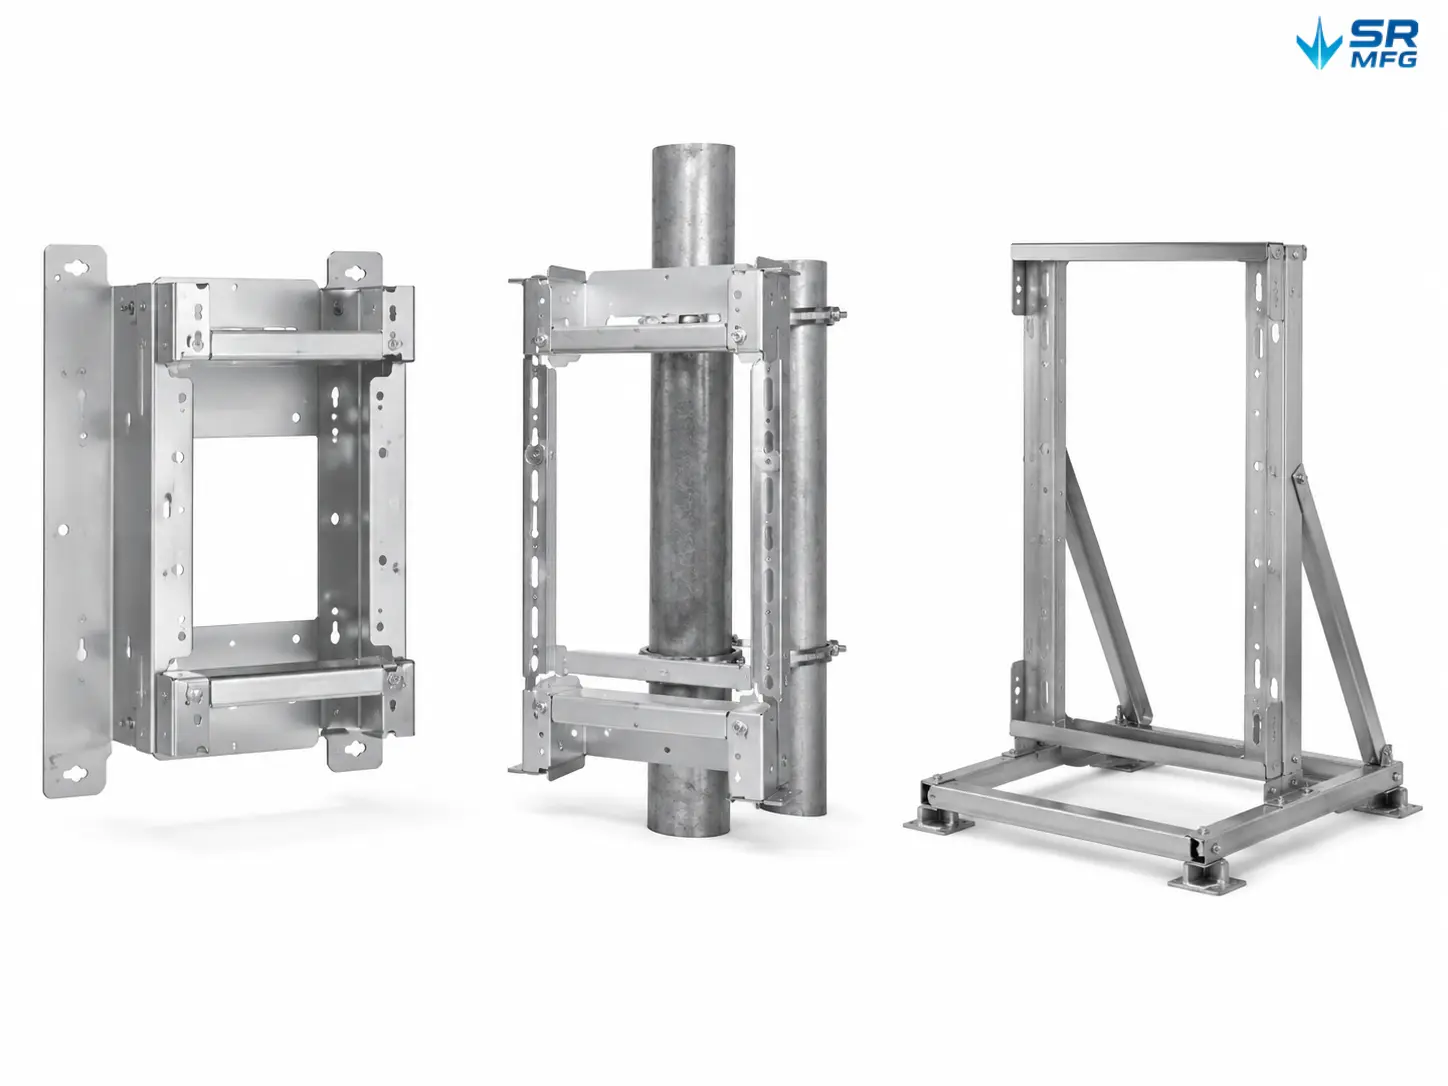
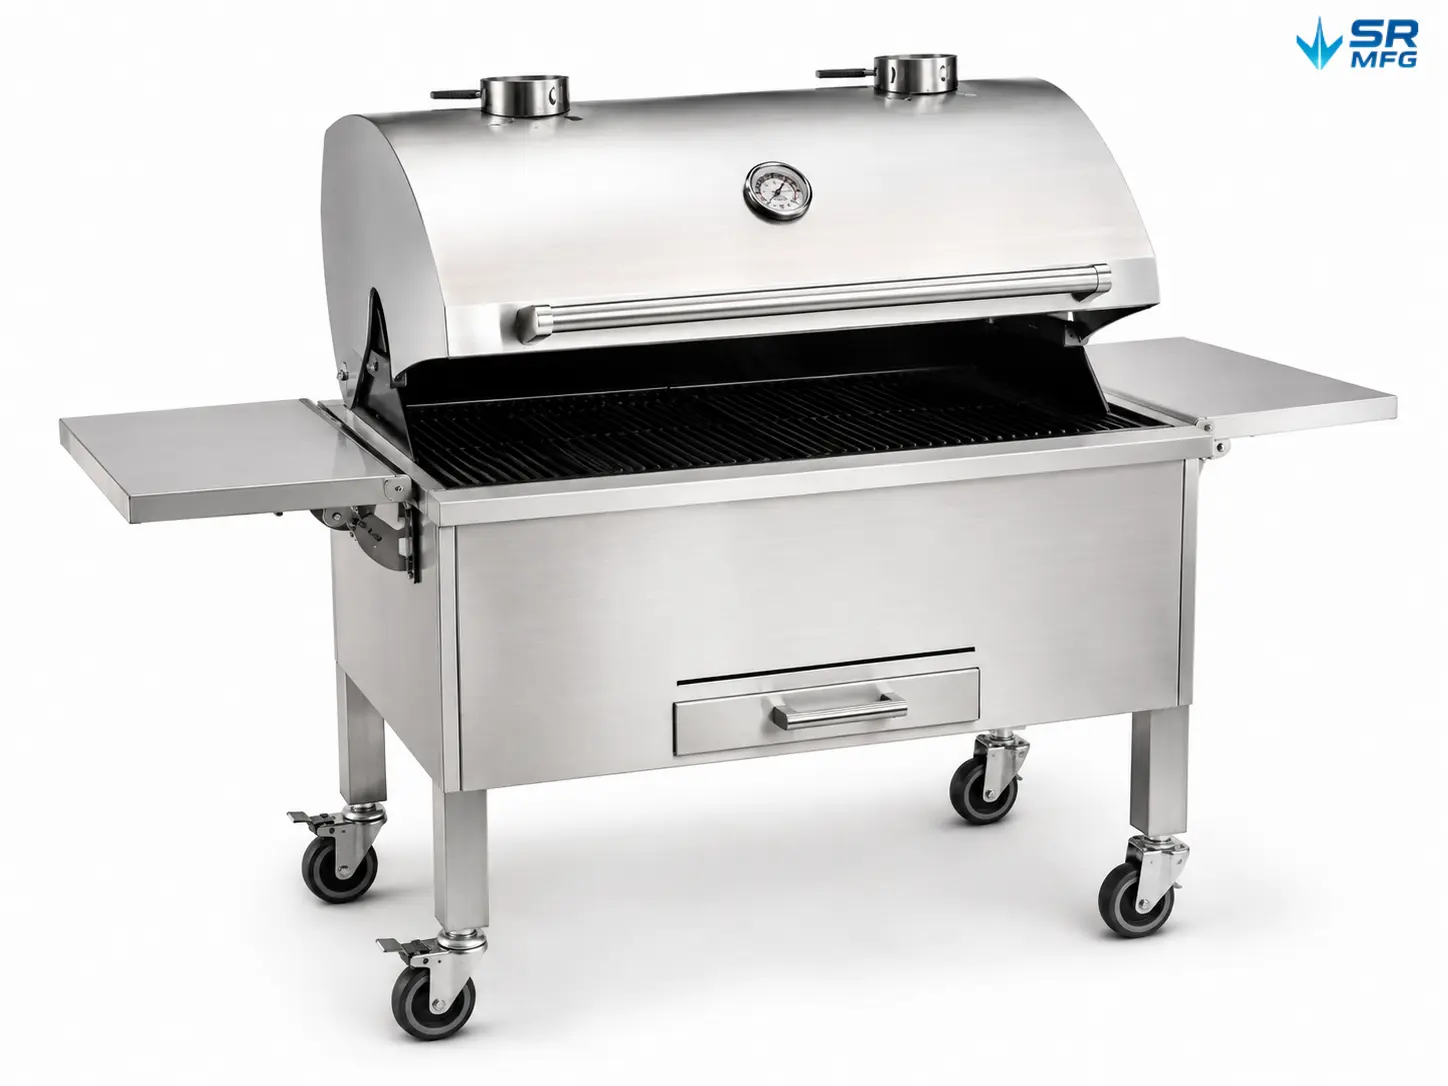
Metal Stamped Products Designed & Manufactured by SR MFG

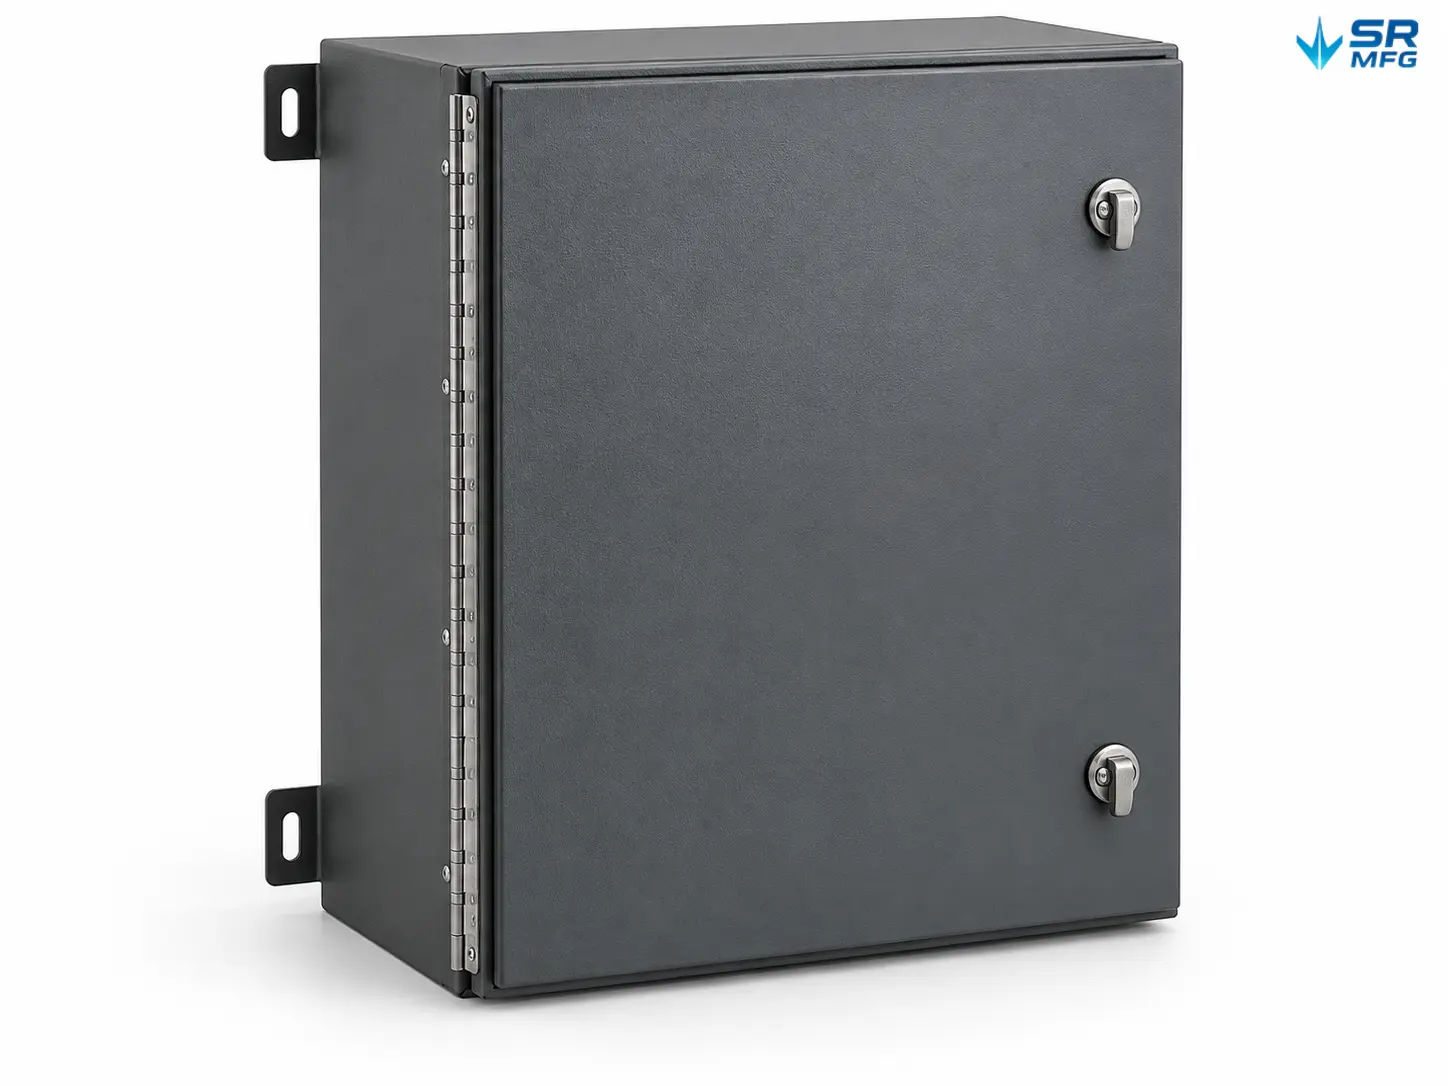
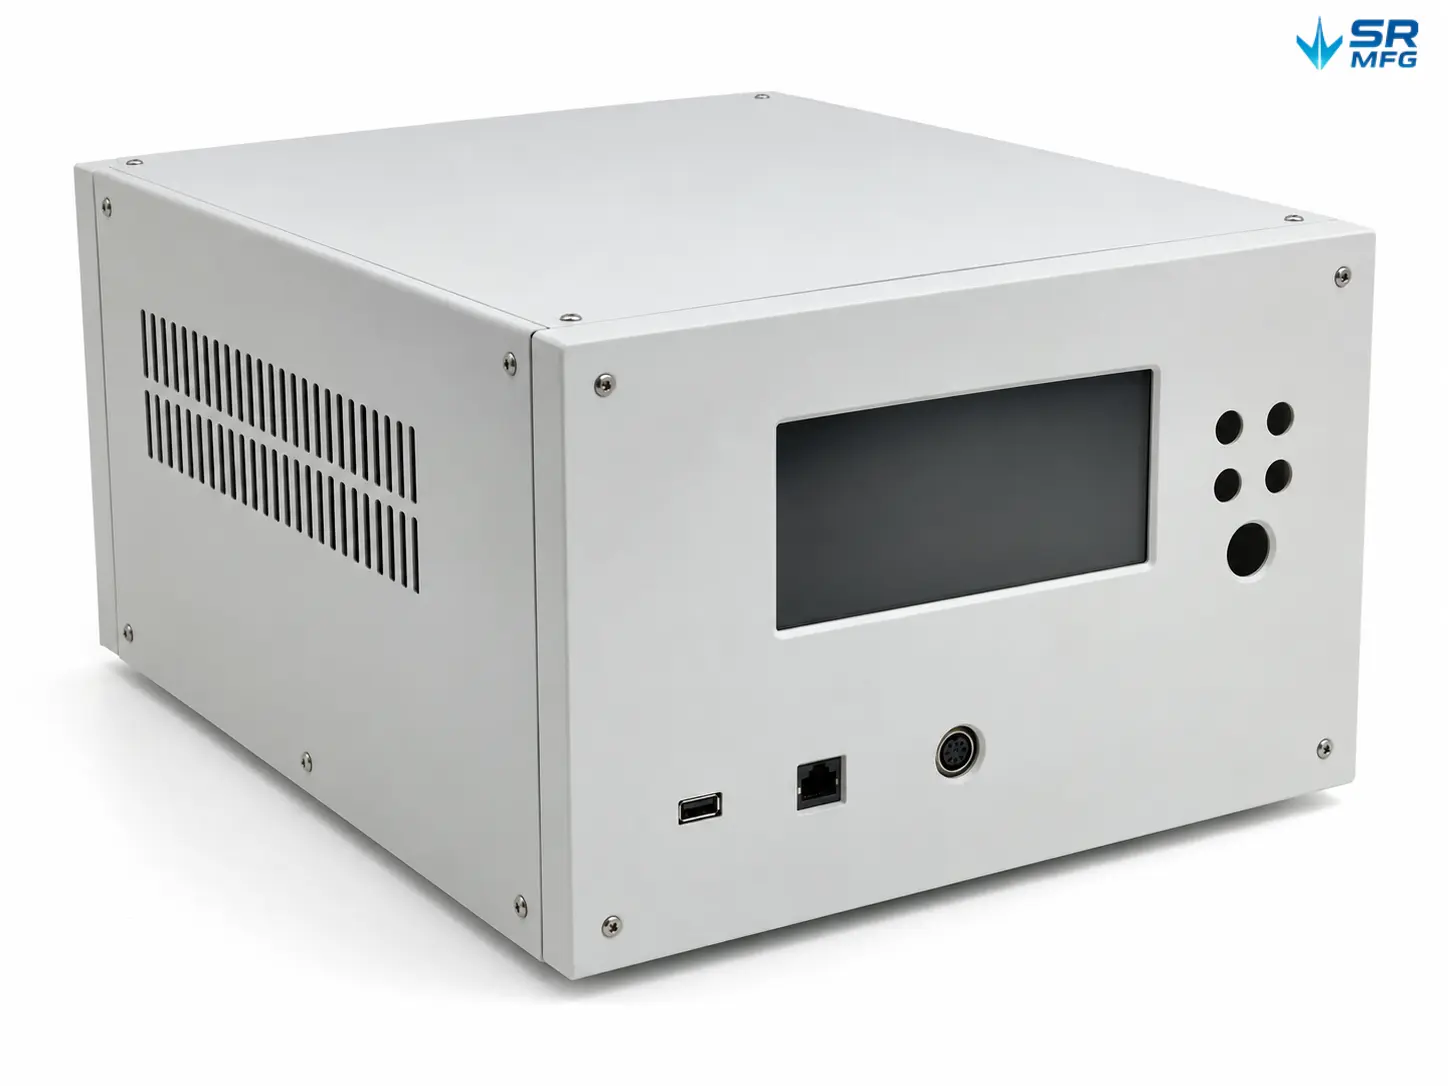
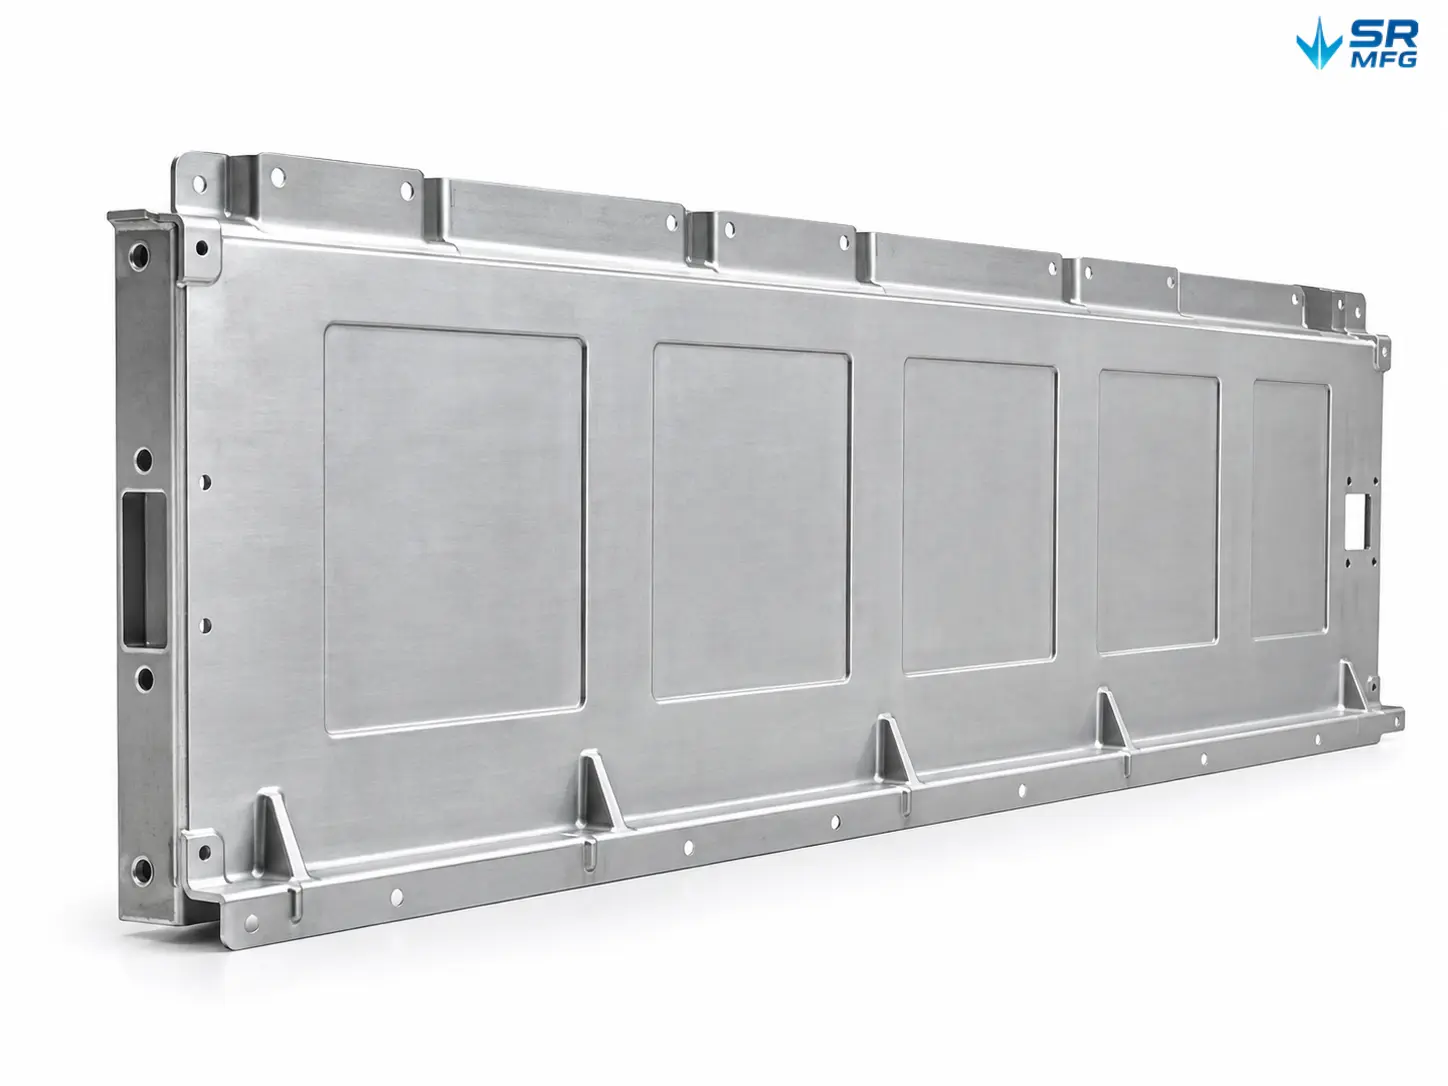
SR MFG designs and manufactures a wide range of custom stamped metal components, including brackets, panels, frames, housings/enclosures, stiffeners, connectors, clips, mounting hardware, and other structural or functional sheet-metal parts—produced to print and optimized for stable mass production.

Sheet Metal Stamping Häufig gestellte Fragen​​

We commonly work with SPCC/SECC, galvanized steel, stainless steel (304/316), und aluminum alloys (5052/6061). Our typical thickness range is 0.5–6.0 mm (thicker materials can be evaluated depending on part geometry and the selected process route). If you can share the material grade, temper/hardness, and surface requirements, we’ll confirm manufacturability and forming risks during the DFM stage.

We support single-operation stamping, compound die stamping, und progressive die stamping (plus localized forming and deep-draw operations when required). In general:

  • Prototypes / small batches / frequent design changes: single-operation stamping for fast development and flexible adjustments

  • Stable volumes and reduced secondary operations: compound dies to improve consistency and reduce handoffs

  • Medium-to-high volume production: progressive dies for stable cycle time and lower unit cost

We’ll recommend the most suitable route based on your part geometry, tolerances, production volume, and lead-time targets, and explain the key factors that drive cost and delivery.

Tolerance capability depends on the material, part complexity, process route, and inspection method. During evaluation, we identify critical-to-quality (CTQ) characteristics and define the appropriate control plan. We then use First Article Inspection (FAI) + in-process inspection to maintain batch-to-batch consistency.

If you provide your drawings and assembly requirements, we can advise on achievable tolerances for features such as hole position, bend dimensions, edge-to-edge distance, flatness, and perpendicularity, and define a sampling or 100% inspection strategy for CTQs in production.


To speed up evaluation, please provide:

  • 2D drawings (tolerances, datums, burr direction, cosmetic surface requirements)

  • 3D files (if available)

  • Material grade / thickness / required surface finish

  • Estimated volumes (prototype quantity, monthly demand, or annual forecast) and target lead time

With complete information, we start with DFM feedback and process evaluation, then provide a prototype and production lead-time plan. If tooling is required, we’ll also outline the die timeline and key milestones (e.g., tryout, adjustments, and FAI approval).

We typically follow a quality flow of incoming inspection → First Article Inspection (FAI) → in-process inspection (IPQC) → outgoing inspection (OQC), with inspection records maintained for CTQ dimensions.

If a nonconformance occurs, we act quickly to contain/segregate the affected parts, identify root cause, implement corrective actions, and provide a clear closed-loop update (issue description, scope/impact, corrective & preventive actions, and re-verification results). If required, we can also provide lot traceability details and inspection reports per customer request.

Metal Stamping Technical Resources

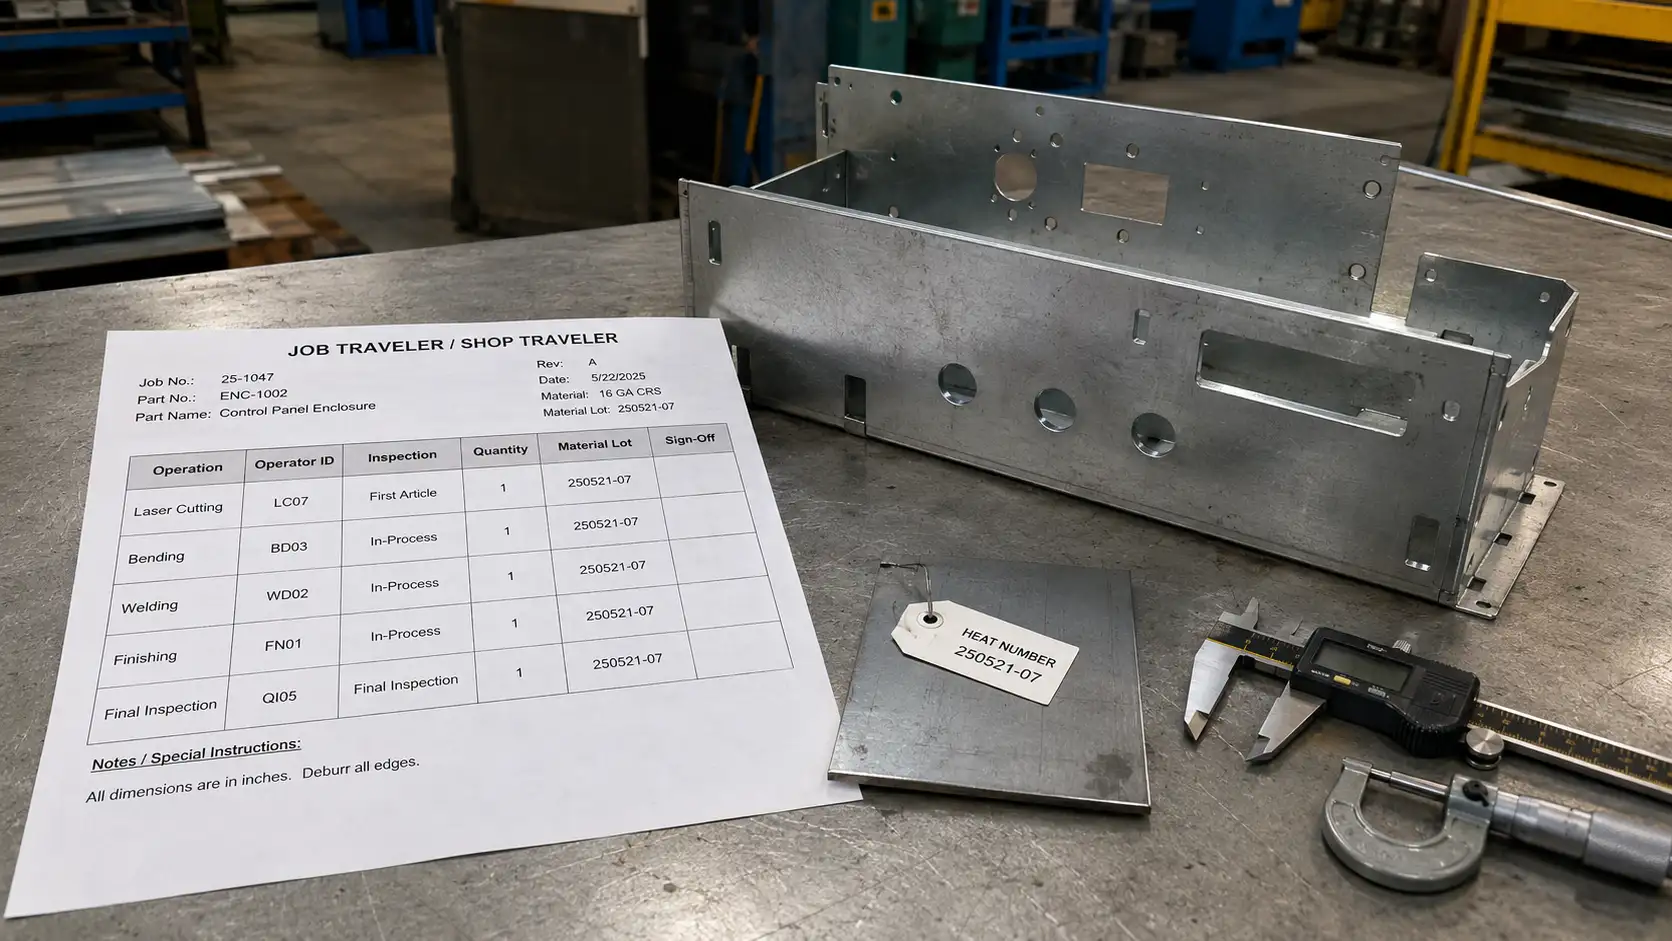
Job Traveler

September 1, 2026|

A missing operator signature on a job traveler can hold up a shipment. An absent inspection record can [...]

Go to Top