
Metallschleifdienste
SR MFG bietet Metallschleifdienste für Blechteile an, die Oberflächennivellierung, Schweißnahtübergangsverschleifung, Kantenbearbeitung und kontrollierte gebürstete oder geschliffene Texturen erfordern.
Wir helfen dabei, erhabene Defekte zu entfernen, sichtbare Übergänge zu verschleifen, die Oberflächenkonsistenz zu verbessern und Teile für Polieren, Beschichten, Montage oder die abschließende optische Freigabe vorzubereiten. Bei optisch kritischen Teilen können wir die Schleifrichtung, A/B-Oberflächenzonen, Rauheitsziele und die Übereinstimmung mit freigegebenen Mustern kontrollieren.
Erhalten Sie ein individuelles Angebot in 24 Stunden
Laden Sie Ihre Zeichnungen zur technischen Prüfung hoch.
Was ist Metallschleifen? Wie es sich vom Polieren und Entgraten unterscheidet
Man kann sich das Metallschleifen als Einebnen einer Oberfläche mit zunehmend feineren Schleifmitteln vorstellen. Durch die Erzeugung einer kontrollierten Relativbewegung zwischen Schleifmittel und Werkstück trägt das Schleifen überschüssiges Material auf vorhersehbare Weise ab, um ausgeprägte Werkzeugspuren, Schweißstufen und tiefe Kratzer zu nivellieren und eine gleichmäßigere und konsistentere Oberfläche zu erzeugen. In der Praxis wird das Schleifen typischerweise mit Schleifbändern, Schleifscheiben oder Schleifbürsten durchgeführt.
Wenn das Ziel ein höherer Glanz – oder sogar eine spiegelähnliche Oberfläche – ist, folgt auf das Schleifen üblicherweise das Polieren oder andere Finish-Operationen.
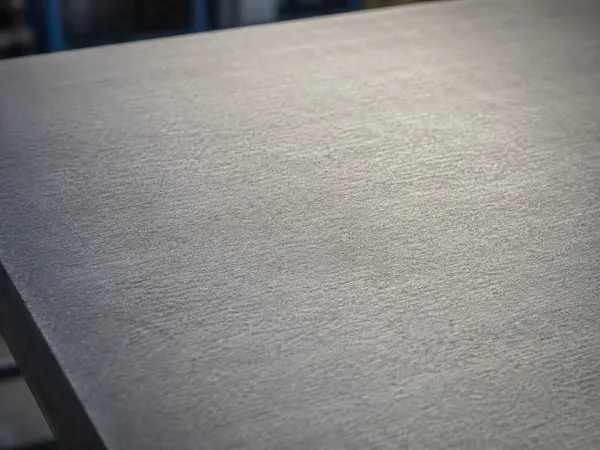
Schleifen vs. Polieren vs. Entgraten
Diese Prozesse mögen ähnlich aussehen, lösen jedoch unterschiedliche Probleme. Nutzen Sie den folgenden Vergleich, um das richtige Finish, den Kantenzustand und die Prüfanforderung für Ihr Teil zu definieren.
Schleifen
Oberflächennivellierung, Defektentfernung und Texturkontrolle.
Werkzeugspuren, Schweißstufen, tiefe Kratzer und unebene Oberflächen.
Flacher und gleichmäßiger. Hoher Glanz ist nicht das primäre Ziel.
Material wird abgetragen, daher sollten Abtragsmenge und Ebenheit kontrolliert werden.
Definieren A-Oberflächenbereich, Schleifrichtung, Ra oder Ra max und freigegebenes Referenzmuster.
Polieren
Feineres kosmetisches Finish, Helligkeit und glatteres Erscheinungsbild.
Matte Oberflächen, feine Kratzer und kosmetische Erscheinungsanforderungen.
Höherer Glanz, glattere Oberfläche und höhere kosmetische Qualitätsstufe.
Kann je nach Material, Methode und Finish-Ziel zu leichten Veränderungen führen.
Zielglanz, Spiegelgrad falls erforderlich, Ra-Ziel und freigegebenes Referenzmuster definieren.
Entgraten / Kantenbrechen
Gratentfernung, sicherere Kanten und einfachere Montagepassung.
Scharfe Kanten, Montageklemmung, Grate an Bohrungen oder Kanten und Handhabungsrisiko.
Glattere, weniger scharfe Kanten mit reduzierten Graten und verbesserter Sicherheit.
Normalerweise minimal, aber kritische Kanten benötigen klare Grenzen und zulässigen Abtrag.
Entgraten, Kantenbrechen, maximalen Kantenradius oder zulässigen Fasenbereich spezifizieren.
Technische Anmerkung: Schleifen, Polieren und Entgraten können kombiniert werden, wenn Teile Oberflächenkorrektur, kosmetisches Finish und sichere Montagekanten erfordern.
Oberflächenstruktur-Optionen beim Schleifen
Wählen Sie die richtige visuelle Textur und Schleifrichtung basierend auf Erscheinungsanforderungen, Material und nachgelagerter Verwendung
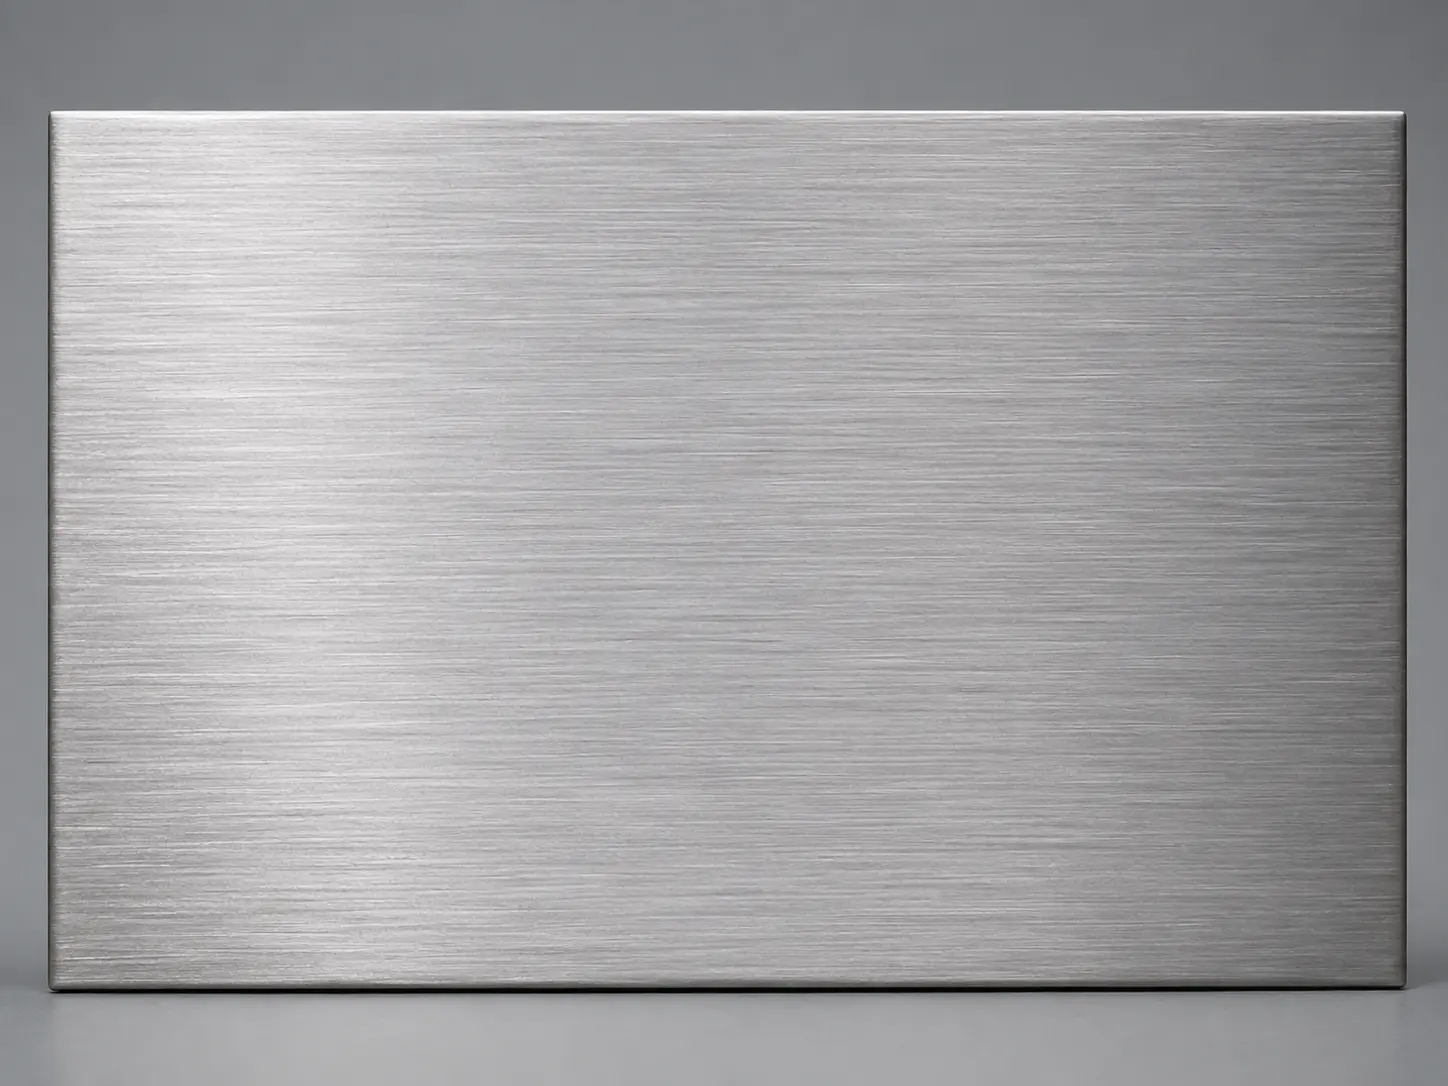
Lineares Bürsten / Gerichtete Schleifrichtung
Texturprofil: Kontinuierliche geradlinige Schleifrichtung in eine Richtung.
Typische Methode: Progressives Bandfinish zum Verfeinern und Festlegen der Schleifrichtung.
Am besten geeignet für: Edelstahlpaneele, kosmetische Gehäuse, sichtbare Oberflächen.
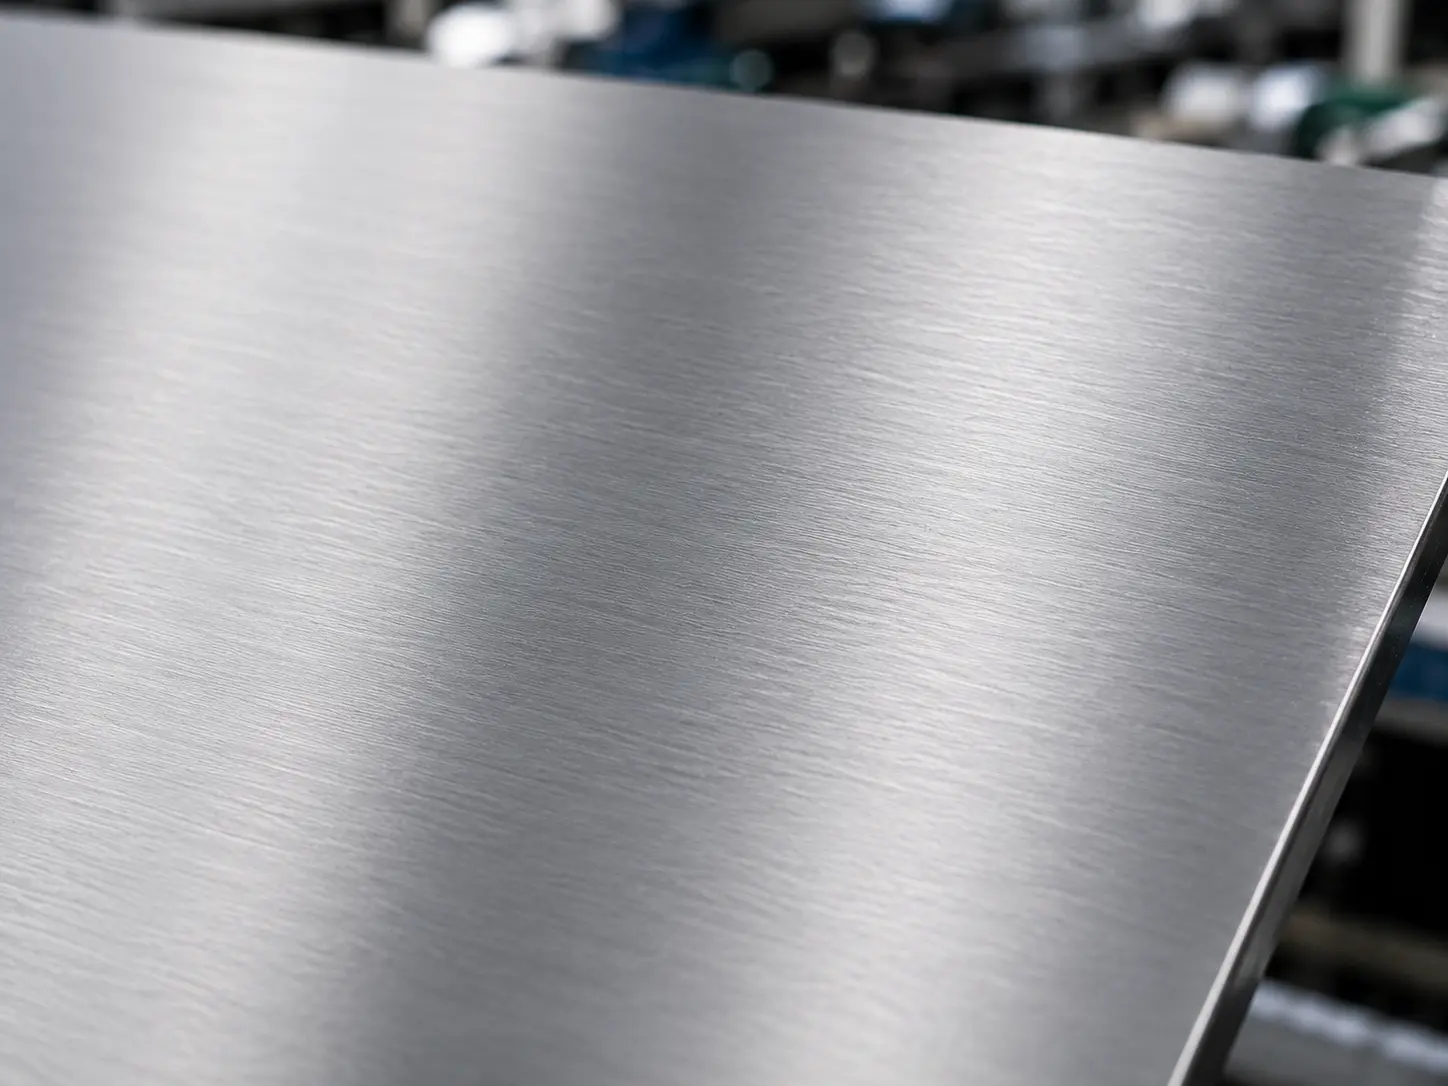
No.4 Satin Finish
Texturprofil: Softer, more uniform directional brushed appearance.
Typische Methode: Typically around 150–180 grit, matched to approved reference.
Am besten geeignet für: 304/316 cosmetic parts, equipment housings, kitchen panels.
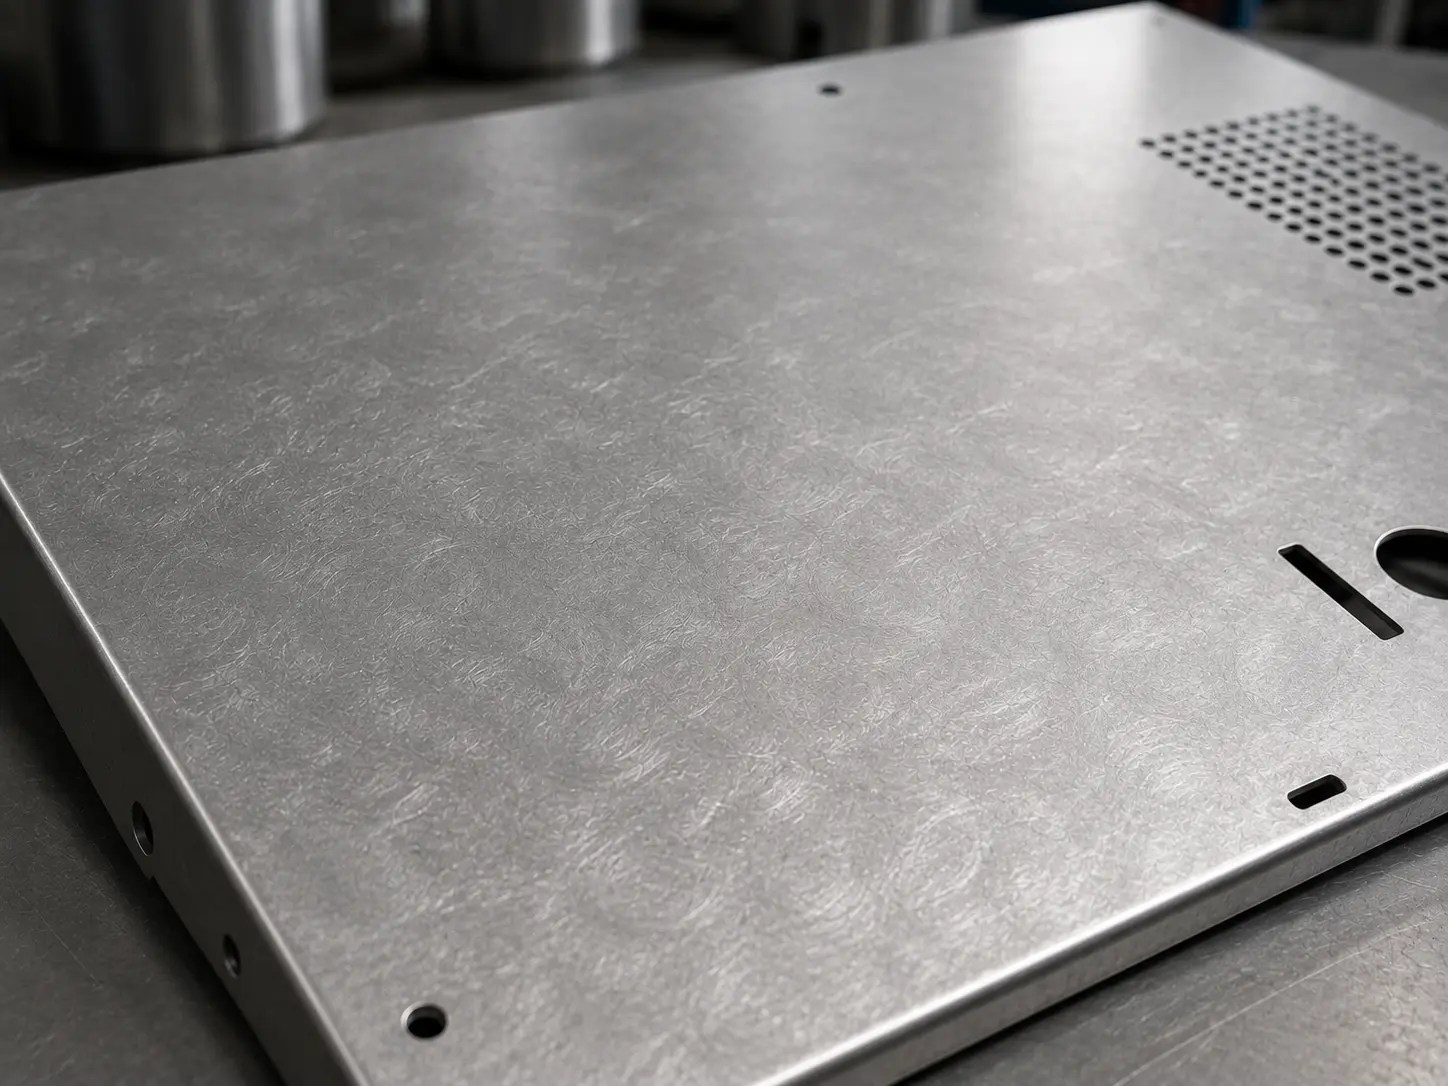
Random / Swirl / Non-Directional Texture
Texturprofil: Randomized pattern with no fixed grain direction.
Typische Methode: Random-orbit sanding or dedicated non-directional tooling.
Am besten geeignet für: Cosmetic surfaces where direction sensitivity is undesirable.
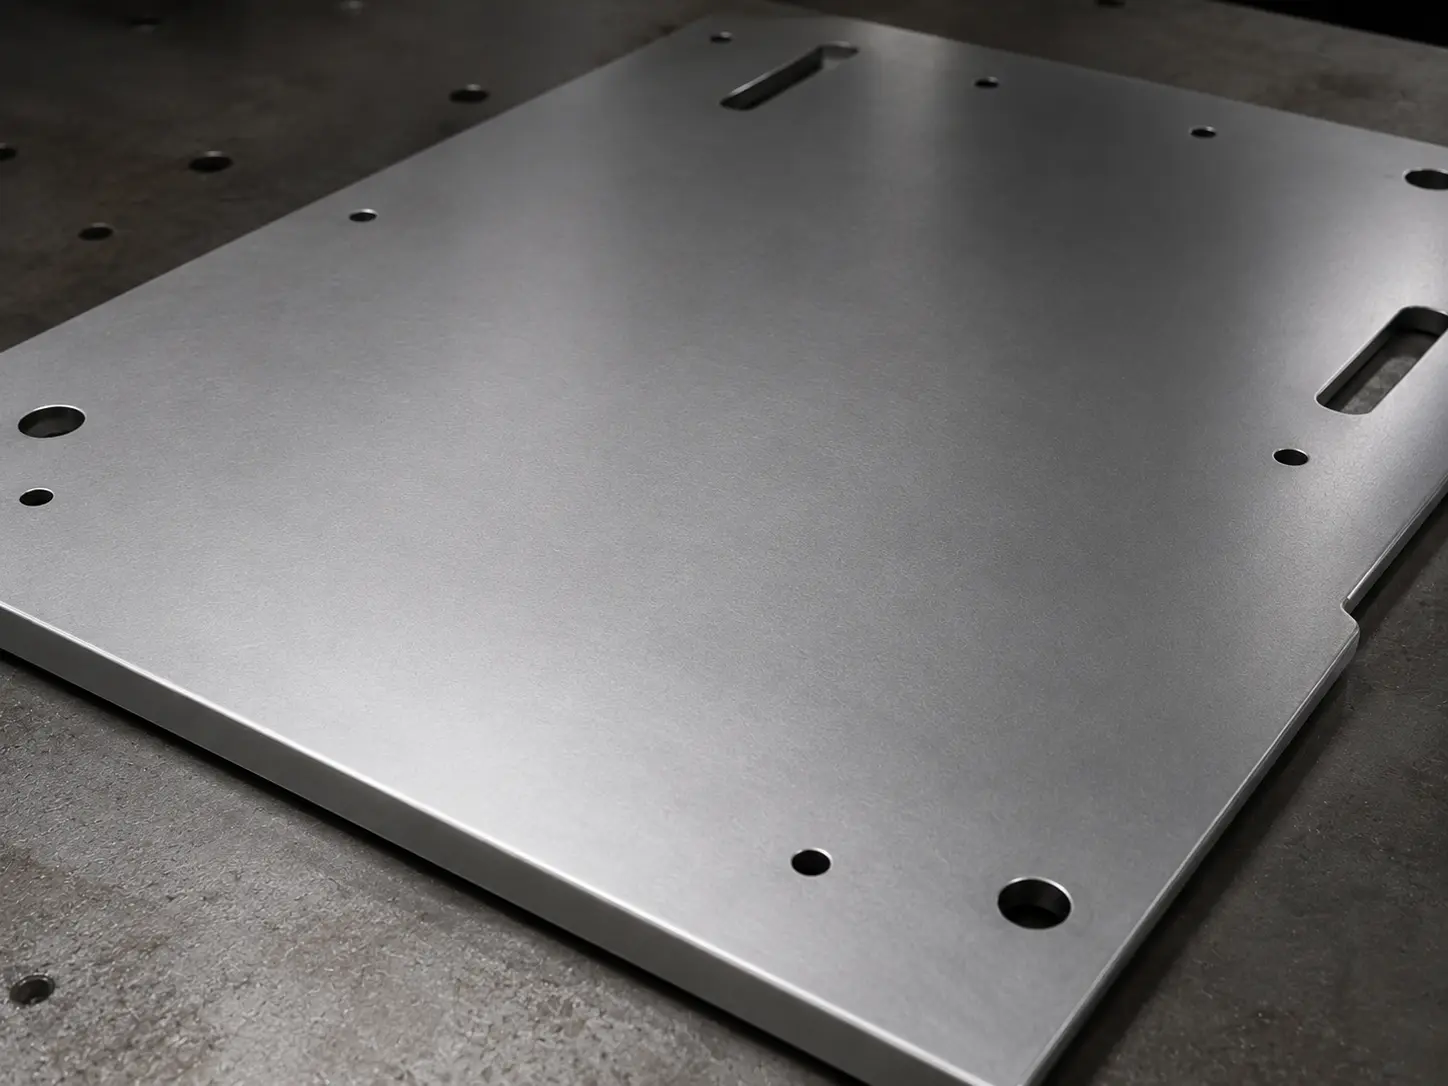
Blending / Matte Uniforming
Texturprofil: More matte and even overall, minimizing visible scratch lines.
Typische Methode: Non-woven abrasive belts or wheels for blending and smoothing.
Am besten geeignet für: Pre-coating uniforming, light cosmetic parts, weld-transition blending.
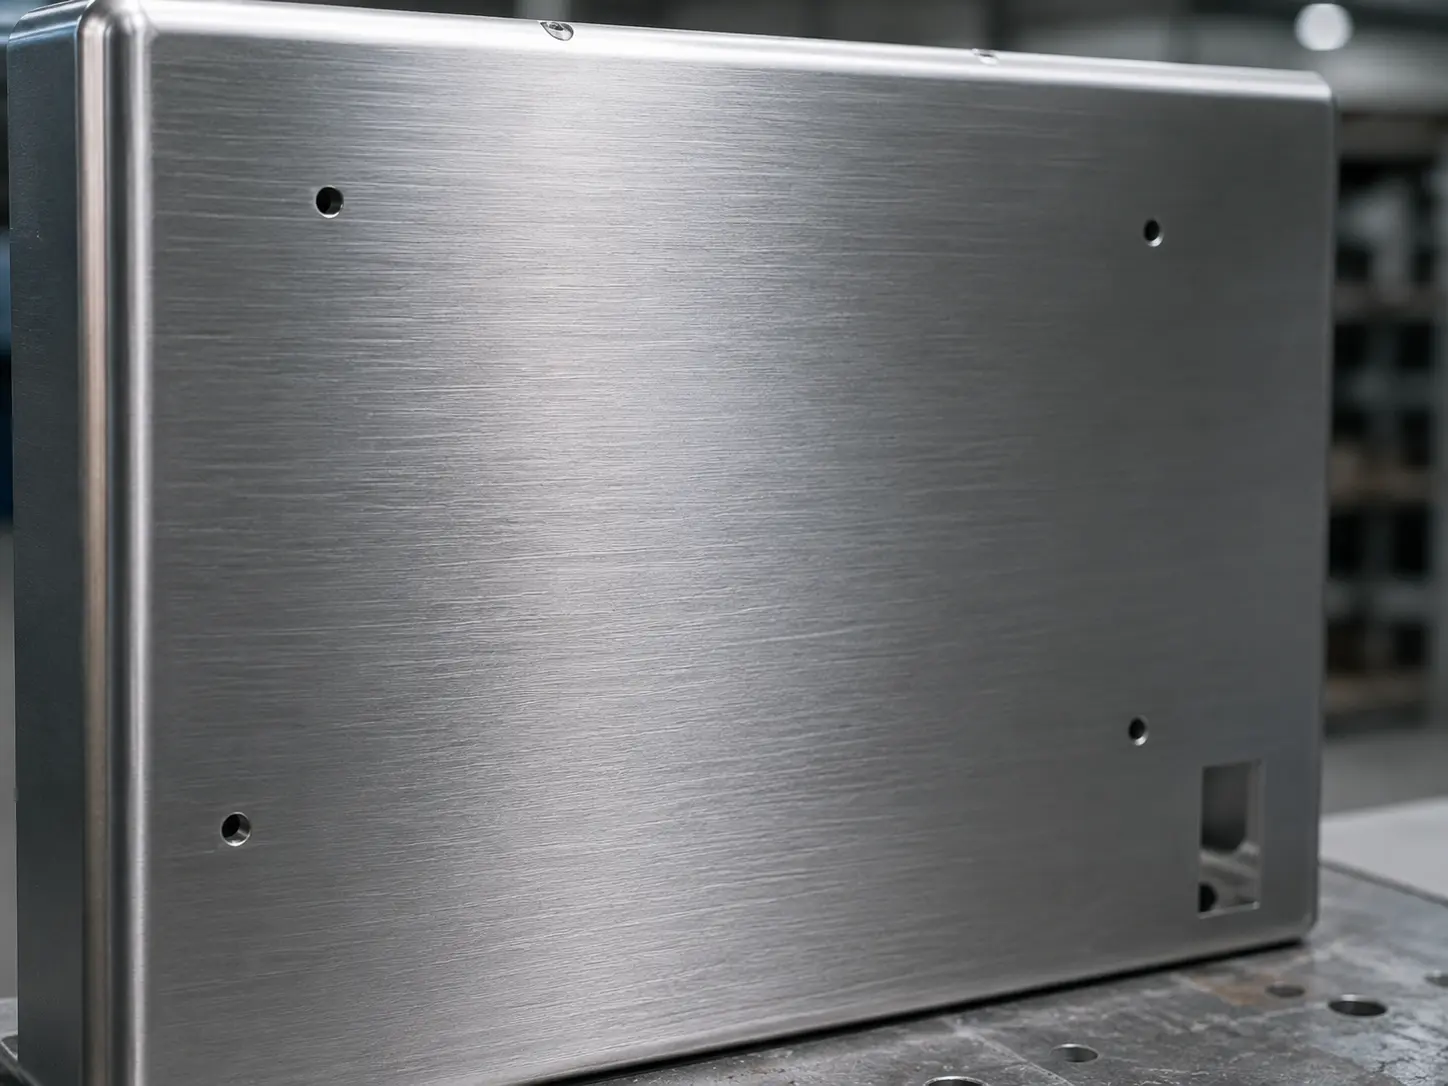
Weld-Grain Restoration / Grain Matching
Texturprofil: Reconstructs the grain so weld areas match the surrounding surface.
Typische Methode: Remove weld steps first, then rebuild the final specified grain direction.
Am besten geeignet für: Cosmetic stainless assemblies, panels, and covers with strict grain matching.
Material Compatibility for Metal Grinding
Carbon Steel /
Stainless Steel /
Cast Iron
Standard capability
- Common abrasive: Aluminum-oxide systems
- Am besten geeignet für: Surface leveling, weld blending, texture control
- Note: Stable stock removal and consistent texture
Hardened Steel &
Bearing Steel
High hardness
- Common abrasive: CBN preferred
- Am besten geeignet für: Controlled grinding of hardened material
- Note: Manage heat input and preserve surface quality
Aluminum &
Copper Alloys
Anti-loading focus
- Common abrasive: SiC / anti-loading systems
- Am besten geeignet für: Soft non-ferrous metals
- Note: Helps reduce smearing, drag marks, and chip adhesion
Titanium & Heat-
Resistant Alloys
Case-by-case
- Common approach: Controlled process parameters
- Am besten geeignet für: Heat-sensitive alloys
- Note: Reduce heat damage, discoloration, and surface issues
Special /
Hard Materials
When applicable
- Common abrasive: Diamond systems
- Am besten geeignet für: Carbides, ceramics, and special materials
- Note: Reviewed by hardness, geometry, and finish target
Technische Anmerkung: Final abrasive selection depends on material hardness, part geometry, finish target, heat sensitivity, and whether wet or dry grinding is required.
Standardized Metal Grinding Process
Metal Grinding Process (Video Demonstration)
Drawing &
Finish Review
- Confirm cosmetic area, grain direction, and finish target
- Review drawing details, Ra target, and approval criteria
Material Check &
Rückverfolgbarkeit
- Verify material grade, incoming surface condition, and batch identity
- Set traceability before grinding begins
Fixturing &
Surface Protection
- Protect critical zones and visible surfaces
- Control clamping, masking, and setup stability
Coarse Grinding &
Defect Leveling
- Remove weld steps, scratches, and major surface irregularities
- Build a uniform base surface for follow-up finishing
Fine Grinding &
Grain Setting
- Refine texture step by step to the specified finish
- Lock grain direction, appearance consistency, and surface quality
Cleaning, Inspection
& Packing
- Clean and dry parts; inspect appearance and Ra as required
- Apply protective packaging before shipment
Technische Anmerkung: Actual grinding flow depends on material, surface zone, grain direction, finish target, heat sensitivity, and approved reference sample.
Ready to Review Your Metal Grinding Requirements?
Send us your drawings, material grade, surface condition, grinding areas, grain direction, target finish, Ra requirements, weld blending needs, and inspection criteria. Our engineering team will review the part geometry and recommend a suitable grinding process.
Industries & Metal Grinding Applications
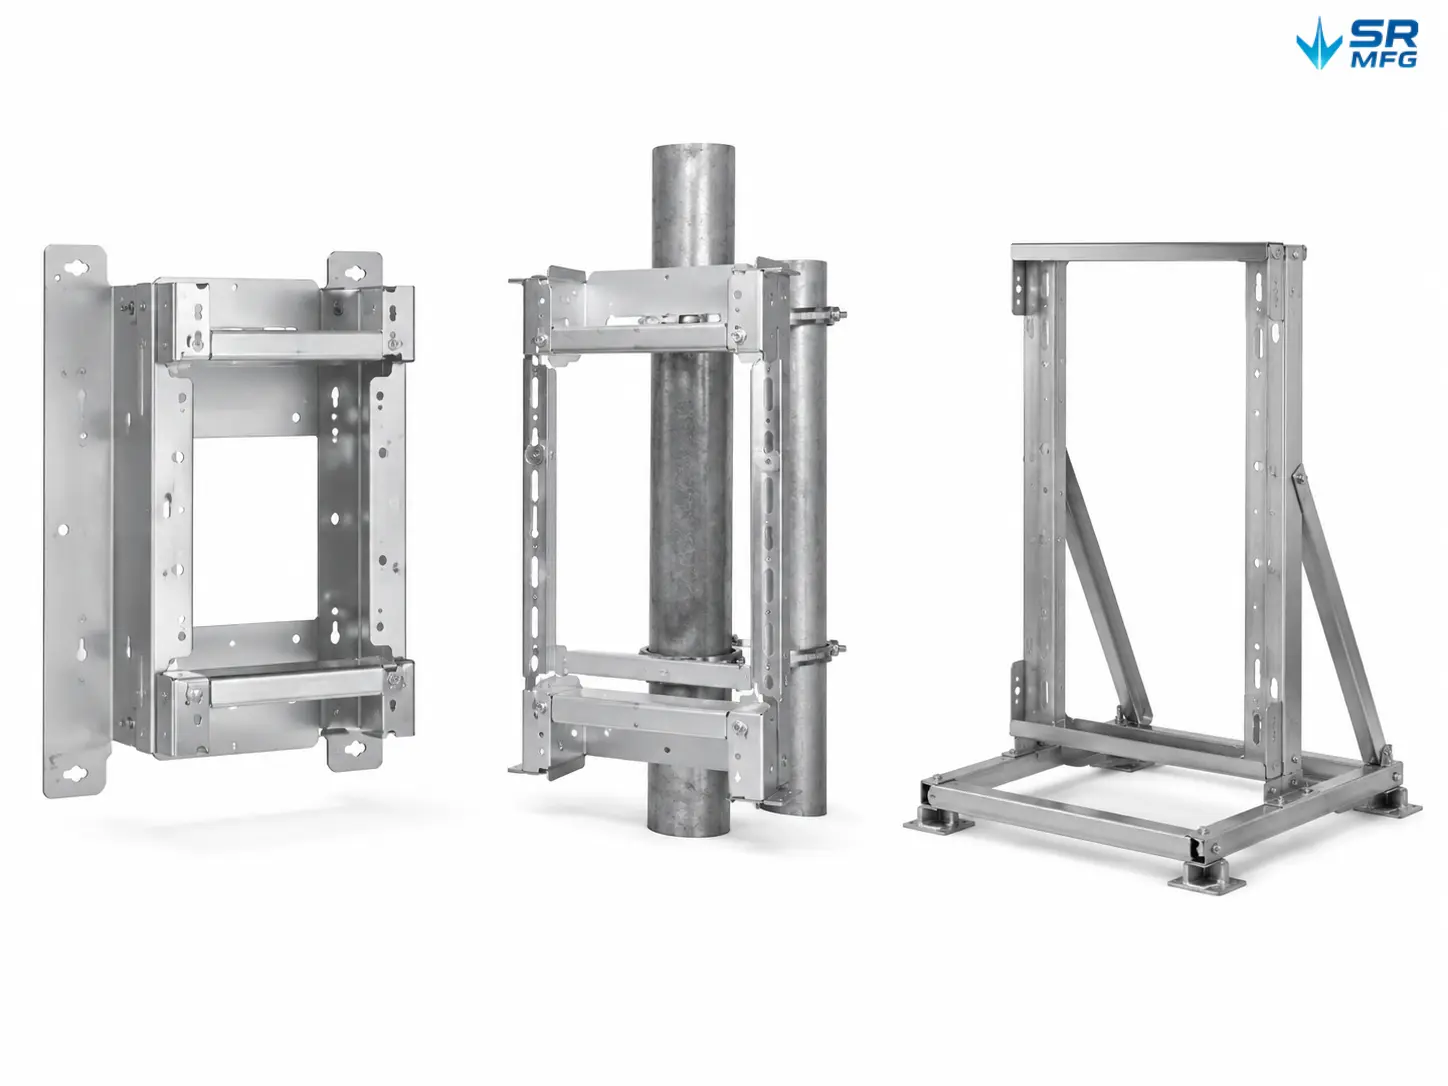
SR MFG provides metal grinding services for sheet metal parts used in data center equipment, consumer electronics, electrical systems, industrial equipment, new energy systems, and outdoor products. Metal grinding helps level uneven surfaces, blend weld transitions, remove tool marks and surface defects, and create a controlled surface texture after cutting, bending, welding, or forming.
We support both prototype validation and stable batch production for metal parts that require safer edges, smoother surfaces, weld blending, dimensional adjustment, or preparation before painting, powder coating, polishing, or other surface finishing processes.
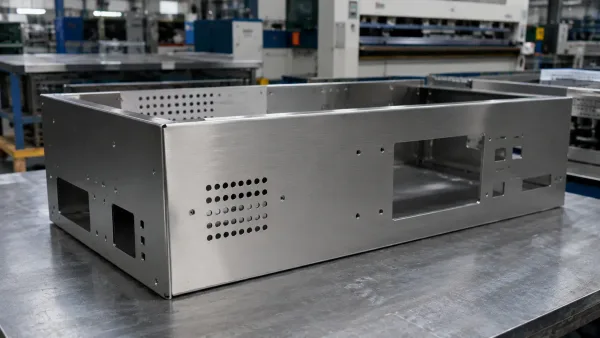
Data Centers & IT Equipment
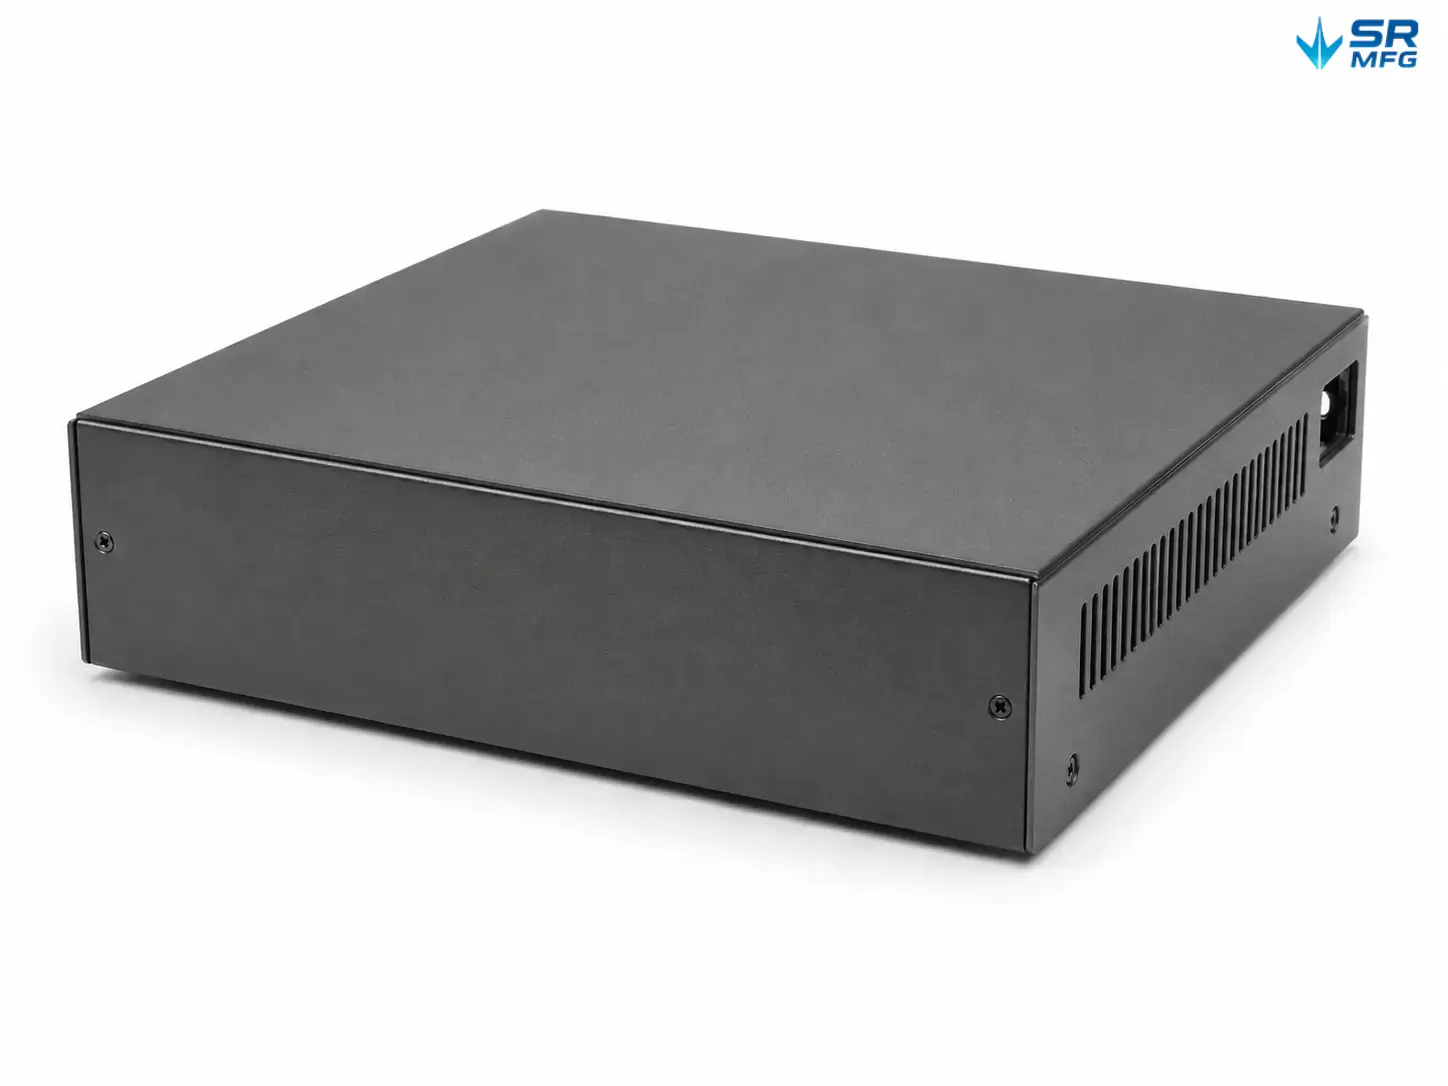
Metal grinding for data center, network infrastructure, and IT hardware parts where clean edges, flat surfaces, and reliable assembly are important.
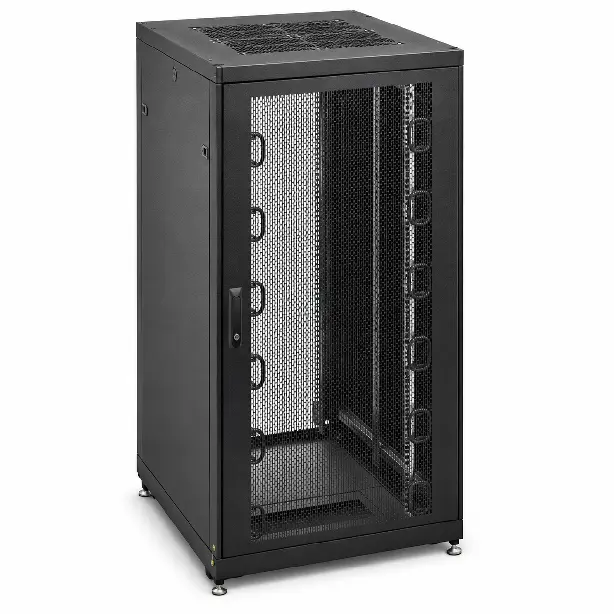
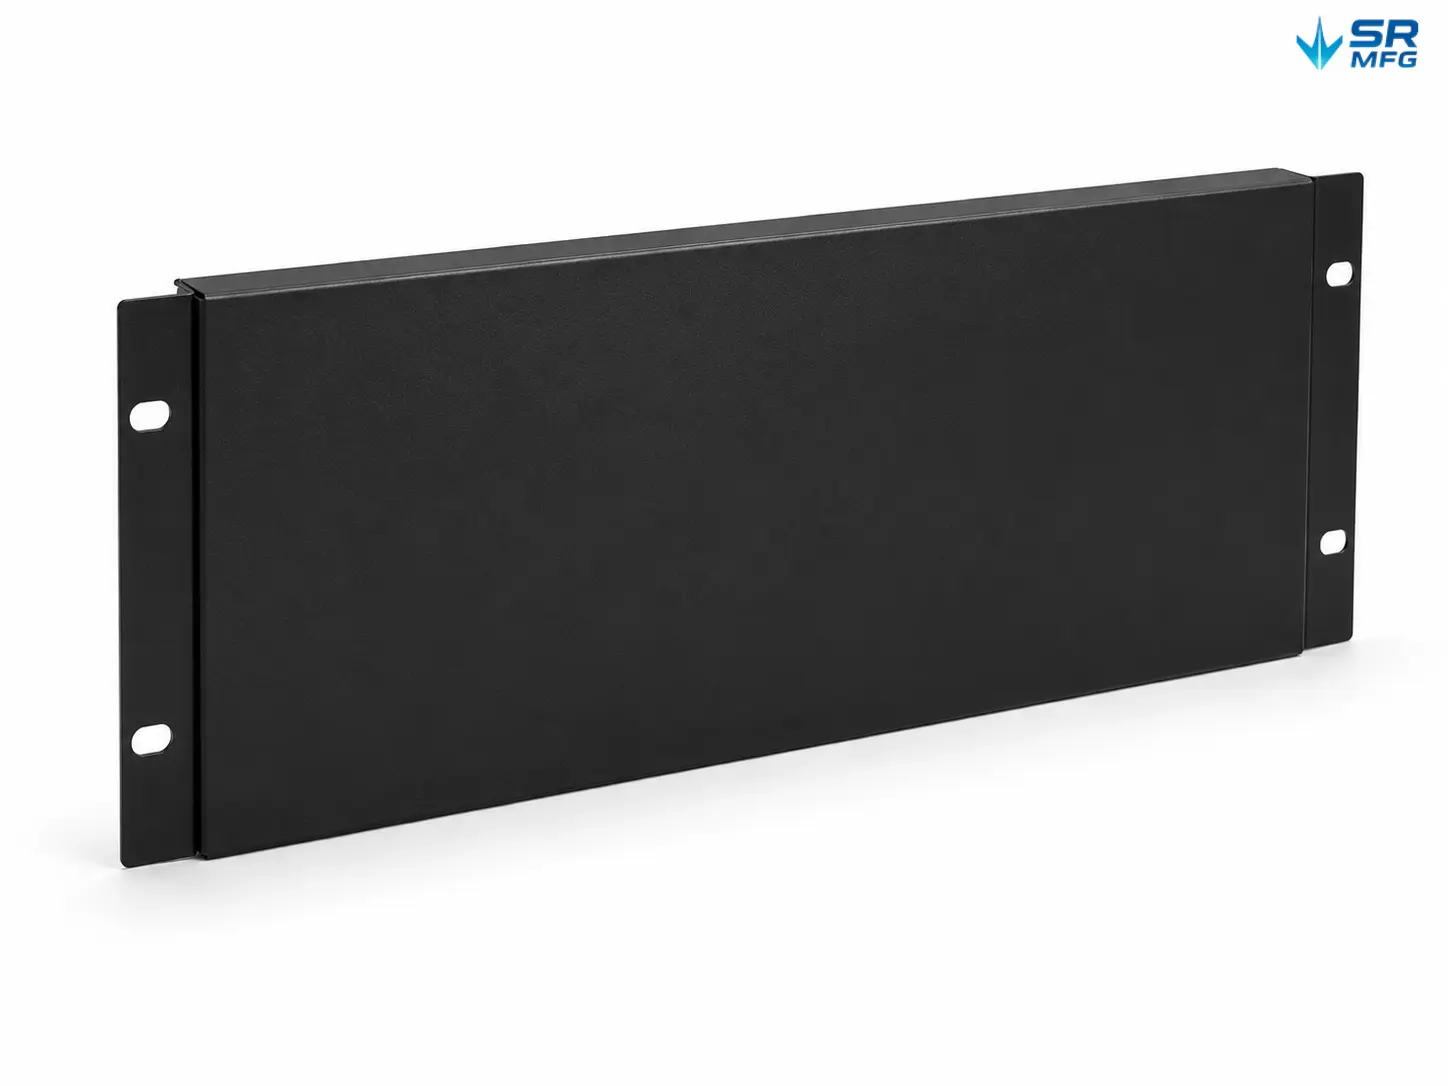
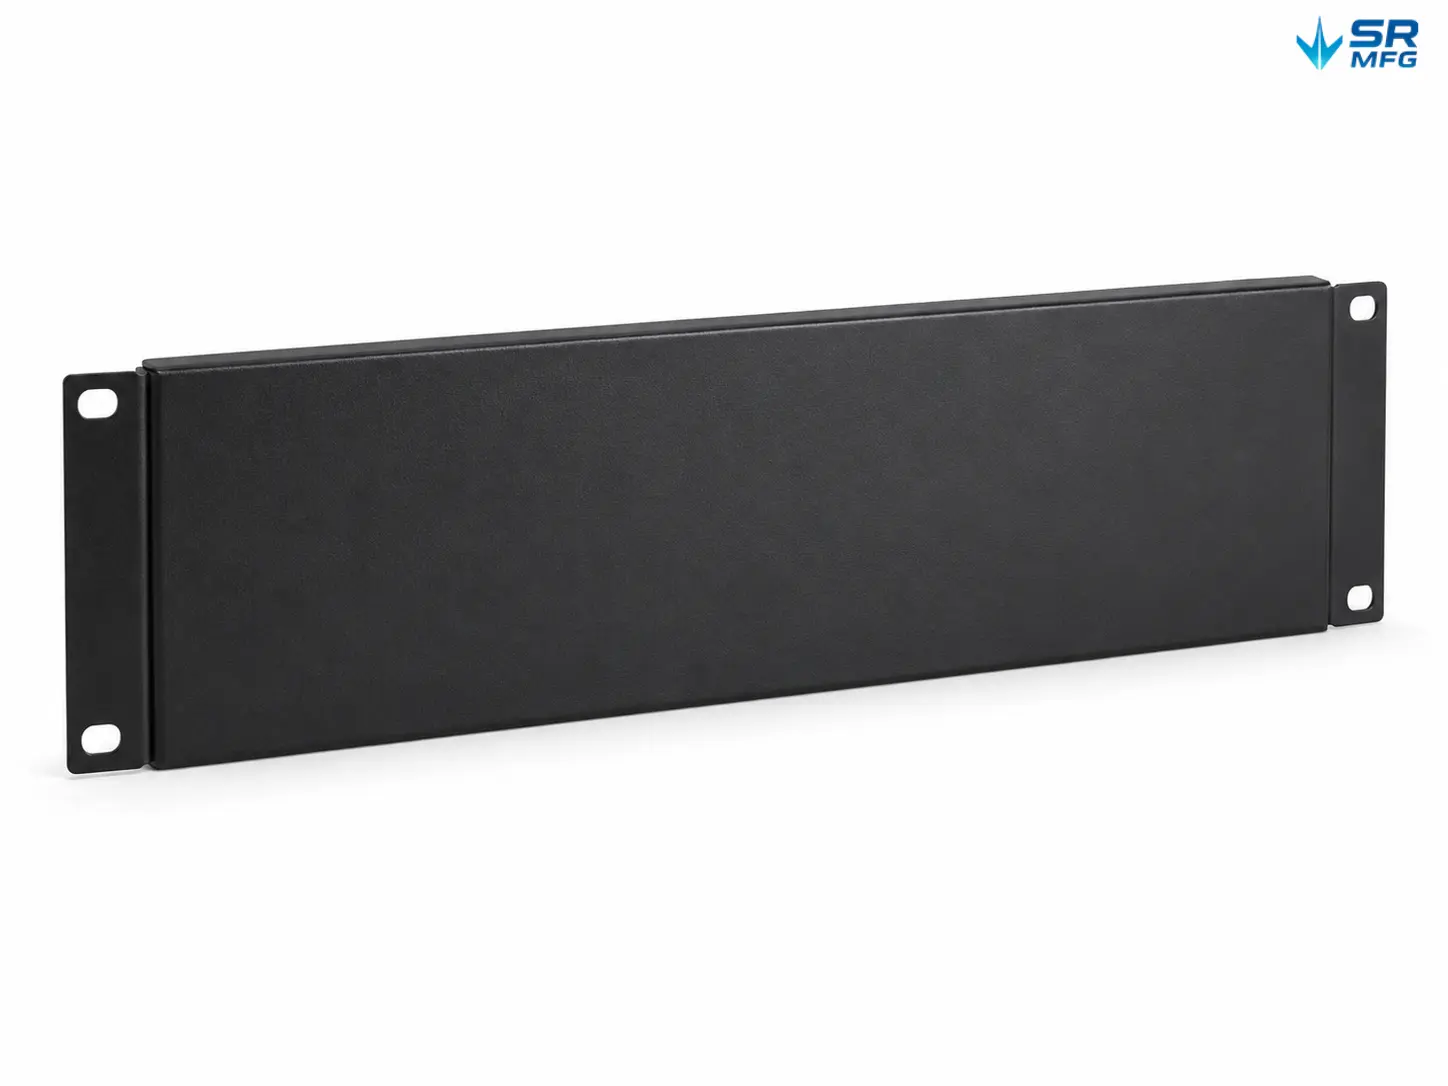
- Server rack frames & rails
- Cable management trays
- Cabinet panels & doors
- Mounting brackets & plates
Unterhaltungselektronik
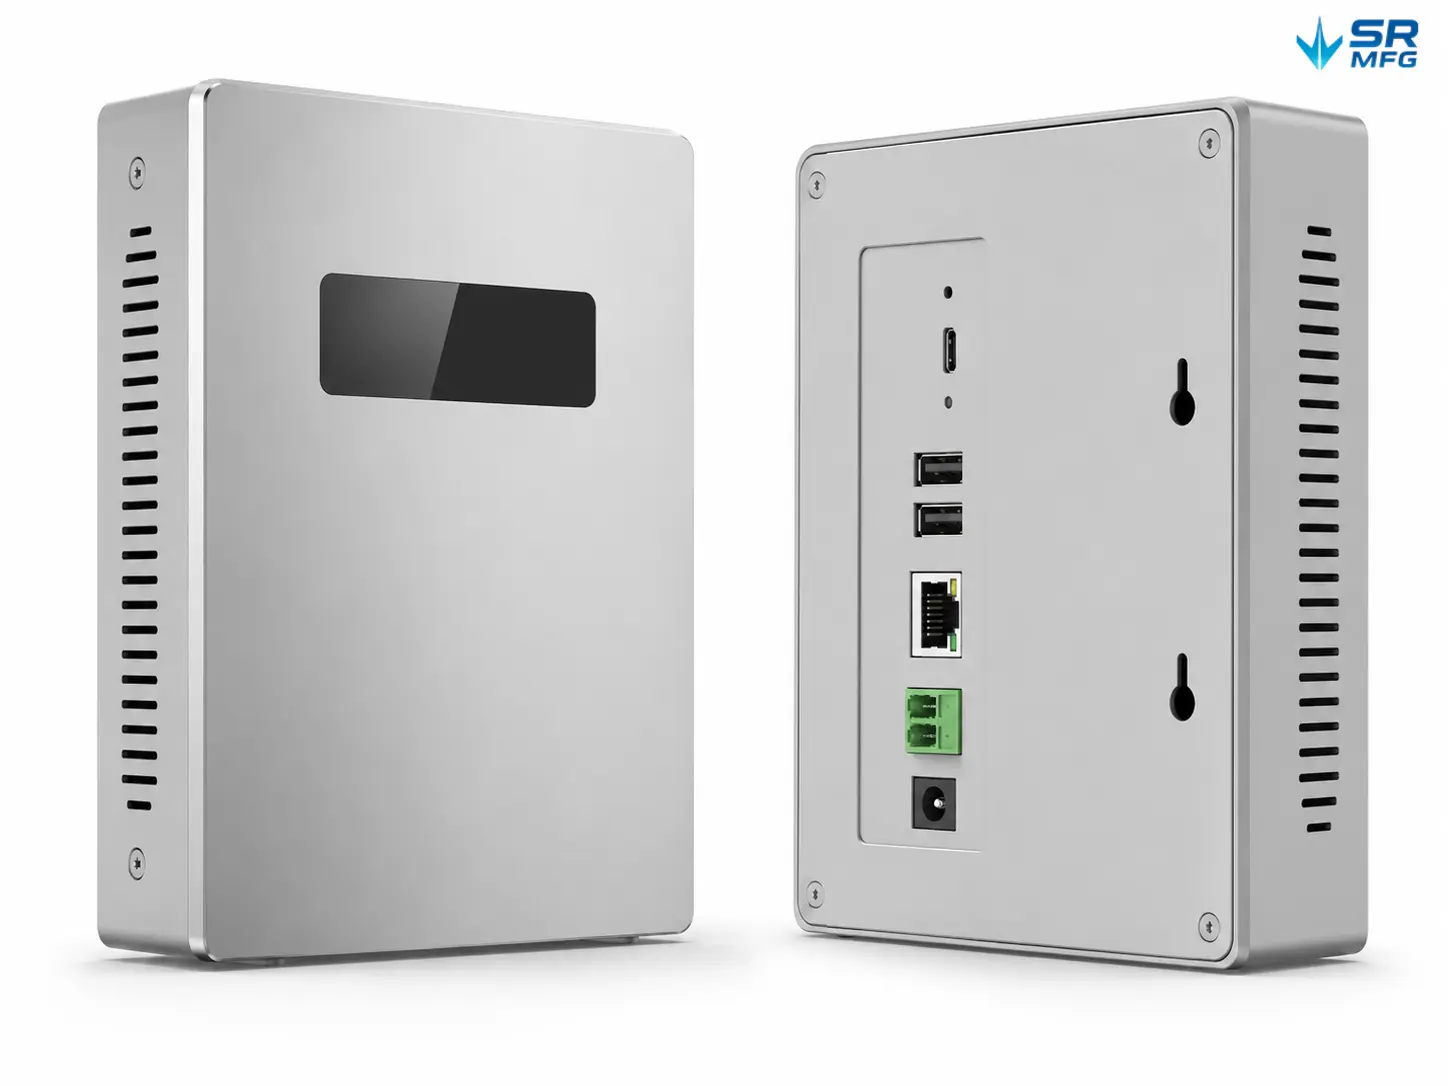
Grinding solutions for consumer electronics housings, internal brackets, display structures, and precision sheet metal assemblies that require clean edges and controlled surface quality.
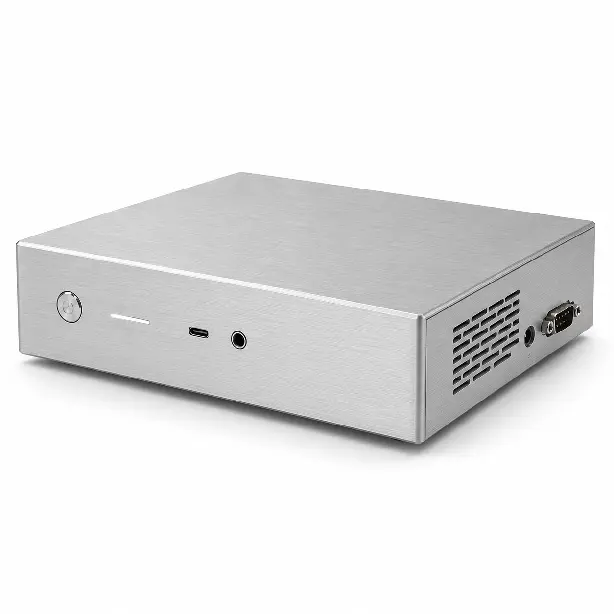
- Device housings & covers
- Internal support brackets
- Display mounting structures
- Speaker & audio metal parts
- Small precision formed parts
Elektrische Geräte
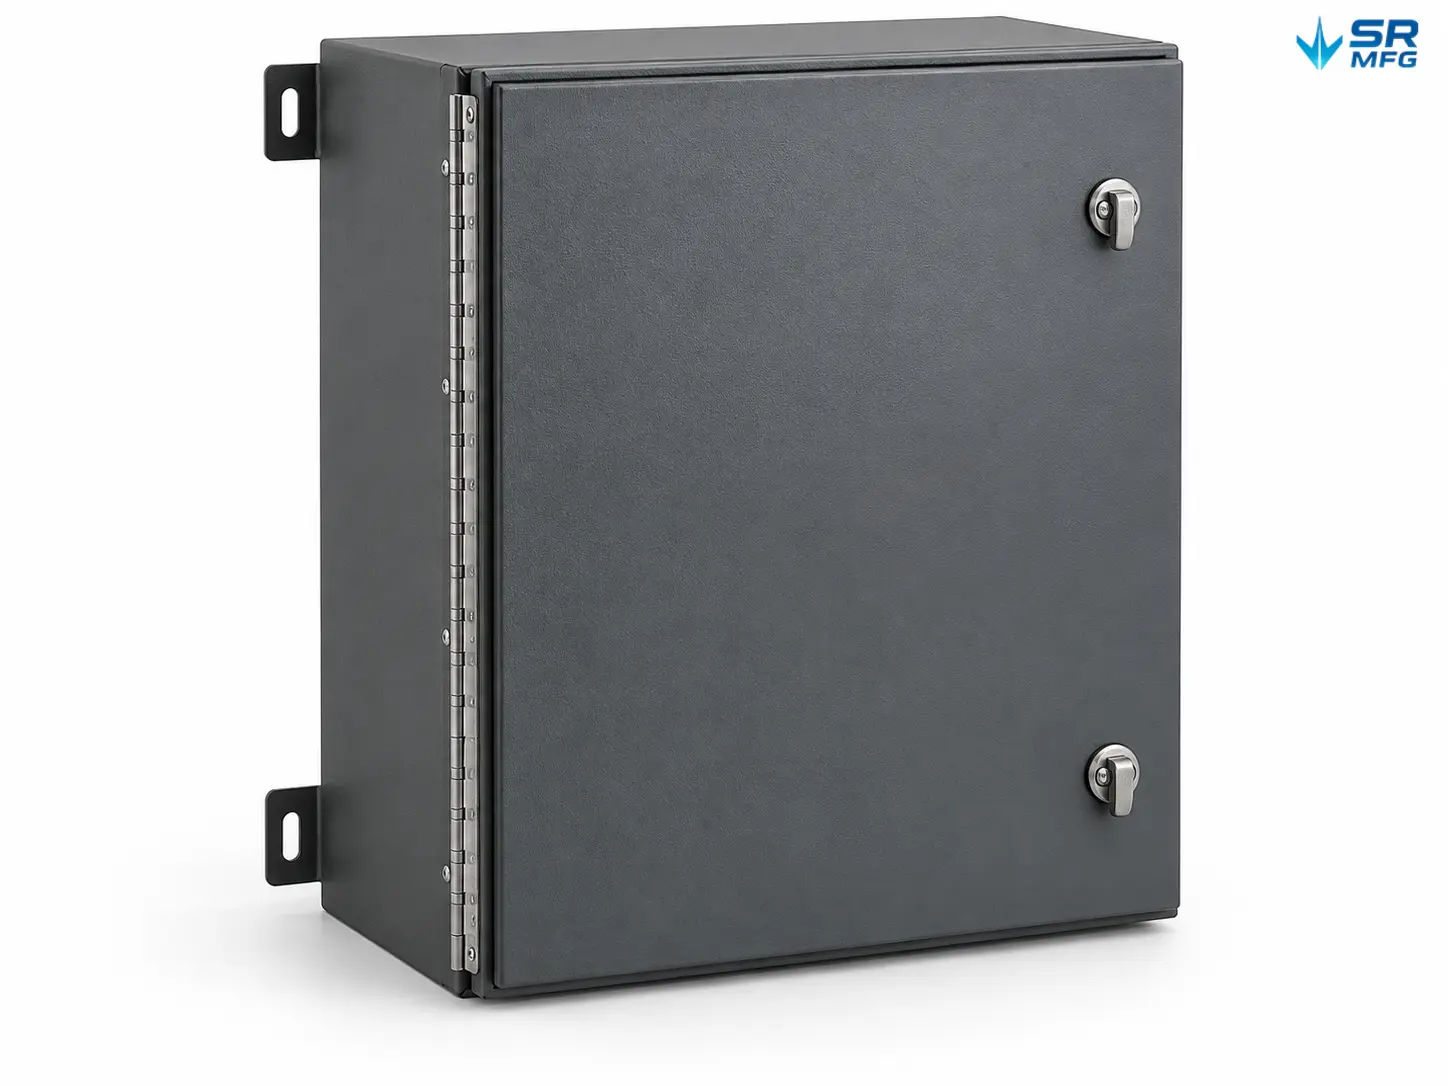
Metal grinding for electrical enclosures, control cabinets, power distribution units, and industrial electrical systems where edge safety, surface preparation, and fit consistency matter.
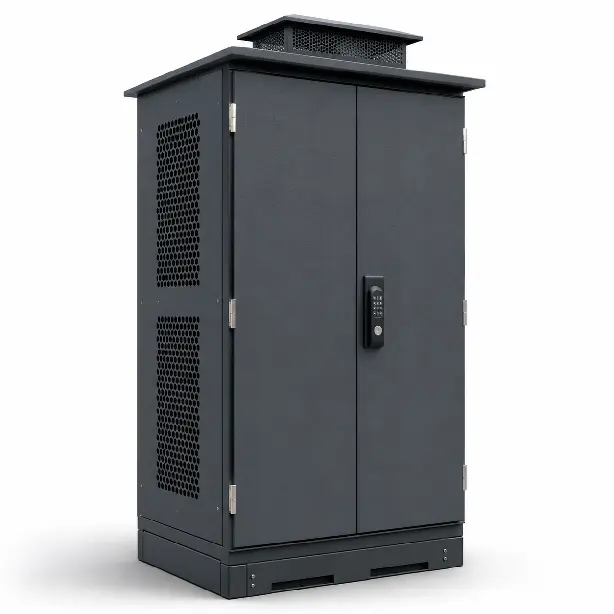
- Electrical cabinet enclosures
- Control box panels
- Terminal mounting plates
- DIN rail brackets
- Ventilation and access panels
Industrieausrüstung
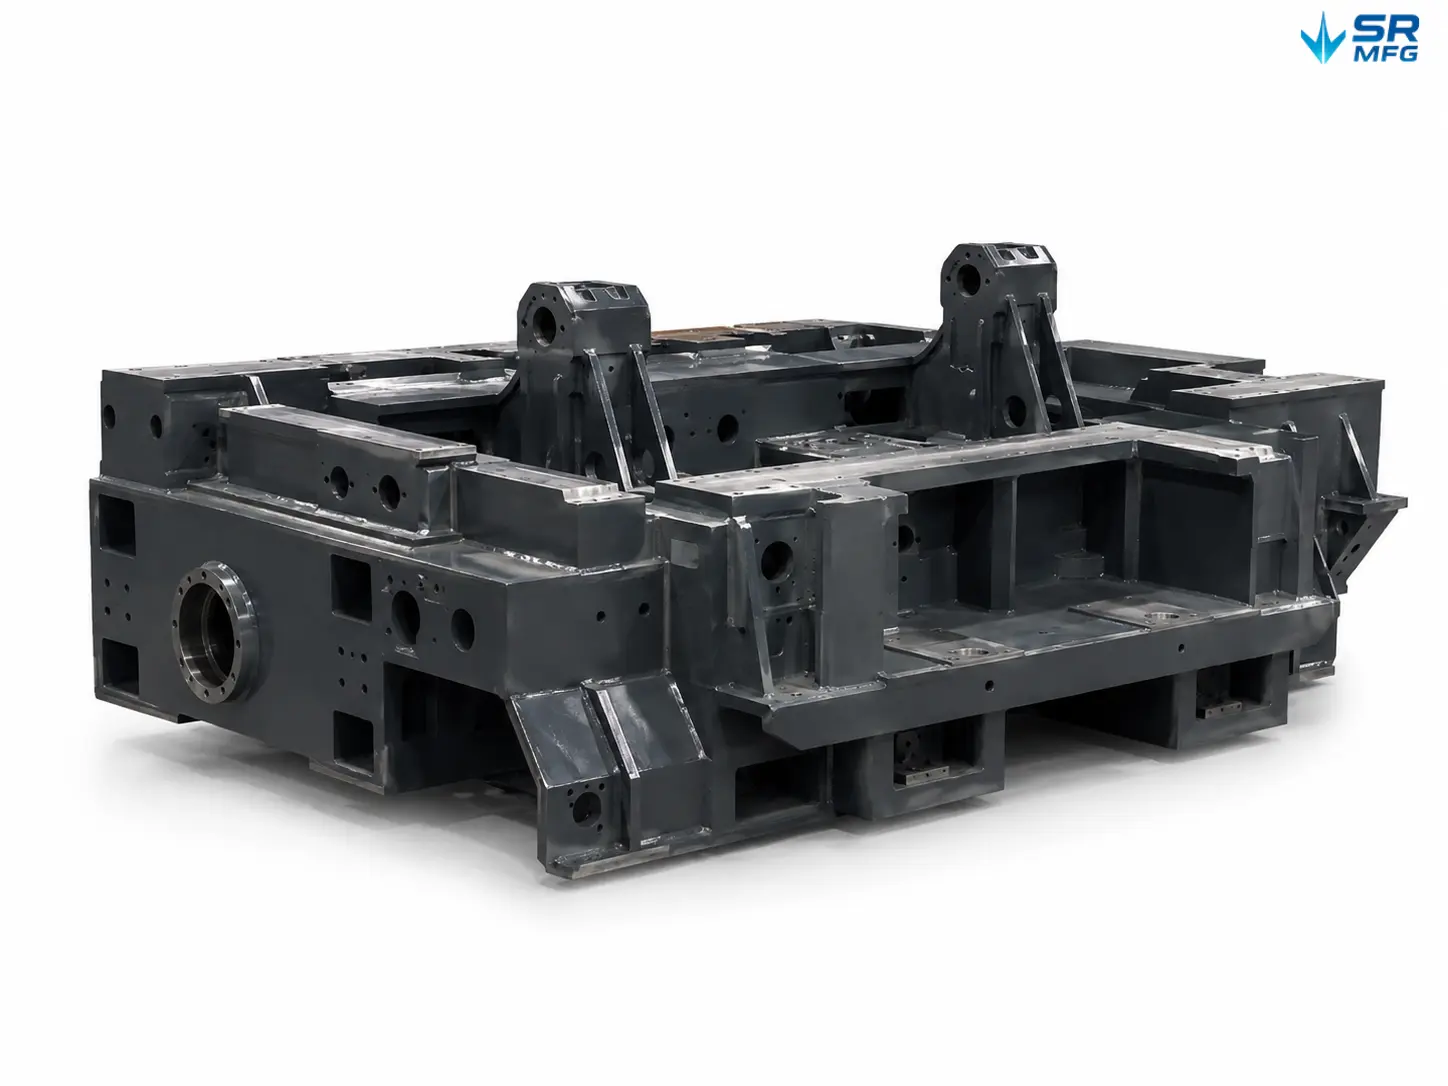
Grinding services for machinery, automation systems, production equipment, and structural machine assemblies that require burr removal, weld smoothing, and surface correction.
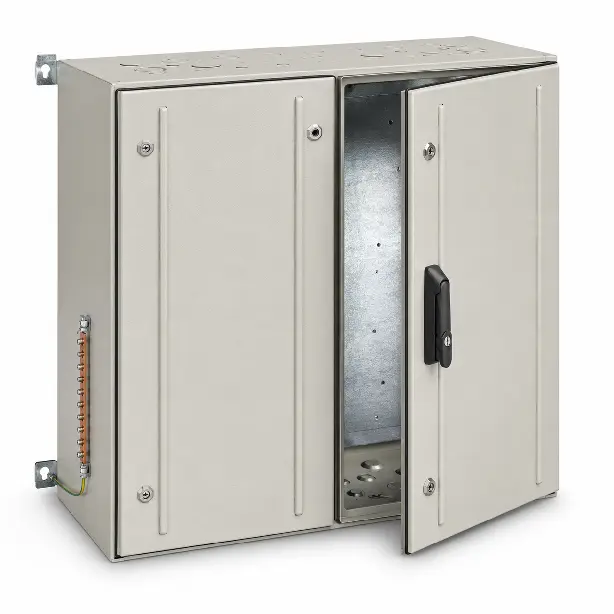
- Machine covers & guards
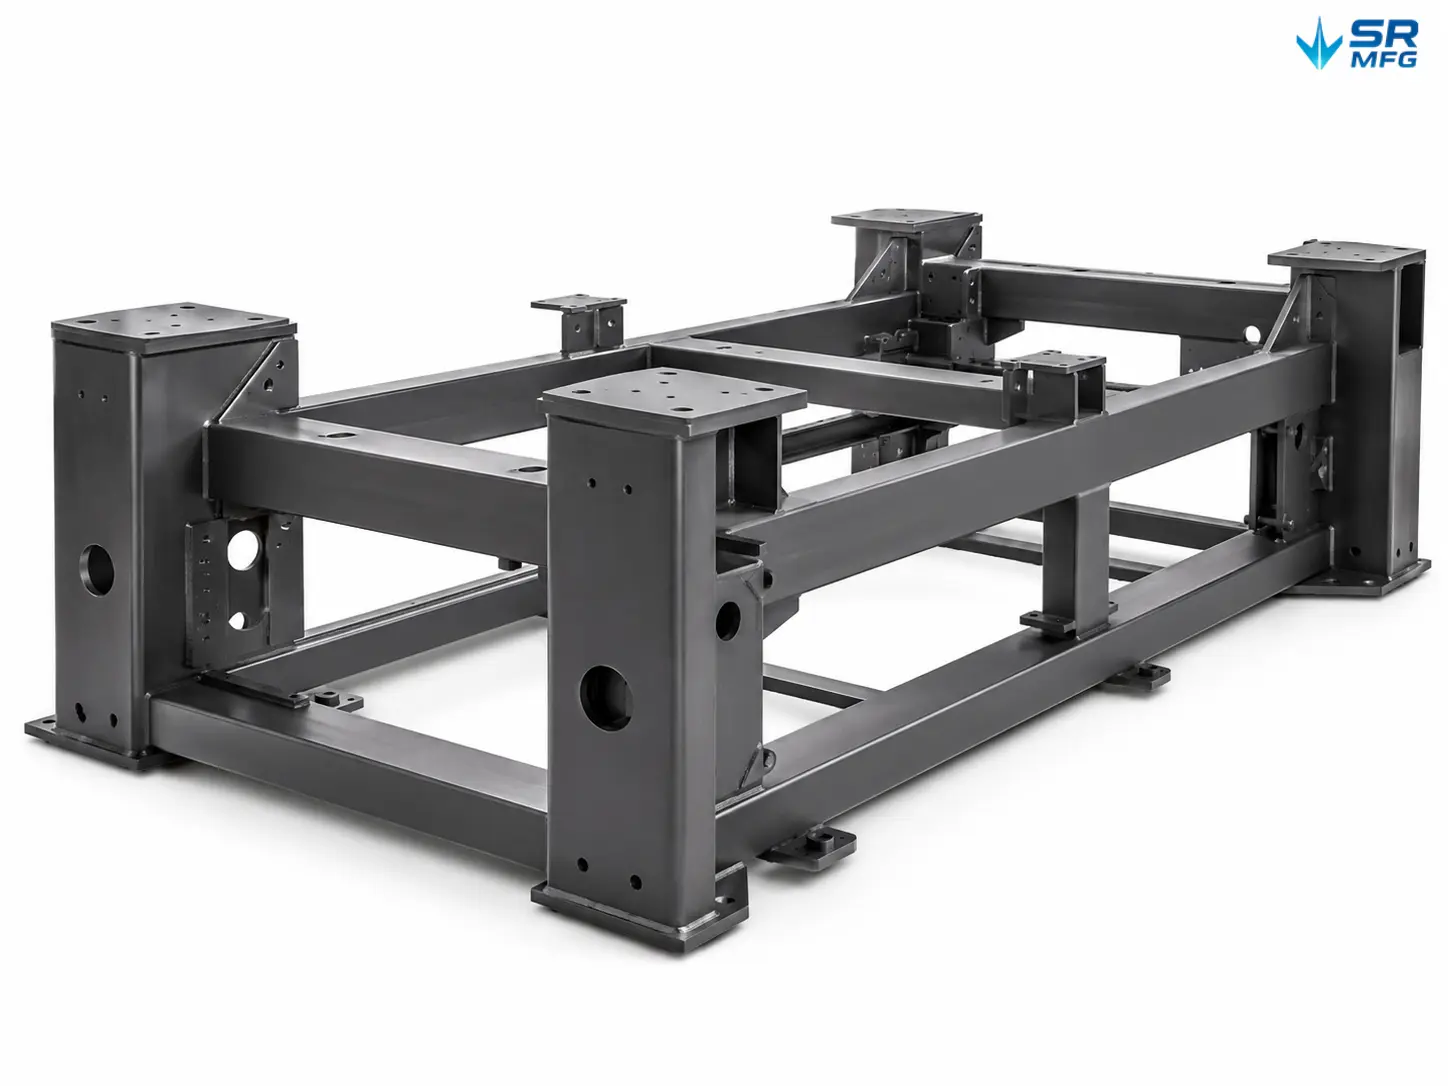
- Equipment frames
- Conveyor brackets
- Sensor mounting plates
- Protective panels & shields
New Energy Systems
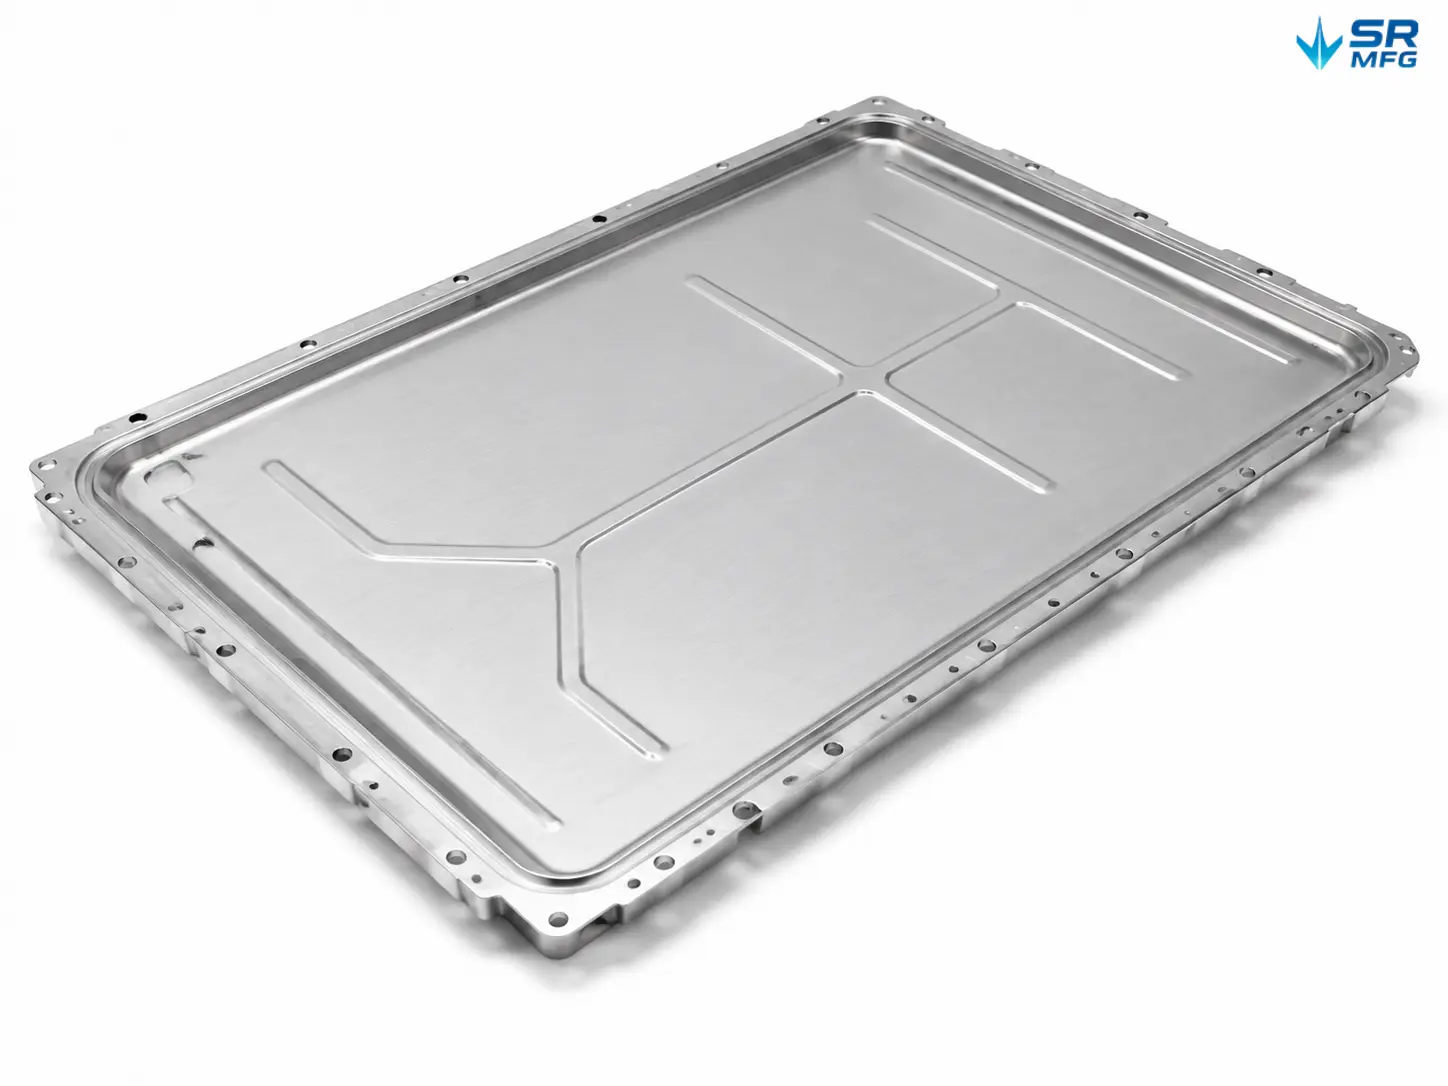
Metal grinding for EV charging equipment, battery systems, energy storage cabinets, and power conversion units where clean edges, weld blending, and surface preparation are required.
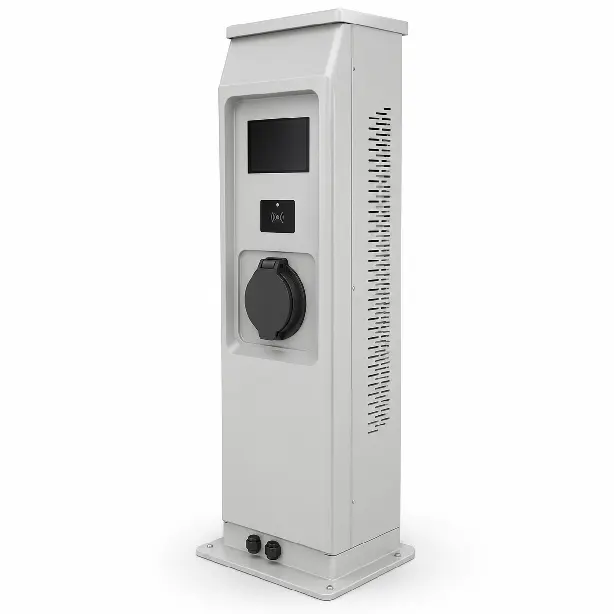
- Battery enclosure parts
- Charging station cabinets
- Energy storage cabinet panels
- Busbar support brackets
- Power module housings
Outdoor Equipment
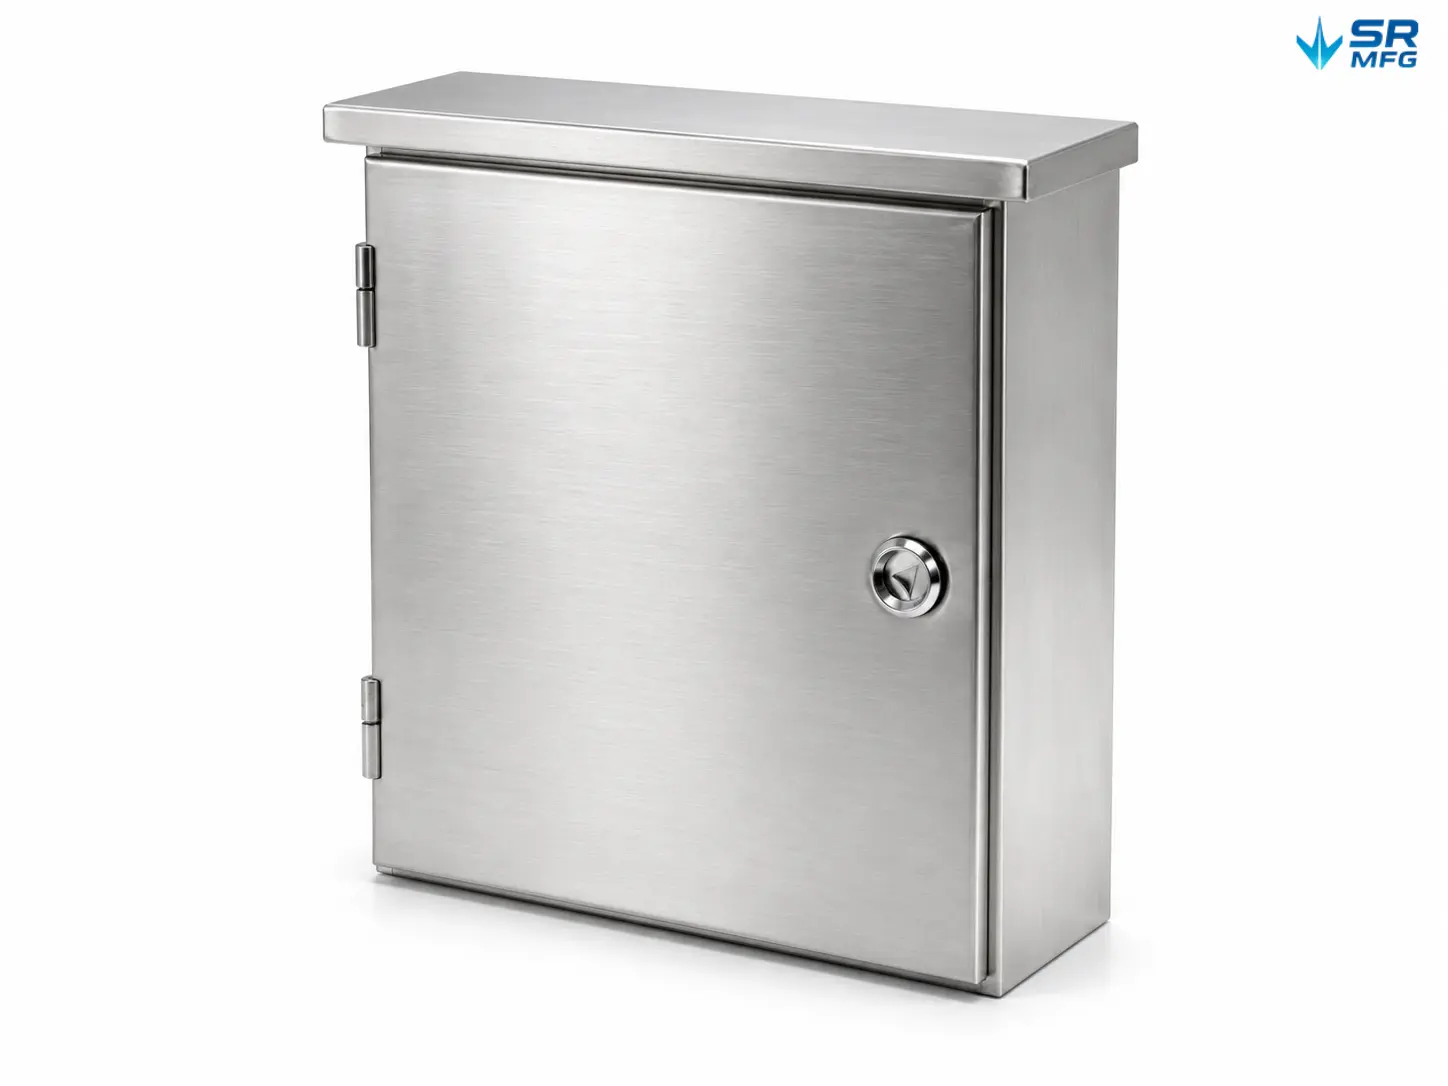
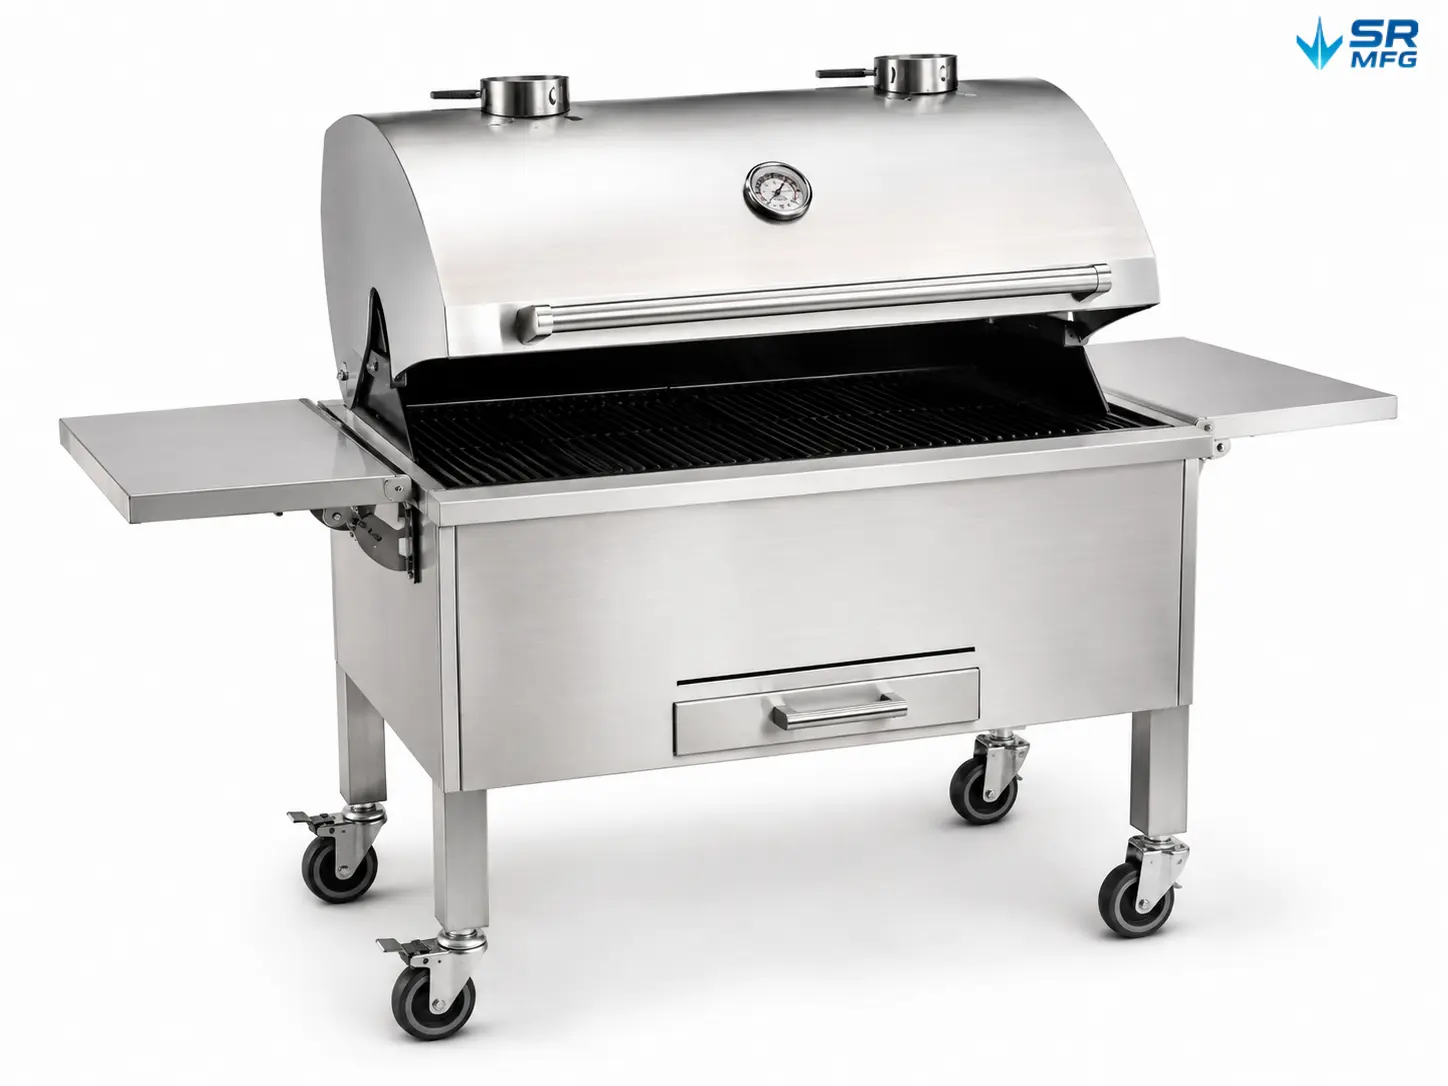
Grinding services for outdoor enclosures, equipment covers, BBQ grills, lighting systems, and structural fixtures that require safer edges, cleaner weld areas, and better preparation for final finishing.
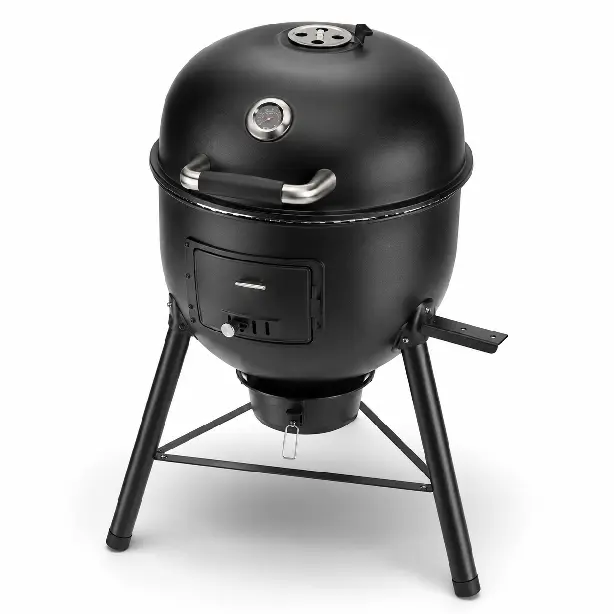
- Outdoor equipment housings
- BBQ grill sheet metal bodies
- Protective covers & panels
- Mounting brackets
- Weather-resistant structural parts
Built for Your Application
Whether you need a single prototype or stable batch production, SR MFG provides controlled metal grinding to improve surface flatness, weld transitions, surface consistency, assembly fit, and readiness for downstream finishing.
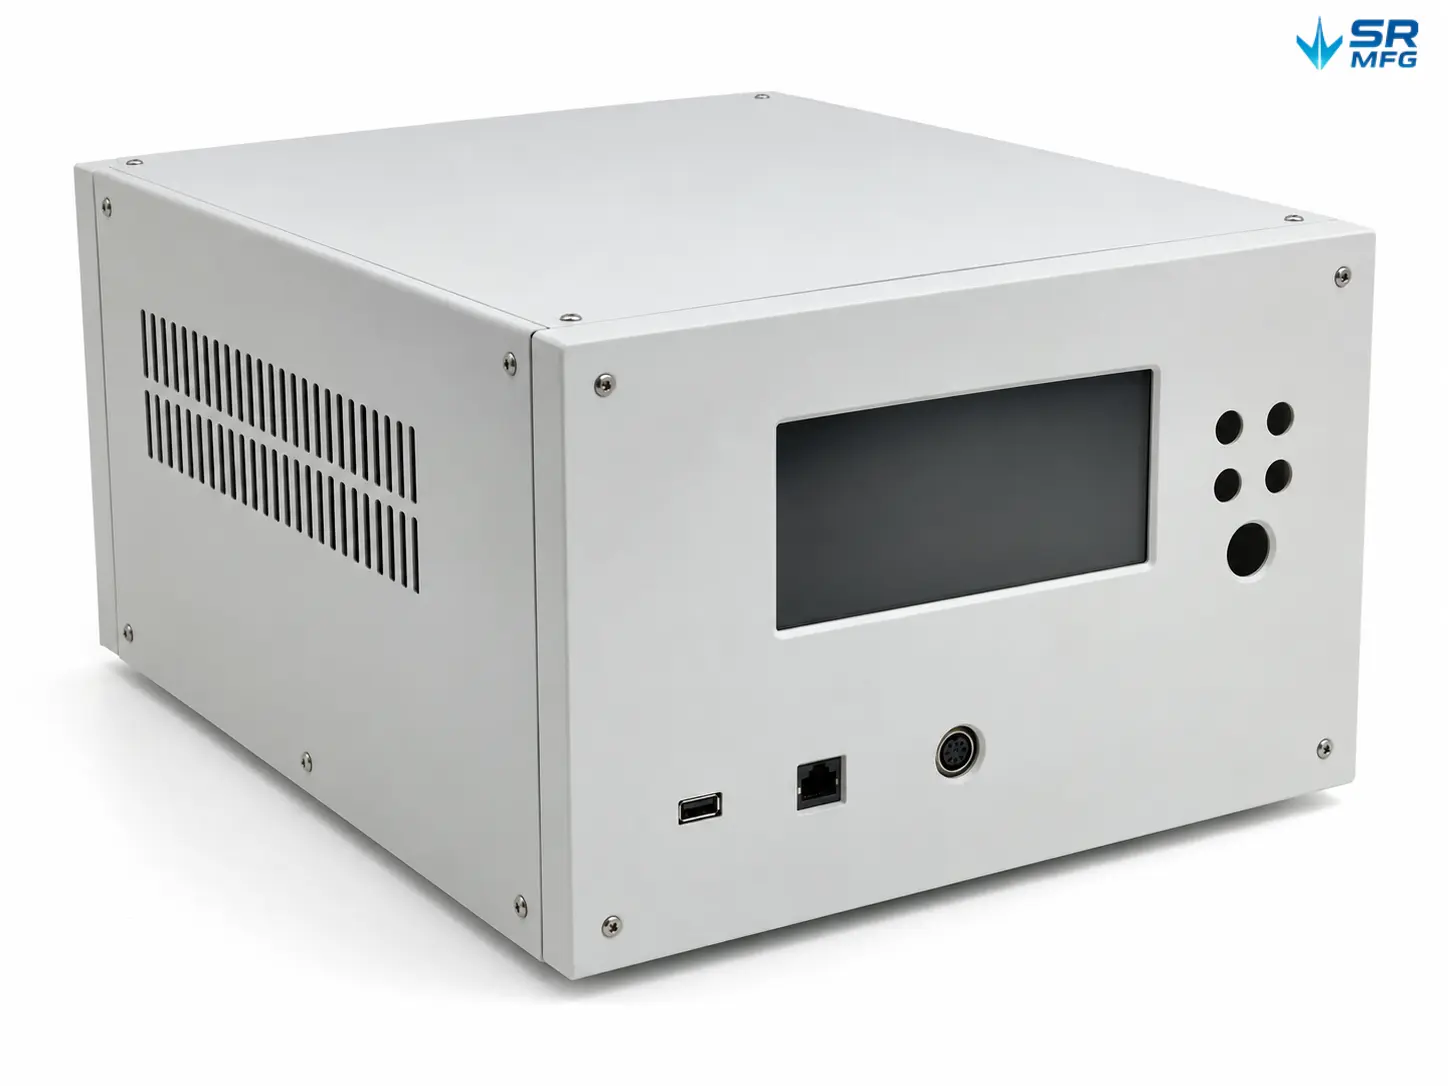
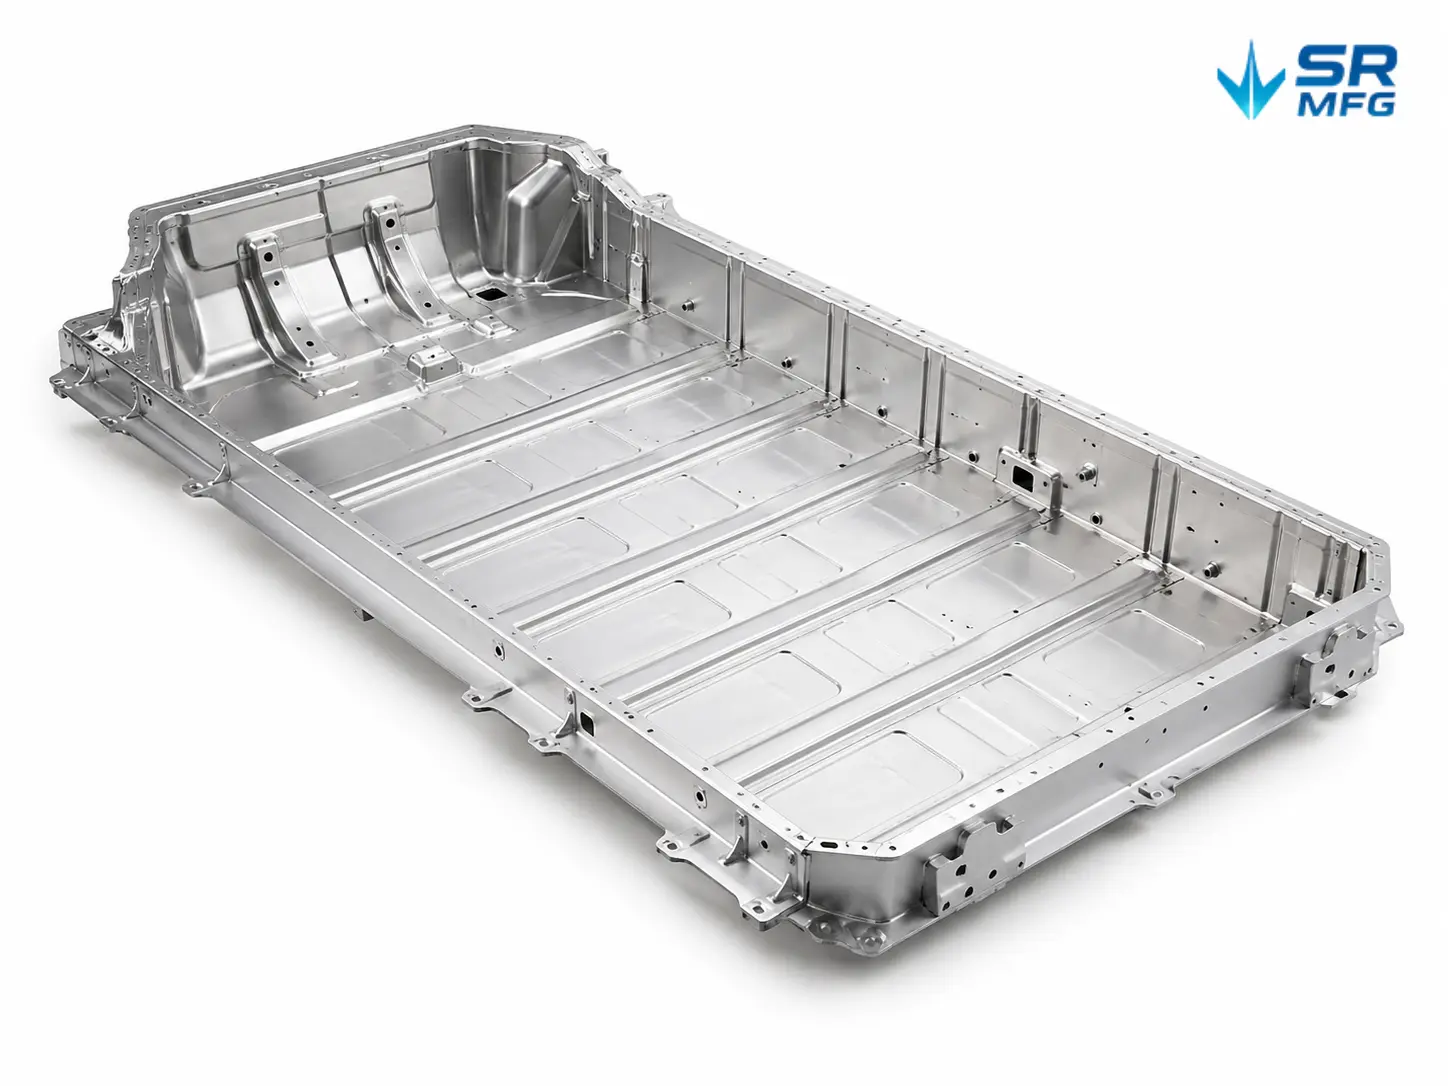
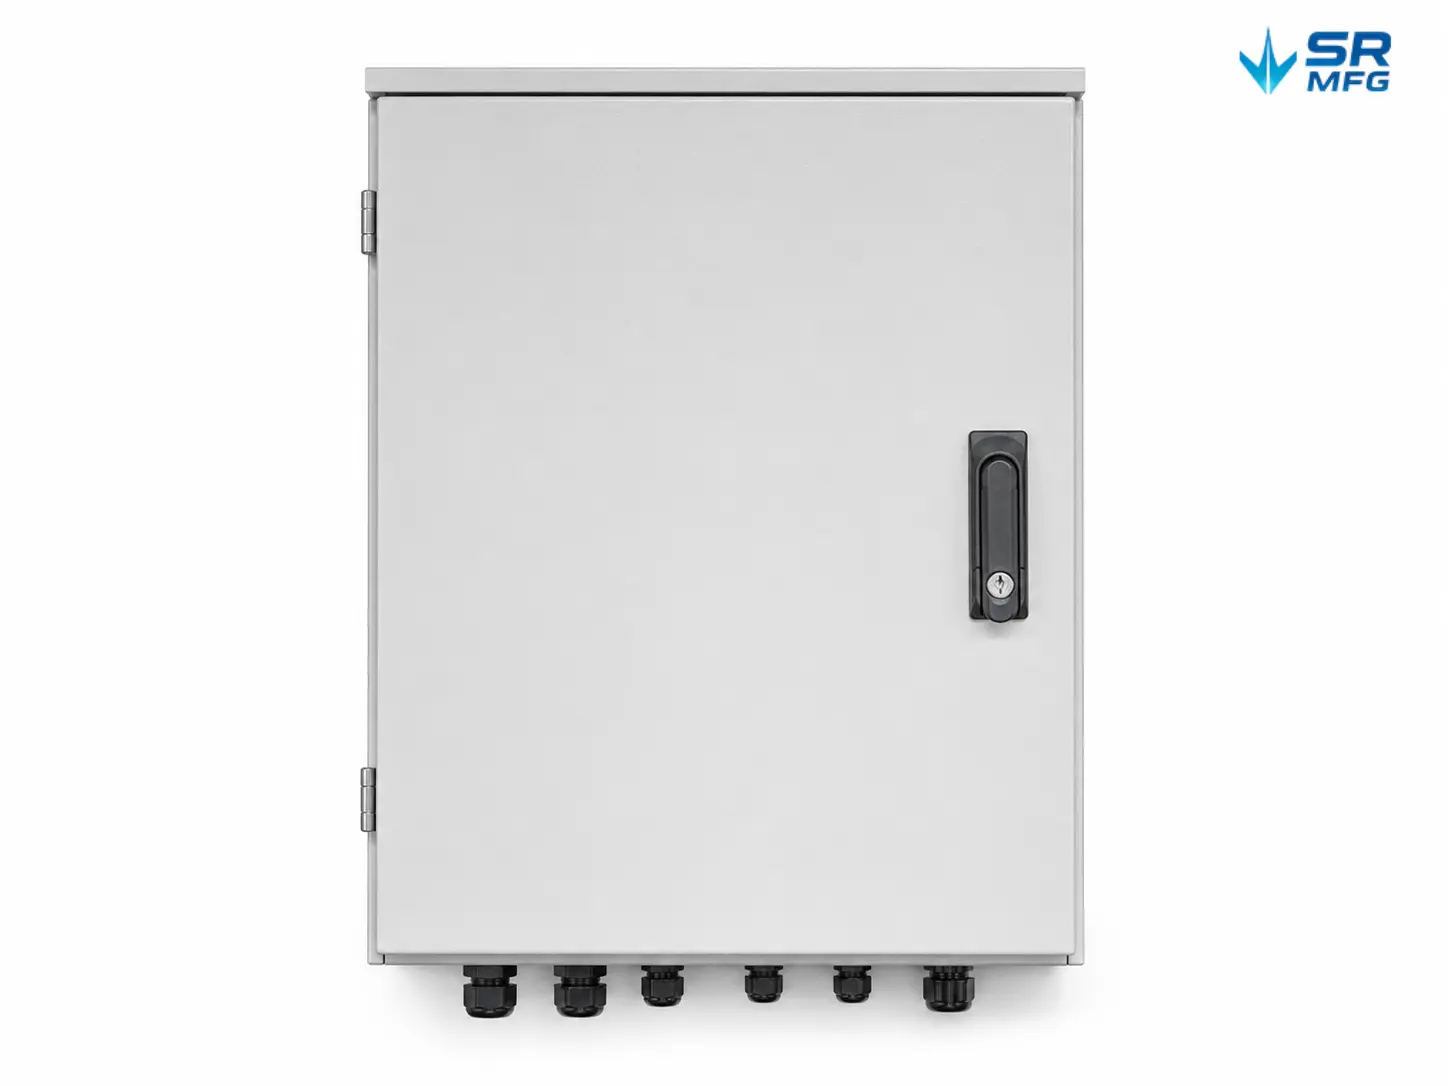
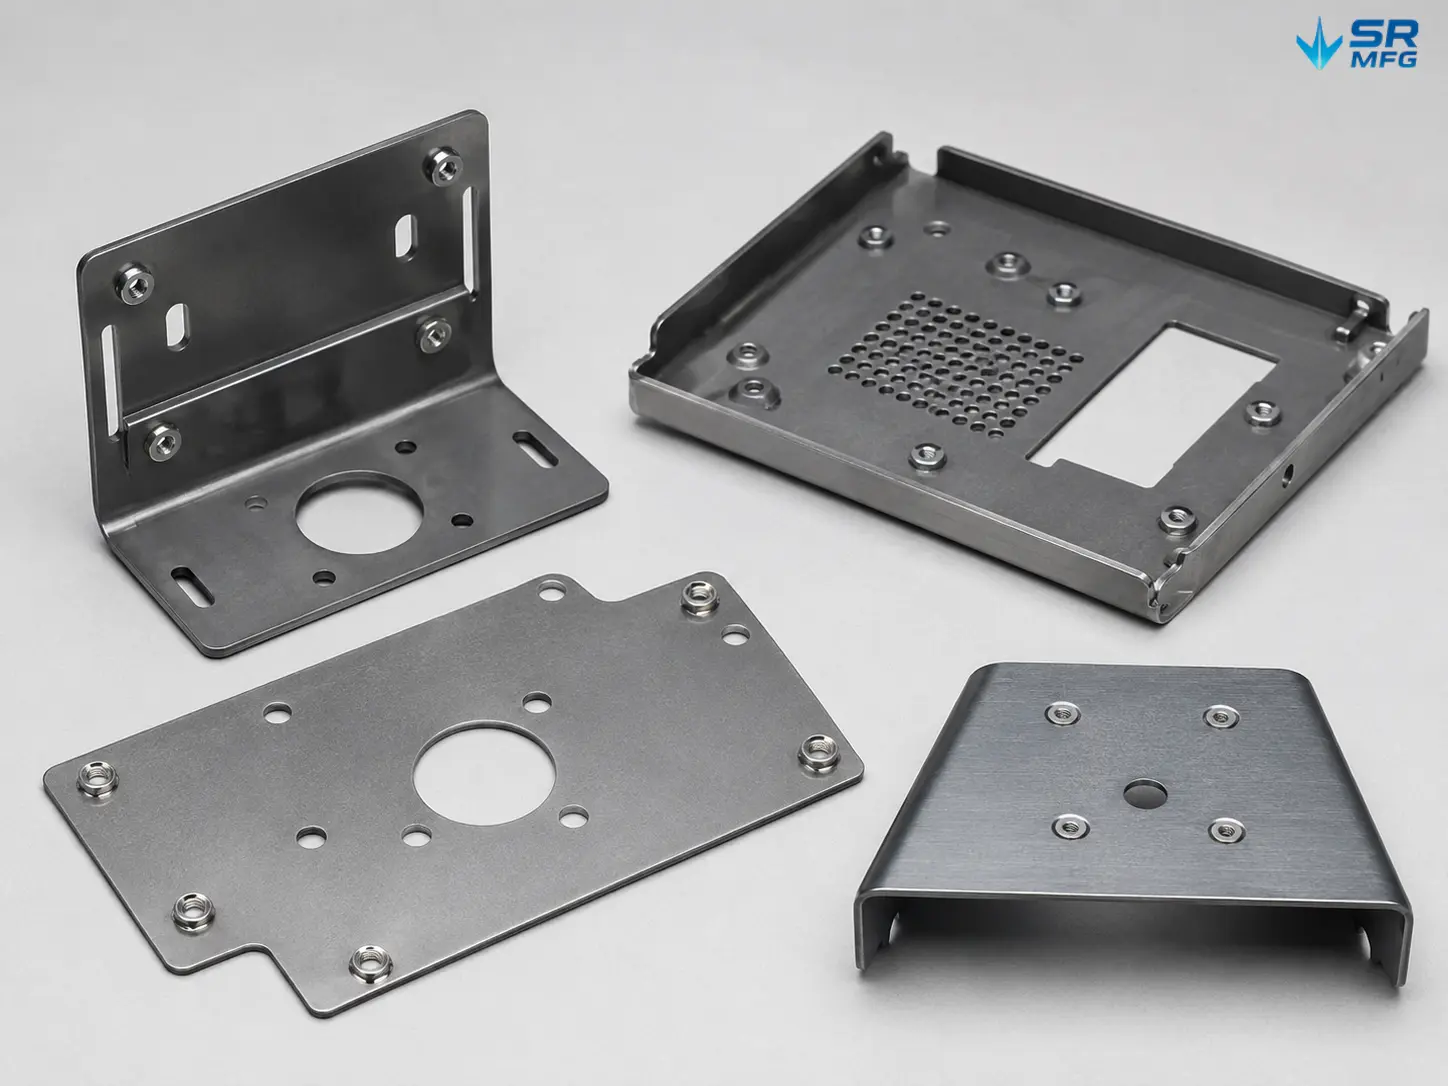
Sheet Metal Parts for Grinding Applications
Metal Grinding Häufig gestellte Fragen
It depends on your goal and where the part will be used. Choose grinding when you need controlled material removal to eliminate cutting marks, weld steps, dents, deep scratches, or to build a consistent “base texture” for brushing or coating. Grinding is primarily about shaping, defect removal, and creating a stable surface foundation. Choose polishing when your main objective is to further reduce roughness and increase gloss/reflectivity while minimizing changes to part geometry—polishing is more about surface refinement. A common route is grind (coarse → fine) to remove defects and heavy lines, then polish to reach a higher cosmetic grade (bright or mirror-like).
Yes. Grinding removes material and can change thickness, edge geometry, or local features. The best way to control risk is to define measurable acceptance criteria up front: specify allowable stock removal (e.g., “cosmetic surface treatment only—must not affect critical dimensions/fit surfaces,” or state a maximum removal). Use masking/protection for critical areas such as threads, sealing faces, grounding points, and mating surfaces. Lock the process window (abrasive grit sequence, pressure, speed, pass pattern) and sign off a first-article reference sample. Close the loop with inspection: perform FAI plus in-process sampling and final inspection on CTQs, tied to cosmetic acceptance.
A practical spec is: Ra + grain direction + A/B surface scope + approved reference sample. Ra is an acceptance metric; abrasive “grit” is only a process reference because the outcome also depends on pressure, speed, consumable wear, lubrication, and material. The same grit does not guarantee the same finish. If a grit must be included, you can attach a rough grit-to-Ra reference table (e.g., 180 grit ≈ 0.76 µm Ra; 240 grit ≈ 0.38 µm Ra), but acceptance should still be based on Ra (or Ra max). Make grain direction visual in the drawing (arrows or lay symbols; ISO 1302 supports this). Also define the measurement rule—where to measure, how many locations, and whether you accept by max value or average. ISO 4288 provides a framework for measurement and evaluation, and common practice is to measure at the location expected to be roughest and apply a defined decision rule (often a max-limit rule).
Example callout format:
A-surface: HL/#4 brushed; grain direction →; Ra ≤ X µm (or Ra X–Y µm); accept per approved sample.
B-surface: Ra ≤ X µm; direction not specified (or non-directional).
Yes—and for A-surfaces and critical mating areas, it is strongly recommended (standard or on request). Roughness is typically measured with a stylus profilometer for Ra (and Rz when required), and reports can include measurement locations, values, instrument details, and conditions. For geometry/dimensions, we can provide inspection records for key dimensions and GD&T features (flatness, parallelism, etc.) per drawing requirements, creating a complete delivery package together with the approved cosmetic sample.
Rust prevention depends on the material. Carbon steel/cold-rolled steel can flash-rust within minutes to hours after grinding and cleaning, so the sequence should be “clean → fully dry → protect immediately,” using rust-preventive oil/inhibitors or VCI packaging for enclosed protection. For stainless steel, avoid cross-contamination from carbon-steel tooling or shared abrasives—free-iron contamination can lead to rust spots; passivation can be used when needed to remove free iron and restore corrosion resistance. For scratch prevention on cosmetic parts, use temporary protective film on A-surfaces, layer separation and cushioning (PE foam/EPE sheets, corner guards), and treat cleaning and drying + isolated packaging as standard—residual abrasive or metal fines can act like sandpaper during transit.
Metal Grinding Technical Resources
Stainless Steel Sheet Metal Fabrication Services for Automation and Energy Equipment
ShuangRui2026-06-30T03:15:01+00:00November 5, 2025|
Understanding Stainless Steel Sheet Metal Fabrication for Automation and Energy Equipment Stainless steel sheet metal fabrication integrates precision [...]
Acceptance Criteria in Manufacturing: How to Define Pass/Fail Rules on Drawings
ShuangRui2026-08-27T03:25:20+00:00August 20, 2026|
Acceptance criteria are the pre-established, measurable conditions that a manufactured part must satisfy before it is approved for [...]
What Is Process Planning in Manufacturing? 6 Steps from Drawing to Production
ShuangRui2026-08-28T07:57:56+00:00August 6, 2026|
Why Most People Get Process Planning Wrong When engineers and buyers hear "process planning," they tend to picture [...]
Unit Price in Manufacturing: How It’s Calculated and What B2B Buyers Should Compare
ShuangRui2026-08-27T03:41:28+00:00August 21, 2026|
When a supplier sends you a quote for 5,000 sheet metal brackets, the number that matters most is [...]
