Specifying oiled stock sounds like a minor surface preference—until the laser hits the material and the cutting chamber fills with smoke, or the dry sheets arrive at your facility with flash rust after a week in humid storage, and the entire batch needs rework before it can even load onto the machine.
The choice between oiled and dry sheet metal is not about which surface is “better.” It is about how that surface condition interacts with the laser cutting process, affects downstream operations like welding and coating, and determines whether your parts arrive at the next stage of production clean, rust-free, and within specification.
The Surface Condition Misconception
Many engineers and buyers treat surface condition as a cosmetic detail. In laser cutting, it is a process variable.
Hot Rolled Pickled and Oiled (HRP&O) steel has been acid-pickled to remove mill scale, then coated with a thin layer of rust-preventive oil (typically 0.5–1.5 g/m²). The oil is not a lubricant for cutting—it is a barrier against oxidation during storage and transport.
Dry sheet (also called dry cold rolled or dry hot rolled) has no oil film. It leaves the mill with a clean, bare surface. Some mills apply a very light dry-film rust inhibitor, but the surface is essentially oil-free.
The misconception is that the oil layer is too thin to matter. In practice, even 0.5 g/m² of oil changes how the laser interacts with the material surface, how much post-processing your parts need, and how carefully you must store the stock before use.
How Oil Affects the Laser Cutting Process
Smoke and Fume Generation
When a laser beam hits oiled steel, the oil vaporizes instantly. This produces visible smoke and fine particulate matter inside the cutting enclosure. The effect is more pronounced with:
- Thinner oil films (below 1 g/m²) that vaporize quickly and create a brief flare
- Higher laser power settings that increase thermal input
- Enclosed cutting chambers where fume extraction capacity is limited
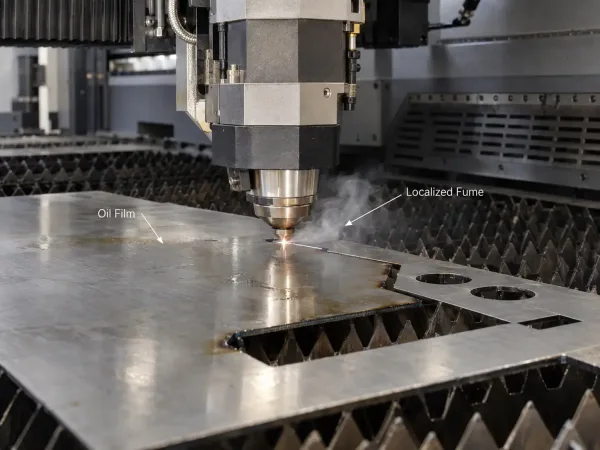
Oiled steel being cut by a fiber laser, showing localized smoke generated as the surface oil vaporizes.
Most modern fiber laser cutters have extraction systems rated for this level of smoke. However, if your machine runs at high duty cycles with oiled stock, the extraction filters load faster and require more frequent maintenance. This is a cost factor that rarely appears on the material price quote but shows up in equipment uptime and consumable expenses.
Edge Quality and Oxidation
The oil film has a measurable effect on the cut edge. During cutting, the oil contributes a small amount of carbon to the kerf zone. On mild steel, this typically produces:
- Slightly darker cut edges compared to dry stock, due to a thin oxide layer formed during the exothermic reaction of burning oil
- Marginally higher surface roughness (Ra) on the cut face, though usually within acceptable limits for most applications
- More pronounced heat-affected zone (HAZ) at the edge, typically 0.1–0.3 mm wider than dry stock cuts
For parts that will be welded, coated, or used in precision assemblies, these differences matter. For general fabrication where edge cosmetics are secondary, the effect is negligible.
Cutting Speed and Gas Consumption
In most cases, oiled stock does not require a significant change in cutting speed or assist gas pressure. The oil layer is too thin to act as a thermal barrier. However, some operators report:
- Oxygen-assisted cutting: Oil combustion can slightly reduce the exothermic contribution of oxygen, requiring a 2–5% increase in gas flow for consistent edge quality
- Nitrogen-assisted cutting: Minimal impact, as nitrogen is inert and the oil burns off independently
- Very thin sheets (below 1 mm): Oil vaporization can cause micro-variations in the cut path, visible as slight edge waviness on tight-tolerance parts
The Hidden Costs of Oiled Stock
Degreasing Requirements
Parts cut from oiled stock almost always require degreasing before welding, powder coating, painting, or assembly. The cost depends on the method:
| Method | Typical Cost per Part | Best For |
|---|---|---|
| Solvent wipe (manual) | 0.50–1.50 | Small batches, simple geometry |
| Alkaline wash (automated) | 0.20–0.80 | Medium to large batches |
| Vapor degreasing | 1.00–2.50 | High-purity requirements |
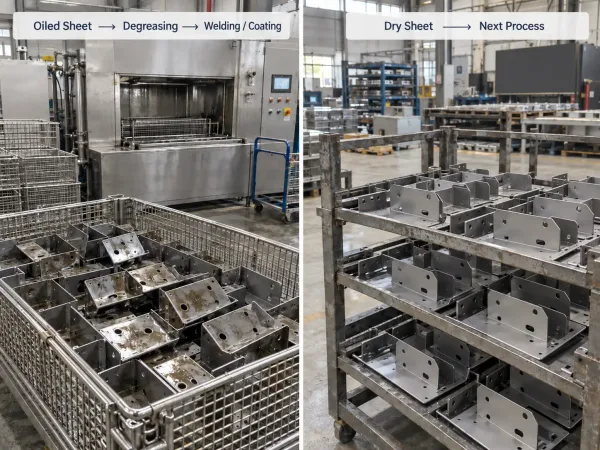
Comparison of the downstream preparation required for oiled and dry laser-cut sheet metal parts.
For a batch of 500 laser-cut brackets, degreasing adds 100–500 to the total cost. This is not a line item on the material quote, but it is a real manufacturing cost that procurement teams should account for when comparing oiled vs dry stock pricing.
Storage and Handling
Oiled stock has a shelf life. The oil film degrades over time, especially in:
- High-humidity environments (above 60% RH): Oil absorbs moisture and loses its protective function within 3–6 months
- Temperature cycling: Repeated heating and cooling breaks down the oil film, leaving bare spots vulnerable to corrosion
- Stacked storage without interleaving: Sheets in direct contact can transfer oil unevenly, creating inconsistent surface conditions
If your production schedule requires storing sheet stock for more than 30 days, oiled stock needs periodic inspection and may require re-oiling or repositioning.
The Risks of Dry Stock
Flash Rust and Surface Contamination
Dry steel is vulnerable to corrosion from the moment it leaves the mill. In controlled indoor environments (below 50% RH, stable temperature), dry stock can remain rust-free for weeks. In practice, most fabrication shops do not maintain ideal storage conditions.
Flash rust—a thin, uniform layer of surface oxidation—can form on dry stock within 24–72 hours in humid conditions. While flash rust does not significantly affect laser cutting quality (the laser burns through it), it creates problems downstream:
- Weld porosity: Rust at the joint introduces oxygen into the weld pool
- Coating adhesion failure: Powder coat and paint do not bond well to oxidized surfaces
- Inspection rejection: Parts with visible rust may fail incoming quality inspection, even if the rust is superficial
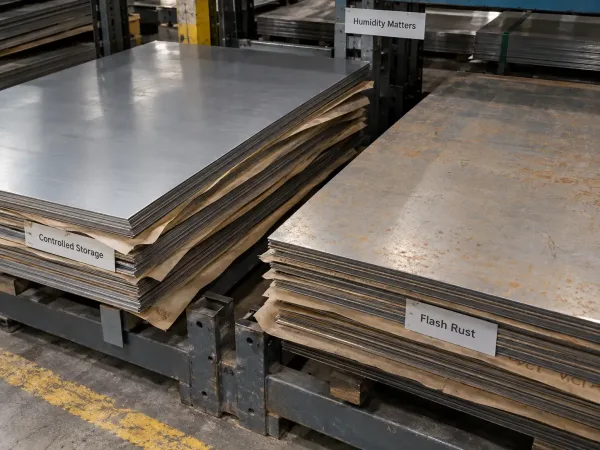
Dry steel sheets showing the difference between controlled storage and early-stage flash rust.
Storage Best Practices for Dry Stock
If you specify dry stock, plan for storage:
- Indoor storage with humidity below 50% RH
- Interleaving sheets with VCI (Vapor Corrosion Inhibitor) paper if storage exceeds 7 days
- FIFO rotation to prevent older stock from sitting in the back of the rack
- Visual inspection before loading onto the laser—any visible rust means the sheet needs cleaning or rejection
Impact on Downstream Processes
Welding Compatibility
Oil on sheet metal surfaces creates immediate problems for welding:
- MIG/TIG welding: Oil burns at the arc, producing porosity, spatter, and inconsistent bead appearance. Even a thin oil film can cause porosity that passes visual inspection but fails X-ray or dye penetrant testing.
- Laser welding: More sensitive to surface contamination than cutting. Oil residue in the weld zone produces micro-porosity and weakens the joint.
- Spot welding: Oil increases contact resistance variability, leading to inconsistent nugget formation.
Practical rule: If the part will be welded after laser cutting, specify dry stock or budget for degreasing before welding. The cost of weld rework from oil contamination almost always exceeds the cost of degreasing.
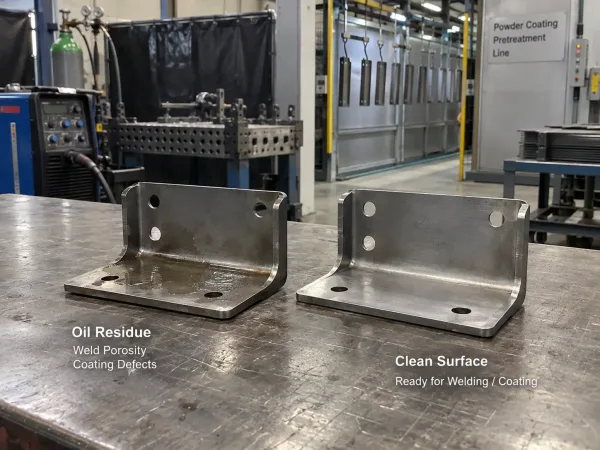 Comparison showing why oil must be removed before welding or powder coating sheet metal parts.
Coating and Painting Adhesion
Powder coating and liquid paint require a clean, oil-free surface for proper adhesion. Applying coating over oil residue results in:
- Fish-eye defects in paint films
- Delamination of powder coat under mechanical stress or thermal cycling
- Adhesion failure in salt spray testing (ASTM B117)
Most coating shops will degrease parts before processing, but this adds time and cost to the workflow. Specifying dry stock eliminates this step entirely.
How to Specify Surface Condition in Your RFQ
Ambiguity in surface condition requirements is one of the most common sources of RFQ clarification and production delays. To avoid this:
On the drawing, specify:
- Material callout with surface condition: e.g., “ASTM A1008 HRP&O” or “ASTM A1008 Dry”
- If dry stock with a rust inhibitor is acceptable: “Dry with VCI paper wrap”
- If oiled stock is acceptable but degreasing is required before welding: note “Degrease before welding per [standard or specification]“
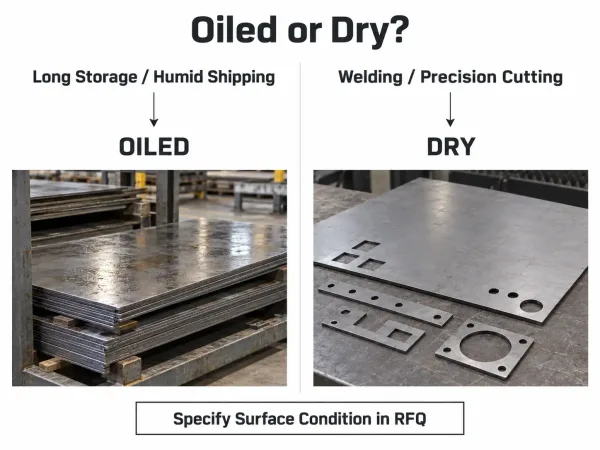
Simple engineering guide for choosing oiled or dry sheet metal based on storage and downstream processes.
In the RFQ, confirm with the supplier:
- What surface condition does the quoted price assume?
- Is degreasing included in the quoted price, or is it a separate line item?
- How will the material be stored between delivery and cutting?
- What is the maximum storage time before cutting?
- Does the supplier stock the specified surface condition, or is it a mill-order item with extended lead time?
Making the Right Choice for Your Project
When to Choose Oiled
- Long shipping distances or extended transit time: Oiled stock resists corrosion during ocean freight or multi-week ground transport
- Humid storage environments: If your facility cannot maintain below 50% RH, oiled stock is safer
- Parts that will be coated immediately after cutting: If the time between cutting and coating is less than 24 hours, degreasing is a single step that integrates naturally into the coating prep process
When to Choose Dry
- Parts requiring welding after laser cutting: Eliminates the degreasing step and reduces weld defect risk
- Controlled indoor storage: If your facility maintains stable humidity and temperature, dry stock stays clean without oil
- Smoke-sensitive environments: High-duty-cycle cutting operations or facilities with limited fume extraction benefit from oil-free stock
- Precision parts with tight edge quality requirements: Dry stock produces cleaner, more consistent cut edges
Key Takeaways
The oiled vs dry decision is not a surface preference—it is a process and cost decision that affects the entire manufacturing chain. Consider the full sequence: storage conditions, cutting performance, post-cut cleaning, and downstream compatibility with welding and coating.
For most general fabrication projects, either surface condition works with minor adjustments. For precision parts, welded assemblies, or coated components, the choice becomes more consequential and should be specified explicitly in the RFQ and on the drawing.
FAQ
Need help specifying the right surface condition for your next laser-cut parts order? Our engineering team can review your drawings and recommend the most cost-effective material and surface specification. [Request a DFM Review →]